Direct answer (120–180 words)
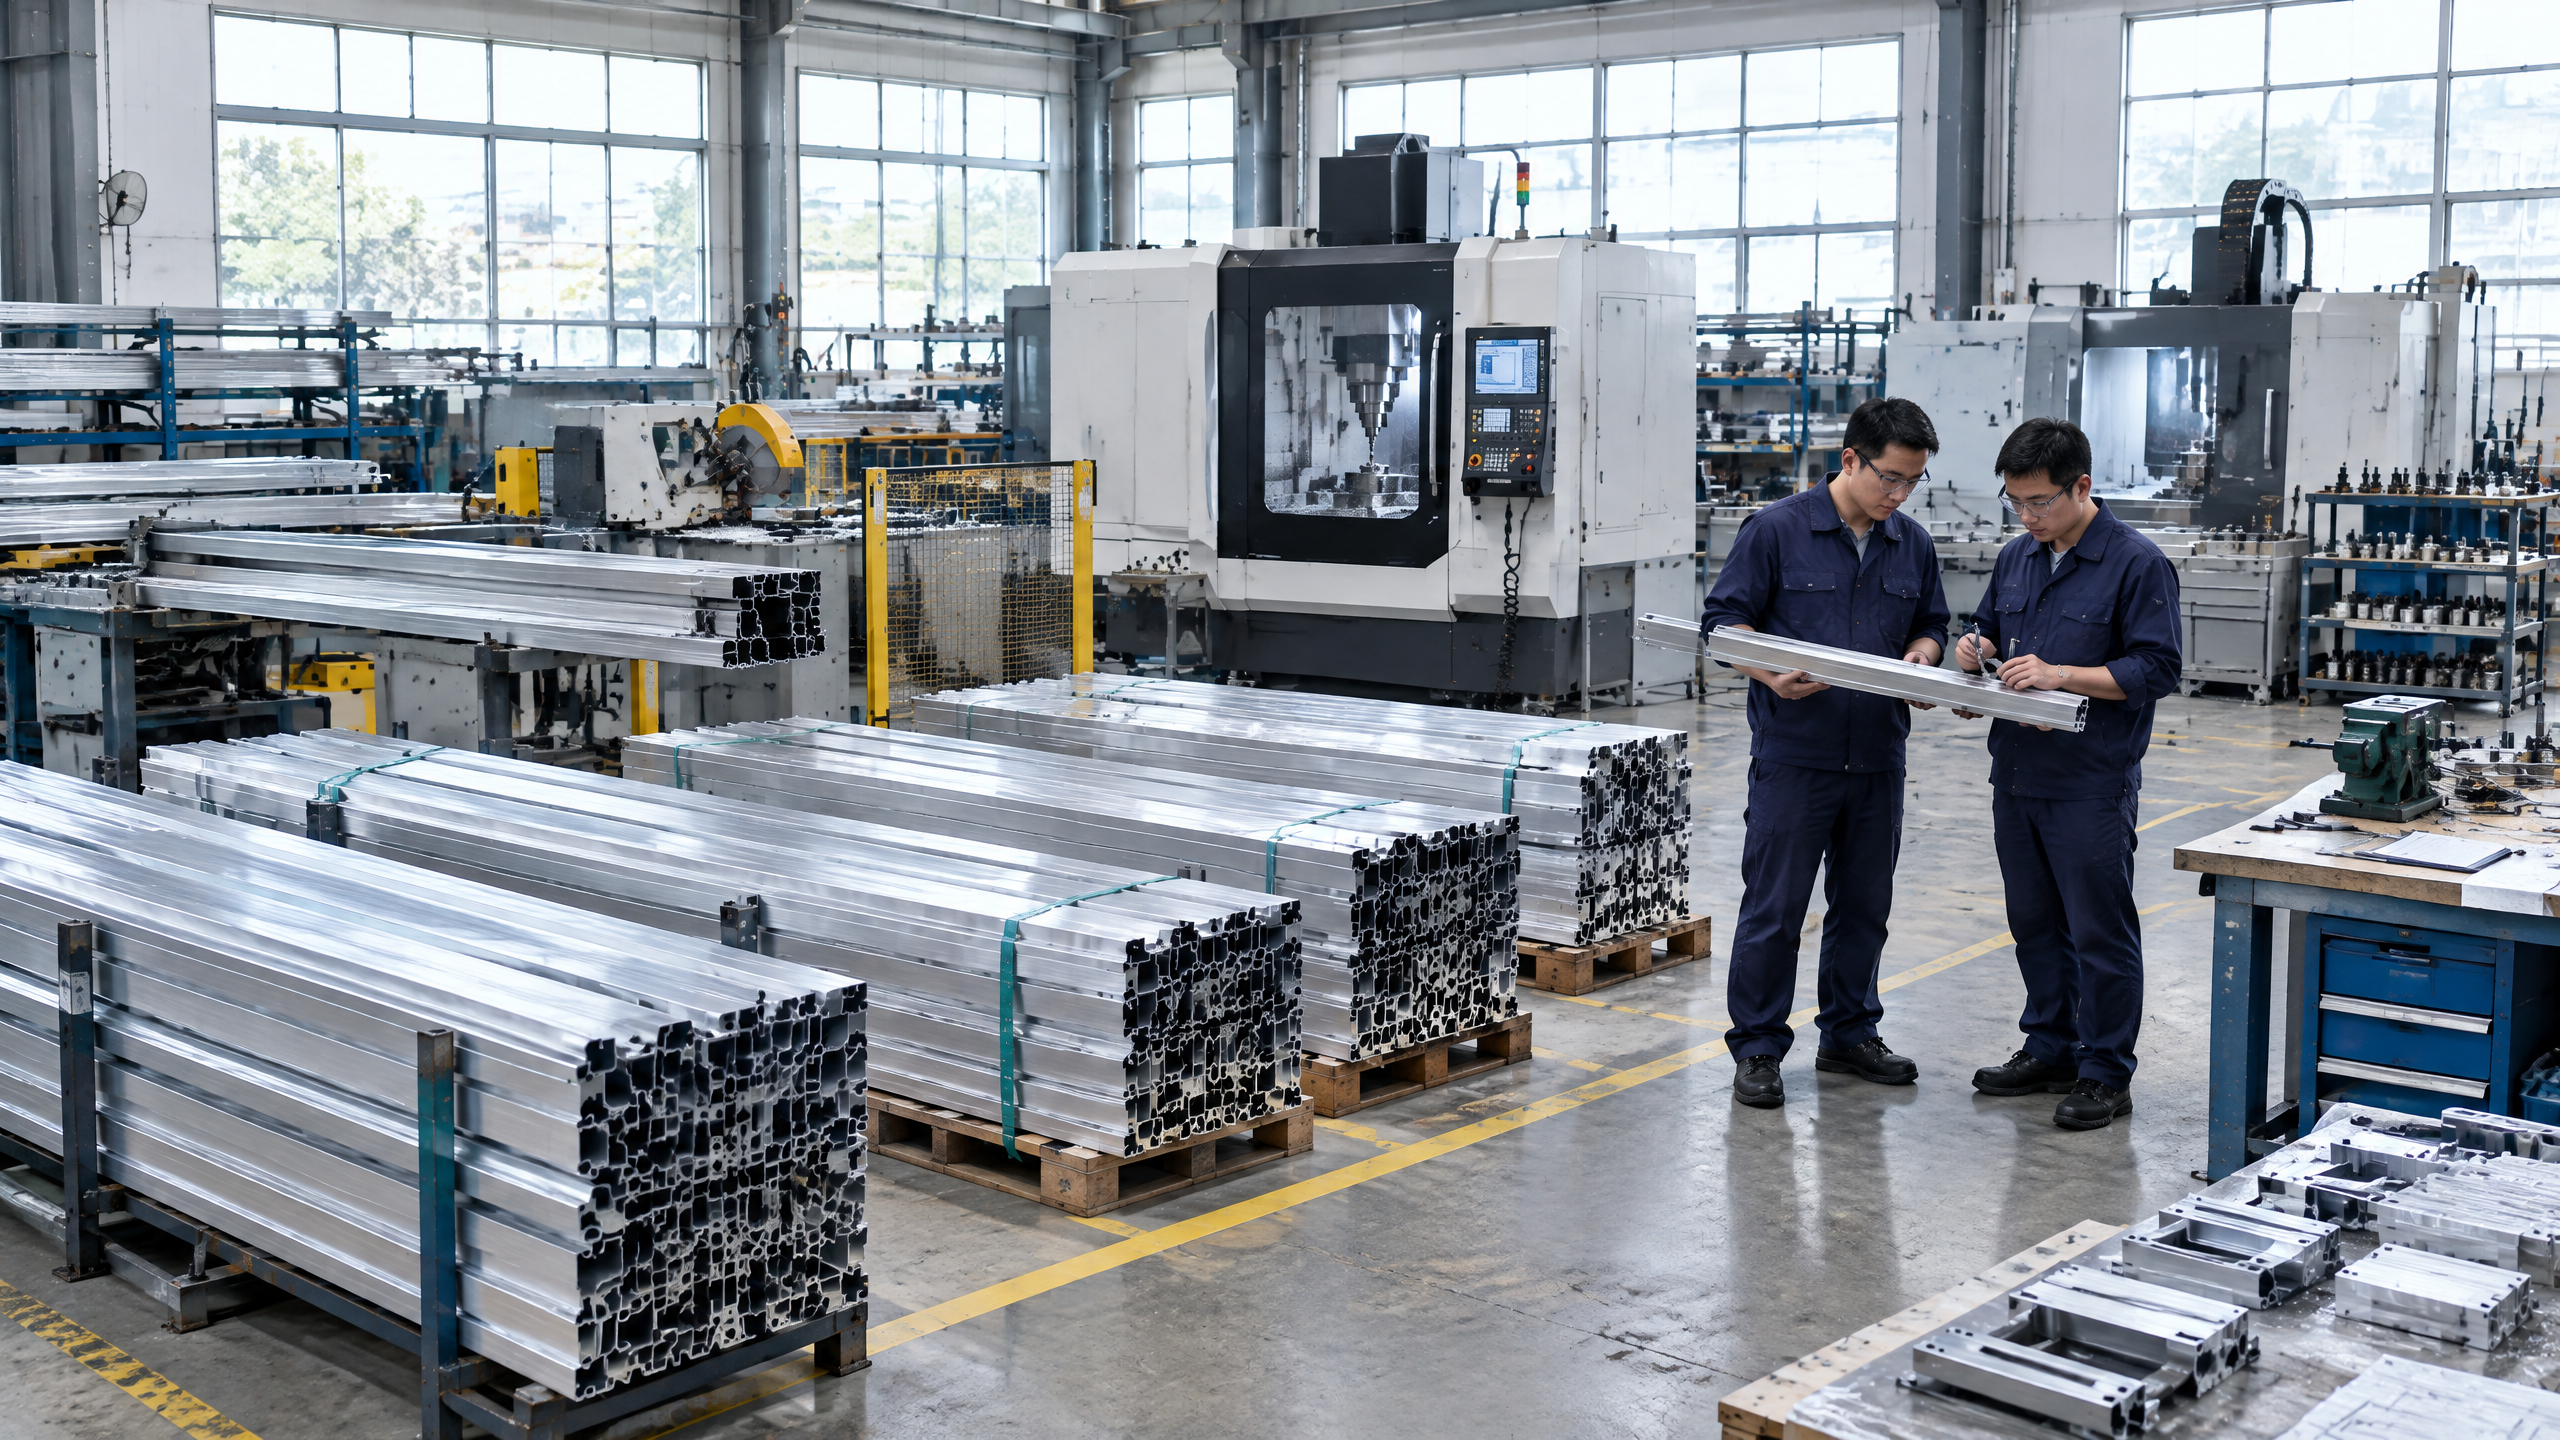
A project team should confirm that a commercial carport manufacturer factory capability matches the project’s technical scope, schedule and risk allocation before issuing purchase commitments. That means documented evidence of production capacity, quality systems, material traceability, welding and finishing processes, tooling tolerances, export packing coordination and logistics experience — together with clear contractual Incoterms and a delivery responsibility matrix that allocates risks. Verification should be evidence-led: factory quality documentation, inspection plans, sample production, and third‑party or client witness checks replace claims. Procurement controls must tie specification acceptance to contract milestones, pre‑shipment inspection and spare‑parts provision. Crucially, site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities. Use the six-step buyer workflow in this guide to align technical, contractual and operational checks before committing budgets.
Buyer context and scope boundary
Who this guide is for
- Distributors, architects, contractors, developers, solar EPCs and fleet operators looking to source architectural aluminium carports, commercial solar carports or industrial/fleet shelters from an overseas or domestic commercial carport manufacturer.
- Project teams responsible for procurement, technical evaluation, logistics and handover.
What "factory capability" covers (and what it does not)
- Covers: engineering resource (drawings, BIM/CAD), tooling and machining capacity (extrusion, folding, welding, CNC), surface treatment and finishing, material sourcing and traceability, quality control processes, packing and export services, production scheduling, test/assembly fixtures, staff competence and factory documentation.
- Does not cover: site structural capacity checks, foundation engineering, local permits, electrical grid connections, local installer certification, energy yield modelling, or final commissioning acceptance. These site-specific items require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Scope boundary for this procurement activity
- Factory capability assessment focuses on the supplier’s ability to deliver the agreed scope at the specified quality and schedule to the point of handover defined by Incoterms and the delivery responsibility matrix. It must be integrated with on-site design and approvals managed locally.
Related Carportiva systems
- Review Carportiva’s technical options and configurations at Carportiva system range and explore all systems for product fit before detailed factory assessment.
Core decision principle
Principle: Evidence trumps assertion
- The procurer’s primary decision rule is simple: accept factory capability when objective, verifiable evidence demonstrates the factory can meet the contracted technical scope, schedule and risk allocation.
- Evidence types: factory quality documentation (inspection plans, quality manuals), production records, material mill tests, traceability logs, capacity charts, sample assemblies, witnessable factory acceptance tests, photographic or video records of processes.
Risk allocation and procurement controls
- Align contractual terms (Incoterms, penalties, milestones) with the technical evidence. Use a delivery responsibility matrix to make ownership of goods, inspection and risks explicit.
- Project procurement controls should enforce acceptance gateways (engineering approval, pre‑production sample approval, factory acceptance test, pre‑shipment inspection) linked to payment milestones.
Regulatory and commercial alignment
- Ensure the factory’s processes comply with applicable standards and that the contract references inspection and acceptance criteria. Consider independent third‑party inspections where verification risk is high.
Planning inputs a project team must assemble
Before engaging in detailed factory capability checks, gather these planning inputs:
Mandatory project basis documents
- Project scope statement (exact items, PV module & inverter model if applicable).
- Site coordinates, climate and environmental parameters.
- Structural criteria (required wind/snow loads, corrosivity category).
- Architecture/clearance constraints, height, vehicular clearances.
- Expected lifetime and warranty obligations.
Technical inputs
- Module dimensions, frame mounting pattern and electrical routing needs for solar carports.
- Surface finish expectations (anodized, powder coat, galvanize).
- Foundation type and anticipated soil bearing capacities (if known).
- Tolerances, expected load cases and limiting deflections.
Commercial and schedule inputs
- Target delivery date, site access windows, staging and storage constraints.
- Budget envelope and purchase decision milestones.
- Preferred Incoterm and whether the buyer or seller handles export customs clearance.
Stakeholders to involve early
- Structural engineer, electrical engineer (for PV), local installer/erector, procurement lead, logistics coordinator, and a representative for asset owner operations.
Reminder: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Technical specification and interfaces
Define the technical scope in clear, verifiable terms
- Create a technical scope comparison that lists buyer requirements and desired tolerances against supplier responses. Use drawings, load cases and acceptance measurements.
- Include interface drawings for:
- Foundation anchor positions and tolerances.
- Module clamps and laying pattern for solar arrays.
- Electrical containment routes, cut‑outs and inverter/combiner interface points.
- Drainage and water run‑off if applicable.
Key technical areas to confirm with the factory
- Material specifications and traceability: aluminium alloy designations, plate and extrusion mill tests, fastener grades and galvanic isolation strategies.
- Structural performance: method statements for welding, bolting and fatigue-critical joints; calculation method and software used; design review evidence.
- Connections and tolerances: thread class, washer types, pre‑load torque values, slot sizes for adjustment, shimming and allowances for thermal movement.
- Surface finishes: process description (e.g., degreasing, chromate conversion, powder coat parameters) and expected coat thicknesses. For galvanizing processes and considerations, consult galvanizing guidance [1].
- Corrosion protection strategy for mixed metals and coastal environments.
- Electro-mechanical interfaces: cable tray routing, earthing/grounding design, conduit penetrations.
- Thermal expansion mitigation: sliding connections, expansion joints.
Technical scope comparison (decision table)
- Use the table below to compare specification items against supplier-provided evidence and acceptance criteria.
| Specification item | Evidence supplier must provide | Minimum buyer acceptance |
|---|---|---|
| Material grade & traceability | Mill certificates, batch numbers, traceability log | Mill certs for all structural items, batch traceability for critical fixings |
| Structural analysis | Calculation files, software used, load case list | Calculations matching buyer load cases and third‑party sign-off plan |
| Weld quality | Welding procedure (WPS), welder qualifications, NDT plan | WPS & welder records; NDT for critical welds as specified |
| Surface finish | Process description, coating thickness tests | Coating spec and sample test report; acceptance after inspection |
| Dimensional tolerances | Shop drawings & as-built checklists | Tolerances per contract and acceptable variance list |
| Module mounting compatibility | Interface drawing & sample assembly | Physical check with client module or verified module drawing |
Technical review checkpoints
- Require supplier to submit a technical query log and a master drawing register. All critical interfaces should be locked before fabrication, with changes through an agreed change control process.
Procurement and factory evidence
What to request during B2B supplier due diligence
- Company and factory identity: legal entity documents, factory address, site photos and floor plan.
- Organizational capacity: number of production lines, shift patterns, key personnel CVs (engineering, QA, production leads).
- Production capacity: current order book, lead‑time matrix for typical product volumes.
- Quality systems and certificates: factory quality documentation such as quality manuals, inspection procedures, NDT procedures and relevant ISO management system certificates (see ISO guidance [2]) where applicable.
- Traceability and material control procedures: BOM control, material receiving inspections, quarantine practices.
- Sample and prototyping approach: availability of pre‑production samples, sample approval process and acceptance criteria.
- Warranty and claims handling process: defined warranty terms and the operational process for claims and spare parts.
Factory quality documentation (required elements)
- Quality manual or QA plan that covers incoming material control, in-process inspections, final inspection, nonconformance controls and corrective action records.
- Inspection and test plans (ITPs) aligned to contract milestones (e.g., pre-production sample, first-off inspection, factory acceptance test, final inspection).
- Material certificates, weld logs, NDT reports where specified.
- Packing lists, export packing coordination records and photos of packing.
Export packing coordination and logistics
- Confirm supplier’s experience with export packing coordination for the intended destination (palletisation, sea-fastening, container stuffing, timber crating standards).
- Request packing method statements and photos of completed packing for similar projects.
- Verify compliance with destination import requirements and fumigation where timber is used; align the packing plan and incoterm responsibilities.
Delivery responsibility matrix
- Create a delivery responsibility matrix to make handover obligations explicit: who is responsible for packaging, export customs, freight booking, insurance and inland delivery. This is especially important for cross-border supply where multiple parties and risks exist.
Example delivery responsibility matrix (decision table)
| Responsibility / Incoterm | Seller responsibility | Buyer responsibility | Typical verification documents |
|---|---|---|---|
| EXW (Ex Works) | Make goods available at factory | All transport, export customs, insurance | Packing list, inspection & release note |
| FOB (Port of shipment) | Export customs clearance, deliver to vessel | Ocean freight, import customs, inland delivery | Bill of lading, export docs |
| CIF/CIP | Seller arranges transport & insurance to named point | Import formalities, inland delivery | Insurance policy, bill of lading, packing list |
| DAP/DDP | Seller delivers to named place (DAP)/clears import (DDP) | Unload (DAP) / none (DDP) | Arrival notice, customs clearance docs |
Note: Use Incoterms to define responsibilities and reference the International Chamber of Commerce Incoterms rules [3] in contracts. Match the Incoterm selection to your project risk appetite and logistics capability.
Verification methods and gatekeeping
- Factory visits: schedule audits focusing on the production area, material storage, finishing lines and packing station.
- Remote audit: structured video walk-throughs with a standard checklist when on-site visits are impractical.
- Third-party inspection: use independent inspection firms for sample testing, pre-shipment inspection or witnessing acceptance tests.
- Witness points and hold points: contractually define hold points where production cannot proceed without buyer approval (e.g., after sample approval or critical welding tests).
Commercial controls and contract alignment
- Embed the technical scope comparison, factory quality documentation, export packing coordination, delivery responsibility matrix and inspection plan into purchase orders and supply agreements.
- Use retention, milestone payments and performance guarantees where appropriate to enforce supplier performance.
Compliance and customs readiness
- Confirm product classification, import documentation needs and any local approvals required for erection or operation. For import rules and documentation basics see customs guidance [4].
- Ensure supplier provides commercial invoices, packing lists, certificates of origin and any required conformity declarations.
Site installation, commissioning and operations
Handover expectations and installer interface
- Define the installation scope in the contract: supply-only, supply-and-install, or supply-and-supervise. Clarify responsibilities for lifting equipment, temporary works and site safety.
- Provide detailed erection drawings, anchor bolt templates and lifting points in advance of delivery. Coordinate arrival of fixings and embedded items with concrete pours and anchor setting.
Pre‑assembly, site storage and handling
- Plan for safe on-site storage to avoid damage and corrosion. Provide supplier packing and unpacking instructions to site teams, and confirm required handling equipment (cranes, forklifts).
- Agree on sequence of deliveries to match lifting, staging and installer availability; consider short‑term protective storage for modules and sensitive components.
Commissioning, testing and acceptance
- For solar carports: commissioning includes electrical continuity, earthing resistance measurement, PV string-level checks and inverter commissioning usually by the electrical contractor or EPC. Define responsibilities clearly.
- Site acceptance tests should mirror factory acceptance criteria where applicable (e.g., dimensional tolerances, mechanical operation). Capture acceptance in a site handover certificate.
Operation and maintenance handover
- Require the supplier to provide as-built drawings, maintenance manuals, spare parts list and a recommended routine inspection schedule.
- Consider a spare parts kit for fasteners and critical components, and include lead times for replacement parts.
Training and long-term support
- Specify training requirements for local installers and maintenance teams: lifting and erection, torque values, re-tensioning intervals, corrosion checks, and electrical safety for PV systems.
- Ensure warranty and spare parts support terms are contractually defined, and confirm response times and local support arrangements.
Reminder: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Implementation risks and mitigation
Common procurement and factory-to-site risks
- Technical non-conformance: parts that do not meet tolerance or material specifications.
- Packaging damage and sea/road damage due to inadequate export packing.
- Delays due to factory bottlenecks or material shortages.
- Customs holds or missing documentation causing port delays.
- Mismatch between foundation template and actual anchor positions on site.
- Incompatible module or electrical interfaces when PV modules are supplied by a separate party.
Mitigation measures and contractual levers
- Pre‑production sample and first-off inspection: require a sample production run and client approval before full production.
- Factory acceptance test (FAT): define FAT scope and witness rights. Use third-party inspectors where necessary.
- Packing approval: require photos of packing and sample crate for approval prior to shipment; specify packing materials and sea-fastening methods.
- Inspection and hold points: insert contractual hold points before shipment and before production of subsequent batches.
- Delivery responsibility matrix and chosen Incoterm: allocate customs, insurance and freight responsibilities so there is clarity who pays and who assumes risk.
- Retentions and performance bonds: use financial levers for high-value projects where supplier performance risk is material.
- Spare parts strategy: secure long‑lead spare parts at contract stage and define minimum on-site spares.
Example risk mitigation checklist
- Technical sign-off document signed by both parties before fabrication.
- A detailed delivery schedule with contingency windows.
- Pre-shipment inspection by an independent inspector.
- Confirmed logistics plan with carrier and port handling instructions.
- Local erection team engagement and pre‑site survey report.
Project procurement controls
- Embed a document control log and change control board into the project to manage revisions to drawings or scope.
- Use project procurement controls to ensure traceability of approvals, inspection outcomes and non‑conformance records.
Six-step buyer workflow for confirming factory capability
Use this named six-step workflow as a procedural template to reduce risk and accelerate decision making.
Step 1 — Define the documented project basis (Inputs & scope)
- Deliverables: scope statement, site data, module or vehicle dimensions, environmental load cases, timeline and budget constraints.
- Action: circulate to technical stakeholders and confirm who will sign technical acceptance.
Step 2 — Shortlist suppliers and run B2B supplier due diligence
- Deliverables: supplier pre-qualification pack (company info, factory photos, capacity statement, references).
- Action: score suppliers against capability and commercial fit.
Step 3 — Issue technical RFQ and run a technical scope comparison
- Deliverables: RFQ package, technical scope comparison table, required evidence list.
- Action: request factory quality documentation, mill certificates, ITPs and sample proposals. Use the technical scope comparison table to compare responses.
Step 4 — Audit, validate and sample
- Deliverables: factory audit report, sample parts, FAT scope.
- Action: perform on-site or remote factory audit; approve pre-production sample and ITP. Confirm export packing coordination.
Step 5 — Contract, confirm delivery responsibility matrix and project procurement controls
- Deliverables: signed contract, PO with hold points, delivery responsibility matrix, agreed Incoterm.
- Action: set payment milestones tied to acceptance gates and inspections.
Step 6 — Supervise production, inspect and handover
- Deliverables: pre-shipment inspection report, packing photos, shipping docs, as-built drawings and handover certificate.
- Action: witness packing, verify documents for customs, coordinate arrival and installer readiness.
Timing and governance
- Attach expected durations to each step and assign owners. Use a central project file and require decision sign-off at each gateway.
Link resources
- For procurement templates and sourcing checklists see sourcing guides. Review product fit at Carportiva system range.
Frequently asked questions
Q: What is the single most important evidence that a factory can meet my project? A: A complete set of aligned, verifiable documents: approved shop drawings, material mill certificates, inspection and test plans, and a pre‑production sample or first-off part approved by the buyer or third-party inspector.
Q: How should I allocate Incoterms for a carport with sensitive components? A: Choose an Incoterm that matches your logistics capabilities and risk appetite. If you want the seller to manage export and main carriage to a port/terminal, use FOB/CIF; for buyer-controlled logistics consider EXW or FOB with buyer arranging main carriage. Use the delivery responsibility matrix in the contract. Reference Incoterms rules [3].
Q: Do I need a factory visit for every supplier? A: Factory visits are highly recommended for strategic or high-value suppliers. Where visits are impractical, use structured remote audits, third-party inspections and detailed photographic evidence.
Q: What are reasonable factory hold points? A: Typical hold points: approval of final shop drawings, approval of pre-production sample, completion of critical welding/NDT, completion of FAT and confirmation of packing method before shipment.
Q: How do I verify surface finish quality remotely? A: Require process descriptions, coating thickness measurements, photographic evidence of finished parts, and third-party lab test reports for critical finishes. Consider requesting sample coupons for lab analysis.
Q: Who is responsible for customs and import documentation? A: That depends on the chosen Incoterm and the delivery responsibility matrix. Confirm in contract whether the seller will provide export and import clearance and supply necessary certificates. For import documentation basics see guidance [4].
Q: What specialist tests might I require? A: Potential tests include galvanizing thickness measurement, coating adhesion tests, weld NDT (magnetic particle, dye-penetrant), material hardness, and load testing of critical members. Specify required tests in the ITP.
Q: How do I manage spares and obsolescence? A: Contractually require a spare parts list, agreed lead times for critical items, and options for local stocking or consignments. Include part numbers and supplier drawings in the handover package.
Q: Can Carportiva assist with factory capability queries? A: For product-specific information and system options consult the Carportiva system range and contact Carportiva sales via /inquiry or info@carportiva.com.
Two decision tables to support sign-off
Decision table — Factory evidence vs. acceptance action
| Evidence provided | Accept as-is | Require clarification | Hold/Reject |
|---|---|---|---|
| Complete mill certificates and traceability for all structural parts | ✓ | ||
| Shop drawings not signed or missing anchor templates | ✓ (require revision) | ||
| Pre‑production sample approved and dimensionally compliant | ✓ | ||
| No packing photos for sea freight or no packing plan | ✓ (require) | ||
| Factory quality documentation with defined ITPs and hold points | ✓ | ||
| Missing NDT records for specified critical welds | ✓ (require NDT) | ||
| Factory unable to meet required delivery window | Hold until schedule resolved |
Decision table — Logistics and responsibility selection
| Factor | Recommendation | Procurement action |
|---|---|---|
| Buyer has strong local logistics capability | Consider EXW or FOB | Ensure buyer arranges export and import customs |
| Buyer wants seller to manage cross-border freight | Consider CIF/CIP or DAP | Require seller to supply freight & insurance docs |
| High damage risk items or complex packing needs | Require supplier to provide export packing coordination and photos | Make packing approval a hold point |
| Long lead time components | Require confirmed production slots and buffer | Include stock or cemented delivery windows in contract |
Conclusion
Assessing commercial carport manufacturer factory capability is a project-critical activity that combines technical verification, contractual clarity and logistics planning. The single best protection is an evidence-led procurement process that ties factory quality documentation, technical scope comparison, pre‑production sample approval and a clear delivery responsibility matrix to contract milestones enforced by project procurement controls. Use the six-step buyer workflow in this guide to create defensible acceptance gates and reduce implementation risk.
Remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
For product fit and technical options consult Carportiva system range and all systems. For procurement templates and further sourcing materials see our sourcing guides. For enquiries and support use /inquiry or contact info@carportiva.com.
References (selected)
- American Galvanizers Association: guidance on hot-dip galvanizing and corrosion protection. [1]
- International Organization for Standardization: management system standards and certification context. [2]
- International Chamber of Commerce Incoterms rules: for contractual delivery terms. [3]
- U.S. Customs and Border Protection basic import/export guidance for documentation and classification. [4]
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion