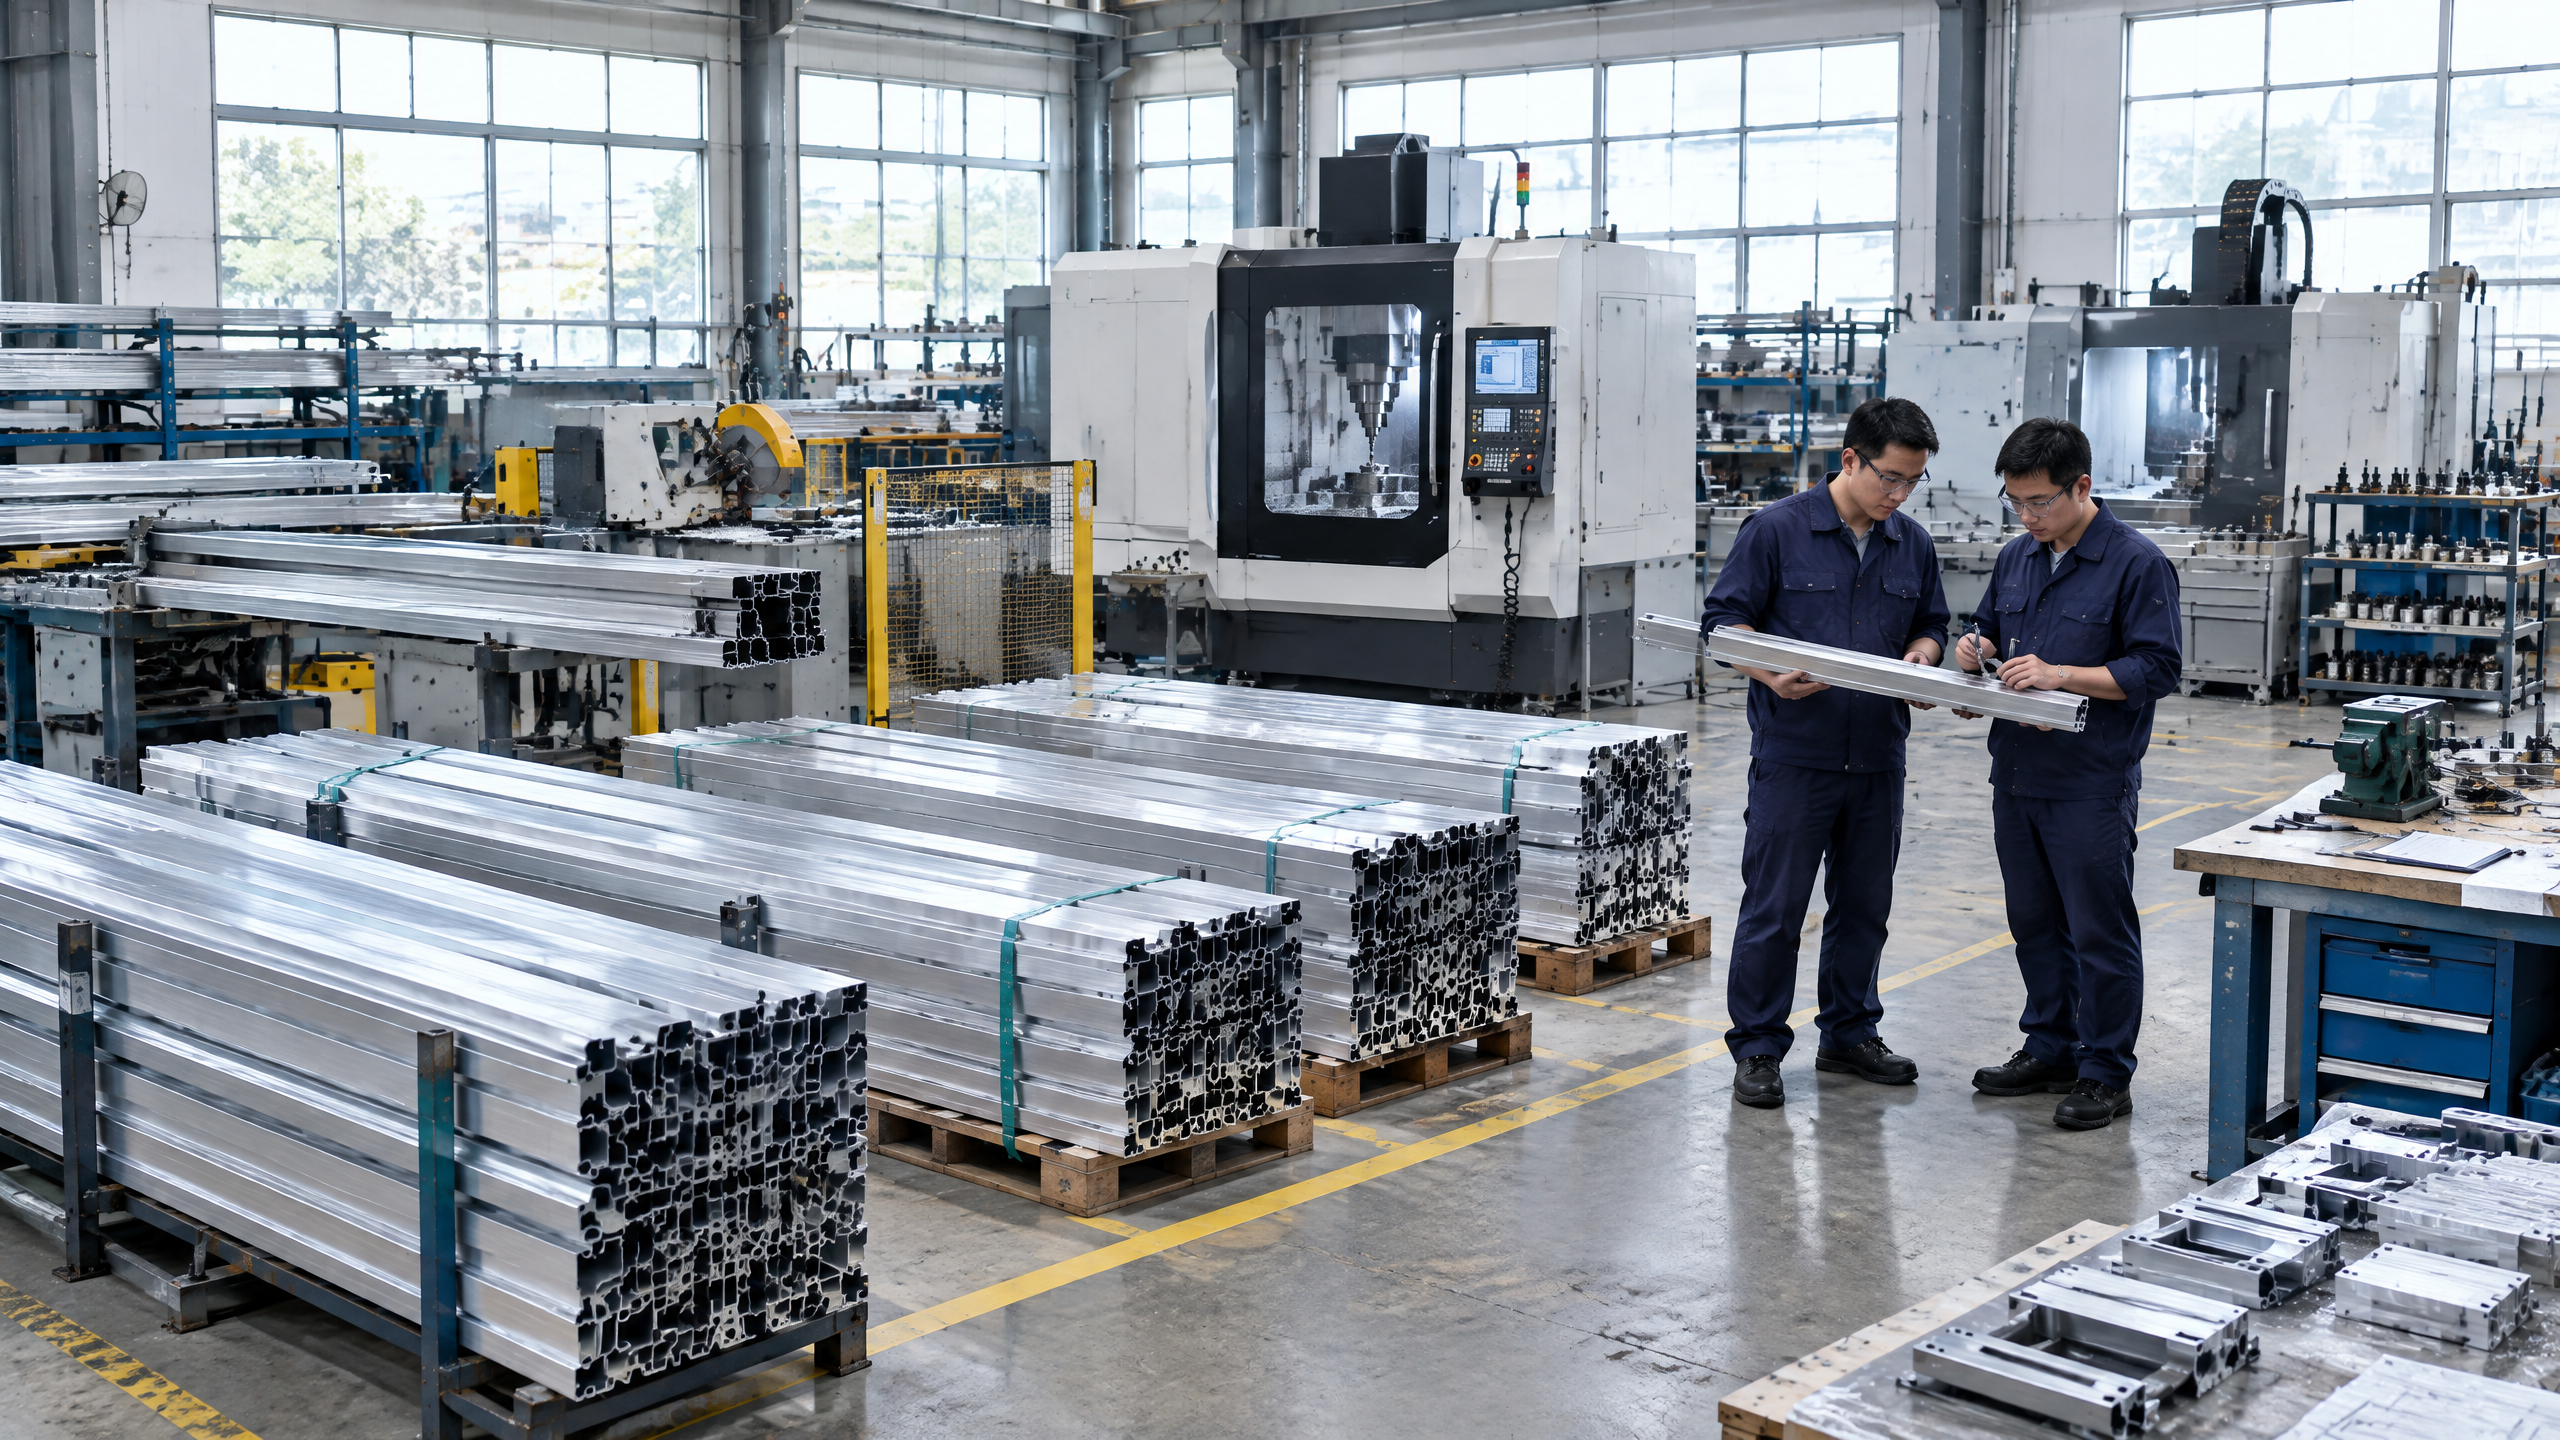
A carport quality control factory inspection matters when the balance of project risk, technical complexity and supply-chain distance means documentation review and post-manufacture verification are insufficient to protect buyer outcomes. Use inspection when you need independent verification of materials, processes and packing that directly affect structural safety, surface performance, electrical integration, transport damage risk or contractual handover obligations. Typical triggers include high-value or long-lead projects, bespoke structural designs, integrated solar systems, multi-site rollouts where supplier batches must be consistent, and instances where local installation teams cannot rework manufactured deviations on site. Inspections complement B2B supplier due diligence, technical scope comparison and factory quality documentation: they reduce ambiguity in the delivery responsibility matrix and are part of project procurement controls that turn supplier promises into verifiable evidence. Always align any inspection plan with a documented project basis and qualified local professionals for structural, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty assessments.
Buyer context and scope boundary
Audience and product scope
- This guide is for global B2B buyers: distributors, architects, contractors, developers, solar EPCs and fleet operators procuring architectural aluminium carports, commercial solar carports and industrial/fleet vehicle shelters.
- Carportiva products, including the Carportiva system range, cover modular aluminium structures and integrated solar mountings whose quality depends on materials, shop fabrication, surface treatment and packing for export.
What this guide covers
- The central subject is carport quality control factory inspection: when it matters, what it should include, and how to fold it into procurement and project controls.
- Secondary topics include B2B supplier due diligence, technical scope comparison, factory quality documentation, export packing coordination and delivery responsibility matrix considerations.
What this guide does not cover in detail
- Site-specific engineering design (structural capacity, foundations), electrical design for solar systems, regulatory approvals, local permits, energy-yield modelling, precise pricing, and warranty interpretation. These items require a documented project basis and local qualified professionals, installers, utilities and authorities; include them in procurement scope but complete them outside factory inspection alone.
Scope boundary statement (required)
- Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities. Factory inspection is one control among many and does not replace local engineering, permitting or on-site commissioning.
Core decision principle: when to inspect, when not to
Decision principle
- Carry out a carport quality control factory inspection when the expected cost of failure (rework, delay, non-compliance, safety exposure, warranty disputes, installation disruption) exceeds the marginal cost and time of inspection plus any corrective works.
- Where the risk is low and supplier confidence is demonstrable through repeatable evidence, remote verification and strong factory quality documentation may be sufficient.
Triggers that typically require inspection
- Custom structural designs, complex attachments (canopies, brackets, anchors).
- Integrated electrical/solar systems where module and racking alignment or cable preparation affect commissioning.
- First production run with a new tooling, new coating method or new galvanizer.
- High-value or time-critical shipments where delays or damage are expensive.
- Multi-site rollouts needing batch consistency.
- Weak or incomplete B2B supplier due diligence.
Situations where inspection is often optional
- Catalog, off-the-shelf systems with short lead times and reputable repeat suppliers with transparent factory quality documentation and production history.
- Low-value purchases where onsite correction is cheaper than inspection.
Reference standards and commercial rules
- Use ISO management system references as a basis for manufacturing and quality process expectations when relevant [2].
- Reference Incoterms for delivery responsibilities that affect what inspection must verify at factory vs. at port or destination [3].
Planning inputs: what to prepare before booking an inspection
Minimum procurement inputs
- Documented project basis: final drawings, structural loadings, foundation details, electrical single-line and earthing requirements, module/rack interface details, and installation method.
- Supplier technical package: as-built drawings, bill of materials (BOM), production drawings, material certificates, process specifications.
- Contractual terms: inspection scope, acceptance criteria, hold points, corrective action timelines, payment milestones, and agreed Incoterm.
Project stakeholders to involve
- Buyer procurement lead and commercial manager.
- Project engineer/structural engineer (local) and electrical designer for solar integration.
- Quality manager or third-party inspector (TPI) specifying sampling and test verifications.
- Logistics lead to manage export packing coordination and shipping hold points.
Sampling and timing decisions
- Define sample size and selection method (random, first-piece, final batch).
- Schedule inspection relative to production (mid-run for process checks, pre-shipment for packing and final checks).
- Specify photographic and documentation deliverables for records.
Decision table — inspection triggers and suggested action
| Trigger condition | Suggested action |
|---|---|
| New supplier or first production run for project | Full carport quality control factory inspection (pre-shipment + mid-process check) |
| Repeat supplier with full factory quality documentation and positive history | Remote document review + targeted pre-shipment check |
| Integrated solar racking and electrical pre-installation required | Include electrical-kitted inspection and cable harness checks in factory inspection |
| Low-value standard catalog units, nearshore supplier | Document review and random sampling on arrival; inspect only if evidence suggests risk |
Mandatory disclaimer
- Structural and electrical items in the project inputs must be validated by local qualified professionals; factory inspection validates fabrication to supplied documents but does not replace site verification or approvals.
Technical specification and interfaces to verify
What the inspection must verify technically
- Dimensional and tolerance compliance to drawings (critical for bolted interfaces and preformed foundations).
- Material conformity: alloy grades, thickness, and material certificates for aluminium, stainless, steel fixings and fasteners.
- Surface treatments: anodizing thickness, powder-coat system and preparation, galvanizing quality where applicable.
- Weld quality, joint design and thread engagement for anchor bolts and structural connectors.
- Pre-assembly and kit completeness: bolt sets, brackets, pre-cut rails, gaskets, sealing materials.
- Solar-specific checks: module clamp positions, spacing, cable boxing, combiner/pre-assembly kits if delivered factory-ready.
Evidence types to collect
- Factory quality documentation such as mill test certificates, welding procedure specifications (WPS), non-destructive test (NDT) records, and surface treatment certificates.
- Dimensional measurement reports, calibrated gauge evidence, and site photos showing key tolerances.
- Component packaging photos and marking records for export packing coordination and traceability.
Coating and corrosion interfaces
- If hot-dip galvanizing is specified, confirm galvanizer documentation and batch traceability; consult galvanizing guidance for acceptable practices where needed [1].
- For aluminium finishes, verify pre-treatment, thickness values and cure parameters for powder coatings.
Electrical interfaces and key limits
- Cable lengths and factory-terminated harnesses must match single-line diagrams; factory inspection should verify connector types, labels and protection of cable ends against moisture.
- Factory-prepared inverter skids or junction boxes should be verified for ingress protection claims and mounting interfaces; final electrical certification remains a local responsibility.
Technical scope comparison
- Before inspection, complete a technical scope comparison between buyer requirements and supplier offer: list deviations, options and defined tolerances; use this comparison as the inspection checklist.
Procurement and factory evidence: what counts, what is optional
Core evidence the buyer should require
- Factory quality documentation: complete manufacturing routings, material certificates, QA/QC checklist, process control records, and final inspection reports.
- Dimensional verification reports with calibrated equipment traceability.
- Test reports (if specified): weld tests, pull-out tests for anchoring if required by project, and coating adhesion or thickness tests.
- Photographic records of completed assemblies, marking, and export packing.
Decision table — evidence acceptance matrix
| Evidence type | Acceptable as primary proof | Acceptable as secondary / conditional |
|---|---|---|
| Mill test certificates with trace number | Yes | No |
| ISO 9001 or equivalent supplier certificate | Yes (process evidence) | Must be paired with factory quality documentation |
| Final inspection report signed by factory QA | Yes | Only if aligned with buyer checklist |
| Third-party inspection report (photos + signed) | Yes | Preferred for high-risk projects |
| Random shipment photographic evidence only | No | Only if combined with sample testing on arrival |
B2B supplier due diligence
- The inspection should be part of a broader B2B supplier due diligence process that includes financial checks, capacity verification, previous project references, process capability and quality-system evidence [2].
- Due diligence informs the degree of in-person inspection required and the selection of third-party inspectors.
Using third-party inspectors vs. in-house
- Third-party inspectors bring independence and consistent reporting; ensure their scope and acceptance criteria are contractual.
- In-house inspection can be used when the buyer has strong technical capability on staff and clear contractual authority to enforce corrective action.
Documentation control and versioning
- Require all factory quality documentation to carry project identifiers, revision numbers and date stamps.
- Keep an auditable trail: PO → drawings → final drawings → inspection checklist → inspection report → non-conformance report (NCR) and corrective action closure documents.
Standards and regulatory references
- Align inspection acceptance criteria with recognized standards where applicable (material standards, weld codes, coating standards) and reference ISO for expected quality management practices [2].
Mid-article CTA
- For tailored procurement support and to discuss how factory inspection integrates with your project procurement controls, contact /inquiry or info@carportiva.com.
Export packing coordination and logistics interfaces
Why export packing matters
- Damaged parts or missing kits due to inadequate packing are a frequent cause of installation delay and extra cost.
- Packing quality is often best verified at factory as part of pre-shipment inspection; coordination reduces repacking at port and claims on arrival.
What to verify in export packing coordination
- Packing configuration against packing list and BOM; all kits and small parts must be counted and bagged or boxed per kit.
- Securing and protection for long extrusions (timber or steel spacers, corner protection, dunnage), and prevention of galvanic contact between dissimilar metals.
- Lashing points for sea freight; container load patterns and blocking to prevent movement.
- Marks, labels and documentation required by destination customs and carriers.
Delivery responsibility matrix and Incoterms
- Clearly define responsibilities for packing, loading, claims and insurance in the delivery responsibility matrix. Reference ICC Incoterms to determine which party is responsible for export packing, clearing and delivery obligations [3].
- For example, under some terms the seller is responsible for export packing and carriage to the named point; under others the buyer assumes more responsibility and must enforce specific packing standards with the supplier.
Packing checklist example
- Packing list verified and signed
- Fragile items wrapped and boxed
- Bolt kits labeled and placed in tamper-proof bags
- Long members protected with edge protection and lashings
- Container stuffing photos from multiple angles
Customs and import considerations
- Ensure export packing includes the documentation and marking required by the destination country's customs authority; check importer guidance where relevant [4].
- Early coordination with freight forwarders reduces surprises in documentation requirements.
Site installation, handover and operations interface
What factory inspection does not replace
- Factory inspection confirms fabrication to supplied documents and packing quality; it does not replace site checks for foundations, local approvals, final structural verification, electrical commissioning or energy yield verification.
Handover expectations
- Agree contractual handover points: when does responsibility transfer from seller to buyer? The delivery responsibility matrix must state this clearly and is confirmed by inspection records and signed delivery documents.
- Ensure documentation delivered with shipment includes as-built drawings, installation manuals, torque tables, and maintenance schedules.
Site installation QA
- Before installation, verify received goods against the packing list and factory inspection report.
- Use incoming inspection to check for damage, missing parts, and conformity; keep photographic evidence and reserve rights to reject shipments per contract.
Commissioning and operations
- For solar carports, commissioning and performance verification are site activities requiring qualified electricians and possibly energy-yield modelling by specialists.
- Establish maintenance intervals and record-keeping that align with factory recommendations and local conditions (salt spray, UV exposure, temperature swings).
Warranty and claims
- Factory inspection reports strengthen both warranty and claim positions by providing pre-shipment evidence.
- Warranties often require proper installation and maintenance; local installers must be qualified and approvals obtained for warranty validity.
Implementation risk: common failures and mitigations
Top implementation risks
- Dimensional non-conformance leading to on-site rework.
- Surface treatment failures (insufficient pretreatment, inadequate coating thickness) causing early corrosion or aesthetic failures.
- Missing bolt kits or mismarked parts disrupting installation sequence.
- Packing damage during transport leading to scratches, dents or bent extrusions.
- Electrical pre-assembly errors that complicate commissioning.
- Customs holds and documentation mismatch delaying delivery.
Mitigation strategies
- Use detailed technical scope comparison and build inspection checklists that cover critical dimensions and interfaces.
- Specify and verify factory quality documentation and third-party lab tests when coatings or galvanizing are critical.
- Require photographic records of packing and container stuffing; if risk is high, require sealing and inspection hold until third-party verification.
- Include contractual hold points and acceptance criteria with remedies and corrective-action timelines.
- Maintain an agreed delivery responsibility matrix that allocates risks and defines who pays for corrective packing or rework.
Contractual levers and payment milestones
- Structure payment milestones to include retention until final acceptance or after successful on-site verification.
- Use partial payments on documentation completion, and final payment only on satisfactory inspection or corrected NCR closure.
Insurance and claims
- Clarify insurance responsibilities for transit damage and who will file claims; ensure that required packing standards are met to comply with insurers’ endorsements.
Six-step buyer workflow: a named process for inspection-led procurement
This six-step buyer workflow converts the decision principle into executable activities that integrate carport quality control factory inspection into project procurement controls.
- Define project basis and technical scope comparison
- Deliverable: approved project drawings, single-line electrical diagrams, BOM, and a formal technical scope comparison showing deviations from supplier proposals.
- Responsible: Buyer project engineer + procurement.
- Supplier due diligence and document pre-qualification
- Deliverable: supplier capability summary, ISO/process evidence, sample factory quality documentation, and references.
- Responsible: Procurement + commercial team.
- Note: Perform B2B supplier due diligence to decide inspection depth.
- Contractualize inspection scope, acceptance criteria and delivery responsibility matrix
- Deliverable: contract annex with inspection checklist, sampling rules, remedies, and defined Incoterm responsibilities.
- Responsible: Legal + procurement + project manager.
- Reference: Incoterms for responsibilities [3].
- Pre-production and mid-process checks
- Deliverable: mid-production dimensional and process check reports; corrective requests if deviations found.
- Responsible: Buyer inspector or third-party inspector + supplier quality.
- Pre-shipment factory inspection (carport quality control factory inspection)
- Deliverable: final inspection report, photographic record of packing, verified packing list and container stuffing photos.
- Responsible: Third-party inspector or buyer QA + supplier.
- Incoming inspection, site acceptance and NCR closure
- Deliverable: incoming goods inspection report, verification of on-site fit with foundations, signed acceptance, or logged NCRs with closure records.
- Responsible: Site installation team + buyer project engineer.
Decision roles matrix (example)
| Step | Buyer role | Supplier role | Inspector role |
|---|---|---|---|
| 1: Scope definition | Lead | Provide design inputs | - |
| 2: Due diligence | Lead | Provide documents | - |
| 3: Contracting | Lead | Agree | - |
| 4: Mid-process check | Support | Provide access | Execute inspection |
| 5: Pre-shipment inspection | Support | Facilitate | Execute & report |
| 6: Incoming inspection | Lead | Receive corrective action | Verify closure |
FAQ
Q: Is a factory inspection always necessary for a carport purchase? A: No. It depends on project risk, supplier history and scope complexity. Use the core decision principle: inspect when the cost of failure exceeds inspection costs. For many standard off-the-shelf systems with mature suppliers, document review and spot checks can be sufficient.
Q: Who should pay for the inspection? A: That depends on commercial negotiation and contract terms. Often buyers pay for third-party inspections in high-risk projects; in some contracts the seller bears inspection costs if defects are confirmed. The delivery responsibility matrix and Incoterms affect who pays for packing and loading [3].
Q: Can remote or video inspections replace in-person factory inspection? A: Remote inspections can be a useful supplement for low-to-moderate risk projects or for mid-process updates. They are less reliable for precise dimensional checks, coating thickness tests or destructive testing, but can reduce travel and provide oversight.
Q: What is the role of factory quality documentation? A: factory quality documentation is the documentary evidence that production followed specified materials, processes and tests. It reduces the need for intrusive inspection when complete and trustworthy; however, documentation must be audited and traceable.
Q: How do I handle non-conformances found at the factory? A: Require a documented non-conformance report (NCR) with root cause, corrective actions and a timeframe for closure. For critical non-conformances, require rework at the factory or reject the batch per contract.
Q: How much sampling is required during inspection? A: Sampling depends on project risk, batch size and contractual acceptance sampling plans. Define sampling methods in the inspection scope and, when in doubt, follow recognized sampling standards or agree conservative samples for structural or safety-critical items.
Q: Does factory inspection guarantee on-site fit? A: No. Factory inspection verifies conformity to the supplied drawings. On-site fit depends also on correct foundations, site tolerances and installer execution. Structural and foundation checks remain local responsibilities.
Q: What documentation should travel with shipment for installation teams? A: As-built drawings, torque charts, installation manuals, packing list, factory inspection report, material certificates, maintenance guide, and any electrical wiring diagrams.
Q: How does packing verification reduce claims? A: Verifying export packing at the factory ensures kits are complete, properly protected and loaded in a way that reduces movement and damage. Photographic evidence from stuffing further supports claims if damage occurs in transit or at destination.
Q: If my supplier has ISO 9001, do I still need inspection? A: ISO 9001 indicates a quality management system but does not guarantee product compliance to specific project tolerances. Use ISO certification as part of B2B supplier due diligence but verify with project-aligned factory quality documentation and targeted inspection where warranted [2].
Q: What legal or regulatory standards apply to deliveries? A: Project-specific standards and local regulations apply; use contractually agreed acceptance criteria. For commercial rules of delivery and responsibility, rely on Incoterms [3]. For customs and import preparation, consult destination customs guidance [4].
Q: Who signs off inspection reports? A: Inspection reports should be signed by the inspector and countersigned or acknowledged by factory QA; contractual acceptance is governed by the delivery responsibility matrix and related contract clauses.
Conclusion
A carport quality control factory inspection matters when it meaningfully reduces the risk of cost, schedule or safety failure relative to its cost and lead-time impact. Integrate inspection into your B2B supplier due diligence and project procurement controls by using a structured technical scope comparison, requiring robust factory quality documentation, and making packing verification and a delivery responsibility matrix explicit in contract terms. Use the six-step workflow to operationalize inspection and ensure inspections are followed by clear NCR processes and on-site verification.
Remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities. For procurement support that aligns factory inspection with your project procurement controls and logistics, contact /inquiry or info@carportiva.com.
Further reading and tools
- Review the Carportiva system range and all systems for product-level technical data.
- See our sourcing guides for templates and checklists you can adapt.
Selected references
- Guidance on galvanizing practice: American Galvanizers Association [1].
- Quality management system references (ISO): International Organization for Standardization [2].
- Delivery responsibilities and trade terms: International Chamber of Commerce Incoterms [3].
- Import documentation and guidance: U.S. Customs and Border Protection trade guidance [4].
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion