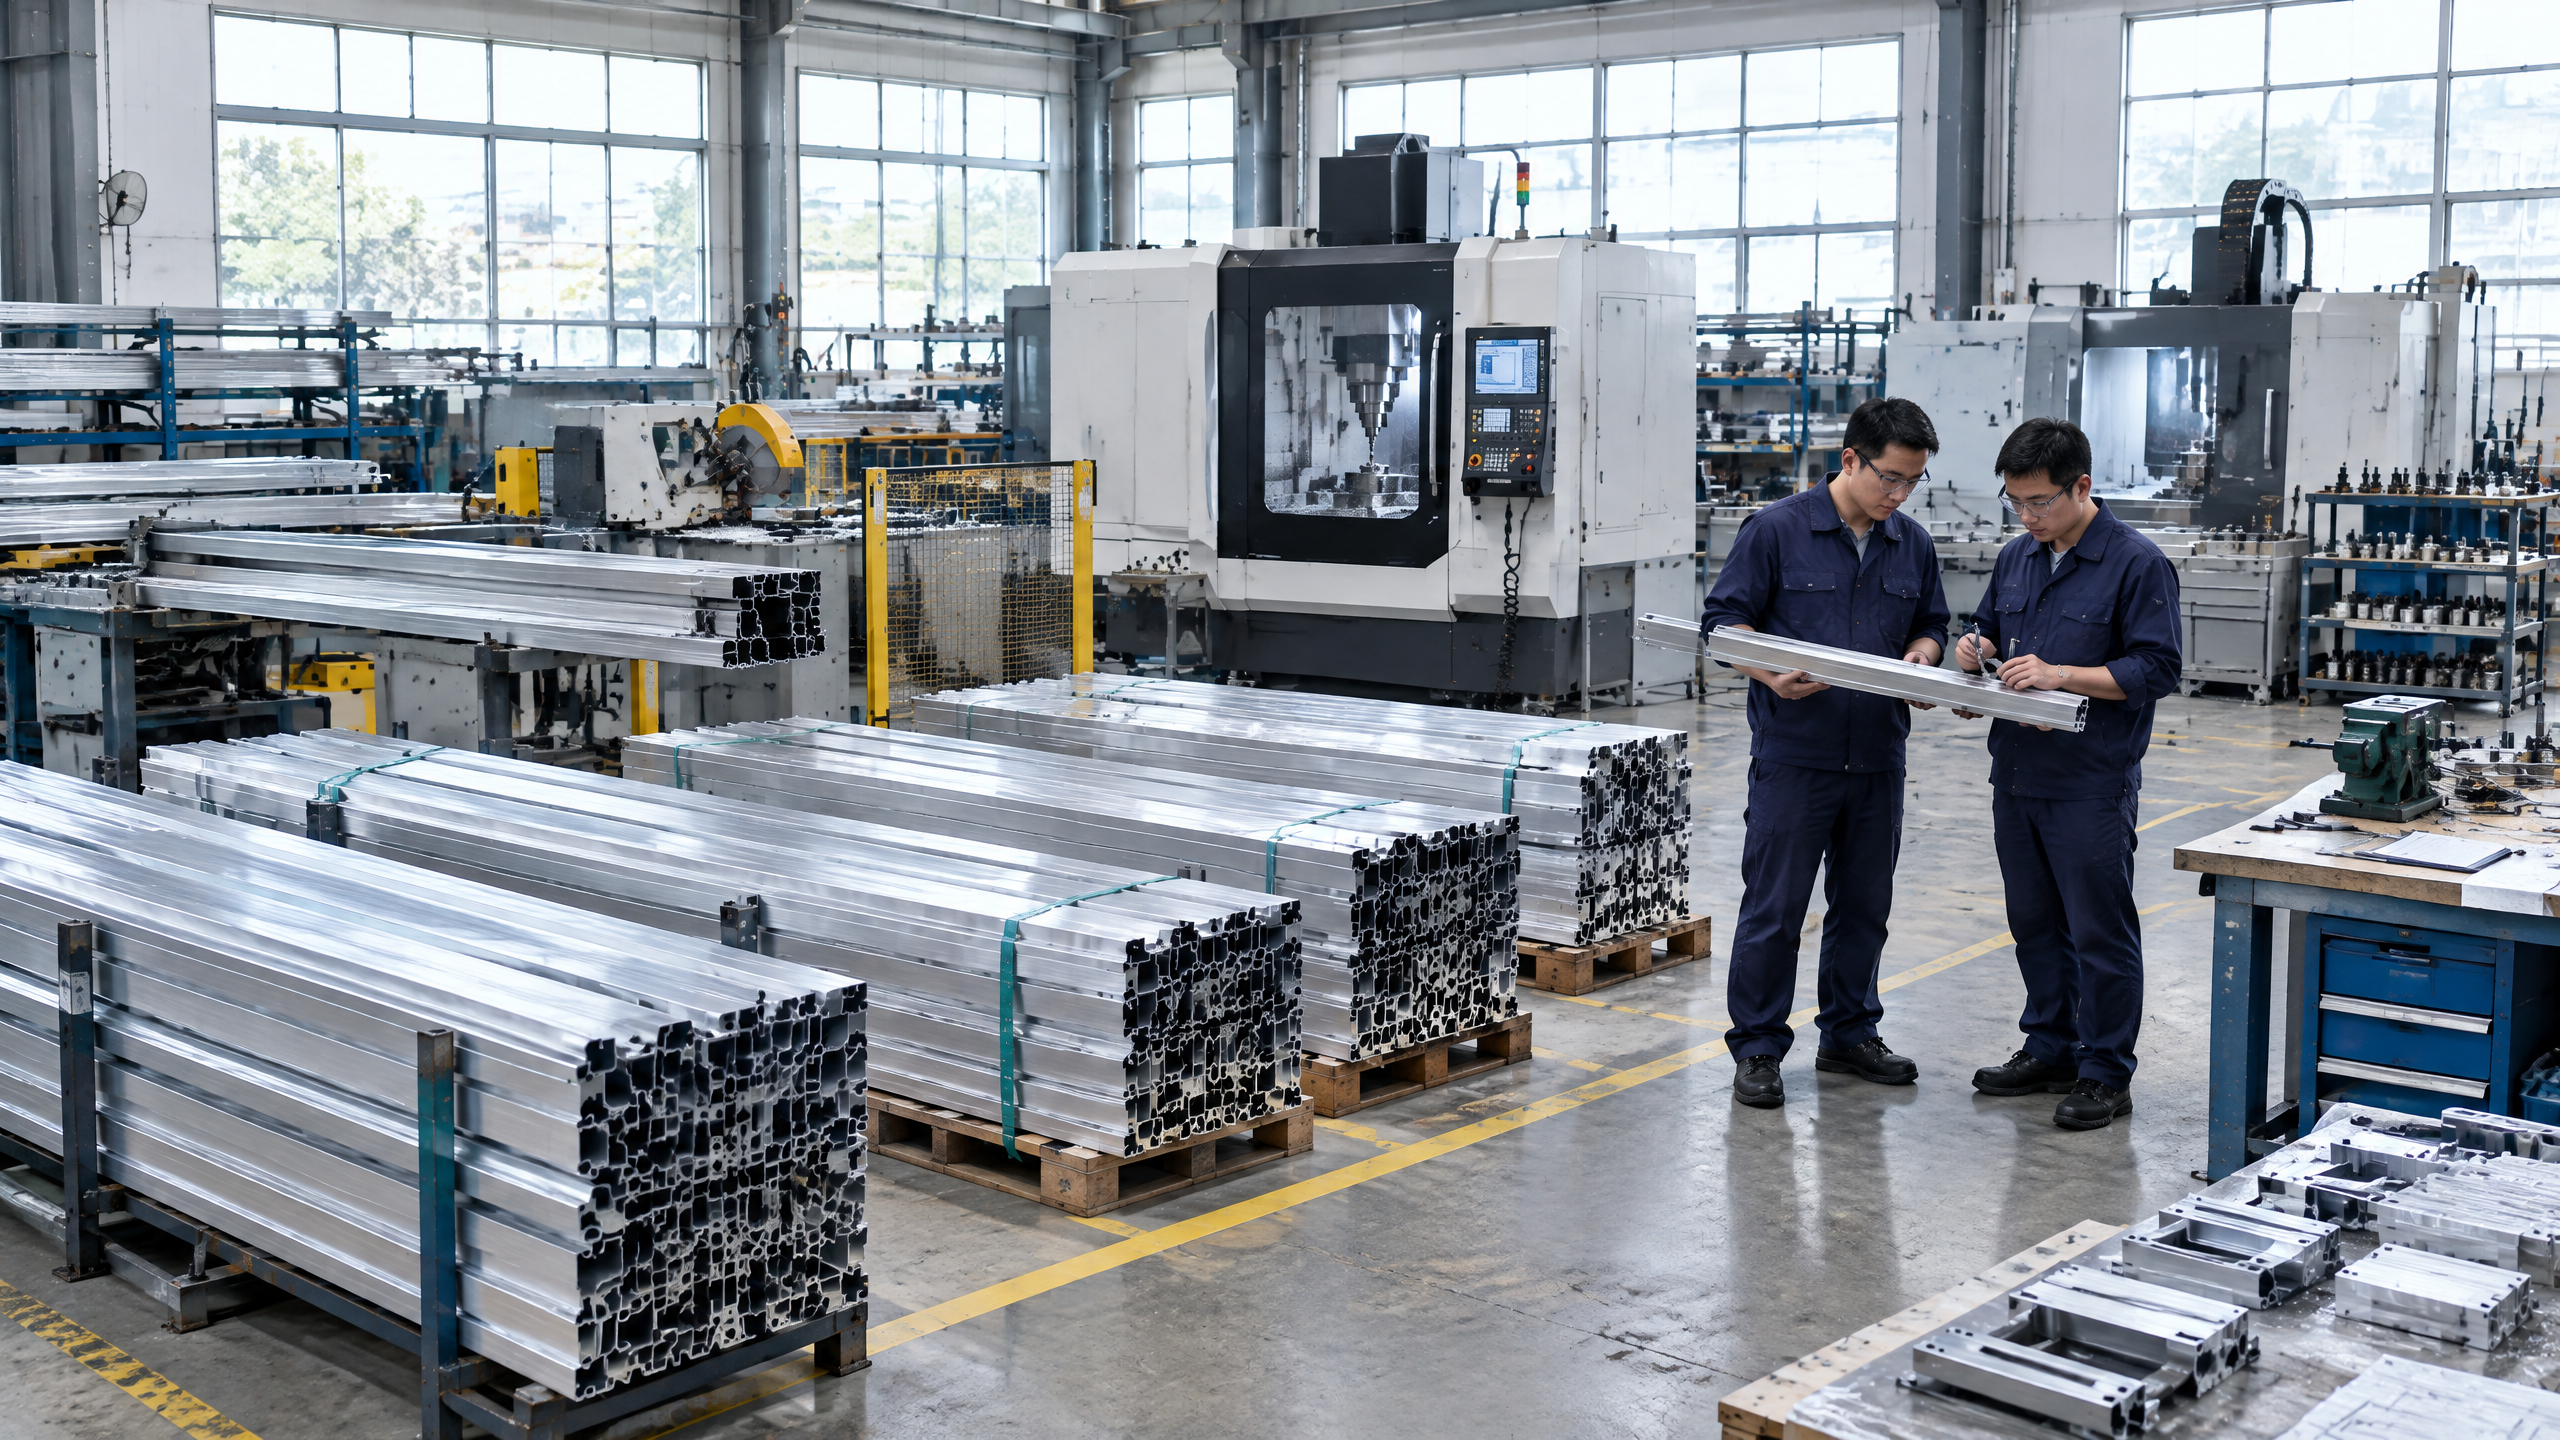
Direct answer (120–180 words) A carport OEM manufacturer matters when the project’s technical complexity, scale, regulatory remit or single-source responsibility makes the manufacturer’s engineering capability, quality systems and contractual obligations determinative for project success. Use an OEM-focused selection whenever the structural design, bespoke interfaces (solar mounting, EV charging, integrated drainage), aggressive lead times, warranty clarity or international shipping requirements create risks that only the originator can control or certify. Conversely, for simple, low-volume standard shelters a distributor or local fabricator can supply acceptable value. The decision should be evidence-led: compare technical scope, factory quality documentation, delivery responsibility matrix and B2B supplier due diligence against your project procurement controls and risk tolerance. Note: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and assessment by relevant local qualified professionals, installers, utilities and authorities before contracting.
Buyer context and scope boundary
Why define the boundary early Defining what you expect from a carport OEM manufacturer—and what you expect from the buyer, EPC or installer—reduces ambiguity, change orders and delivery disagreements. In B2B procurement the “scope boundary” separates manufacturer outputs (engineered components, quality certification, packaging) from buyer/accountabilities (foundations, site electrics, permits, local testing). Carportiva supplies architectural aluminium carports, commercial solar carports and industrial/fleet shelters; these product families illustrate a recurring boundary debate: is the supplier simply a parts manufacturer or a systems OEM who accepts integrated performance responsibility?
Typical scope partitions
- Manufacturer (OEM) scope: engineered frame and connections, surface treatments, fixed hardware, module mounting interfaces, factory assembly instructions, factory quality documentation, export packing coordination.
- Buyer/EPC/installer scope: site survey, foundations, crane and lifting, local approvals, electrical balance-of-system, final commissioning, warranty registration where local conditions affect coverage.
Who this guide is written for This guide targets global B2B buyers—distributors, architects, contractors, developers, solar EPCs and fleet operators—who must decide whether and when to prioritise the carport OEM manufacturer in procurement. Use the guidance to shape sourcing, contract risk allocation, technical review and factory-sourced evidence.
Core decision principle: when the OEM is the critical variable
Make the manufacturer the primary procurement variable when any of the following apply:
- Structural complexity. Projects with high wind/snow loads, long spans, cantilevers or unusual ground conditions require OEM structural engineering and stamped calculations.
- System integration. Solar PV, EV charging, lighting, or integrated drainage systems that rely on precise mounting interfaces mean the OEM’s mounting tolerances, fastener schedules and grounding detail drive outcome.
- High-volume repeatability. Multi-site or fleet programmes demand consistent parts, serialised components and factory quality control.
- Performance warranties. If you require manufacturer-backed warranties for structural integrity, finish or system interface, the OEM’s documentation and contractual language matter.
- Cross-border logistics and export. When international shipping controls, special packing or customs requirements are present, factory coordination and export packing coordination matter.
- Regulatory or insurer conditionality. Where local approvals or insurance underwriters demand OEM-produced calculations, test reports or factory certificates.
When the OEM is less critical
- Single, simple, low-cost shelters with standard loads where local fabrication is efficient.
- Projects where the buyer accepts engineering responsibility and local stampings in lieu of OEM responsibility.
Decision principle summary Prioritise the carport oem manufacturer when the technical scope or commercial structure makes the manufacturer’s engineering output, factory evidence and logistic performance material to project risk. Otherwise, treat the OEM as one of several supply options and transfer more responsibility to the buyer or local contractor.
Planning inputs: what you must assemble before talking to OEMs
A documented project basis reduces ambiguity and anchors procurement. Before engaging an OEM supplier collect the following inputs and make them part of your procurement controls:
Mandatory project inputs
- Project brief and performance criteria: primary use (parking, PV, shades), expected lifetime, exposure class, intended warranties.
- Site data: topography, soil report (or geotech trigger if required), site coordinates, wind and snow loads or relevant climatic data.
- Local regulatory constraints: planning restrictions, façade/height limitations, heritage overlays if any.
- Utilities and grid interface: transformer capacity, point of connection, interface details for PV or EV.
- Interface drawings: elevations, bay layouts, hampered access zones and existing services.
- Schedule and milestone constraints: target delivery windows and site critical path.
- Commercial envelope: budget range, contract procurement controls, preferred Incoterms and payment milestones.
- Quality and safety expectations: QMS evidence required, factory inspection windows, hold points.
- Responsibilities matrix: who is responsible for foundations, electrical handover, commissioning and warranty acceptance.
Why documented inputs matter Incomplete or informal scopes cause scope creep, re-engineering and disputed responsibility. A documented project basis enables technical scope comparison between suppliers, clarity on delivery responsibility matrix and enforceable project procurement controls.
Important legal and professional note Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and assessment by relevant local qualified professionals, installers, utilities and authorities for any contractual or financial decision.
Technical specification and interfaces
Technical scope comparison: what you must compare When evaluating a carport oem manufacturer you need a structured technical scope comparison that aligns delivered components to project responsibilities. Key items to compare:
- Structural design basis: design codes referenced, load cases considered, design life and serviceability limits.
- Connection and tolerance details: bolt grades, connector geometry, torque requirements, tolerances for module mounting.
- Surface treatment and corrosion protection: aluminium alloy, anodising, powdercoat, or galvanizing if steel elements are present. If galvanizing is used, verify alignment with industry guidance on thickness and inspection [1].
- Module and PV mounting interface: rails, clamps, grounding points and PV module compatibility.
- Electrical handover points: string combiner positions, inverter mounts, DC cable penetrations and grounding continuity.
- Drainage and waterproofing interfaces: where applicable, roof interfaces and runoff provisions.
- Lifting and temporary works: lift points and protective assembly sequences.
- Access and maintenance features: access routes, recommended maintenance intervals and spare parts lists.
Decision table 1 — Technical scope comparison (sample)
| Technical element | OEM-manufacturer responsibility | Buyer/EPC or installer responsibility |
|---|---|---|
| Structural frame engineering | Design, calculations, stamped drawings (if offered) | Provide geotech, site loads; accept foundation responsibility |
| PV module mounting interface | Supply rails, clamps, grounding points | Provide modules; installer secures modules per manufacturer torque specs |
| Finish (powdercoat/anodise) | Specify process and provide certificates | Inspect on arrival; record damage on delivery |
| Electrical harnesses to combiner | Optional; depends on contract | Provide inverter, balance-of-system, final electrical connection |
Interface tolerance and acceptance criteria Specify measurable handover tolerances (e.g., squareness, hole positional tolerances, bolt torque range). Without these, disputes arise during install. The technical scope comparison becomes the basis for factory inspections and final acceptance.
Standards and management systems Request evidence of quality management systems (QMS) consistent with recognised frameworks (for example ISO management systems where applicable) and ask to see the OEM’s factory quality documentation and inspection regimes for the relevant product family [2].
Procurement and factory evidence
B2B supplier due diligence: what to verify B2B supplier due diligence is a discrete procurement activity. Verify these elements in writing:
- Company legal identity and trading history.
- Financial stability and credit references relevant to order size.
- Manufacturing capacity and lead-time confirmation for ordered volumes.
- Product liability insurance and scope of coverage.
- Factory quality documentation: inspection plans, traceability of critical components, non-conformance handling and calibration records.
- Third-party inspection options and rights to witness factory acceptance tests (FAT).
- Export packing coordination and customs readiness for cross-border shipments.
- Delivery responsibility matrix including Incoterms, who organises freight, insurance and customs clearance.
Factory quality documentation: minimum evidence set Ask for the following factory-provided evidence before contract award:
- Material certificates (traceable to mill test reports where applicable).
- Welding procedure specifications (WPS) and welder qualification records if welding is relevant.
- Finished product inspection reports and dimensional checks.
- Coating and surface treatment certificates; sample panels may be required.
- Packing lists, palletisation plans and export packing coordination documents.
- Serialisation or part-number records that support spare parts procurement.
Decision table 2 — Factory evidence and buyer action
| Factory evidence | Why it matters | Minimum buyer action |
|---|---|---|
| Material certificates | Ensures base metal meets structural spec | Require MTRs; hold payment until received |
| Inspection test reports | Confirms dimensions and performance were checked | Schedule FAT or appoint third-party inspector |
| Packing coordination plan | Prevents shipping damage and customs mismatch | Approve export packing coordination; confirm Incoterms |
| Non-conformance report (NCR) history | Reveals factory’s handling of defects | Review NCR examples; require corrective action plans |
Logistics and Incoterms Agree Incoterms early in the procurement controls. The delivery responsibility matrix must define transfer of risk, cost and document responsibility. Use recognised Incoterms rules for clarity [3]. For cross-border shipments, confirm customs documentation and HS codes; align the packing list and commercial invoice to avoid customs delays and demurrage. Refer to applicable customs authorities for import requirements [4].
Factory acceptance and witness tests Where product performance or fit is critical, include factory acceptance tests with documented acceptance criteria. Rights to witness, hold points and remedial action obligations must be contractually embedded. Require factory quality documentation and define rework allowance and acceptance thresholds.
Mid-article CTA If you need OEM-level technical input or a supplier-specific factory evidence checklist for a project, contact our commercial team: /inquiry or info@carportiva.com. Explore Carportiva’s engineered options in the Carportiva system range and review all systems for product families and technical notes. See our sourcing guides for procurement templates.
Site installation and operations
Site readiness checklist A clear split between factory scope and site scope reduces delays. The buyer must confirm the following at least in advance of delivery:
- Foundations completed to design tolerance and curing schedule met.
- Access routes, laydown areas and crane lifting plans agreed and permitted.
- Temporary works and protection for adjacent buildings in place.
- Local approvals and permits secured for assembly and commissioning.
- Electrical interface points (service cabinets, inverter locations) prepared and labelled.
- Qualified installers engaged, trained and with verified competence records.
Installation interface: role clarity Agree specific handover points: when does the OEM’s responsibility end and the installer’s begin? Typical handover milestones:
- Arrival / off-load inspection: OEM bundles, packing and visible damage verified by buyer/inspector.
- Pre-assembly inspection: dimensional checks and component counts.
- Bolted assembly: torque and connection checks per OEM instruction.
- Final commissioning: electrical interconnection, earthing continuity tests and functional checks.
Operational maintenance and spares Require a minimum spare parts kit for critical connections and unique fasteners that might be exposed during the design life. Define maintenance intervals in the contract and require OEM guidance on permissible repair methods to avoid warranty invalidation.
Warranty administration Define the warranty triggers: acceptance certificate, commissioning sign-off, or time from delivery. Clarify whether foundation-coupled issues are excluded. The buyer must ensure warranties are coherent with local legal frameworks and understand that warranty on energy yield (PV) typically involves separate performance guarantees.
Professional note reiteration Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and review by relevant local qualified professionals, installers, utilities and authorities. Factory documentation does not replace local engineering validation.
Implementation risks and mitigations
Key risks that elevate the OEM decision
- Non-conforming components: parts arrive with dimensional variance that prevents onsite assembly. Mitigation: factory acceptance testing, measured tolerances in contract and hold points.
- Transit damage: poor packing or rough handling causing bent frames. Mitigation: export packing coordination and documented packing plans with photos.
- Customs and clearance delays: misdeclared HS codes or incomplete documents cause demurrage. Mitigation: accurate documentation, engage customs broker, follow CBP or local customs guidance [4].
- Quality management lapses: inconsistent production between batches. Mitigation: request QMS evidence, site visits, and witness sample production.
- Warranty disputes: unclear responsibility for foundation-affected damage. Mitigation: explicit delivery responsibility matrix and contractual clauses defining exclusions.
- Schedule slippage: factory capacity mismatch or supplier upstream delays. Mitigation: supplier capacity check, lead-time guaranteed milestones, liquidated delay terms where appropriate.
- Integration failures: PV modules or EV infrastructure incompatible with mounting geometry. Mitigation: technical scope comparison and tests against module datasheets.
Recommended contractual clauses
- Hold points and acceptance criteria: embed measurable checks and rights to reject non-conforming goods.
- Packing and documentation obligations: require packing plans and a warranty that packing is suitable for the mode of transport.
- Responsibility matrix and Incoterms: specify who handles freight, insurance and customs [3].
- Repair and remedial obligations: specify maximum time for remediation and responsibility for rework shipping costs.
- Traceability and serialisation: require traceability for key structural components.
Operational controls (project procurement controls) Implement project procurement controls to manage risk: defined approval authority, inspection triggers, document control, change order policy, and contingency allowances. The project procurement controls should be visible in the contract and enforced during procurement and delivery.
Six-step buyer workflow for OEM-led carport procurement
Named six-step buyer workflow — "Define, Qualify, Contract, Verify, Ship, Commission"
- Define — Establish the documented project basis
- Deliverables: scope document, geotech, load cases, budget envelope, schedule.
- Why: anchors technical scope comparison and sets acceptance criteria.
- Qualify — B2B supplier due diligence and shortlisting
- Deliverables: supplier questionnaire, financial review, capacity assessment, factory documentation request.
- Why: reduces supplier risk and confirms capability to meet quality and schedule.
- Contract — Technical and commercial terms
- Deliverables: contract with delivery responsibility matrix, Incoterms, warranty clauses, hold points, FAT rights, packing and insurance obligations.
- Why: transfers and allocates risk clearly; contractually protects buyer.
- Verify — Factory verification and acceptance planning
- Deliverables: FAT schedule, inspection checklists, dimensional tolerances, sample tests and witness rights.
- Why: prevents surprises and gives legal footing for rejection.
- Ship — Export packing coordination and logistical handover
- Deliverables: packing lists, shipping marks, customs documentation, nominated freight forwarder and insurance certificates.
- Why: ensures safe arrival and clear import clearance.
- Commission — Site acceptance and operations handover
- Deliverables: installation sign-off, commissioning reports, registered warranty, spare parts list and maintenance plan.
- Why: confirms final handover and triggers warranty.
Workflow responsibilities Assign a responsible party for each step (Buyer PM, OEM supplier, third-party inspector, EPC contractor). Embed communication protocols and escalation paths within your project procurement controls.
Frequently Asked Questions (FAQ)
Q: What is the difference between an OEM manufacturer and a system supplier? A: An OEM manufacturer produces engineered components and may provide certificates and part-level quality documentation. A system supplier combines components into an integrated solution, potentially taking responsibility for system performance, interfaces and warranty. Contractual language defines whether an OEM assumes systems responsibility.
Q: When should I insist on OEM-stamped structural calculations? A: Insist on OEM-stamped calculations when the manufacturer’s design governs structural performance, when local regulations require manufacturer documentation, or when insurers or authorities request original engineered documentation. If local engineers perform the final stamping, make sure responsibilities are explicit.
Q: How do I assess factory quality documentation? A: Verify material certificates, inspection test reports, non-conformance handling, calibration records and the factory’s QMS. Use third-party inspections and request evidence of regular batch records. Require factory quality documentation as a contractual deliverable.
Q: What is export packing coordination and why is it important? A: Export packing coordination defines how components are packed to survive sea, rail or road transport, including palletisation, moisture barriers, crates and separation of sensitive parts. Proper coordination reduces transit damage and customs issues.
Q: Who decides Incoterms and what do they affect? A: Incoterms are negotiated in the contract; they determine who pays for freight, insurance and clears customs, and where risk transfers from seller to buyer. Use them to define the delivery responsibility matrix and avoid ambiguity [3].
Q: Can I rely on a distributor’s warranty if the OEM offers one? A: Only if the distributor is authorised to assign or administer the OEM warranty. Verify warranty transferability and whether the OEM requires direct registration or commissioning evidence by approved installers.
Q: What factory tests are meaningful for carports? A: Dimensional checks, galvanizing/coating thickness tests (if applicable), bolt torque verification, assembly trials on critical connections and load checks on prototype assemblies are meaningful. Specify acceptance criteria in the contract.
Q: How should I handle spare parts for multi-site rollouts? A: Require a spares kit per standard module and serialise critical components. Negotiate lead-time guarantee for replenishment and ensure part numbers are fixed in the contract to avoid mismatch over production revisions.
Q: How do I manage energy yield expectations for solar carports? A: Energy yield is a site-specific outcome dependent on orientation, shading, module selection, inverter design and system losses. Energy yield guarantees, if required, should be provided by parties with the capacity to model and underwrite performance; otherwise rely on pre-contract modelling and local validation.
Q: What are acceptable factory witness arrangements? A: Either buyer-appointed inspectors, third-party inspection agencies or buyer representatives may witness FAT. Define the scope, criteria for passing, and how witness observations are recorded and acted upon.
Conclusion
Recap and practical takeaways The carport oem manufacturer matters where technical complexity, system integration, repeatability or international logistics make the manufacturer’s engineering, factory evidence and contractual responsibilities central to project success. Use a structured procurement approach—define a documented project basis, perform B2B supplier due diligence, complete a technical scope comparison, demand factory quality documentation, specify export packing coordination, and agree a delivery responsibility matrix within your project procurement controls. These steps convert manufacturer capabilities into predictable outcomes and reduce operational and contractual disputes.
Next actions
- Collate the documented project basis and scope checklist.
- Initiate supplier qualification and request the factory evidence checklist.
- Plan a factory acceptance test and agree export packing coordination in contract.
If you want tailored procurement support, factory evidence templates or to discuss system options, contact Carportiva: /inquiry or info@carportiva.com. Review the Carportiva system range, compare all systems and consult our sourcing guides for templates and checklists.
Final professional reminder Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and assessment by relevant local qualified professionals, installers, utilities and authorities before making procurement or contractual commitments.
Further reading and relevant standards
- Refer to galvanizing and corrosion guidance where coatings are specified [1].
- Consider QMS and management system expectations in alignment with ISO frameworks [2].
- Use recognised Incoterms for commercial terms clarity [3] and consult local customs guidance for import readiness [4].
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion