Direct answer (120–180 words)
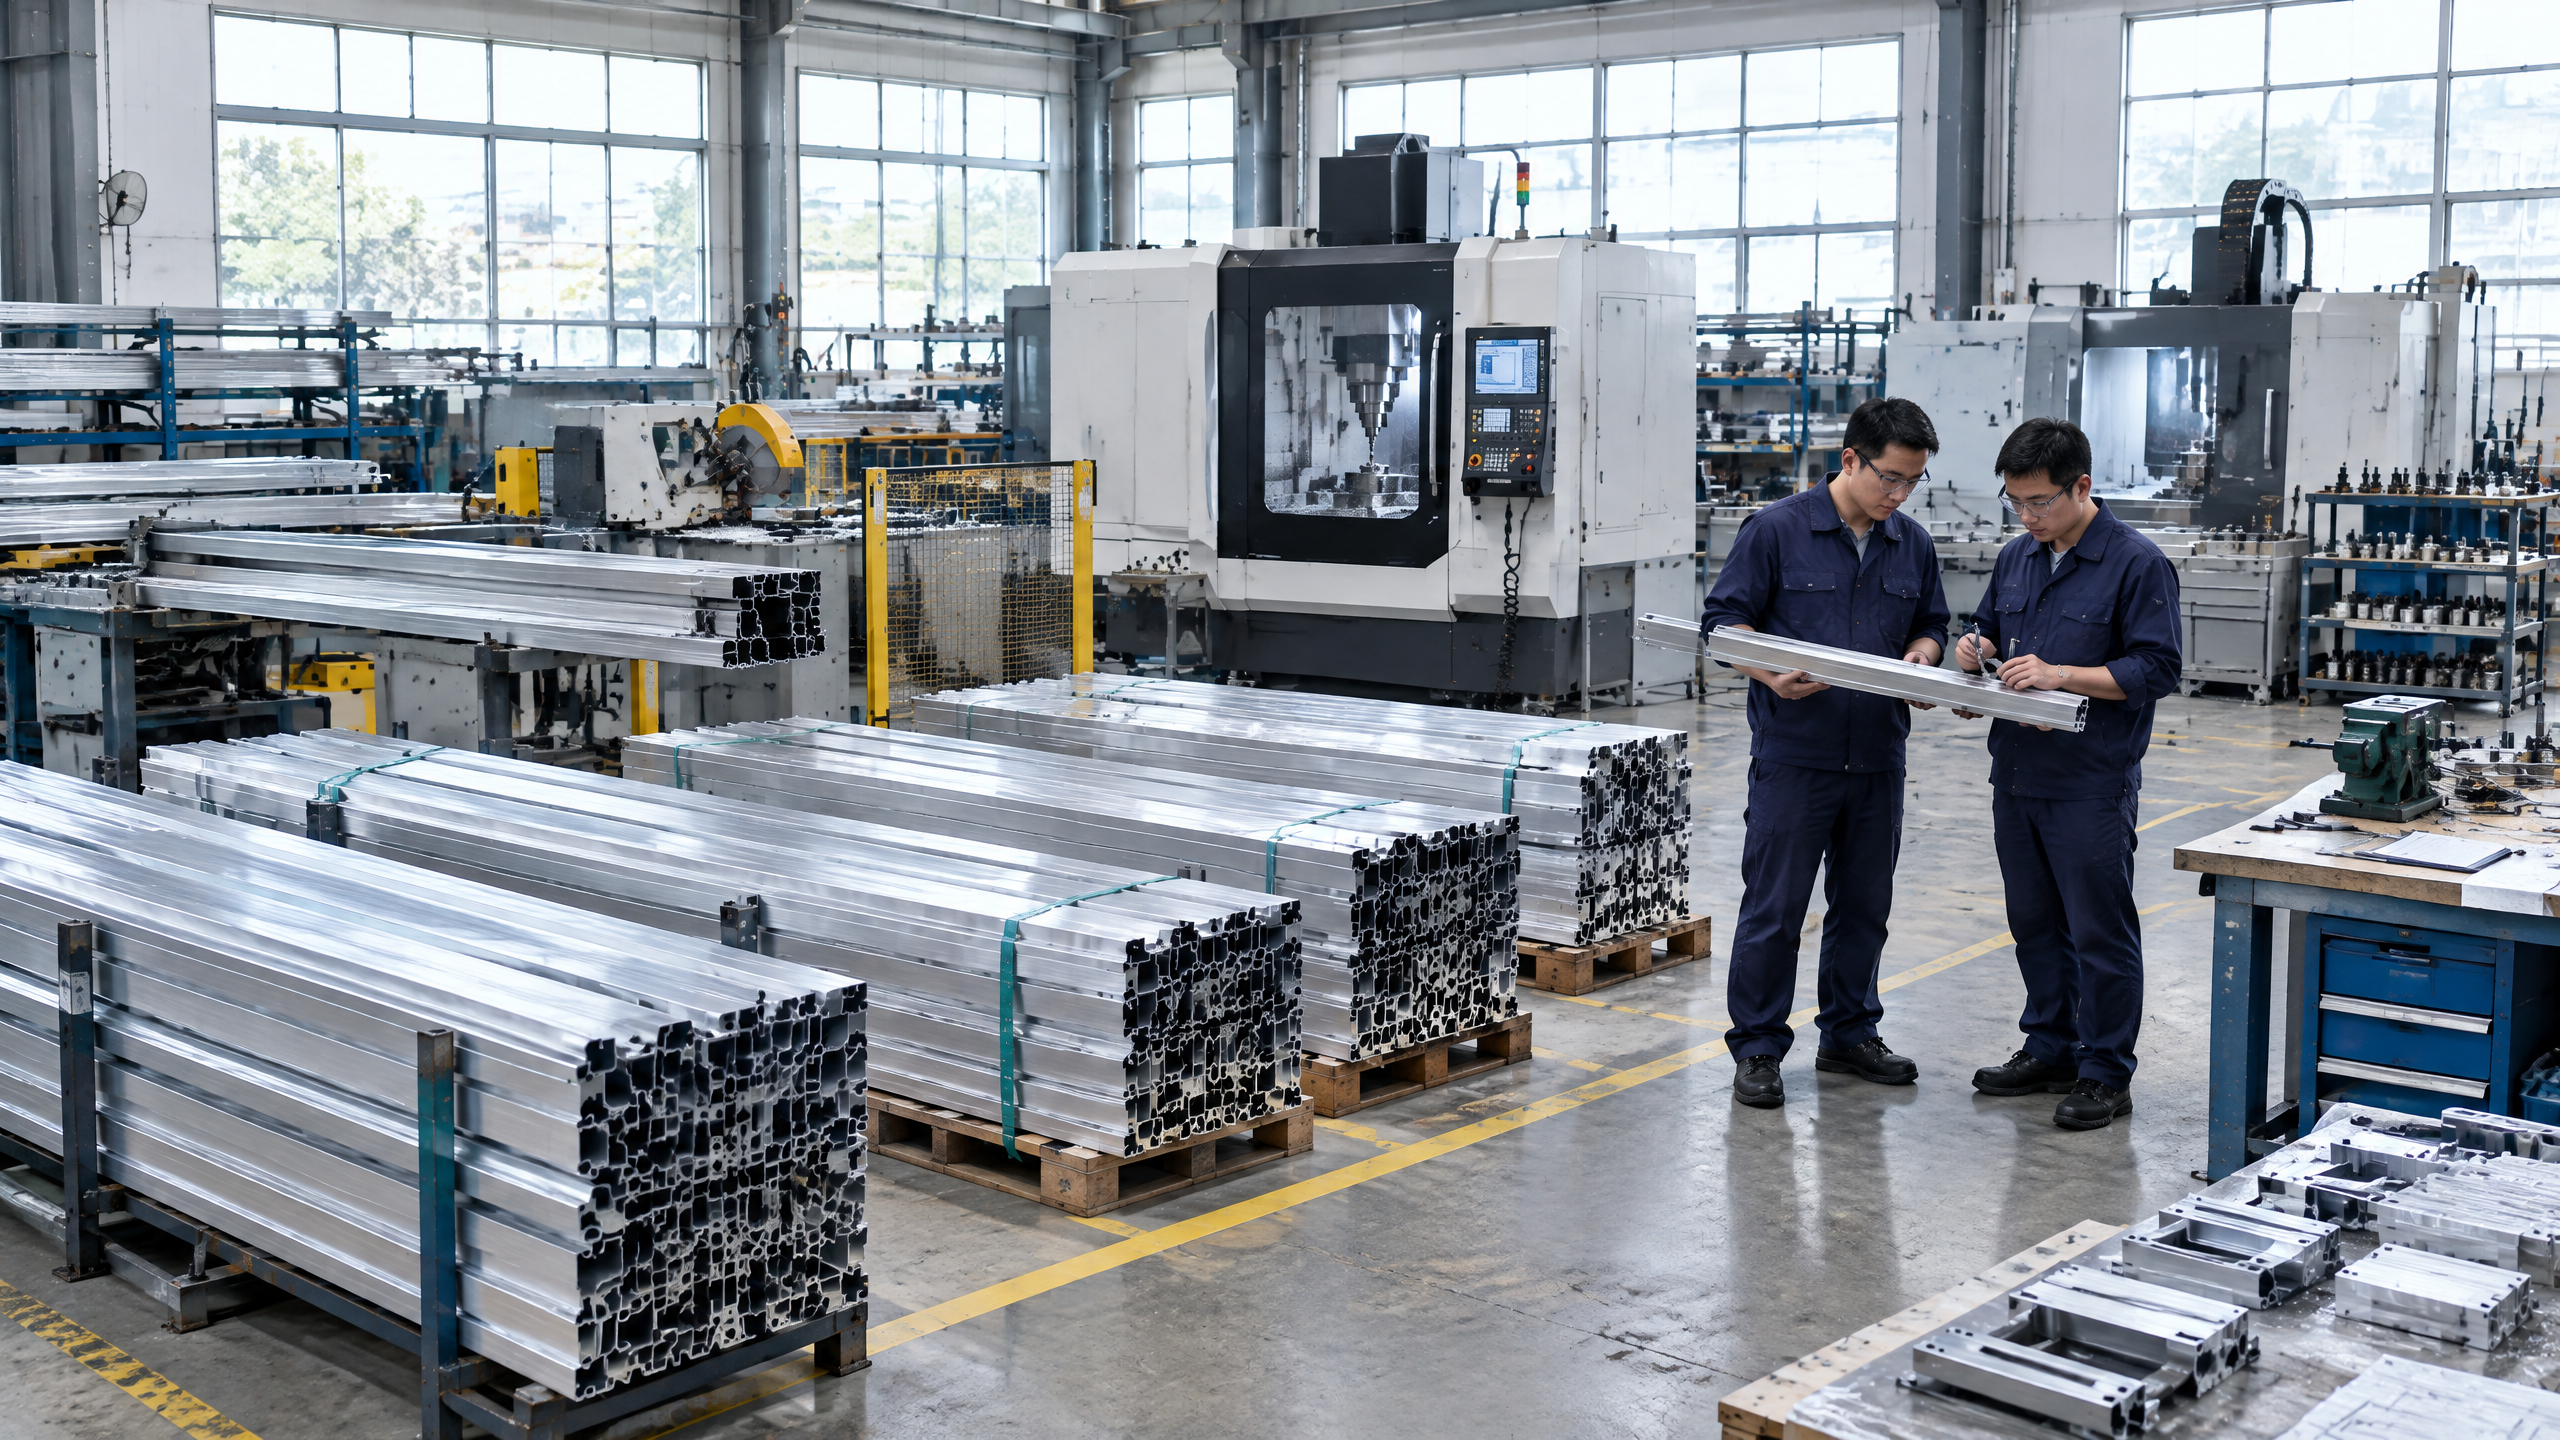
An evidence-led carport factory quality control approach focuses procurement on verifiable controls at source: documented specifications, repeatable production processes, material traceability, dimensional verification, protective coatings and packing methods that survive transport and installation. For B2B buyers (distributors, architects, contractors, developers, solar EPCs, fleet operators) the objective is to convert technical requirements into a clear technical scope comparison, require factory quality documentation and inspection gates, and map responsibilities with a delivery responsibility matrix tied to contract terms and Incoterms. Good practice mixes pre-shipment checks (FATs, dimensional reports, coating thickness readings), controlled export packing coordination and shipping documentation, plus defined site acceptance tests and spare-part provisioning. Project procurement controls must mandate a documented project basis and verified competence from local engineers, foundations contractors, utilities and authorities before system handover. This guide sets the procurement and implementation steps you should require to turn carport factory quality control into predictable outcomes.
Buyer context and scope boundary
Who should use this guide
- Distributors evaluating multiple suppliers for architectural aluminium carports and industrial shelters.
- Architects and consultants specifying system interfaces and finish quality.
- Contractors and developers responsible for foundations, local approvals and installations.
- Solar EPCs procuring commercial solar carports where PV yield connects to structural and electrical interfaces.
- Fleet operators procuring shelters at scale with predictable delivery and maintenance needs.
What this guide covers
- Factory quality control processes and the buyer evidence to request.
- How factory quality links to procurement, packing, shipping and site installation.
- Decision tools to compare supplier scope and delivery responsibility.
What this guide does not replace
- Site-specific structural capacity checks, foundation design, permit processes, electrical design and approvals, lead time confirmation, local price negotiation, energy yield modelling and warranty acceptance: all of these require a documented project basis and the involvement of relevant local qualified professionals, installers, utilities and authorities. Use local engineers and authorities to validate those items before ordering.
Scope boundaries for carport procurement
- Systems: architectural aluminium carports, commercial solar carports and industrial/fleet shelters (see Carportiva system range for typical system types).
- Factory responsibilities: manufacture, pre-assembly, coating and packing.
- Buyer/contractor responsibilities: foundations, local approvals, PV modules (if separate), electrical interconnection, testing on site and operation.
Key stakeholders and their responsibilities (high level)
- Buyer/Owner: defines performance, pays, accepts on site.
- Specifying Engineer/Architect: sets technical scope and interfaces.
- Procuring Contractor/EPC: manages procurement, interfaces, permits.
- Factory/Supplier: delivers compliant goods per agreed scope.
- Local Installer: installs to local codes, integrates with foundations/electrical.
Core decision principle: control at the point of manufacture
Primary procurement principle Prioritise verifiable controls undertaken at the factory and documented evidence that those controls were performed. Quality at-site is rarely improved after shipment; latent defects (wrong dimensions, incorrect coatings, missing connections) are expensive to correct and disrupt schedules. The core principle is therefore: make factory actions auditable, contractual and measured.
Why that principle matters
- Repeatability: factories with controlled processes can repeat acceptable results across multiple units.
- Traceability: material and process traceability enables defect root-cause analysis and warranty enforcement.
- Transfer of risk: clear delivery responsibility matrix and Incoterm selection reduces ambiguity in transit damage or customs issues [3].
- Cost predictability: documented technical scope comparison and project procurement controls reduce scope creep and change orders.
Standards and frameworks that support control
- Quality management systems and process standards provide a framework for measurable controls (see ISO guidance on quality management systems) [2].
- Industry guidance on protective coatings and corrosion protection helps specify durable finishes (see galvanizing guidance) [1].
In practice, the decision principle means: require defined acceptance gates (e.g., material certificates on receipt, pre-paint inspection, dimensional checks, FATs), and tie payment/milestones to evidence.
Planning inputs: what you must define before supplier evaluation
Essential project inputs every buyer must provide before evaluating factory quality control
- Documented project basis: project drawings, bill of quantities, load cases, relevant codes and a schedule.
- Technical performance requirements: structural loads, wind/snow zones, concealment and aesthetic tolerances, PV array orientation and allowances for module clamps.
- Material and finish expectations: galvanizing, aluminium alloys, powder-coating system, fastener grades.
- Foundation and anchor design assumptions: soil class, anchor embedment and setting tolerances.
- Interface definitions: where carport connects to building, electrical meters, combiner boxes, cable trays.
- Logistics constraints: site access, unloading equipment, storage allowances, customs routes and expected delivery windows.
- Commercial boundaries: agreed Incoterm, insurance, inspection rights, payment milestones.
- Acceptance criteria and remedial obligations: what constitutes acceptance at site and the process for non-conformance.
Why a documented project basis is non-negotiable
- It transforms subjective expectations into objective acceptance criteria.
- It enables suppliers to prepare accurate technical scope comparison spreadsheets and price properly.
- It is the basis for warranty and performance claims, and for local engineers to confirm foundations and approvals.
Planning checklist for procurement kickoff
- Prepare a single-point project brief document and share with shortlisted suppliers.
- Request a preliminary technical scope comparison from suppliers based on that project basis.
- Set inspection and acceptance gates (e.g., materials release, paint checks, pre-shipment inspection, site acceptance).
Technical specification and interfaces
Create both a high-level specification and a line-by-line scope to avoid gaps. Use the technical scope comparison to pit suppliers side-by-side.
Technical scope comparison table
| Specification area | Buyer requirement (example) | What to verify in supplier response |
|---|---|---|
| Primary structure | Aluminium grade, section profile, load rating | Alloy designation, section drawings, structural calculations (by whom) |
| Connection details | Bolted/welded connections, fastener grades | Drawings, torque specs, coating of fasteners |
| Foundations interface | Anchor type, embedment depth, grout | Anchor shop drawings, anchor templates, anchor material certs |
| Coatings & corrosion protection | Hot-dip galvanizing / powder coat spec | Coating standard, test methods, mill certificates |
| PV mounting & cable trays | Module clamp detail, earthing, uplift | PV mounting drawings, clamp types, earthing path |
| Drainage & gutters | Flow rates, outlets | Shop drawings, flow sections |
| Accessories & finishes | Lighting, signage, gutters | BOM, finish schedule |
| Pre-assembly | Modules assembled to frame vs bolt-on | Extent of pre-assembly, shipping dimensions |
| Testing & documentation | FAT, dimensional reports, coatings tests | Named tests, frequency, documented reports |
| Packing & shipping | Crate design, dunnage, markings | Export packing coordination plan, photos, packing list |
Key technical interfaces to define
- Foundation bearings and tolerance bands: provide anchor templates and coordinate with local installers.
- PV and electrical interfaces: specify combiner/DB locations, cable bend radii, conduit entries and earthing scheme.
- Architectural interfaces: canopy height, soffit finishes, lighting locations and pathways.
- Lifting/handling: lifting points, maximum unit weights and service clearances.
Detail on drawing and review cycles
- Require supplier shop drawings with dimensional tolerances and anchor templates early enough for foundation design (commonly before foundation cast).
- Define review cycles: preliminary review (for coordination), detailed review (for construction), and final shop drawings (for manufacture).
On structural calculations and verification
- Require the supplier to specify whether structural design is included or if the buyer’s engineer is responsible. Where suppliers provide calculations, request the basis, assumptions and the author’s qualifications. Cross-check locally.
Technical tolerances and how to control them
- Define allowable dimensional stack-ups and maximum permissible misalignments.
- Require factory dimensional control records, especially for long-span assemblies and module rails where PV alignment affects yield.
Procurement and factory evidence: what to require and why
What to request as minimum documentary evidence
- Material certificates and mill test reports for primary structural materials.
- Supplier process descriptions for welding, surface preparation, coating.
- Factory quality documentation including inspection plans, IPQC records and non-conformance procedures.
- Dimensional control records: measurement reports, jigs/fixtures used, and serialised component IDs if applicable.
- Welding procedure specifications and welder qualification records where welding is critical.
- Coating test results: thickness readings, adhesion tests, salt spray reports if performed by the supplier.
- Pre-shipment photographs and packing lists.
- Bills of materials with supplier source for proprietary components.
- Traceability matrix correlating components to test records and serial numbers.
Use of factory quality documentation “Factory quality documentation” is the buyer’s primary evidence that controls were applied. Require a consolidated package with:
- Inspection & Test Plan (ITP) showing hold points.
- Record of each hold-point’s completion with operator signature, date, and any remedial actions.
- Non-conformance report register and closure evidence.
Due diligence on the supplier
- Conduct B2B supplier due diligence: company registration checks, financial stability review, production capacity review, workforce skills, and prior client references (ask for contactable references).
- Verify factory capability with photos of tooling, jigs, painting booths, galvanizing arrangements or subcontractor relationships.
- If third-party inspections are required, define the scope and authority of the inspector.
Factory acceptance testing (FAT) and pre-shipment inspection
- Define what constitutes FAT for structural and PV mounting systems. FATs may include assembly checks, bolt torque checks, and functionality tests (e.g., integrated lighting).
- Clarify whether FATs are witnessed by buyer or authorised agent and whether a witnessed acceptance is required for shipment release.
Decision table: Documents and risk mitigation
| Document / Evidence | Purpose | Risk mitigated |
|---|---|---|
| Material mill certificates | Verifies alloy/steel grade and mechanical properties | Wrong material grade, early corrosion/failure |
| Factory quality documentation (ITP, IPQC) | Shows process controls and hold points | Uncontrolled production, missed inspections |
| Dimensional inspection reports | Verifies geometry and fit | Foundation mismatch, assembly rework |
| Coating test reports | Verifies protective finish properties | Premature corrosion, appearance defects |
| Pre-shipment photos & packing lists | Confirms packaging and content before shipment | Missing parts, inadequate packing leading to damage |
Caveats about third-party attestations
- Third-party inspections provide confidence but are not a substitute for contractual requirements and traceable factory records.
- Define the inspector’s scope, access and reporting format in contract language.
Relevant standards and guidance
- Refer to general principles of quality management and inspection traceability such as those in ISO guidance for process controls [2].
- For corrosion protection, consider galvanizing guidance to inform coating specifications [1].
Export packing coordination and delivery responsibility matrix
Export packing coordination
- Export packing is a functional quality control activity: properly packed components reduce on-site damage and erection delays. A packing plan must consider sea/road transport, transhipment, crane-lift procedures and storage at site.
- Require a written export packing coordination plan from the supplier showing crate design, dunnage, component separation, moisture protection, lifting points, and strapping.
- Photos of packed crates and a packing list should accompany the shipping documents.
Packaging considerations for carport systems
- Long items (e.g., rails) require cradles and keyed packing to prevent bending.
- Pre-assembled frames might need stiffening during transport to preserve alignment.
- Corrosion-sensitive items require moisture barriers or desiccants within crates.
Delivery responsibility matrix Use a delivery responsibility matrix to map who is responsible for each activity from factory to site. Tie this matrix to Incoterm selection [3].
Decision table: Delivery responsibility matrix (example)
| Activity | Supplier responsibility (example Incoterm: CIP) | Buyer responsibility |
|---|---|---|
| Manufacture & inspection | Supplier | — |
| Pre-shipment FAT & documentation | Supplier | Right to witness |
| Export packing coordination | Supplier | Provide packing requirements & photos |
| Export customs clearance | Supplier (under CIP if agreed) | Buyer provides export licenses if required |
| Main carriage / freight | Supplier | Buyer verifies insurance and route |
| Import customs clearance | Buyer | Buyer obtains import permits and pays duties |
| On-site delivery and unloading | Buyer / local contractor | Buyer arranges local crane & labor |
| Site acceptance testing | Buyer & installer | Supplier to provide support if contracted |
Notes:
- Select Incoterms deliberately. Incoterms define many delivery responsibilities and risk transfer points; use ICC guidance to interpret terms [3].
- Customs and import documentation must align with destination country requirements. Consult customs guidance and local brokers [4].
Shipping documentation that must be aligned
- Commercial invoice, packing list, bill of lading/air waybill, certificates of origin (if needed), export/import licences, and any testing certificates required by local authorities.
Customs and import considerations
- Confirm classification and documentation requirements early. Use customs authority guidance for import procedures and duties [4].
- Plan for possible customs holds and ensure spare parts and critical fasteners are included in clear-labelled kits to prevent assembly stoppages if parts are detained.
Site installation and operations
Coordination between factory output and site readiness
- Provide factory shop drawings and anchor templates early enough for foundation execution. Early alignment prevents off-site manufacturing that results in incompatible anchors.
- Confirm site lifting and handling equipment and provide supplier with the maximum packaged dimensions and weights. This minimises local unloading problems.
Installation documentation the buyer must require
- Full shop drawings and anchor templates.
- Assembly sequence drawings and torque specifications for joints.
- Tools, consumables and special equipment list.
- Spares list and recommended stock levels.
- Operation & Maintenance manual with maintenance intervals, coating repair procedures and contactable support.
Site acceptance testing (SAT) vs Factory acceptance testing (FAT)
- FAT confirms that the manufactured parts meet documented factory acceptance criteria; SAT validates the installed system in its working context.
- Define SAT scope: alignment checks, bolt torque verification, earthing continuity, water drainage performance, lighting function, and PV commissioning if applicable.
- Specify remedial response times if SAT reveals defects.
Ownership of on-site tasks
- Local installers typically have responsibility for anchor setting accuracy and final assembly. Ensure installers are pre-qualified and that their scope is clearly written into contracts.
- Warranty activation often requires completed SAT and signed handover documents.
Training and maintenance handover
- Insist on installation training for the buyer’s maintenance teams or the installing contractor, with a short written log of attendees and topics.
- Ensure spare-part kits and consumables are included or available.
Safety and compliance
- Ensure local health and safety requirements for lifting, working at height and electrical works are followed. Local authorities and installers must be engaged to confirm compliance.
Reiteration (mandatory) Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Implementation risks and practical mitigations
Common implementation risks and practical buyer controls
- Scope gap between supply and expectation
- Risk: Missing items (e.g., anchor kits, earthing parts).
- Mitigation: Use technical scope comparison and detailed BOMs; require packing lists.
- Dimensional mismatch with foundations
- Risk: Anchor misalignment prevents fit-up.
- Mitigation: Lock down anchors from supplier shop drawings; perform measurement verification before cast; allow templates.
- Coating damage in transit
- Risk: Scratched powder coat or exposed galvanizing causing early corrosion.
- Mitigation: Require export packing coordination, pre-shipment photo evidence, and defined remedial painting procedures.
- Inadequate material traceability
- Risk: Unknown alloy or fastener grade leading to failures.
- Mitigation: Require mill certificates and correlate to BOM.
- Customs holds and documentation errors
- Risk: Delays and demurrage costs.
- Mitigation: Validate export documentation and use customs brokers; understand classification and permits [4].
- Late or misunderstood changes
- Risk: Design changes during production cause rework or delays.
- Mitigation: Freeze design on agreed date; use a change-order process with cost/time impacts.
- PV energy yield shortfalls due to mounting alignment
- Risk: Improper module tilt or shading due to inaccurate spacing.
- Mitigation: Include PV mounting in technical scope and require alignment tolerances and installation checklists.
- Warranty claim friction
- Risk: Dispute over root cause of defect (factory vs site).
- Mitigation: Define warranty coverage and claim process contractually; keep traceability records.
Project procurement controls to include in procurement documents
- Maintain a single source of truth for contracted technical requirements.
- Use staged payments tied to deliverables and documentary evidence (shop drawings, FAT reports, shipping docs).
- Require a contingency and spare part policy for long lead items.
- Hold a pre-shipment acceptance gate where buyer or authorised inspector must sign off.
Risk matrix (summary)
| Risk | Likelihood (practical) | Impact | Key control |
|---|---|---|---|
| Anchor template mismatch | Medium | High | Early shop drawings & verification |
| Packing-induced damage | Medium | Medium | Export packing coordination & photos |
| Material grade mismatch | Low–Medium | High | Mill certificates & traceability |
| Customs delay | Medium | Medium–High | Early customs review & broker engagement |
| Scope omission | Medium | High | Detailed technical scope comparison |
Six-step buyer workflow: Factory Quality Assurance for Carport Procurement
Name: Factory Quality Assurance for Carport Procurement (FQACP) — six-step workflow
Step 1 — Project definition and documented basis
- Produce a single project brief that includes drawings, loads, finishes, interface points and acceptance criteria.
- Distribute to shortlisted suppliers and use as the basis for quotations.
Step 2 — Technical scope comparison and supplier selection
- Request a technical scope comparison from vendors that maps your project items to supplier deliverables.
- Evaluate against acceptance gates: materials, coatings, FAT capability, packing, lead time, and references.
Step 3 — Contract & inspection plan
- Contractually require a factory quality documentation package: ITP, traceability matrix, rectification timelines.
- Agree on an Inspection & Test Plan (ITP) with defined hold points and definition of FAT and SAT responsibilities.
Step 4 — Shop drawings, anchor templates & foundation alignment
- Require final shop drawings and anchor templates for local foundation work.
- Approve these before foundations are cast or anchors fixed.
Step 5 — Production controls, FAT and pre-shipment checks
- Enforce the ITP during production. If buyer inspection is required, schedule FAT with clear pass/fail criteria.
- Require pre-shipment evidence: photos, dimensional reports, packing lists, and coating test reports.
Step 6 — Shipping, customs coordination & site acceptance
- Execute export packing coordination and confirm delivery responsibility matrix for shipment.
- On arrival, perform SAT, verify documents and close-out non-conformances before final payment and warranty start.
Templates and gates to prepare
- Standard ITP template with sign-off fields.
- Factory pre-shipment checklist.
- Packing and shipping checklist.
- SAT template and handover certificate.
Decision points and go/no-go gates
- Groundwork: shop drawing approval before casting.
- Production: completion of FAT & ITP hold points before shipping.
- Site: SAT sign-off before final payment and warranty activation.
FAQ
Q: What documents practically prove carport factory quality control? A: A consolidated package including ITP, material mill certificates, dimensional inspection reports, coating test results, welding procedure and qualification records, pre-shipment photos and a comprehensive packing list. These items form the backbone of factory quality documentation.
Q: Should I always witness FAT? A: Witnessing FAT is best practice for high-value or complex systems. If the buyer cannot attend, appoint an independent inspector with a clear mandate. Inspections should be defined contractually.
Q: How do Incoterms affect responsibility for damage in transit? A: Incoterms set the transfer of risk and costs; choose terms that align with your logistics capabilities and insurance arrangements. Refer to ICC Incoterms guidance for interpretation [3].
Q: How early do I need anchor templates? A: Anchor templates or shop drawings must be approved before foundations are placed. Late release of templates is a frequent cause of rework.
Q: Can the supplier supply foundations? A: Some suppliers offer foundation design as a service; where they do, require clear responsibilities and local sign-off by a qualified engineer. If the supplier does not provide foundations, the buyer must ensure local contractors receive accurate templates.
Q: What are reasonable acceptance gates to tie to payments? A: Typical gates: shop drawing approval (10–20%), completion of production/FAT & shipping release (50–70%), site acceptance and handover (remaining balance). Exact values must be negotiated contractually.
Q: How should I handle spare parts? A: Require a spare-parts list and supply terms. For long lead items, specify spares at contract stage and include their packing within main shipment where possible.
Q: Who validates energy yield for solar carports? A: Energy yield modelling is the responsibility of the party supplying the PV design (often the solar EPC). However, mounting alignment and shading from structures are installation-dependent — coordinate with structural and PV design teams.
Q: Are photos of packed crates sufficient proof? A: Photos are useful but should be accompanied by a documented packing list and, where necessary, an independent packing inspection for long or mission-critical shipments.
Q: What is a reasonable lead time for manufacturing? A: Lead time varies with scope, finishing and capacity. Obtain firm lead-time commitments in writing and build schedule contingency into the project plan.
Two decision tables to support procurement choices
Decision table 1 — When to require on-site buyer inspection vs third-party inspection
| Project characteristic | Recommend buyer witness? | Recommend third-party inspector? |
|---|---|---|
| Critical structural interfaces, tight tolerances | Yes | Optional (buyer preferred) |
| High-value, complex PV mounting systems | Yes if possible | Yes (as backup) |
| Repeated production of many identical units | No (sample witness) | Yes (periodic spot checks) |
| Low-value, high-volume simple parts | No | No (spot check suffices) |
| Export to regulated markets with strict import checks | Yes (if buyer compliance required) | Yes (recommended) |
Decision table 2 — Pre-shipment checklist (minimum)
| Item | Required evidence | Who provides |
|---|---|---|
| Material certificates | Mill/test reports | Supplier |
| Dimensional checks | Measurement report & drawings | Supplier |
| Coating verification | Thickness readings & photos | Supplier |
| Packing plan | Crate drawings, dunnage details | Supplier |
| Shipping documents | Packing list, invoice, B/L | Supplier |
| Customs pre-clearance paperwork | Certificates of origin, permits | Buyer / Supplier (as agreed) |
| Pre-shipment photos | Multiple angles of packed crates | Supplier |
| ITP completion | Signed hold-point records | Supplier |
Conclusion
Carport factory quality control is the single most effective lever a B2B buyer has to reduce downstream project risk in the sourcing, cost and factory delivery cluster. Translate technical requirements into a documented project basis, insist on factory quality documentation, use a technical scope comparison as the frame for bids, and codify responsibilities with a clear delivery responsibility matrix. Require pre-shipment evidence, plan export packing coordination and ensure local foundations and approvals are validated by qualified professionals prior to installation. Use contractual inspection gates and staged payments to align incentives.
If you want assistance converting a project brief into a procurement-ready scope, or to review factory quality documentation, contact our team: /inquiry or info@carportiva.com. For product context and example system types see Carportiva’s all systems and sourcing guides.
Final reminder: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
/inquiry — or — info@carportiva.com
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion