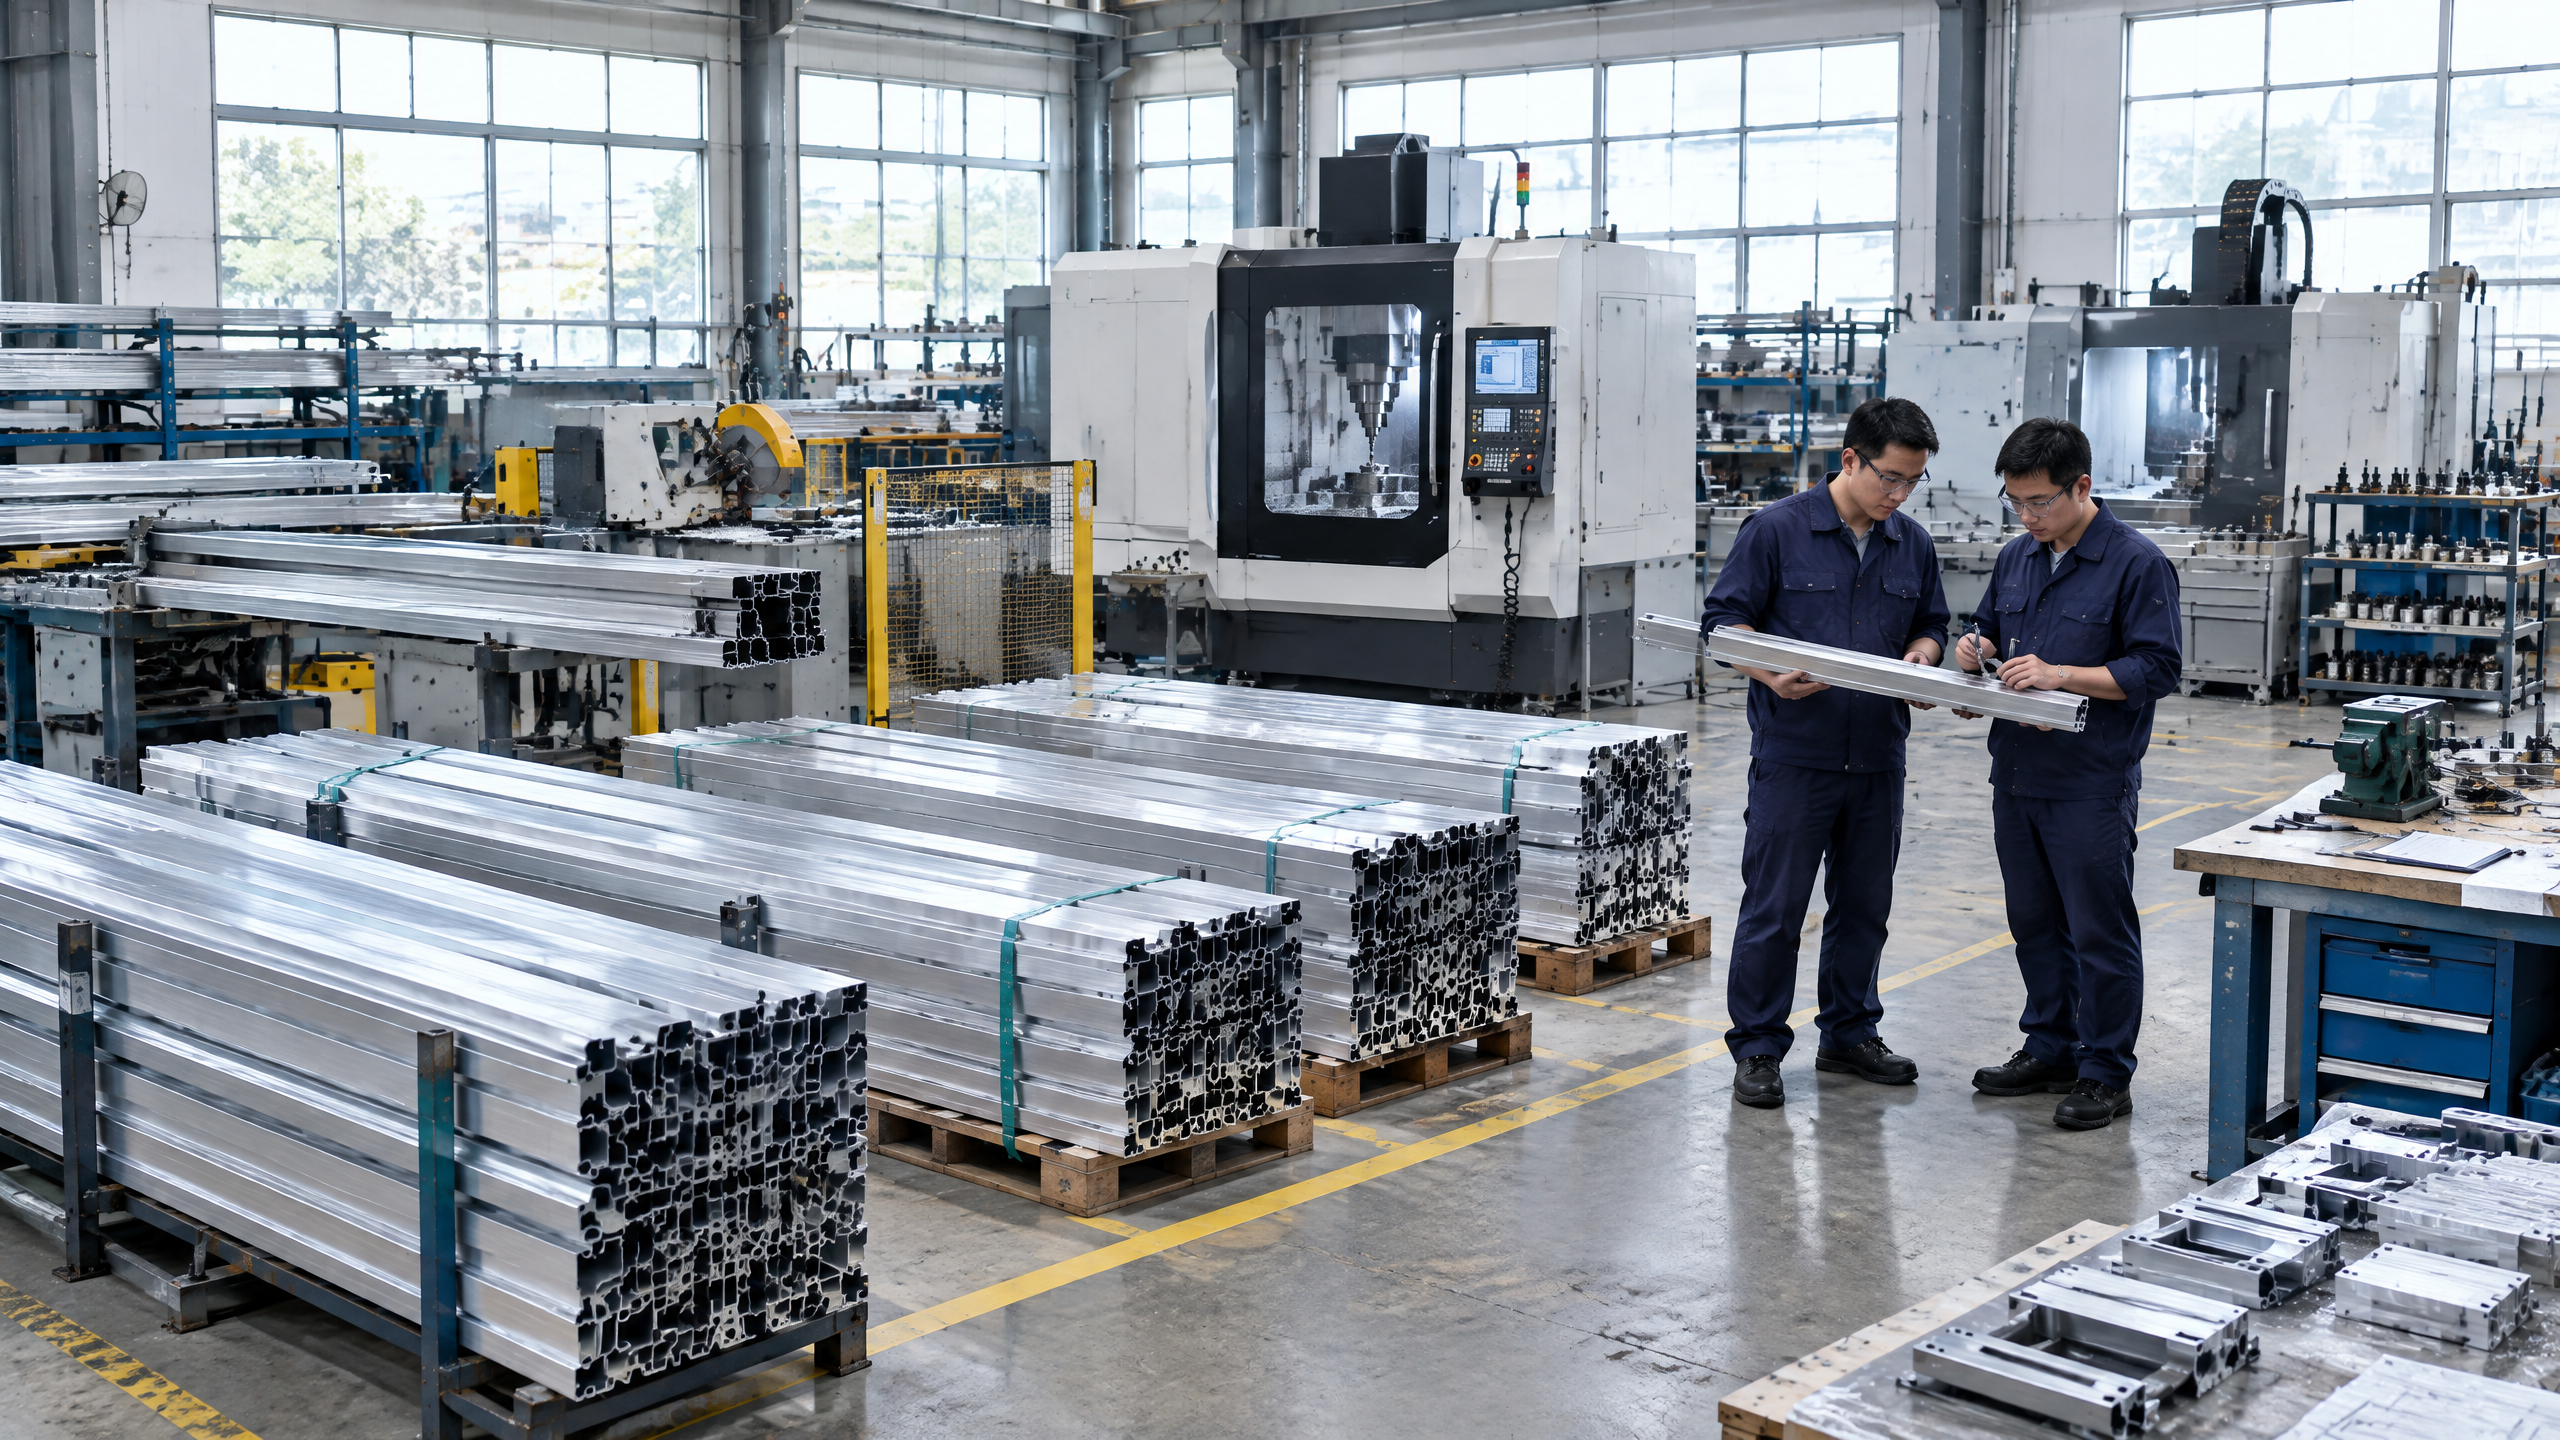
A carport factory audit checklist matters whenever a B2B buyer must convert a project specification into a reliable, deliverable supply package where cost, schedule and on-site performance are tied to factory output. Use the checklist to validate that the vendor’s organisation, processes, material controls, quality documentation and packing/transport arrangements match the buyer’s technical scope, logistics terms and project procurement controls. It is most valuable where bespoke structural interfaces, integrated PV (or other electrical systems), long lead items, cross-border shipments, multiple sub-suppliers or complex warranty and installation responsibilities create risk. A well-constructed audit connects supplier evidence to a delivery responsibility matrix, supports a technical scope comparison against tender documents, and focuses follow-up actions (test witness, factory QA hold points, export packing coordination). It does not replace local engineering for site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty — those require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Buyer context and scope boundary
Who should consider a carport factory audit checklist?
- Distributors and resellers looking to add branded carport systems to an inventory.
- Architects and contractors specifying carports that interface with buildings or civil works.
- Developers and fleet operators procuring based on total cost of ownership and uptime.
- Solar EPCs integrating PV modules, inverters and DC/AC infrastructure into a carport structure.
What the checklist is — and is not
- It is a structured instrument to gather evidence of factory capability, quality systems and manufacturing practice aligned to a defined technical scope.
- It is not a substitute for contract terms, site engineering, legal due diligence, or regulatory approvals.
- It complements B2B supplier due diligence and should be integrated with procurement-stage controls such as supplier scorecards, commercial terms and inspection plans.
Scope boundary: what the audit typically covers
- Facility level: organisation, workforce, test and inspection capability.
- Process level: fabrication, surface treatment, assembly, welding, bolting and pre-assembly.
- Material control: incoming raw material traceability and storage.
- Documentation: factory quality documentation, drawings, test records and traceability statements.
- Logistics readiness: export packing coordination, labelling, and transport staging.
- Compliance readiness: calibration, certificates of conformity, and applicable standards.
When to stop: areas left to project stakeholders
- Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Core decision principle: audit when production risk is not acceptably mitigated by documents alone
Decision principle in one sentence:
- Conduct a factory audit whenever documentary evidence, supplier history and contractual protections do not reduce the probability or consequence of a failure to a level acceptable for the project’s commercial and technical exposure.
Practical triggers
- First-time supplier or new manufacturing site for a known supplier.
- Significant design change, bespoke interfaces, or integrated electrical/solar scope.
- High-value orders, long lead times, or single-source critical components.
- Complex export or import routes that increase logistics or customs risk.
- Insufficient or non-standard factory quality documentation supplied during tender.
Risk vs. cost: a simple framing
- Low risk / low value orders: rely on documentation, sample inspections, or third-party certificates.
- Medium risk: add desktop due diligence, sample testing, or a focused audit.
- High risk / high value: full factory audit, witnessed tests, hold points, and strengthened contractual remedies.
Decision table — when a factory audit is typically recommended
| Risk factor | Low | Medium | High |
|---|---|---|---|
| Supplier is incumbent with mature history | No | Possibly | Yes (if scope changes) |
| Order value / project criticality | No | Possibly | Yes |
| Custom structural interfaces or PV integration | No | Yes | Yes |
| Cross-border export with complex logistics | No | Yes | Yes |
| Factory quality documentation incomplete | No | Yes | Yes |
Use the table as a guide, not a rule. Adapt the weighting to your organisation’s risk appetite.
Planning inputs: what you need before you audit
A measured audit starts with a set of planning inputs that align procurement, technical and logistics teams.
Mandatory inputs
- Contract/commercial terms (Incoterm) and delivery responsibility matrix. Which party is responsible for packing, export, insurance and import clearance? Clarify per [Incoterms rules] where appropriate [3].
- Technical specification and drawings: a definitive baseline for technical scope comparison between tender documents and factory output.
- Project schedule: procurement milestone dates, manufacturing window, and site availability.
- Quality requirements: acceptance criteria, test witness points, non-conformance procedures, and required certificates.
- Regulatory and local approvals list: what certificates or approvals must accompany shipments for customs and on-site acceptance.
- Packaging and logistics plan: export packing coordination is particularly important for long ocean voyages or multi-modal transport.
- Contact matrix: who in supply, quality, engineering, logistics and commercial will act on audit findings.
Optional but high-value inputs
- Historical supplier performance data and supplier financial health indicators.
- Sample component or full-scale prototype for comparison.
- Independent or internal inspection agency scope and escalation path.
Planning outputs
- A tailored carport factory audit checklist that maps to the technical scope comparison, delivery responsibility matrix, and procurement acceptance criteria.
- A pre-audit document request and a factory visit plan that identifies hold points and witness tests.
Technical specification and interfaces: what the audit must confirm
The audit must translate drawings and specifications into factory-verifiable attributes. Key technical areas:
Structural and materials
- Material certificates and traceability for aluminium alloys and fasteners: review incoming goods records, mill certificates and trace links to each batch.
- Structural connections: verify welding procedure specifications (WPS) and qualified welders, mechanical connector torque control, bolt grades and anti-rotation measures.
- Surface treatment and corrosion protection: for steel components (if used) check galvanising, coatings and handling consistent with local exposure. Reference technical guidance from the American Galvanizers Association for hot-dip galvanizing best practice where relevant [1].
- Section sizes and tolerances: confirm dimensional control and fabrication tolerances in production jigs.
Electrical and PV interfaces (if applicable)
- Mounting interfaces for modules: confirm module clamping, grounding and module-to-structure electrical continuity.
- Cable management: confirm routing, conduit access, and strain-relief details that match the electrical design.
- Connection boxes and earthing: factory-installed or on-site provision? Confirm continuity with project electrical design.
Foundations and structural interaction
- Anchor and baseplate tolerances: confirm that baseplate locations, bolt hole sizes and anchor design match the project’s foundation drawings.
- Lateral load provisions: wind uplift and lateral restraint provisions must align with the engineered analysis — confirm that factory does not modify structural geometry without change control.
Manufacturing tolerances and assembly
- Pre-assembly strategy: confirm whether the supplier will pre-assemble modules, and if so, how they pack and protect joints and bolts.
- Quality control hold points: identify points where factory will stop production pending inspection (e.g., post-welding QC, post-surface-treatment, pre-packaging).
Testing and inspection
- Shop tests: dimensional checks, bolt torque records, welding visual inspection; identify tests that must be witnessed.
- Non-destructive testing (if required): verify availability and calibration of NDT equipment and certified operators.
- Electrical continuity and insulation testing for integrated PV: confirm acceptance procedure and test records.
Document control
- As-built drawing issuance process: how the factory handles revision control and final as-built documentation.
- Serialisation or tagging system that allows items to be traced to test reports and mill certificates.
Technical scope comparison
- Conduct a line-by-line technical scope comparison between the purchase specification and the factory records: list deviations, accept/reject criteria and corrective action timelines.
Procurement and factory evidence: what to collect and why
This section focuses on the documentary and observable evidence that should appear on a carport factory audit checklist. It also emphasises B2B supplier due diligence and contractual alignment.
Core documentary evidence (minimum baseline)
- Company and site credentials: business registration, site address verification and capacity statements.
- Quality management evidence: ISO 9001 registration or equivalent where applicable; audit the scope of the certificate to ensure manufacturing operations are included [2].
- Material certificates: mill/test certificates linked to batch numbers and part numbers.
- Welding documentation: WPS, welder qualifications and welding inspection reports.
- Calibration records: measurement tools and NDT equipment calibration certificates.
- Factory inspection records: internal QA checklists and final inspection records for recent orders.
- Packaging and export documents: packing lists, export packing coordination plan, labelling conventions and fit-for-purpose crating procedures.
- Traceability and serialisation: system for linking part IDs to certificates and inspection records.
- Non-conformance and corrective action records: examples of NCRs and how they were closed.
Physical evidence to observe
- Cleanliness and storage: are raw materials stored to prevent contamination or corrosion?
- Jigs and fixtures: condition, adjustment capability and serial numbers for key fabrication jigs.
- Workshop layout: material flow, segregation of operations, staging areas for finished goods and packing stations.
- Personnel competence: visible training records, signage on safe operating procedures and PPE usage.
- Packing methods: confirm cushioning, bracing and moisture protection for sea freight; look for exemplar crates.
Export packing coordination and customs considerations
- Confirm export packing coordination: packing materials, anchoring inside containers, desiccant use, and blocking/bracing instructed for ocean transit.
- Verify the supplier's packaging plan aligns with import country requirements and any customs/inspection access needs.
- Where export documents or packing lists will pass to customs, ensure they meet the importing authority’s guidance; the U.S. Customs and Border Protection guidance on import documents is a useful reference for complex imports [4].
Delivery responsibility matrix and contractual fit
- Match documentary evidence to the delivery responsibility matrix: who provides packing, who arranges export documentation, and who insures goods in transit? Use the delivery responsibility matrix to allocate actions and verify the supplier’s obligations are consistent with the chosen Incoterm [3].
- Table: evidence required by delivery responsibility matrix
| Contract term / Incoterm (example) | Supplier responsibilities (evidence expected) | Buyer responsibilities (evidence to verify) |
|---|---|---|
| EXW (Ex Works) | Packing suitable for collection; availability of export documents as agreed | Transport booking, export customs clearance (if arranged), insurance (if buyer-arranged) |
| FOB (Free On Board) | Packing for export, export customs clearance, delivery to vessel, export packing coordination evidence | Sea freight, insurance (if buyer), import clearance and duties |
| CIF / DDP | Packing, export clearance, delivery to named place, insurance for seller-leg | Import clearance (for CIF the buyer), site arrangements (for DDP the seller if agreed) |
Note: Use Incoterms rules as a framework and confirm specific responsibilities in the contract [3].
Factory quality documentation: what makes a compliant folder
- A structured folder should include: QA manual (or summary), inspection plans, hold points, mill certificates, welding/painting records, final inspection report, packing lists, and shipping declarations.
- Evaluate whether documents are signed, dated and linked to product serial numbers or part batches.
B2B supplier due diligence beyond technical evidence
- Financial stability, governance, sub-supplier management and insurance coverage.
- Past performance references and claims handling history for warranty and insurance events.
- Export control and sanctions compliance where applicable.
Decision table — documentation depth vs. procurement controls
| Procurement control level | Document depth required | Typical actions |
|---|---|---|
| Standard catalogue purchase | Basic mill certs, packing list | Desktop review, random inspection |
| Project-critical order | Full factory quality documentation, weld certs, pre-shipment inspection | Factory audit, witnessed tests, hold points |
| Integrated systems (PV, electrical) | All above + electrical test records, module mounting test reports | Specialist witnessed tests, installation interface protocol |
Site installation, commissioning and operations: audit implications
A factory audit should verify not just what leaves the gate, but how factory decisions affect on-site installation and long-term operation.
Installation readiness checks
- Pre-assembled modules: confirm how they are transported and if they exceed handling or crane capacities on site.
- Baseplate and anchor bolt tolerances: require a measurement protocol and acceptance limits to avoid on-site rework.
- On-site adjustments: identify factory tolerances and whether shims or cut-to-fit items are supplied for alignment.
- Lift and handling specifications: include weight, centre of gravity, and lifting points on packing lists.
Commissioning and handover
- Required documentation for handover: as-built drawings, torque reports, test certificates and maintenance manuals.
- Training: factory-supplied training for installers or a supervised first-install session can reduce early-life failures.
- Spare parts and warranty spares: clarify what spares are supplied with the shipment and what must be ordered separately.
Operations and maintenance
- O&M manual completeness: routines for bolted joint checks, surface maintenance, PV cleaning (if applicable), and periodic inspections.
- Warranty claims process: an evidence trail back to factory quality documentation simplifies claim validation.
Operational risk transfer
- Clarify when responsibility passes for damage during transit or storage — map this against the delivery responsibility matrix and ensure insurance aligns.
Implementation risks and mitigations
Common implementation risks and practical mitigations derived from factory audit findings:
- Misaligned scope between purchase order and factory production
- Mitigation: technical scope comparison during the audit; require sign-off on redrawings and change control.
- Material non-conformity arriving on site
- Mitigation: insist on batch certificates and implement a traceability and sample-testing regime; place hold points for critical items.
- Packaging failure in transit (leading to damage)
- Mitigation: require export packing coordination plan, witnessed packing checks, and photos of packed units prior to dispatch. Refer to export/import guidance where relevant [4].
- Insufficient welding or mechanical connection competence
- Mitigation: require weld procedure and welder qualification review; specify NDT or witness points for critical welds.
- Incomplete or illegible documentation for customs
- Mitigation: verify packing lists and commercial invoices during audit; confirm export compliance processes.
- Ambiguous responsibilities for installation defects
- Mitigation: define the delivery responsibility matrix in the contract and retain factory as-built and torque reports for claim resolution.
- Sub-supplier failure (e.g., fasteners, modules)
- Mitigation: request sub-supplier lists, critical component certificates and, where necessary, audit or sample-test critical sub-suppliers.
Risk register template (exemplar items)
- Risk: Foundation mismatch — Likelihood: Medium — Impact: High — Mitigation: Early technical scope comparison and pre-shipment baseplate measurement certificate.
- Risk: Corrosion on site due to incorrect surface treatment — Likelihood: Low — Impact: High — Mitigation: Verify surface treatment method and sampling per American Galvanizers Association guidance where applicable [1].
Six-step buyer workflow: a named process for procurement teams
A repeatable workflow helps embed the carport factory audit checklist into procurement controls and reduces ad-hoc decision-making.
- Define and lock the technical baseline
- Produce a clear technical scope and install interface drawings. Include installer, civil and electrical teams in review. Use a formal technical scope comparison to compare tender vs. supplier proposals.
- Commercial terms and delivery responsibility allocation
- Agree Incoterm and compile the delivery responsibility matrix. Clarify export packing coordination responsibilities and insurance. Align incoterms with the logistics provider and customs needs [3].
- Desktop due diligence and document request
- Request factory quality documentation, mill test certificates, welding records and packing plans. Score supplier evidence against minimum acceptable levels. This completes a first pass of B2B supplier due diligence.
- Execute the carport factory audit checklist
- Run the factory audit focusing on process controls, traceability, pre-shipment packing, and evidence supporting technical scope compliance. Produce an audit report with non-conformances and required corrective actions.
- Hold points, test witness and pre-shipment verification
- Agree and document hold points (e.g., post-welding, post-paint, pre-pack) and schedule witness tests. Verify packing by photos or witness packing, and confirm documentation for export/import compliance [4].
- Accept, ship and monitor post-delivery performance
- Accept shipments against the agreed documentation, perform site check against tolerance and torque reports, and enter warranty/maintenance records into asset management. Feed supplier performance back into procurement scorecards and project procurement controls.
Each step should map to responsible stakeholders, timelines and escalation paths.
Frequently asked questions (FAQ)
Q: What does a carport factory audit checklist typically include? A: It includes document reviews (quality certificates, material mill certs), physical inspections (storage, jigs, welding stations), process checks (WPS, painting, assembly), packing and logistics confirmation (packing list, export packing coordination), and verification of traceability and calibration records.
Q: How does the audit differ for integrated solar carports? A: Integrated solar carports require additional electrical interface checks: module mounting hardware, earthing continuity, cable management, DC/AC integration details, and electrical test records. You should require witnessed electrical insulation and continuity tests and confirm that mechanical and electrical scopes are reconciled.
Q: Can I rely on ISO certificates alone? A: No. ISO certification (e.g., ISO 9001) is informative about a supplier’s management system but does not guarantee specific product conformance. The factory audit verifies the implementation of processes and the presence of the concrete factory quality documentation needed for the project [2].
Q: When is a pre-shipment inspection sufficient instead of a full factory audit? A: Pre-shipment inspections may suffice for low-risk, repeat purchases where product design is standard and previous audits or strong documentary evidence exist. For bespoke, high-value or high-risk projects, integrate pre-shipment inspections as part of a broader audit and hold-point strategy.
Q: How should the delivery responsibility matrix influence audit scope? A: If the supplier is responsible for packing and export (e.g., FOB or DDP), the audit must include export packing coordination and documentation controls. If the buyer handles export, the audit still needs to verify that the goods are packed to the buyer’s specification for transport and storage [3].
Q: Who should perform the audit? A: Ideally a multidisciplinary team comprising procurement, technical engineering, quality assurance and logistics. For specialised tests (NDT, electrical), include qualified third-party technicians or witnesses.
Q: What if the supplier refuses an audit? A: Refusal to permit an audit is a procurement red flag. Options include conditional acceptance with extra documentary evidence, third-party inspection at shipment, or re-evaluating supplier suitability. Use contractual clauses to require access if audits are part of bid award terms.
Q: What governing standards should the audit reference? A: Reference relevant engineering and manufacturing standards and management standards like ISO for quality processes. For galvanizing and corrosion protection, use industry references (e.g., American Galvanizers Association) rather than inventing ad-hoc criteria [1][2].
Mid-article CTA If you would like a project-specific discussion of how the carport factory audit checklist should be applied to your specification, contact /inquiry or info@carportiva.com. You can review the Carportiva system range at the Carportiva system range and our sourcing guides.
Implementation checklist (practical items to close out before shipment)
Use this checklist in conjunction with your carport factory audit checklist as a pre-shipment closure tool.
- Technical scope signed-off by buyer and supplier (including electrical interfaces).
- All critical material mill certificates attached and cross-referenced to part numbers.
- Welding and painting records completed and signed.
- NDT and electrical test reports produced; witness signatures captured where required.
- Final inspection report completed and serial numbers assigned.
- Packing photos (full unit and critical areas) stored and shared.
- Export packing coordination plan complete; container blocking and bracing plan included.
- Customs documentation prepared and verified (commercial invoice, packing list, certificates).
- Delivery responsibility matrix finalised and accepted by both parties.
- Spare parts list and spare torque tools (if agreed) packed and documented.
- Maintenance and warranty documents included in the shipping paperwork.
Practical templates: two simple decision tables you can adopt
1) Audit necessity scoring (simple weighted model)
| Factor | Weight (%) | Supplier score (0–5) | Weighted score |
|---|---|---|---|
| New supplier / site | 20 | ||
| Order value / criticality | 25 | ||
| Custom interfaces / PV integration | 20 | ||
| Logistics complexity (cross-border) | 15 | ||
| Documentation completeness | 20 | ||
| Total | 100 | Sum (target: >60 suggests audit required) |
2) Document pack by procurement control level
| Document | Catalogue purchase | Project-critical | Integrated systems |
|---|---|---|---|
| Mill certificates | Yes | Yes (linked to parts) | Yes (linked) |
| Welding WPS & welder quals | Optional | Yes | Yes |
| NDT & electrical test records | No | Yes | Yes (witnessed) |
| Packing & export plan | Basic | Detailed | Detailed with photos |
| Final inspection report | Brief | Detailed | Detailed with witness |
These tables help quantify audit decisions and align evidence expectations to procurement controls and risk.
Closing considerations and constraints
- The carport factory audit checklist is a risk-control tool best used inside a documented procurement process with clear contractual alignment.
- It links directly to project procurement controls and reduces ambiguity on technical scope and delivery responsibilities.
- The checklist should be living: update it after every audit to capture supplier improvement and recurring non-conformances.
- Do not presume conformance: demand traceability from mill certificates to serialised parts and retain records for warranty and claims.
Important compliance note
- Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Conclusion
The carport factory audit checklist matters when procurement decisions carry technical complexity, high value or significant logistics and interface risk. It translates procurement requirements into verifiable factory evidence, aligns supplier capability to a delivery responsibility matrix, and supports a technical scope comparison that reduces downstream rework and disputes. Use the checklist as part of an end-to-end procurement workflow that includes desktop due diligence, a structured audit, defined hold points and post-delivery verification. For projects that involve integrated systems or cross-border deliveries, strengthen the checklist with witnessed tests, detailed export packing coordination and clear contractual obligations aligned to Incoterms and customs needs [3][4]. For tailored guidance on how this applies to a specific project or to review our product range, contact /inquiry or info@carportiva.com. Review our Carportiva system range and the full list of all systems and consult our sourcing guides for additional procurement templates and checklists.
References (selected)
- American Galvanizers Association — galvanizing guidance and technical resources [1].
- International Organization for Standardization — management system standards applicable to quality assurance [2].
- Incoterms rules — to align delivery responsibility and contractual obligations [3].
- U.S. Customs and Border Protection — import and documentation guidance relevant to export packing coordination and customs compliance [4].
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion