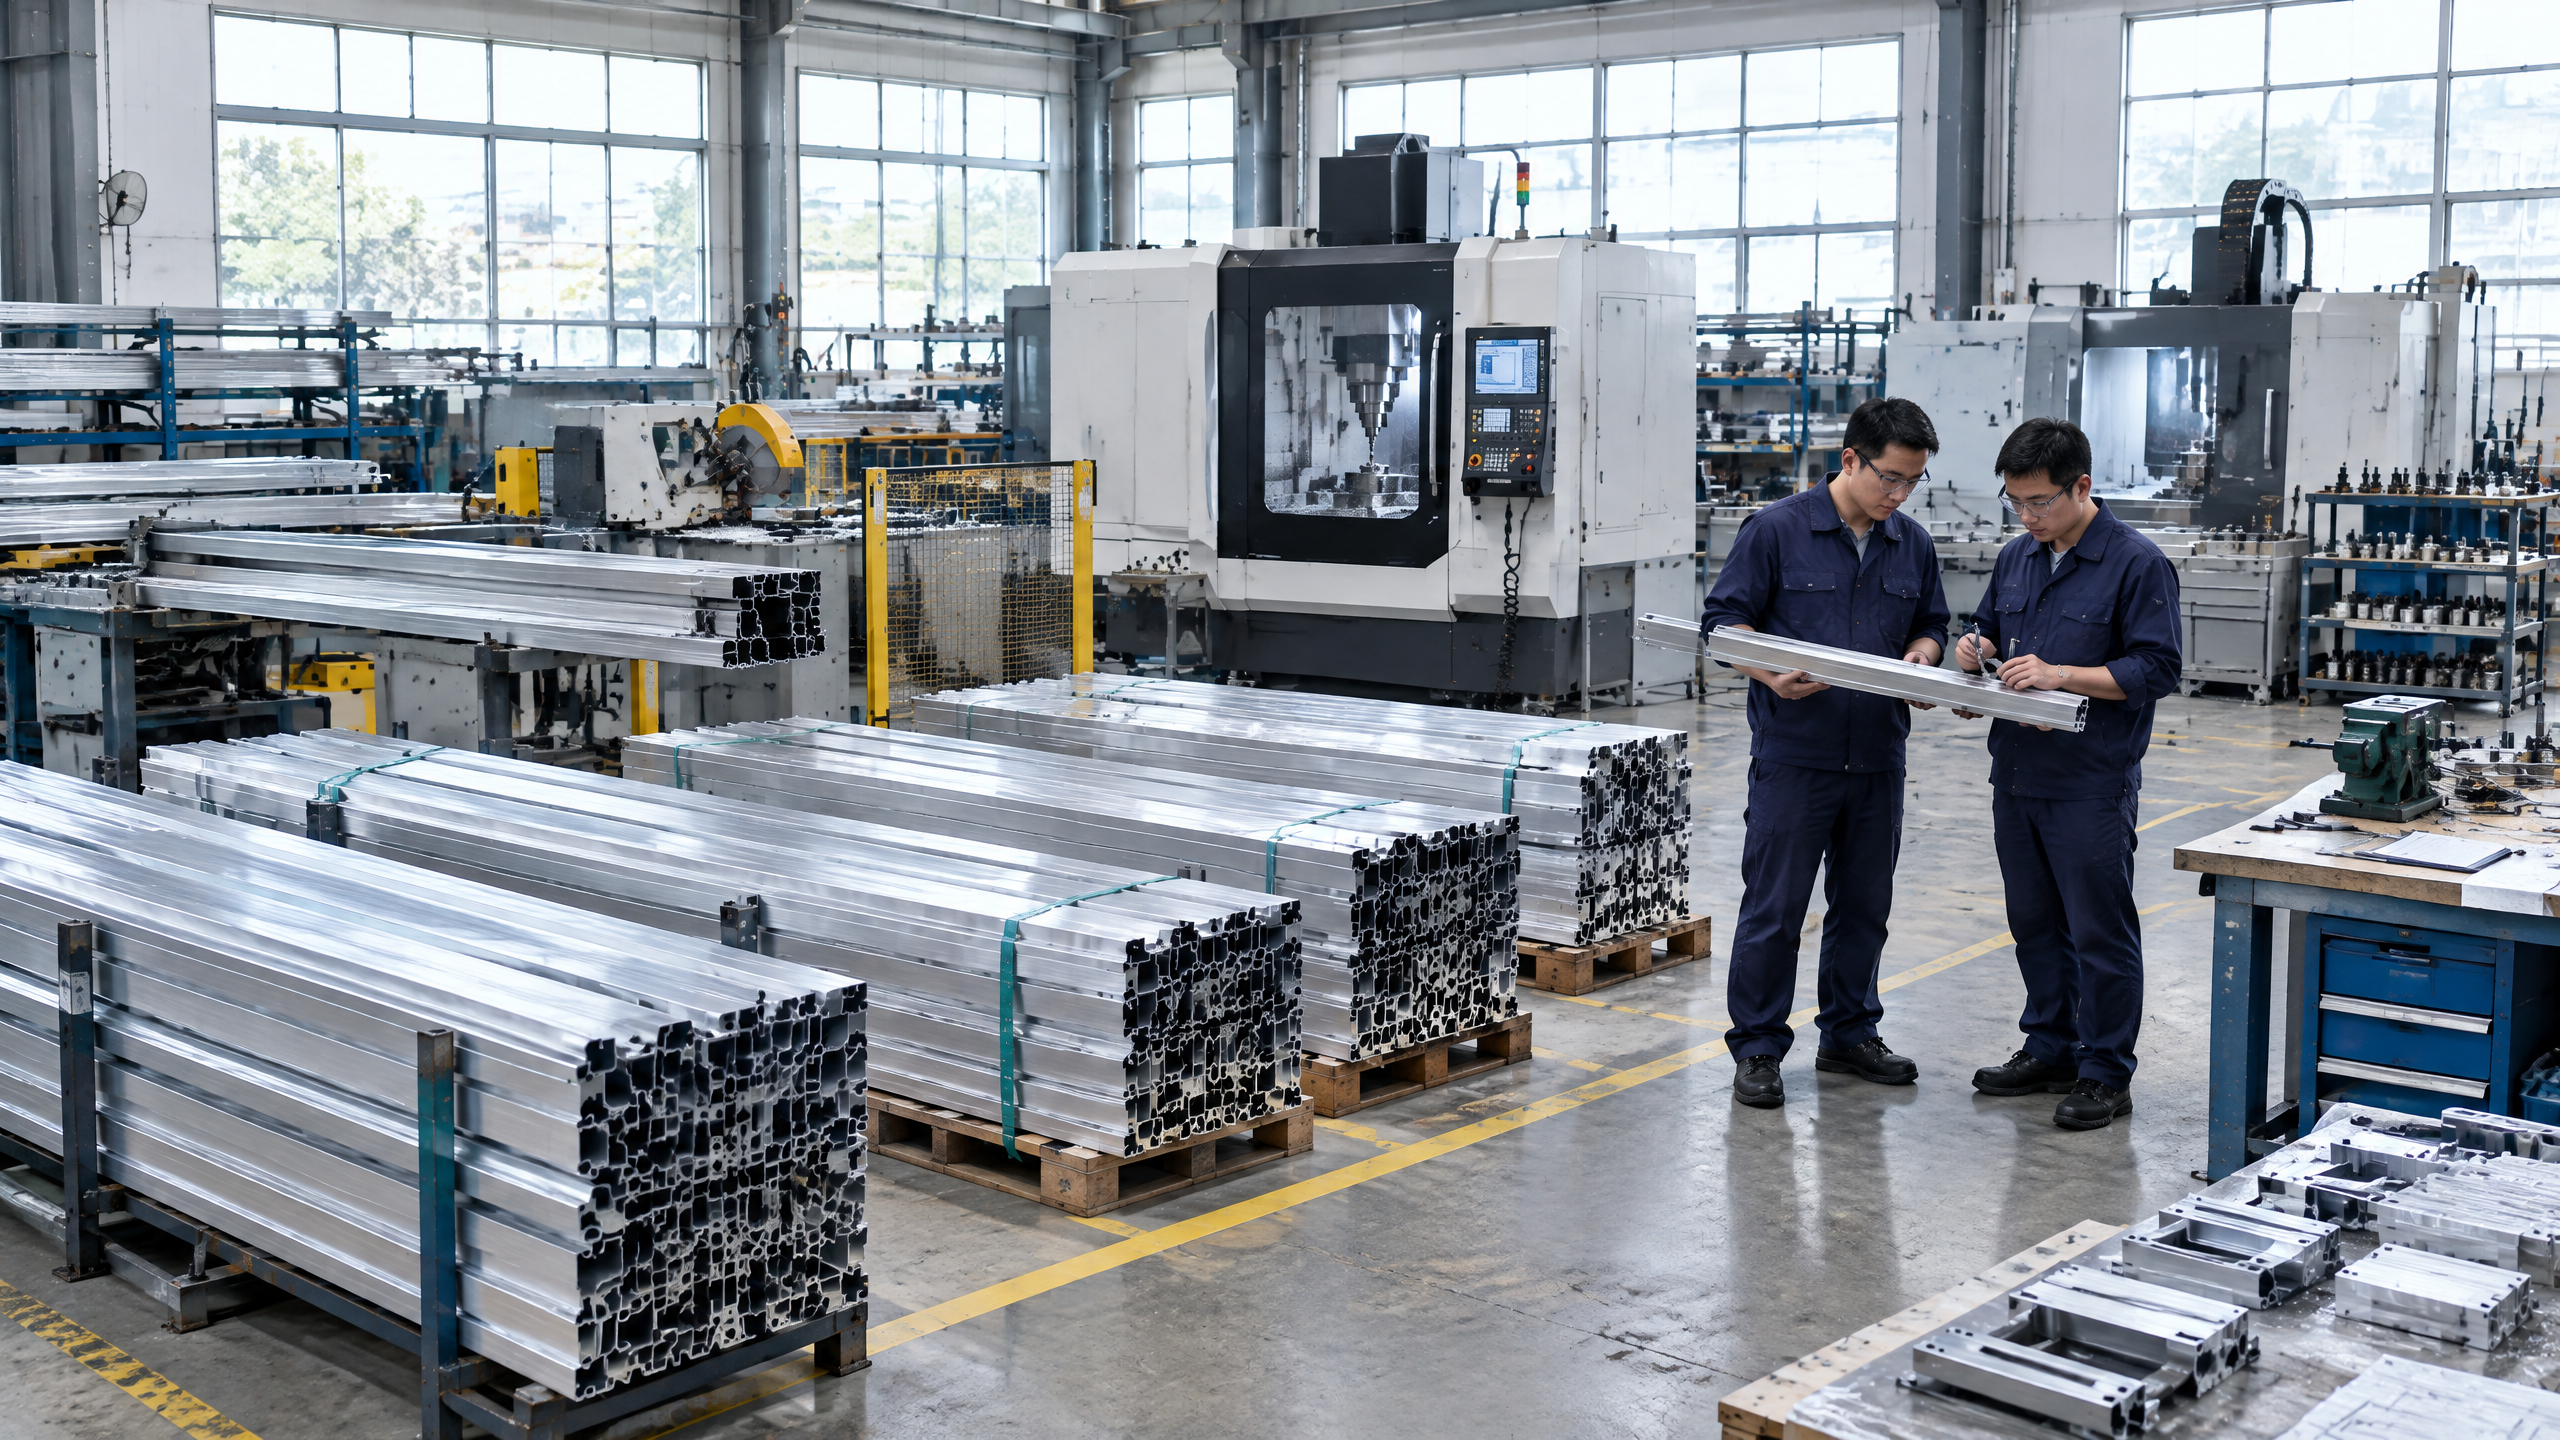
A carport incoming-goods inspection must be a documented, repeatable sequence that verifies delivered components against controlled procurement documents before parts move to storage or installation. At minimum it should confirm identity, quantity and condition of items, match material certificates to specified grades and finishes, cross-check the carport packing list and delivery paperwork, record any transit damage and issue a site receipt record or non-conformance report when deviation occurs. The inspection scope should be risk-based: higher-risk items (structural members, plant-fabricated assemblies, electrical/power interfaces) require more detailed checks and documentary evidence; routine ancillary items can follow sampling rules. A robust inspection links factory evidence (packing lists, mill certificates, photos) to on-site checks, uses clear disposition rules for acceptance/hold/reject, and preserves evidence for warranty, customs and contractor handover.
Buyer context and scope boundary
Purpose and audience
- This guide is written for B2B buyers of Carportiva architectural aluminium carports, commercial solar carports and industrial/fleet shelters: distributors, architects, contractors, developers, solar EPCs and fleet operators.
- The objective is a pragmatic, risk-focused incoming inspection that prevents installation of non-conforming parts and reduces rework, schedule risk and warranty disputes.
What this guide covers
- Visual and documentary checks to confirm identity, quantity and condition.
- Material certificate matching, surface/coating checks, and basic dimensional verification where practical.
- Processes for recording site receipt record entries, issuing a non-conformance report, and preserving evidence for later warranty or customs needs.
What this guide does not cover
- Design, structural calculations, foundation design, electrical design and commissioning, local permit compliance, or energy-yield modelling. These items require a documented project basis and input from local qualified professionals, installers, utilities and authorities (see required project-note statement later).
- In-field structural testing, load testing or certification beyond checking supplied factory certificates and batch traceability.
Scope boundaries and responsibility matrix
- Supplier responsibility: produce agreed items per contract, provide the carport packing list check, material certificates, factory inspection reports and pre-shipment photos.
- Buyer responsibility: perform delivery quantity verification, transit damage inspection and material certificate matching on receipt, issue site receipt record and non-conformance report as required.
- Where contracts use seller-minor-hold/Incoterm handover rules, refer to agreed Incoterm for transfer of responsibility and risk [3].
Core decision principle
The single decision rule for incoming goods is: do not release to installation unless documentation and inspection evidence together establish conformity to contractual requirements or acceptable disposition is recorded.
Key elements of the decision principle
- Documentation-first: required documents (packing list, material certificates, factory inspection report) must be present and consistent with the physical shipment.
- Identity and quantity: every item or sample must be identifiable and counted against the carport packing list check and purchase order.
- Condition and safety: any transit damage inspection must determine whether an item is safe to install or requires repair/replacement.
- Traceability: material certificate matching must link mill/heat/batch numbers to delivered items.
- Formal disposition: site receipt record must capture acceptance/rejection, and a non-conformance report must be raised when deviations affect fit, function or safety.
This rule emphasizes evidence before action. For high-risk items (primary support members, fabricated trusses, PV module rails, electrical junction components) require full documentary match and zero-tolerance for missing certificates. Low-risk consumables can be accepted on sampling and later verification.
Planning inputs: what to prepare before delivery
Inspection readiness checklist
- Approved drawing set and parts list (revision-controlled).
- Purchase orders with item codes, finishes and acceptance criteria.
- Expected delivery schedule and staging plan.
- Pre-shipment documentation via supplier: signed factory inspection report, carport packing list check, mill/test certificates, photos of crating/securement.
- Named inspection team with defined roles (receiving clerk, technical inspector, safety officer), equipment and PPE.
- Templates for site receipt record and non-conformance report.
People and roles
- Receiving clerk: matches packing list, signs off basic delivery quantity verification.
- Technical inspector: verifies material certificate matching, dimensional and finish checks, and coordinates transit damage inspection.
- Safety officer: ensures safe unloading and checks for hazardous packing materials.
- Contract administrator: logs acceptance/rejection decisions and manages supplier communications.
Tools and equipment
- Digital camera or phone for photographic evidence (date/time-stamped).
- Basic measuring tools (tape, calipers for sample checks).
- Torque wrench if fasteners are pre-torqued or assembled.
- Protective storage covers and racks to control corrosion risk after acceptance.
- A locked, documented process for quarantine and tagging of rejected items.
Scheduling and communication
- Schedule a receiving window to avoid congestion and provide proper unloading equipment.
- Confirm who bears unloading responsibility per contract/Incoterm [3].
- Require that supplier sends digital copies of the carport packing list check and material certificates at least 24–48 hours before arrival to enable pre-matching.
Key documents to request in advance
- Packing list with itemised SKUs and weights.
- Mill/heat/material test certificates for structural aluminum and alloyed components.
- Surface-treatment certificates (anodizing, powder coat, galvanizing notes where ferrous steel is used) — see coating guidance with reference to galvanizing best practice [1].
- Factory inspection and assembly photographs.
- Handling and storage instructions.
Technical specifications and interfaces to check
Critical technical interfaces to verify on arrival
- Structural members: profile identification, dimensional check at representative points, visible weld quality and connection holes.
- Coatings and finishes: color match, uniformity, adhesion declarations and any passivation/anodizing specification.
- Fasteners and accessories: material (stainless grade), count, fitment, and lubrication/coating.
- Pre-assembled units: squareness, bolt torque, fit of connectors and integrity of pre-welded assemblies.
- Electrical interfaces (for solar carports): conduit entries, trunking, junction boxes, earthing points and routing provisions — coordinate with electrical design package.
Material certificate matching
- Match material certificate data (alloy grade, temper, mill batch/heat number) to item markings or tags on the delivered parts.
- Certificates should be legible, signed by authorised laboratory or mill and reference the specific batch numbers present on parts.
- Where third-party testing was required in the contract, confirm the certificate meets the sampling and test method requirements outlined in the contract.
Surface and corrosion protection
- For any ferrous components (brackets, anchors) verify coating specifications and inspection certificates. When zinc coatings are specified, consult galvanizing guidance for acceptable coating ranges and inspection considerations [1].
- For aluminium components verify anodizing or powder-coat standard and batch evidence; check for contamination, blistering or orange-peel texture inconsistent with the specification.
Dimensional tolerances and fit
- Use project tolerance table (purchase document) for acceptable dimensional deviations. For assemblies, check a sample or first-in-lot for accurate hole alignment and bolt fit.
- If the carport integrates PV modules, confirm module rail spacing and clamp compatibility with the module supplier’s installation instructions.
Documentation and sign-off criteria
- Define clear pass/fail criteria for visual inspection, dimensional checks and certificate presence.
- Require written sign-off on the site receipt record for accepted lots and documented hold status for non-conforming lots.
Procurement and factory evidence to require and verify
Essential factory-supplied evidence
- Carport packing list check: an itemised packing list that matches purchase order SKUs and quantities and shows packing locations (crate, pallet, box).
- Factory inspection report: signed checklist from factory quality control evidencing assembly checks, torque records if applicable, and photographs.
- Material certificates: mill or test certificates for structural alloys and any critical fastener batches.
- Shipping documentation and Incoterm confirmation: commercial invoice, packing list, bill of lading/airway bill and Incoterm allocation of risk and responsibility [3].
- Pre-shipment photographs: images of crates, internal packing and distinctive parts to speed identity checks.
How to verify documents on arrival
- Cross-match the supplier’s carport packing list check to the physical load before unloading; ensure counts and package identifiers match.
- Use the material certificate matching process: read batch/heat numbers on certificates and on metal tags, ambient markings or supplier labels.
- Validate the factory inspection report against photographs and any on-factory QC signatures or stamps.
- If document copies are missing, hold delivery and request immediate electronic transmission; do not accept critical structural items without certificates.
Document retention and traceability
- Keep digital and physical copies of all documents and photographs linked to the site receipt record for warranty, customs and handover.
- If parts are routed to multiple sites, create unique lot identifiers and retain traceability records for each destination.
Regulatory and customs considerations
- Prepare to present documentation to customs authorities where required; consult local import guidance and ensure commercial invoices and packing lists are accurate to avoid delays [4].
- For cross-border shipments confirm that product descriptions, HS codes and origin marks are consistent with customs declarations.
Quality management alignment
- Encourage suppliers to operate to ISO quality management processes; reference ISO purchasing and inspection guidance to align inspection content and records [2].
Decision table — Document evidence vs minimum acceptance action
| Document present | Matches PO & packing list | Action required |
|---|---|---|
| Yes / Yes | Yes | Proceed to unload and perform physical inspection. Create site receipt record. |
| Yes / No | No | Quarantine shipment; open non-conformance report; request corrective documentation from supplier. |
| No / Yes | N/A | Do not accept critical structural items; allow acceptance of low-risk consumables subject to supervised unloading and supplier follow-up. |
| No / No | N/A | Reject delivery or accept under explicit written temporary concession with hold and documented risk transfer per Incoterm [3]. |
Site receipt, handling and installation operations
Unloading and safety
- Confirm safe access, available lifting equipment, adequate staging area and required PPE.
- Require supplier to supply any special lifting fixtures or instructions included in the pre-delivery data.
- If handling instructions are part of the packing list or factory documents, ensure strict compliance to avoid damage.
Delivery quantity verification and initial checks
- Perform delivery quantity verification on receipt: match visible package counts and SKUs to the carport packing list check before or during unloading.
- Mark crates/pallets with unique receipt identifiers and annotate discrepancies on the carrier delivery note.
Transit damage inspection
- Conduct transit damage inspection immediately upon unloading and before storage: photograph any dents, bent flanges, ruptured crates, fluid stains or exposed unprotected edges.
- For suspected internal damage (concealed damage) note visible signs and, if necessary, open packaging in presence of carrier or inspector to document concealed damage.
Site receipt record and custody
- Complete a formal site receipt record for each lot: include document cross-references, observed defects, acceptance status and the inspector’s signature.
- Tag accepted items with acceptance tags; tag quarantined items as "HOLD" and attach the non-conformance report.
Storage and preservation
- Store components off the ground on pallets or racks with separation to avoid surface-to-surface contact.
- Protect raw aluminium against direct contact with dissimilar metals, saltwater or acidic materials; follow supplier storage notes.
- For long lead times prior to installation, further preservation (protective coverings, desiccant, regular inspection) may be required.
Non-conformance handling and corrective action
- If non-conforming items are found, raise a non-conformance report immediately, record the batch and associated material certificates and notify supplier with photographic evidence.
- Agree corrective action: rework on-site, return to factory, or replacement, and set timelines for response. Capture any temporary acceptance concessions in writing.
Installation handover
- Do not release components to the installation team without an explicit site receipt record showing acceptance or approved disposition.
- Provide the installation team with copies of any constraints (tight tolerances, special fixation requirements, sequencing) and the corresponding certificates and connection details.
Decision table — Inspection result vs disposition and evidence required
| Inspection result | Disposition | Evidence to attach to site receipt record |
|---|---|---|
| Conforms fully | Accept | Packing list, material certificates, photos of received condition, inspector sign-off |
| Minor cosmetic damage (does not affect function) | Conditional accept | Photos, written supplier concession, agreed on-site repair scope |
| Missing documentation (e.g., material certificate) | Quarantine / Hold | Tagging, non-conformance report, request for supplier certificate within agreed timeframe |
| Major damage or incorrect item | Reject | Photos, carrier note, non-conformance report, initiation of replacement logistics |
Implementation risks and mitigation strategies
Key implementation risks
- Missing or incomplete material certificates — risk to structural integrity assessment and future warranty claims.
- Transit damage not detected in time — risk to installation quality and safety.
- Incorrect finishes or coating failures discovered post-installation — costly rework.
- Miscounted or missing parts leading to installation delays and site idle time.
- Customs and import delays due to incomplete documentation — schedule and cost impacts.
- Disputes on responsibility when Incoterms are not clearly applied — legal and commercial risk.
Risk mitigation measures
- Require pre-shipment documentation and photos at least 24–48 hours before arrival.
- Insist on batch marking on parts that matches material certificates; sample-match prior to acceptance.
- Use hold-and-release procedures with clear timelines for supplier corrective action.
- Include inspection acceptance milestones in payment terms and release only after documentary compliance.
- Require supplier to provide packaging and handling instructions and include damage thresholds in contract.
- For high-value or mission-critical projects, mandate third-party inspection at factory or at point-of-origin.
Risk escalation protocol
- Minor deviations → document and allow conditional acceptance with agreed rectification plan.
- Major deviations or safety-impacting defects → stop release, quarantine, issue non-conformance report and trigger supplier corrective action and replacement logistics.
- Customs/document issues → engage customs broker and contract administrator immediately to remedy.
Evidence preservation to reduce dispute risk
- Timestamped photos at unloading and during any opening of packaging.
- Digital copies of all certificates and supplier QC reports uploaded to contract document repository.
- Detailed site receipt records and signed carrier delivery notes, including reservations or caveats.
A named six-step buyer workflow for incoming carport parts
This is a workable, repeatable six-step workflow buyers can adopt. Each step specifies the main actor and minimum evidence required.
- Pre-arrival verification (Procurement / Contract Admin)
- Action: Confirm supplier has sent the carport packing list check, factory inspection report and material certificates at least 24–48 hours before shipping.
- Evidence: Electronic documents saved in procurement system; notification to receiving team.
- Unloading and safety check (Site Supervisor / Safety Officer)
- Action: Verify safe unloading conditions, verify carrier and Incoterm responsibilities [3], check packaging integrity before moving crate.
- Evidence: Safety checklist, carrier manifest acknowledgement.
- Delivery quantity verification (Receiving clerk)
- Action: Count visible packs and match to packing list; annotate any discrepancies on carrier paperwork.
- Evidence: Annotated packing list, photographic record.
- Transit damage inspection and initial acceptance (Technical Inspector)
- Action: Perform transit damage inspection on accessible items, document any visible or concealed damage with photos and measurements.
- Evidence: Photographs, preliminary damage log.
- Material certificate matching and technical checks (Technical Inspector / QA)
- Action: Match batch/heat numbers on material certificates to part markings; perform required dimensional or finish checks on samples.
- Evidence: Matched certificate pages, measurement log, test sampling notes.
- Site receipt record and disposition (Contract Admin / QA)
- Action: Create the site receipt record, attach all evidence, accept or raise a non-conformance report and define corrective action and timelines.
- Evidence: Signed site receipt record, non-conformance report (if any), supplier acknowledgement.
This workflow is designed to be scalable: for multi-site deliveries, include unique lot IDs and a central document repository.
Frequently asked questions (FAQ)
Q: Who should sign the site receipt record? A: The site receipt record should be signed by the responsible receiving representative on behalf of the buyer (receiving clerk or site supervisor) and by the carrier where possible. An additional technical inspector signature is recommended for structural deliveries.
Q: Can I accept a delivery without material certificates and obtain them later? A: For low-risk consumables this can be acceptable with documented buyer concession. For structural items and critical interfaces (primary members, electrical components), do not accept without material certificate matching. Record any temporary concession and set strict timelines in the site receipt record.
Q: When should a non-conformance report be issued? A: Issue a non-conformance report whenever the delivered item does not match the contractual specification, is damaged beyond minor cosmetic impact, or lacks required documentation that affects fitness for installation.
Q: Can photographs be used as the only evidence of pre-shipment condition? A: Photographs are helpful but insufficient alone. They should be combined with packing lists, factory inspection reports and certified material certificates to build a defensible acceptance record.
Q: What is concealed damage and how is it handled? A: Concealed damage is damage not apparent until packaging is opened. If suspected, open the packaging in the presence of the carrier or an independent witness, photograph the condition, raise a non-conformance report and notify the supplier promptly.
Q: Are third-party inspections necessary? A: For high-value or critical structural components, third-party factory or pre-shipment inspections reduce risk. This requirement can be contractually mandated and should be coordinated in the planning phase.
Q: How long should records be retained? A: Retain inspection documents, certificates and photographs according to your contract and warranty terms. Many projects retain records at least the duration of the warranty plus any required statutory periods; consult your legal and records policy.
Q: What about customs and import documentation? A: Ensure packing lists, commercial invoices and origin declarations align with customs requirements. Retain these documents as they may be required for release or duty claims [4].
Decision tables and example dispositions
Decision table — Quick disposition guide for common arrival scenarios
| Scenario | Immediate action | Document/communication |
|---|---|---|
| All docs present, items undamaged | Accept | Site receipt record + photos |
| Packing list matches but missing material certificates for primary members | Hold | Non-conformance report; request certificates; do not release to install |
| Visible damage to critical member | Reject or hold | Non-conformance report; photographic evidence; carrier damage claim initiated |
| Minor cosmetic damage to non-structural part | Conditional accept | Documented repair plan; supplier concession; updated site receipt record |
| Short shipment of non-critical consumables | Accept with remedy plan | Delivery note annotated; supplier replacement schedule |
| Customs paperwork incomplete on cross-border delivery | Hold | Engage customs broker; provide accurate docs; update stakeholders |
Decision table — Who verifies what (roles and responsibilities)
| Item / task | Supplier | Receiving clerk | Technical inspector | Contract admin |
|---|---|---|---|---|
| Provide carport packing list check | X | |||
| Provide material certificates | X | |||
| Delivery quantity verification | X | |||
| Transit damage inspection | X | X | ||
| Material certificate matching | X | |||
| Create site receipt record | X | |||
| Issue non-conformance report | X | X | ||
| Coordinate replacement logistics | X | X |
Conclusion and next steps
A structured carport incoming goods inspection provides risk reduction and a clear, auditable trail from factory to installation. The inspection combines documentation verification (carport packing list check, material certificate matching, factory inspection reports) with on-site checks (delivery quantity verification, transit damage inspection), and formal disposition via site receipt record or non-conformance report.
For buyers of Carportiva systems, adopt the six-step workflow above, require pre-shipment evidence from suppliers, and maintain a disciplined hold-and-release process for any deviation. For product information and system selection, see the Carportiva system range in our catalogue and review all systems to confirm the specified item codes and accessories. For procurement templates and related processes consult our sourcing guides. If you would like help applying this inspection workflow to a specific procurement, please contact our team via /inquiry.
Important project note: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and input from relevant local qualified professionals, installers, utilities and authorities. This guide is a procurement and receiving process guide and does not replace those necessary project activities.
For tailored procurement support or to initiate a project conversation, contact us at info@carportiva.com.
References and further reading
- American Galvanizers Association — guidance on zinc coatings and inspection considerations [1].
- International Organization for Standardization — quality and purchasing standards that can guide supplier documentation and control [2].
- ICC Incoterms — for clarity on delivery and transfer of risk responsibilities [3].
- U.S. Customs and Border Protection — basic import documentation guidance [4].
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion