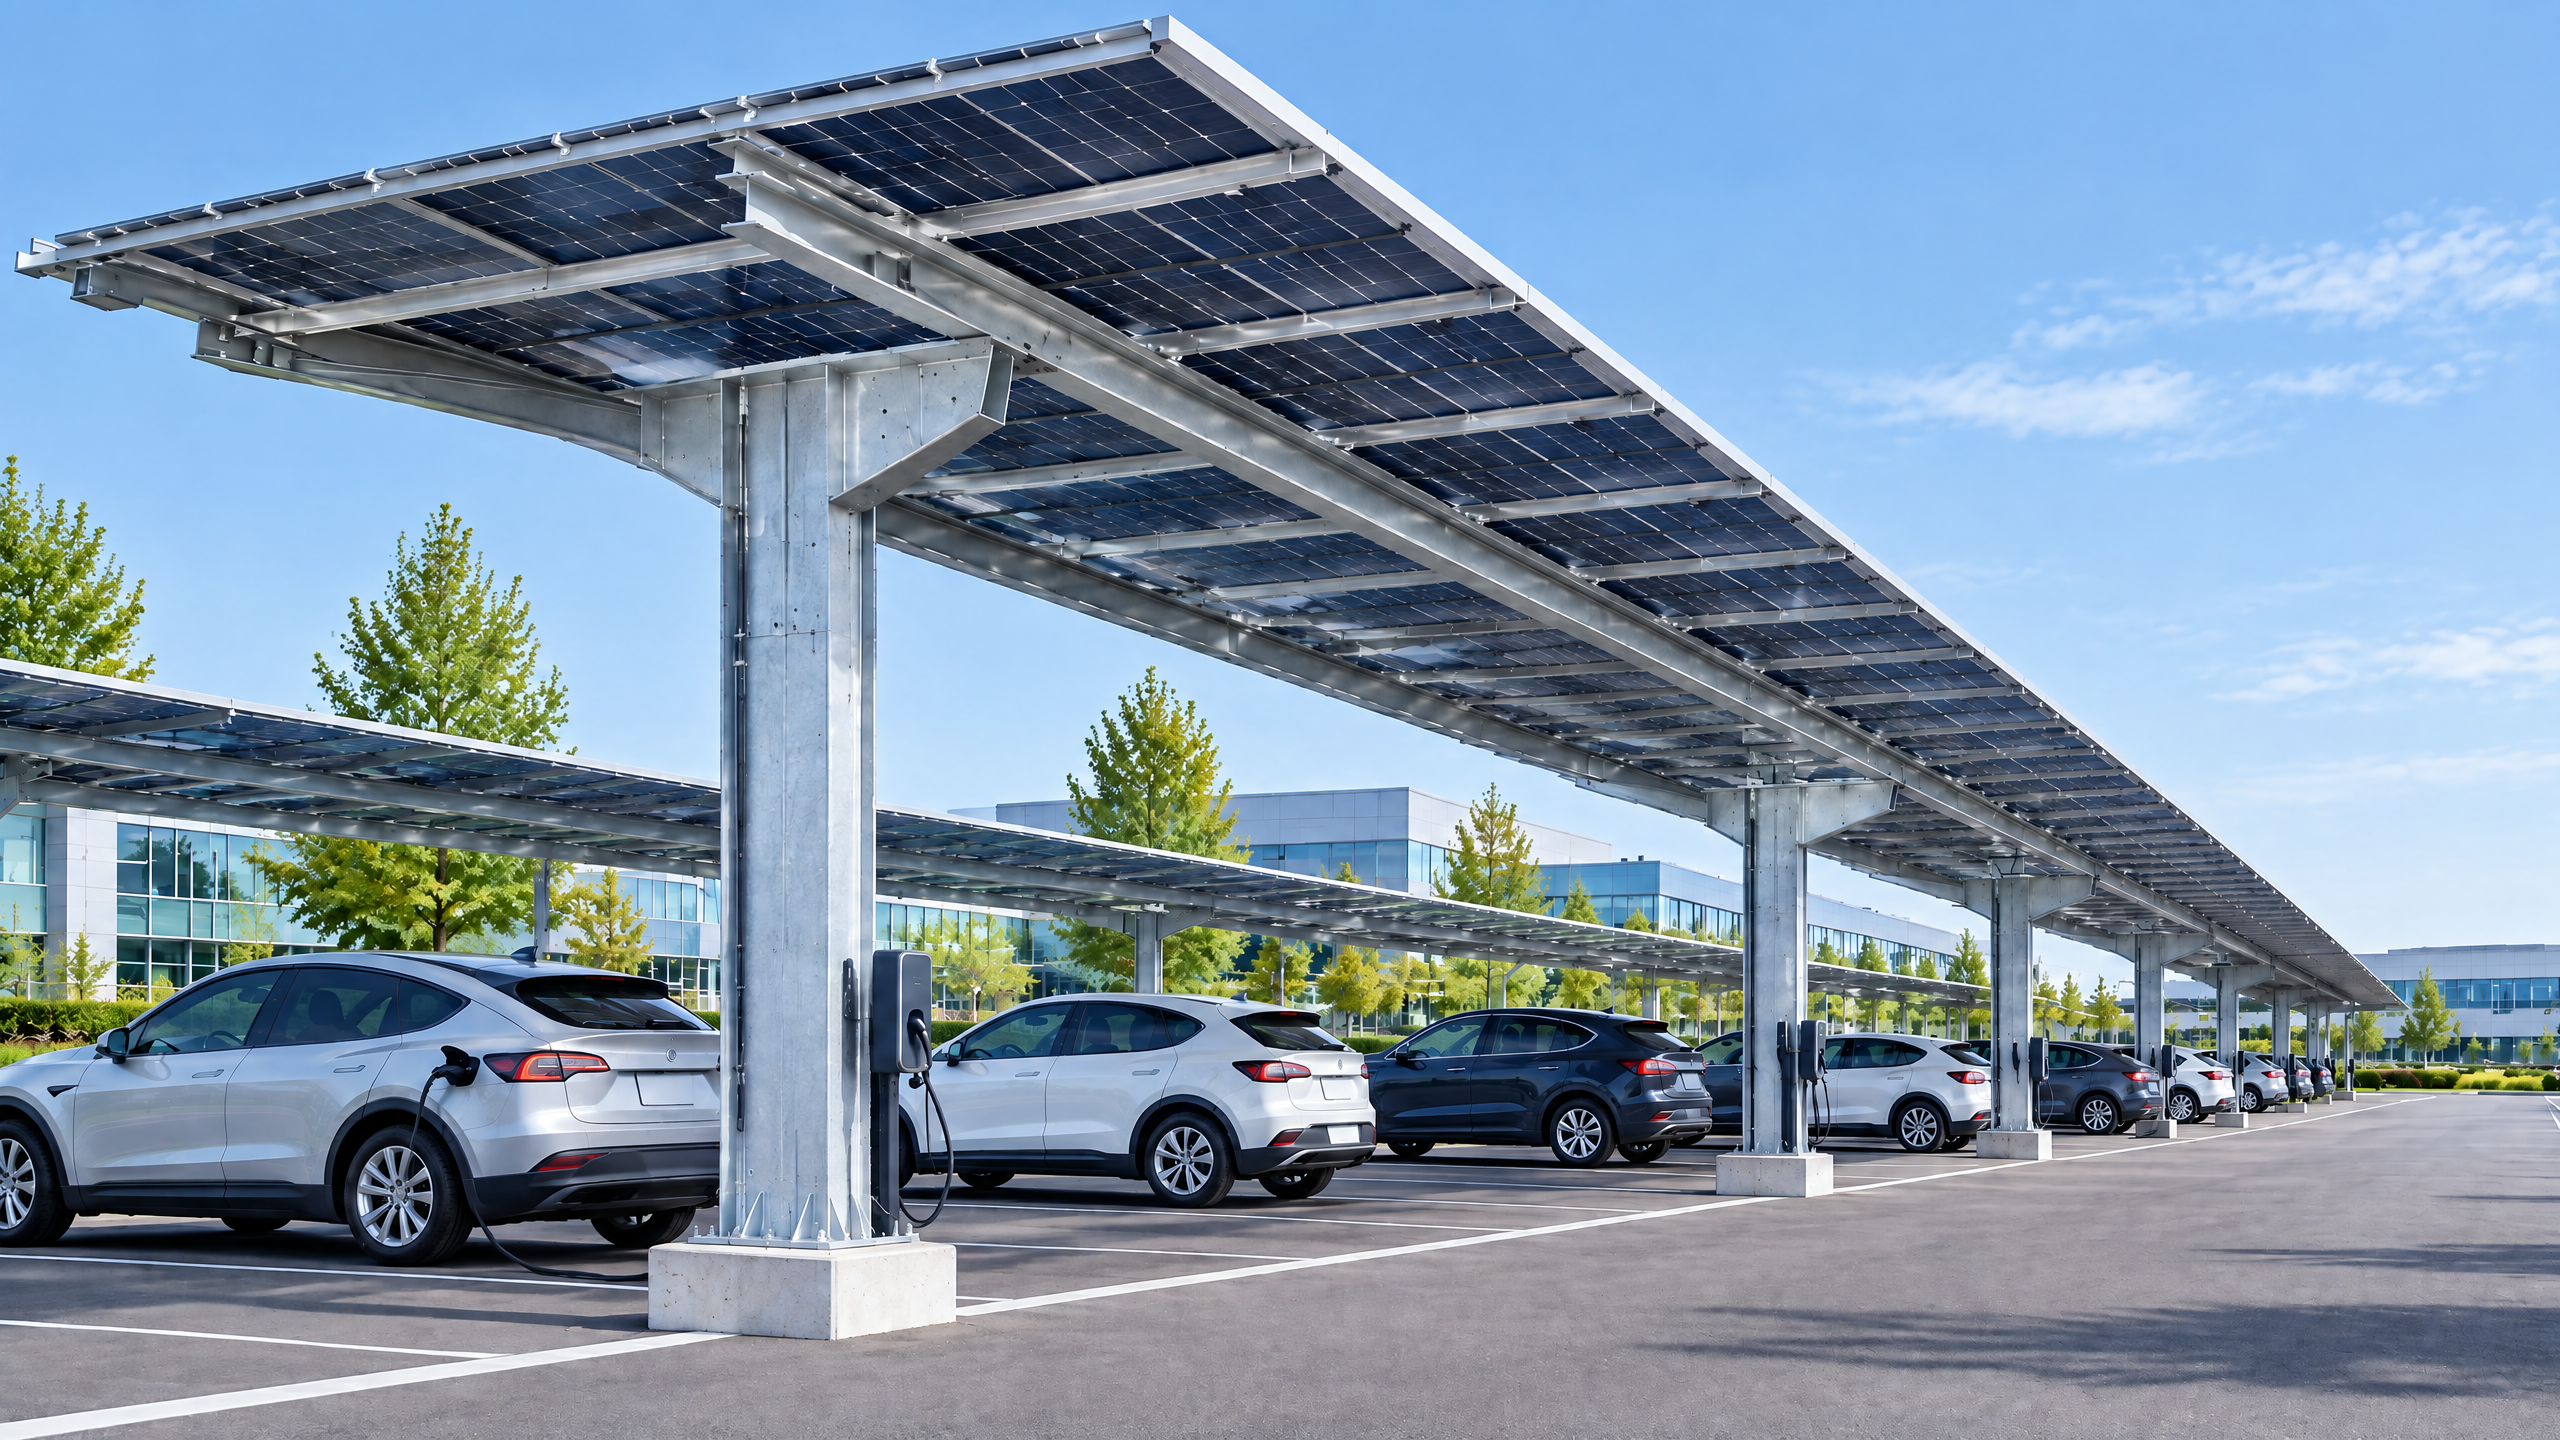
Clear specification of the solar carport manufacturer PV interface is the single most important procurement control that determines cost, delivery risk and site-installation friction for commercial carport projects. A PV interface specification defines where the manufacturer’s scope ends and the buyer’s (EPC/contractor/structural engineer) scope begins: mechanical mounting and rail geometry, module clamping zones, grounding/earthing provisions, cable routing and access points, DC/AC handover locations, and packing/delivery formats. For B2B buyers this is a procurement artefact — it should be evidence-led, unambiguous and contractually referenced to protect schedule, quality and warranty outcomes. Use explicit delivery responsibility matrices, factory quality documentation and export packing coordination instructions; require supplier evidence through B2B supplier due diligence and a documented technical scope comparison during tender evaluation. Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Buyer context and scope boundary: what "PV interface" actually covers
The term "PV interface" within a commercial solar carport procurement context describes all physical and electrical connection points where the carport structure and the photovoltaic (PV) system interact. To set practical boundaries for procurement and minimise downstream change, define whether the carport manufacturer is responsible for:
- The structural support sub-system for PV modules (rails, clamps, module seats).
- Foundation-to-column interface and anchor specifications (often provided as a design-for-construction output).
- Integrated cable containment, routing channels, combiner box housings, and cut-outs for electrical hardware.
- Earthing/grounding bonding points and specified lug types.
- Module-to-structure clamps and module carrier geometry (affects module compatibility).
- Mechanical access provision for inverter/combiner servicing (platforms, clearances).
- Protection against corrosion for metallic parts and finish standards.
Roles typically involved: buyer (owner/developer), distributor, carport manufacturer, PV module supplier, electrical contractor/EPC, structural engineer, civil contractor and local authorities. The specification must clearly state who supplies what, referencing drawings, product data sheets, and acceptance criteria. Ambiguity here drives claims, rework and schedule slippage.
Key boundary rule-of-thumb: anything that affects electrical interconnection point(s), the physical mounting interface to the PV module frame, or the handover location for DC cabling must be explicitly called out and allocated to a single party in contract documents.
Core decision principle: allocate responsibility to control cost and delivery risk
The primary procurement decision principle is to convert interface ambiguity into contractual clarity. Three practical controls convert that principle into action:
- Freeze a documented Project Basis of Design: a single, version-controlled file set that includes site loads (wind, snow, seismic), module model(s), inverter/combiners model and location, and permitted foundation types.
- Apply a delivery responsibility matrix (DRM) in the contract and purchase order that maps every deliverable (mechanical, electrical, packaging, documentation) to a named party and acceptance criteria.
- Require factory quality documentation, packing instructions and an export packing coordination plan before the first production shipset departs the factory.
Using these controls reduces the most common failures: mismatched module mounting geometry, missing cable entries at combiner locations, and unexpected import delays because packing or documentation did not meet local customs or utility requirements.
Decision highlight: Pricing comparisons that omit delivery terms, packing responsibilities and acceptance criteria create artificially low bids. Specify Incoterms explicitly and combine them with a delivery responsibility matrix to quantify risk and cost allocation. Reference relevant Incoterms to the ICC rules for clarity during contracting [3].
Planning inputs: what to collect before you write the PV interface spec
Before drafting tender documents or PO line items, collect the following planning inputs. Each item should be captured in the project basis and shared with all bidding manufacturers:
- Definitive site survey and coordinate grid (topographic, utilities, obstructions).
- Structural design criteria (design wind speed, snow load, seismic zone) and representative foundation types (pile, pad, slab). If geotechnical data exists, include it.
- Selected PV module model(s) and module frame profile/dimensions, or a banded list of acceptable module frames and clamping zones.
- Inverter and combiner location(s), required DC isolator positions and stringing maps.
- AC interconnection point(s) and meter location(s).
- Fire-safety and access requirements (clearways, panel access, spacing for emergency services).
- Corrosion zone classification (coastal, industrial) to determine surface treatment and finish.
- Desired warranty envelope (structural, waterproofing, galvanic isolation, finish).
- Delivery constraints: earliest manufacturing start date, phased delivery windows, staging areas, and import/customs considerations.
- Local code references and permit timelines.
Document each input as an auditable item; changes should trigger a change-order mechanism. Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Technical specification and interfaces: what you must define explicitly
A robust PV interface specification is organized into mechanical and electrical subsections. Each clause should state acceptance criteria (dimensions/tolerances), testable performance outcomes and documentation deliverables.
Mechanical interface points to define
- Module clamp zone envelope: exact frame contact area (recommended in mm), clamp types, maximum allowable torque and any acceptable module anti-lift features.
- Rail geometry and module pitch: spacing between module rows, rail height off deck, module tilt (if any), and mounting rail profile cross-section. Indicate whether rails are continuous or segmented.
- Structural connections: column-to-rail connections, brace geometry, design loads and connection details. Define allowable field modifications.
- Foundation interface: anchor type, plate dimensions, grout levels and anchor embedment. Specify whether bolt patterns are provided or must be adapted by the civil contractor.
- Corrosion protection: hot-dip galvanizing class or paint system, reference to galvanizing guidelines; provide surface treatment acceptance and visual inspection criteria. Relevant guidance on galvanizing practices is available [1].
- Access and serviceability: clearance zones around inverters/combiners, walkway provisions and maintenance access sequencing.
Electrical interface points to define
- DC handover point: location where module strings, MC4 or equivalent connectors and cabling are handed over to the electrical contractor; specify connector type, entry point size and gland type.
- Earthing/grounding points: define bonding lug locations, conductor size, and grounding conductor termination details.
- Combiner box and inverter mount interface: include cut-out sizes, mounting tolerances and weight support capacities.
- Cable management: cable tray routing, minimum bend radii, separation between DC and AC wiring and cable entry detail into enclosures.
- Monitoring hardware: housings, telemetry pathways, DC monitoring shunt or string-level monitoring locations and cable runs.
- Lightning protection and surge protection device (SPD) accommodation.
- Testing and commissioning acceptance tests that the factory is expected to pre-test (if any).
Technical tolerances and testable acceptance
- Provide dimensional tolerances on interface features (e.g., +/- 2 mm for rail bolt hole centers over a 3 m span).
- Require pre-shipment dimensional checks, torque check protocols and inspection records as part of factory quality documentation.
- Define electrical continuity and bonding resistance limits for earthing connections and require test records.
Standards and management systems
- Require the manufacturer to document quality management controls (QMS) consistent with ISO quality practices [2], and to provide traceability for structural-grade materials and fasteners.
- Specify applicable finish and corrosion standards; refer to galvanizing best practice [1].
Procurement and factory evidence: what to ask for, and why
Robust procurement controls convert supplier claims into evidence. As part of B2B supplier due diligence, require:
- Company profile and factory capacity statement with photographs of production lines and storage.
- A documented quality plan, including inspection points, FAI (first article inspection) procedures and corrective action process.
- Factory quality documentation: material certificates, traceability lists, torque and tensile test records at batch level where applicable, and non-conformance logs.
- Sample assemblies or prototype panels for mechanical fit checking with the actual module frames.
- FAT (factory acceptance test) plan and witness protocols; identify what the factory will test, what buyers can witness and the acceptance criteria.
- Packing list and export packing coordination plan, including weight/volume per package, palletisation drawings, sea/air container packing orientation, and export document checklist. Coordinate packing to meet customs and carrier restraints; CBP guidance on import documentation provides an overview of required documents for U.S. imports [4].
- Shipping Incoterm explicitly stated (e.g., FCA, FOB, CIF) together with the delivery responsibility matrix. Refer to ICC Incoterms rules for contractual clarity [3].
- Lead time confirmation and guaranteed ship date windows, with holdback or liquidated damages clauses where appropriate.
- A spares and consumables list (recommended per MW or per site) with price and lead time commitments.
- Warranty and remedies: clear definition of which party is responsible for what warranty items; specify warranty claim process and expected response times.
Typical procurement evidence requests mapped to decision points:
| Evidence item | Why it matters | Decision outcome |
|---|---|---|
| Factory quality documentation | Confirms material traceability and inspection controls | Use to accept or reject supplier on technical grounds |
| Export packing coordination plan | Avoids damage and customs detentions | Reduces risk of import rejection and repacking delays |
| FAT plan with witness slots | Validates pre-shipment compliance | Reduce on-site rework; schedule witness to match PO milestones |
| Incoterm + DRM | Sets legal delivery and risk allocation | Quantify landed cost and responsibility for damage/loss |
Be explicit in the purchase order about which documents must be submitted before shipment release. Treat missing or incomplete factory quality documentation as a formal non-conformance.
Caveat: Do not substitute factory documentation for independent on-site verification where local regulations or utility interconnection requirements mandate independent testing or certified installers.
Delivery responsibility matrix (decision table)
A delivery responsibility matrix (DRM) assigns each element of the PV interface to the responsible party and clarifies acceptance criteria and handover evidence. Use the DRM as a contractual annex.
| Deliverable / Interface item | Carport manufacturer | Electrical contractor / EPC | Buyer / Owner | Acceptance evidence |
|---|---|---|---|---|
| Structural frame (columns, rails) | Manufacture & ship | N/A | Inspect on delivery | Mill certs; packing list; visual inspection |
| Module clamp assemblies | Supply & pre-fit where specified | Install modules | Witness if required | Torque records; sample fit report |
| Foundation anchor plates | Supply or provide anchor layout (specify) | Install per civil drawings | Structural engineer sign-off | Anchor bolt template; embedment report |
| DC cable entry knockouts / glands | Deliver in position | Make DC cable connections | Electrical test | Drilling/cutout records; IP rating evidence |
| Earthing lugs and bond points | Supply and attach | Bond to system ground | Electrical inspector | Bond continuity test report |
| Combiner box housing (if supplied) | Supply | Connect and commission | Witness | FAT report; wiring diagram |
| Export packing and shipping | Pack per packing plan | Coordinate receiving | Confirm receipt & damage check | Packing list; damage report |
| Documentation pack (O&M, drawings) | Provide | N/A | Verify completeness | Document transmittal and acceptance |
Note: The DRM must be cross-referenced with the Incoterm used in the contract. For example, transfer of risk under FOB vs DAP changes which party is responsible for insurance and transport to port of arrival [3]. For cross-border shipments, ensure export packing coordination explicitly addresses customs documentation requirements [4].
Site installation and operations: interface impacts on the critical path
How the PV interface is specified materially affects the site critical path:
- Pre-fit parts reduce on-site time: Where the carport manufacturer pre-fits clamps or pre-routes tray work, on-site labour is reduced but factory assembly needs accurate module dimensional data and module sample verification.
- Staged deliveries require careful export packing coordination and unloading plans: If the site lacks heavy lifting equipment, specify smaller skids and on-site handling equipment as part of the procurement plan.
- Integration with civil works: Anchor bolt templates and pile work must be coordinated early. Late changes to anchor positions are costly and delay commissioning.
- Commissioning handover: Decide whether the manufacturer will support first-commissioning onsite for mechanical fit and initial module string checks or remain a remote technical backstop.
- O&M access and spare parts: Clearly define which spare parts are retained on site, which are shipped on demand, and expected lead times for replacements.
Operations note: Require the supplier to provide a documented O&M manual that explicitly references the PV interface items and provides replacement part numbers, expected torque values for routine checks and recommended inspection intervals. This document should be part of the factory quality documentation and handed over at final acceptance.
Important compliance statement: Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Implementation risk: common failures and mitigations
Risk: Module-to-rail incompatibility
- Cause: Module frame profile varies from sample or the supplier uses a generic clamp.
- Mitigation: Require module-specific clamp drawings, provide module sample for fit check, and include a change-order mechanism for module substitution.
Risk: Missing cable entries at combiner/inverter housings
- Cause: Electrical layout changed after manufacturing; factory packing omitted glands.
- Mitigation: Freeze electrical routing before production; require an electrical drawing sign-off and include an export packing coordination checklist for cable glands.
Risk: Corrosion and finish failure in coastal/industrial sites
- Cause: Incorrect or unspecified galvanizing/paint class.
- Mitigation: Specify finish class and inspection criteria; require finish test records and refer to galvanizing best practices [1].
Risk: Customs/import delays due to documentation
- Cause: Missing or incomplete export paperwork, wrong HS codes, improper packing declaration.
- Mitigation: Include export packing coordination; require supplier to provide pre-alert document pack and coordinate with the buyer’s customs broker; reference customs documentation guidance [4].
Risk: Ambiguous delivery terms leading to cost disputes
- Cause: Incoterm not specified or misinterpreted.
- Mitigation: State Incoterm in the contract and combine with the delivery responsibility matrix. Reference ICC Incoterms guidance [3].
Risk: Factory quality variation between production lots
- Cause: Lack of batch-level traceability or inconsistent inspection.
- Mitigation: Require factory quality documentation, material certificates and batch traceability as part of B2B supplier due diligence. Encourage an initial FAI and periodic audits.
Risk: Lead-time slippage
- Cause: Poor production planning, material shortages, or shipping delays.
- Mitigation: Require a confirmed production schedule with milestone deliverables, material long-lead item lists and contingency plans. Agree penalties or expedited options as part of procurement controls.
Project procurement controls and change management: Embed a formal change management workflow in the contract that defines how scope changes are priced and scheduled. This reduces dispute risk and gives all parties a predictable process for modifications.
Procurement checklist: B2B supplier due diligence essentials
Below is a practical checklist to include with RFPs or RFQs to ensure a consistent B2B supplier due diligence process. Require evidence for each checked item.
- Company legal registration and financial standing documents (as allowed by procurement policy).
- Factory capacity statement and single-line production flow.
- References for comparable projects (provided as client contact details where allowed).
- Factory quality documentation and inspection plans.
- Material certificates (steel grade, fastener grade).
- Welding procedures (if relevant) and qualified welder lists.
- Pre-shipment sample or prototype approval process.
- FAT plan with witness options and acceptance criteria.
- Export packing coordination plan and packing drawings.
- Incoterm and transit insurance responsibilities.
- Lead time commitments and backlog disclosure.
- Warranty terms and suggested warranty claim process.
- Spare parts list and recommended on-site spares.
Wherever possible, verify submitted documents with independent checks: visit the factory, request photos or videos of manufacturing steps, and where regulatory requirements exist, require local third-party test houses for proofs (e.g., bolt tensile tests or coating thickness).
Six-step buyer workflow: repeatable procurement process for the PV interface
A named, repeatable workflow compresses risk and makes tender outcomes comparable. Use this six-step buyer workflow in projects:
- Define the Project Basis (Design Freeze)
- Output: Version-controlled Basis of Design, module list, inverter/combiners, soil report, permit constraints.
- Action: Gather site survey, structural criteria and module geometry; circulate for stakeholder sign-off.
- Create the Interface Specification Package
- Output: Contract annex detailing mechanical & electrical PV interface, acceptance criteria, DRM and packing requirements.
- Action: Draft explicit interface drawings, connector types, clamp envelopes and handover points.
- Pre-qualify Suppliers and Conduct B2B supplier due diligence
- Output: Shortlist based on capacity, QMS evidence and references.
- Action: Request factory evidence, site photos, FAT plans and past project documentation.
- Issue Tender with Technical Scope Comparison requirements
- Output: Comparative matrix populated by bidders.
- Action: Require standardized response format so bids can be assessed apples-to-apples for scope, price and lead time. Use the technical scope comparison table below during evaluation.
- Contract, FAT, and Export Packing Coordination
- Output: Signed purchase order with DRM, FAT schedule and packing plan.
- Action: Schedule FAT, require factory quality documentation and pre-shipment approval for packing; confirm Incoterm.
- Delivery, Site Acceptance, Commissioning and O&M Handover
- Output: Accepted deliverables, commissioning report and O&M manual.
- Action: Verify packing condition on arrival, perform mechanical fit checks, electrical continuity and bonding tests, and complete handover package.
Each step should have named owners and deliverable dates and should be integrated into your project procurement controls master schedule.
Technical scope comparison (decision table)
Use this table to compare levels of supplier responsibility in the tender evaluation. Populate with supplier responses and score for cost-risk trade-offs.
| Scope item | Minimal (lowest CAPEX) | Recommended (balanced) | Comprehensive (turnkey) |
|---|---|---|---|
| Module clamp supply | Provide generic clamps, buyer verifies fit on-site | Provide module-specific clamps; prototype fit included | Supply pre-fitted modules/clamps and torque records |
| Rail & pre-assembly | Deliver rails cut to length | Deliver rails, partially assembled with mid-rail braces | Deliver rail assemblies pre-assembled and protected for direct installation |
| Cable management | Provide basic trays; no pre-routing | Provide trays and pre-cut cable entry points | Provide full tray runs pre-installed with cutouts and gland plates |
| Combiner/inverter housing | Supply housing only | Supply housing and mounting brackets | Supply pre-installed combiner housings and wiring stubs |
| Factory testing | Visual checks only | Dimensional checks and torque test | Full FAT with electrical continuity, bonding and witness options |
| Export packing | Standard pallet packing | Pallet packing + protective crating | Custom crate packing per component + export packing coordination |
| Warranty service | Standard manufacturer warranty | Manufacturer warranty + response SLA | Extended warranty with defined spares kit and on-call support |
Score bids not only on CAPEX but on total cost-to-complete: consider installation time, expected rework, customs handling and warranty remedy logistics.
Mid-article CTA
Need a project-specific interface review or an evidence pack for tendering? Start an inquiry: /inquiry. Also review our recommended system options here: SolarGrid commercial solar system and see all systems for broader options; refer to our sourcing guides for procurement templates.
FAQ — short answers to common procurement and interface questions
Q: What exactly is the "handover point" for DC cables? A: The handover point is the agreed physical location where pre-assembled DC cable tails or module string cables are connected to the EPC’s system—this must be specified as a connector type, gland size and IP rating.
Q: Who must provide combiner enclosures? A: This depends on the contractual DRM. Suppliers can provide housings (then they must meet IP and mounting criteria) or the EPC can supply and mount them. State this explicitly in the PO and inspection criteria.
Q: How do I manage module substitutions mid-project? A: Insist on a formal substitution clause: require the new module supplier to provide gap reports against the original interface dimensions and permit the manufacturer to rework clamps or rails within a defined change order mechanism.
Q: Are factory weld records and material certificates necessary? A: Yes—factory quality documentation that includes weld procedures, welder qualifications and mill/test certificates is essential for structural components and should be part of pre-award due diligence.
Q: How should we handle Incoterms and insurance? A: Specify the Incoterm in the contract and match it with the DRM. For overseas shipments, consider FCA or FOB if you control the sea freight, or CIF/DAP if you require the supplier to arrange carriage to site; consult ICC Incoterms for exact risk transfer rules [3].
Q: What documentation do customs authorities usually require on arrival? A: At a minimum: commercial invoice, packing list, bill of lading/air waybill, certificates of origin and any material-specific test certificates or licences. Coordinate the packing plan with customs brokers early [4].
Conclusion — balancing cost, schedule and technical certainty
Specifying a robust solar carport manufacturer PV interface is not a technical nicety — it is the procurement mechanism that translates design into deliverable outcomes. Successful B2B procurement balances three axes: clarity of scope (technical and contractual), verified manufacturing evidence (factory quality documentation and FATs), and logistical certainty (export packing coordination and explicit delivery responsibility matrix). Use a documented project basis, require evidence for claims through B2B supplier due diligence, and build decision tools (technical scope comparison and DRM) into the contract. That approach reduces disputes, accelerates commissioning and preserves warranty value.
If you want Carportiva to review your interface package or provide a supplier evidence pack tailored to your procurement schedule, contact our team: info@carportiva.com. For product options, see SolarGrid commercial solar system, explore all systems or review our sourcing guides.
Note: This guide is intended to support procurement decisions. Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
References
- American Galvanizers Association: guidance on galvanizing practice and inspection.
- International Organization for Standardization (ISO): quality management system principles and standards.
- International Chamber of Commerce Incoterms: rules for international trade and risk transfer.
- U.S. Customs and Border Protection: basic import/export documentation guidance.
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion