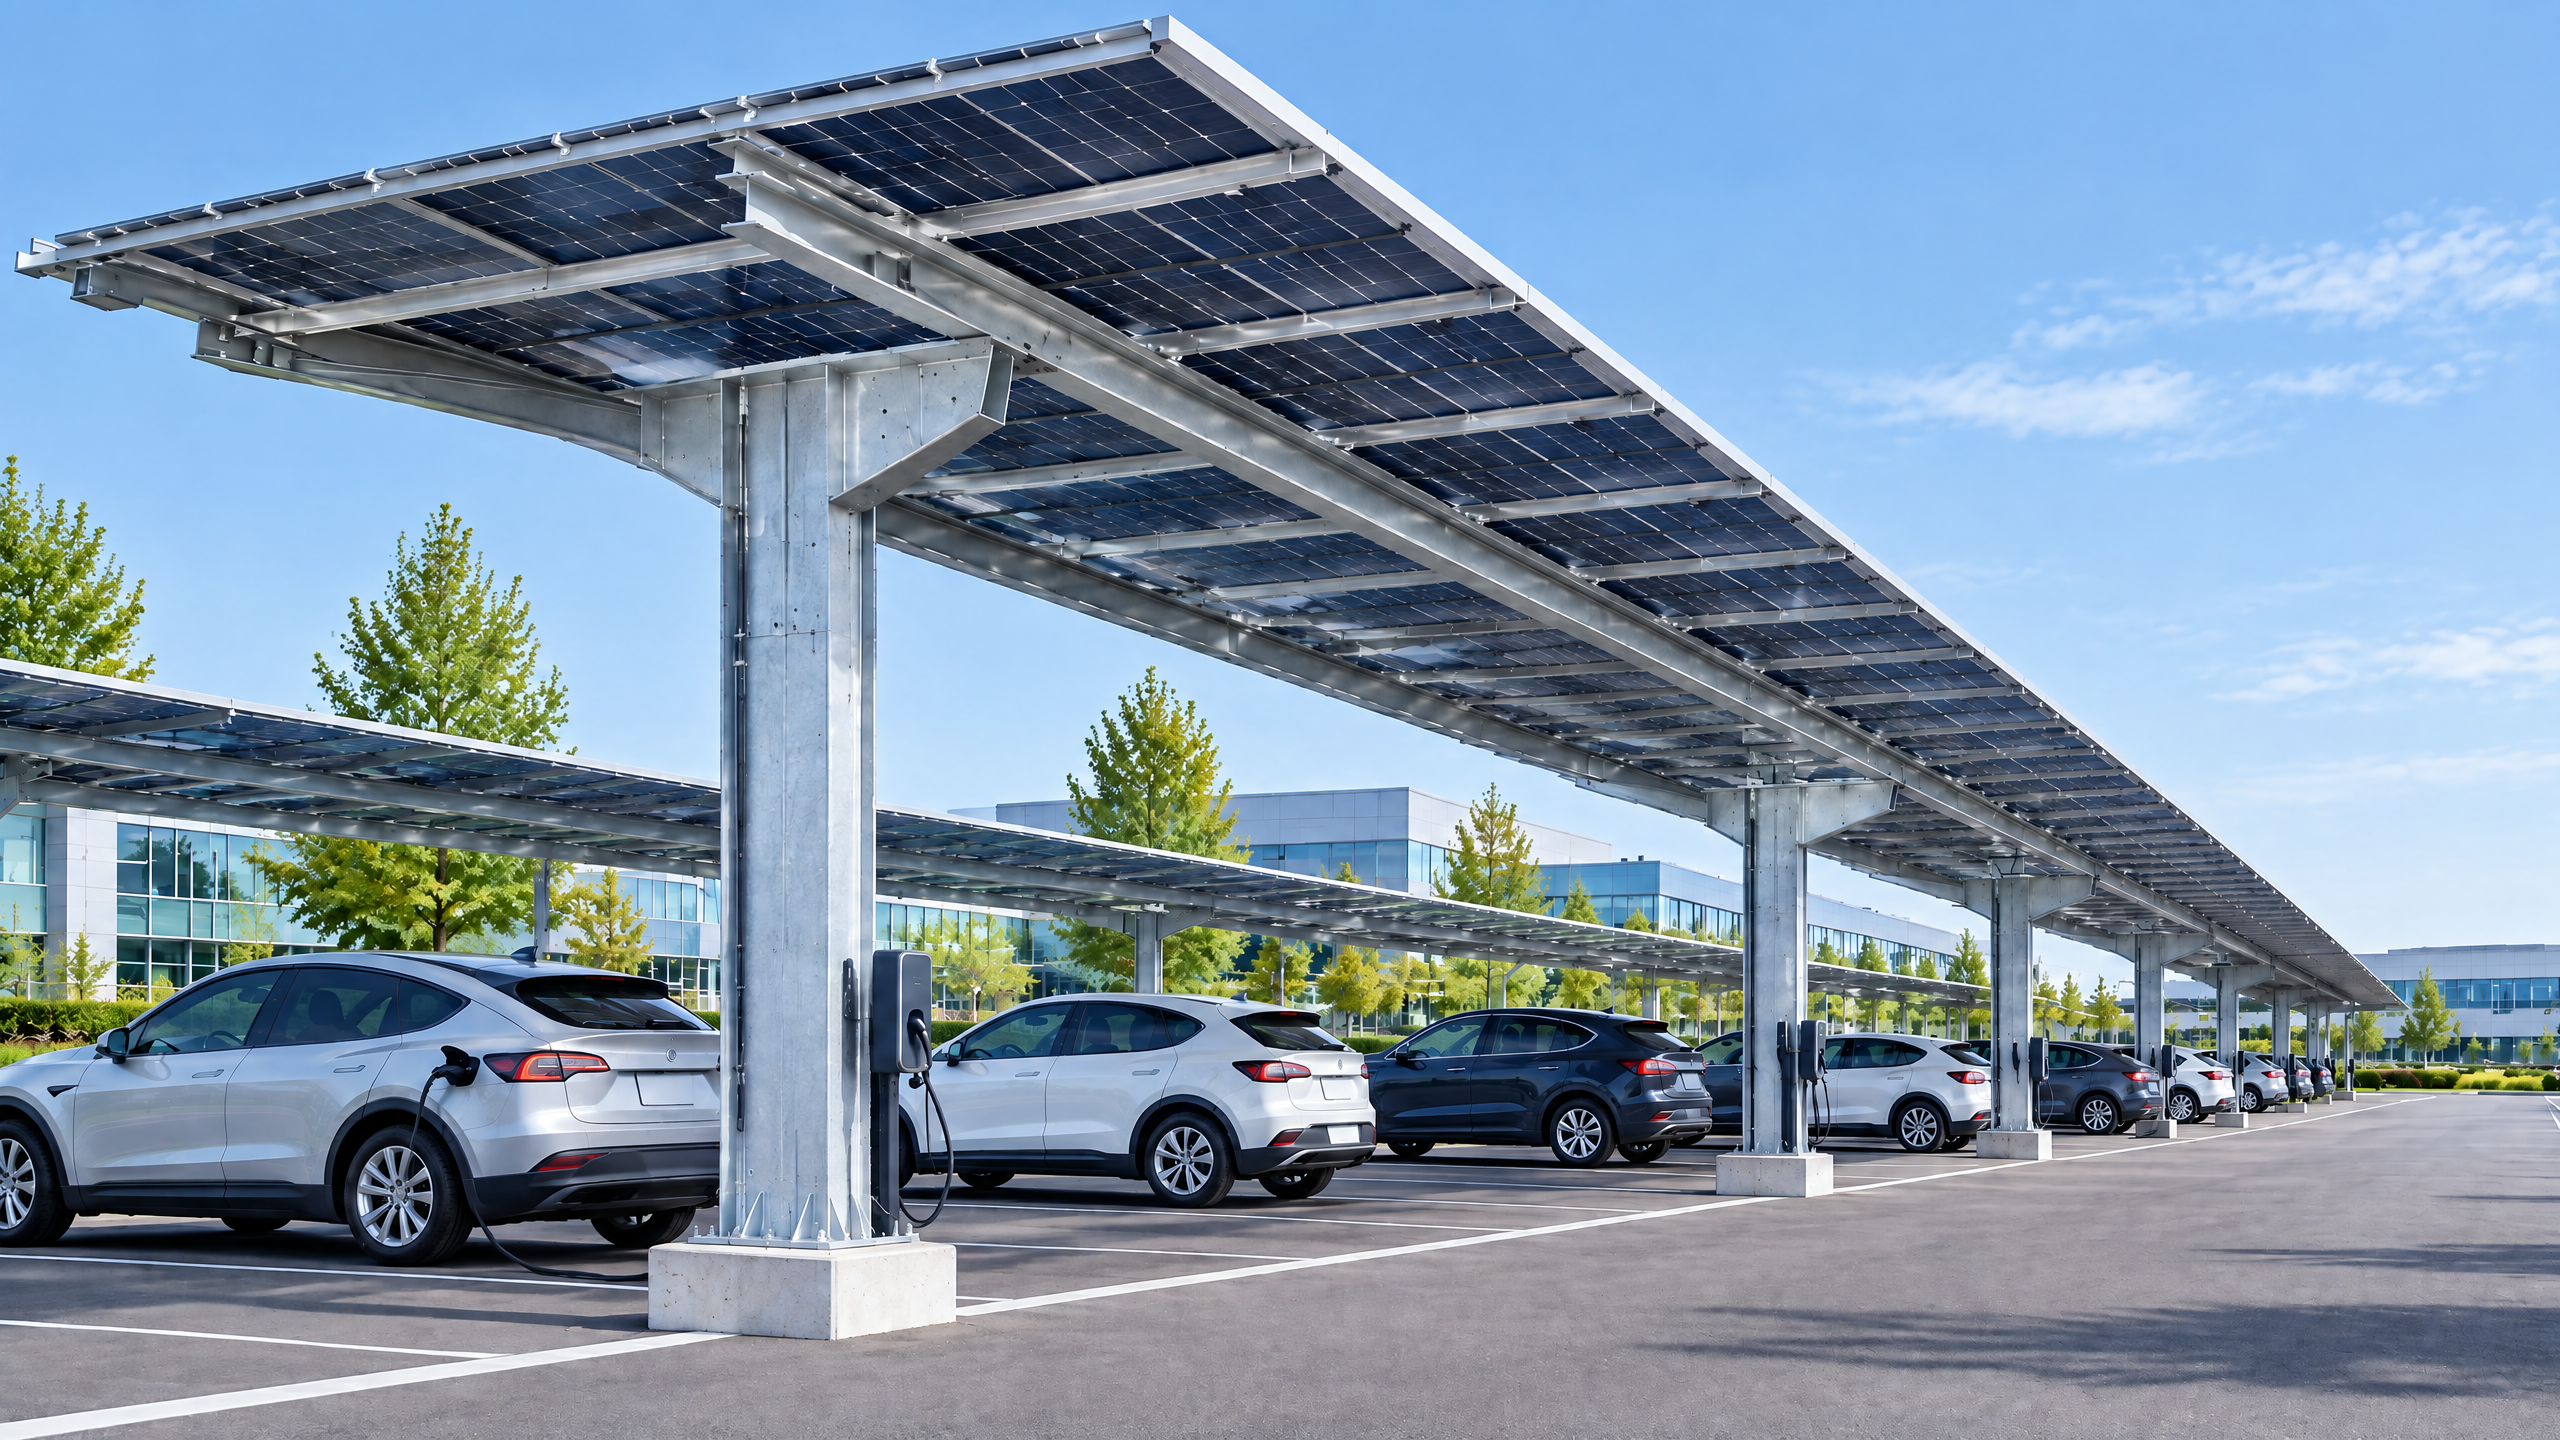
Supplier evaluation matters at every decision point in a B2B aluminium carport procurement, but its intensity and evidence requirements should scale to project complexity, contractual risk and the role the supplier plays in delivery. For single-site, low-value canopy purchases a basic check of manufacturing capability, financial stability and lead time may be sufficient; for multi-site rollouts, commercial solar carport programs, or projects with integrated electrical systems (PV, EV charging, site power), a structured aluminium carport manufacturer supplier evaluation is essential. The evaluation determines whether the manufacturer can meet technical scope, produce consistent factory quality documentation, coordinate export packing and logistics, accept defined delivery responsibilities, and operate within the buyer’s project procurement controls. This guide explains when and how to apply that evaluation rigor, what evidence to require, how to compare options technically and commercially, and how to translate supplier evidence into contract and implementation controls for a successful procurement and delivery lifecycle.
Buyer context and scope boundary: who needs deep supplier evaluation?
Why classify procurement scope?
- Buyers must match due diligence depth to contractual exposure. Distributors, architects, contractors, developers, solar EPCs and fleet operators will have different liabilities and operational dependencies on the carport supplier.
- If the aluminium carport includes integrated electrical systems such as PV or EV charging, risk moves from pure structural supply to multi-trade integration and ongoing performance; that raises the required evaluation standard.
Which buyer groups typically require full evaluation?
- Solar EPCs and developers procuring commercial solar carports (system-level responsibility) — full manufacturer verification plus integration evidence.
- Multi-site rollouts managed by a distributor or contractor — supplier capacity, repeatability and supply chain resilience need verification.
- Architects and contractors responsible for site approvals or installations — proof of design detail, interface control and site documentation is necessary.
- Fleet operators and facility managers procuring bespoke fleet shelters with operational warranties — evidence of long-term durability and serviceability is important.
Scope boundaries to define before evaluation
- Product-only supply vs. supply-and-installation contract.
- Whether the supplier is responsible for integrated systems (PV, electrical, canopy finishes).
- Expected delivery terms (EXW, FOB, CIF, DDP) and who manages customs, duties and local handling.
- Warranty coverage, spare parts availability, and service SLAs.
Clear scope definition reduces ambiguity in aluminium carport manufacturer supplier evaluation and helps select the correct evidence package for procurement review.
Core decision principle: evaluate to control the three delivery levers
Three delivery levers underpin buyer decisions:
- Technical fit — can the supplier meet the defined performance and interface requirements?
- Operability — can the supplier deliver repeatable factory quality and manage logistics to meet schedule?
- Contractual risk allocation — are responsibilities and liabilities clear and enforceable?
Use these levers to decide the level of supplier scrutiny. For example, if technical fit is high risk (complex foundations, integrated PV) and the supplier will control logistics to site, both technical and commercial evidence must be comprehensive. If operability and contractual exposure are low, a lighter evaluation may suffice.
This is the core control: increase evidence and contractual granularity proportionally to technical complexity, commercial exposure and geographic or regulatory risk.
Planning inputs: what you must define before evaluating suppliers
Before you request documentation or score suppliers, capture a documented project basis covering:
- Project brief: capacity (number of carports), site locations, intended use (parking, solar generation, fleet), design life.
- Schedule and key milestones: procurement window, factory lead time, shipment windows, on-site installation dates.
- Budget envelope and payment profile.
- Primary interface responsibilities: who provides foundations, electrical connections and commissioning?
- Regulatory constraints: permit timelines, local loading codes, wind and snow exposure classifications (require local engineer confirmation).
- Acceptance criteria: dimensional tolerances, coating performance, electrical commissioning criteria for PV/EV systems.
Essential planning rule: Do not start supplier scoring without a documented project basis. This ensures evaluation is evidence-led and comparable across bidders.
Note: Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Technical specification and interface control: what to compare and why
A robust technical comparison aligns supplier proposals to the same baseline and prevents scope creep. Start with a technical scope comparison matrix that forces each bidder to state compliance, deviation and build detail.
Key technical items to require:
- Structural design data: section sizes, alloy grade (e.g., aluminium series), wall thicknesses, connection details and anchor loads.
- Corrosion protection: coating system, anodizing details, or specified hot-dip galvanizing of steel components (for mixed-material connections). Reference corrosion guidance in procurement and inspection plans [1].
- Load ratings and design codes applied (buyer must request copies of calculation basis and the referenced local standard; do not accept “meets code” without the calculation).
- Tolerances and dimensional drawings: fabrication shop drawings and as-built interfaces for modules, rails and canopies.
- Electrical interfaces (if applicable): PV racking integration, DC/AC equipment mounting, wiring containment, junction box locations, inverter/transformer foundations and earthing/grounding provisions.
- Site interfaces: anchor types, required foundation drawings, and utility connection points.
- Transport and packing constraints: maximum piece size, on-site handling limitations, and export packing coordination.
Technical scope comparison (sample)
| Requirement | Buyer baseline | Supplier A response | Supplier B response | Notes |
|---|---|---|---|---|
| Canopy span | 6.0 m | Complies; alum. extrusions 6061-T6 | Deviates: 5.5 m span with additional mid-support | Supplier B proposes added supports; impacts site works |
| PV racking interface | Module clamp zone and rail spacing | Factory pre-drilled rails; clamps supplied | Rails supplied; clamps by local installer | Clarify responsibility for module electrical bonding |
| Anchor loads | To be provided by buyer engineer | Provides anchor load envelope | Requires site-specific soil report | Supplier B conditions tender on soil report |
Technical comparison forces clarity on scope, deviations and who performs the remedial work.
Procurement and factory evidence: what to ask for, what to accept
Aluminium carport manufacturer supplier evaluation must include documentary evidence from the factory and supply chain. The evidence should be verifiable, specific to the proposed scope and recent.
Essential evidence categories:
- Corporate and financial: company registration, years in operation, audited financial statements or bank references where relevant for risk assessment.
- Production capacity and process: factory layout, production lines for aluminium extrusion, punching and assembly, finishing (anodizing or powder coating) and dedicated assembly areas for PV integration.
- Quality management: factory quality documentation including inspection and test plans (ITPs), non-conforming material procedures, batch traceability and final inspection reports. Reference applicable ISO standards for quality management expectations [2].
- Material test documents: mill certificates for aluminium alloys, supplier traceability for fasteners and structural connectors.
- Welding and joint procedures: welding procedure specifications (WPS) and welder qualification records where applicable.
- Pre-shipment inspection and packing: photographs of previous shipments, description of export packing coordination and export crate specifications, marking and lifting points.
- Logistics and delivery: typical lead times, shipping routes, export documentation capability and customs experience.
- References and visit access: client references for similar projects and willingness to allow factory inspections or third-party audits.
Factory evidence decision table (acceptance criteria)
| Document type | Minimum acceptable evidence | Verification method |
|---|---|---|
| Factory quality documentation | Written ITP and QC plan specific to project or product family | Factory audit or third-party review of documents and sample records |
| Material certificates | Mill test certificates traceable to part numbers/batches | Cross-check against supplier material records and third-party lab testing when required |
| Export packing coordination | Packing list template, crate specifications, lifting drawings, and handling instructions | Review of previous shipping photos and sample crate; mock-up approval for special items |
| Delivery responsibility matrix | Supplier stated Incoterms and responsibilities for each milestone | Contract clause referencing chosen Incoterm and proof of carrier/insurer arrangements |
When is third-party inspection warranted?
- High-value projects, projects with integrated PV where electrical safety is essential, multi-site rollouts, and when onsite access to factory is limited. Use a qualified inspection house to validate factory quality documentation and sample production.
On export and delivery: align documentation to Incoterms and customs practice
- Define the delivery responsibility matrix in contract terms and use recognized Incoterms to avoid ambiguity [3]. For customs and import readiness, verify the supplier’s export documentation practices and familiarity with destination customs (for U.S. imports, CBP guidance should be followed) [4].
Do not accept generic statements. Insist on project-specific factory quality documentation and traceable records.
Mid-article CTA If you need a supplier evaluation checklist or bespoke procurement scope review for a carport or commercial solar carport, contact our team at /inquiry or email info@carportiva.com. For integrated systems see our SolarGrid commercial solar system and for system choices visit all systems and our sourcing guides.
Site installation and operations: translating factory evidence into site success
Factory capability is necessary but not sufficient. Successful on-site delivery depends on interface control, installation planning, and operations readiness.
Site installation proof points to require:
- Installation method statements: step-by-step procedures including lifting plans, installation tolerances, temporary bracing and sequencing.
- Foundation and anchor details: foundation drawings and anchor bolt templates aligned to supplier anchor load data. If the supplier is not responsible for foundations, require anchor load envelopes and embedment tolerances.
- Erection drawings and crane/lift requirements: maximum lift weights and required on-site equipment.
- Electrical handover documentation (if PV or EV charging included): as-built wiring diagrams, earth continuity tests, inverter commissioning reports, and operator manuals.
- Spare parts and repair kits: recommended spare parts list and lead times for replacement extrusions, brackets and specialized fasteners.
- Maintenance schedule and expected interventions: frequency of inspections, recommended cleaning for coatings and PV modules, and procedures for coating repair.
Operational handover and training
- Supplier should provide training materials, on-site training sessions for the installer/maintenance team and clear escalation paths for warranty or post-delivery support.
Operational readiness decision table (site handover)
| Handover item | Minimum deliverable | Acceptance criterion |
|---|---|---|
| Installation records | As-built drawings and installation sign-off by installer | Signed handover certificate with photographic evidence |
| Electrical commissioning | Test certificates for PV/inverter and earth leakage tests | Commissioning report signed by qualified electrician and supplier rep |
| Spare parts | List of critical spares with supplier lead times | Procurement plan for spares aligned to project lifecycle |
Remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Implementation risk: common failure modes and mitigations
Identify common causes of delay, cost overrun or performance shortfall and how supplier evaluation reduces them.
- Scope ambiguity leading to rework
- Detection: supplier bids with differing assumptions on anchors, PV interface, or finish.
- Mitigation: insist on a technical scope comparison and require the supplier to mark deviations in writing.
- Factory quality inconsistent with drawings
- Detection: missing traceability, incomplete ITP, or non-project-specific QC documentation.
- Mitigation: require factory quality documentation, sample inspections and third-party audits for repeatable production.
- Logistics and packing failures
- Detection: damaged items on arrival, lack of proper lifting points or oversized components not cleared for transport.
- Mitigation: require export packing coordination documentation and a pre-shipment sample pack approval.
- Delivery responsibility confusion
- Detection: disputed responsibility for damage in transit or customs hold-ups.
- Mitigation: define a delivery responsibility matrix in contract terms referencing Incoterms and specify milestones for handover and insurance [3].
- Site installation mismatch
- Detection: foundation anchors do not align with factory-drilled plates or erection sequence causes delays.
- Mitigation: require anchor templates, erection drawings and, if needed, early site visits or 3D coordination.
- Warranty and long-term support gaps
- Detection: supplier cannot provide spare parts in a timely manner or declines certain warranty claims.
- Mitigation: include contractual service levels, spare parts obligations and escalation procedures in procurement documents.
Use contractual levers (acceptance tests, holdbacks, milestone payments tied to deliverables) combined with evidence-led supplier evaluation to mitigate these risks.
A six-step buyer workflow for aluminium carport manufacturer supplier evaluation
This named workflow is actionable and repeatable for B2B buyers. Follow it as a minimum for medium-risk procurements; scale up verification for high-risk or multi-site projects.
- Define the documented project basis
- Deliverable: Project brief, technical baseline, schedule, constraints and acceptance criteria.
- Purpose: Creates the common yardstick for all supplier responses.
- Issue technical RFQ with mandatory evidence list
- Deliverable: RFQ specifying technical scope comparison template, required factory quality documentation, material certificates and expected Incoterms.
- Purpose: Forces suppliers to provide comparable technical and documentation packages.
- Shortlist and perform due diligence
- Deliverable: Completed B2B supplier due diligence checklist covering corporate, financial and production capability, plus reference checks.
- Purpose: Removes suppliers with unacceptable commercial or capacity risk.
- Technical reconciliation and factory verification
- Deliverable: Completed technical scope comparison, factory quality documentation review and, where needed, third-party inspection or factory visit.
- Purpose: Verifies factual compliance and identifies deviations.
- Contract allocation of risk and delivery responsibilities
- Deliverable: Contract with delivery responsibility matrix, Inspections / acceptance tests, warranties, milestone payments and penalties.
- Purpose: Makes responsibilities explicit and enforceable (reference Incoterms) [3].
- Pre-shipment inspection, logistics coordination and site readiness
- Deliverable: Pre-shipment inspection report, export packing coordination sign-off, shipment schedule and site installation plan with foundation verification.
- Purpose: Ensures a clean handover to site and reduces rework and delays.
This workflow integrates technical and commercial checks; it is the practical embodiment of project procurement controls and should be part of any procurement SOP.
Procurement controls and contract clauses to protect buyers
Translate supplier evaluation findings into contractual terms and procurement controls.
Contractual items to include:
- Delivery responsibility matrix (explicitly link to Incoterm): spells who is responsible at each point (manufacture, loading, export, import, on-site delivery) and who insures goods [3].
- Acceptance tests and hold points: define factory and site acceptance tests, criteria for acceptance and remedies for non-conformance.
- Documentation obligations: require factory quality documentation, material certificates, as-built drawings and spare parts list as preconditions for final payment.
- Warranty and post-delivery support: define warranty scope, exclusions and response SLAs. Also specify spare parts lead times.
- Change control process: define how technical deviations are managed and priced.
- Penalties and liquidated damages: where project critical dates exist, tie payments or LDs to delivery milestones.
- Audit rights: allow buyer or appointed third-party inspections at the factory with notice periods and cost allocation rules.
- Customs and export compliance: require supplier to provide accurate HS codes, packing lists and commercial invoices; reference customs guidance where relevant [4].
Contract language should convert supplier evidence into enforceable obligations. The delivery responsibility matrix should be a contractual annex so responsibilities cannot be misinterpreted.
FAQ: focused answers for procurement teams
Q: What is the single most important document to request during evaluation? A: There is no single magic document; however, a project-specific factory quality documentation package (ITP, material certificates and sample inspection reports) is the most direct evidence that the factory can manufacture to the buyer’s requirements.
Q: How do I choose Incoterms for an aluminium carport shipment? A: Choose based on who holds risk and manages customs. If the buyer wants minimal logistics burden, DDP places delivery risk on the seller; if the buyer prefers control of import operations, FOB or EXW may be better. Link the selection to your delivery responsibility matrix and verify supplier experience with the chosen Incoterm [3].
Q: Is a factory visit essential? A: Not always. A third-party inspection plus robust factory quality documentation may suffice for lower-risk projects. For high-value, complex or multi-site procurements, a factory visit or extended audit is strongly recommended.
Q: What evidence is required for integrated PV carports? A: In addition to structural documentation, require electrical drawings, inverter and module mounting details, PV racking interface documentation, commissioning procedures, and as-built electrical test reports. Also ensure installers are certified for electrical works in the destination jurisdiction.
Q: How should we evaluate packing and transport? A: Request export packing coordination details: packing lists, crate drawings, load restraint plans and photos of prior shipments. Evaluate whether parts can be moved with local site equipment. Poor packing is a frequent cause of site rejection.
Q: Can I rely on references alone? A: References are necessary but insufficient. Use them with documentary evidence, factory documentation and (when required) third‑party verification.
Decision support: two practical tables to use in procurement
Decision table 1 — When to escalate supplier evaluation
| Project characteristic | Low evaluation required | Medium evaluation | Full evaluation (mandatory) |
|---|---|---|---|
| Project value per site | < low budget threshold | Moderate | High or multi-site rollouts |
| Technical complexity | Simple canopy only | Some interfaces (e.g., PV rails) | Integrated systems (PV, EV), bespoke structural demands |
| Supplier role | Product only supply | Product + limited coordination | Product + logistics + installation or long-term service |
| Geographic factors | Local supplier, low customs complexity | Cross-border shipment, known customs | Long lead times, remote site, complex import rules |
| Regulatory exposure | Minor permits | Standard local permits | Critical structural approvals or energy/yield guarantees |
Decision table 2 — Minimum documentation checklist by procurement tier
| Document/record | Low tier | Medium tier | High tier |
|---|---|---|---|
| Technical scope response | Standard product sheet | Detailed shop drawings | Project-specific shop drawings and load calculations |
| Factory quality documentation | Basic QC statement | ITP + sample records | Full ITP + batch traceability + third-party audit |
| Material certificates | On-request | Mill certificates for main components | Mill certificates traceable to part numbers and weld records |
| Export packing coordination | Packing list | Packing drawings + photos | Packing drawings + mock-up approval + handling instructions |
| Delivery responsibility matrix | Basic Incoterm | Incoterm + delivery milestones | Detailed matrix with insurance, handover points and penalties |
Use these tables to set buying rules and to standardize what “pass” looks like at each procurement tier.
Final considerations and procurement checklist
- Ensure the technical scope comparison accompanies all bids and that suppliers explicitly note deviations.
- Require factory quality documentation proportionate to project risk; for critical components insist on traceability to mill certificates.
- Include export packing coordination and logistics plans early; unresolved packing often delays projects at the port.
- Establish a delivery responsibility matrix in the contract referencing Incoterms to avoid disputes over liability [3].
- Use project procurement controls to link payments to clearly defined milestones and documented deliverables.
- For packages involving international shipping, validate supplier experience with customs documentation and destination requirements; consult import authorities or resources as required [4].
- Do not rely solely on supplier claims; request verifiable evidence and, where doubt remains, third-party verification.
Remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Conclusion
Aluminium carport manufacturer supplier evaluation is not an optional procurement formality — it is the mechanism by which buyers turn supplier statements into enforceable, verifiable outcomes. The depth of that evaluation should be proportionate to the project’s technical complexity, contractual exposure and operational dependency on the supplier. Using structured technical scope comparison, demanding factory quality documentation, planning export packing coordination, and documenting a clear delivery responsibility matrix supported by contract clauses and project procurement controls will materially reduce schedule, cost and performance risk. For projects involving integrated PV or system-level delivery, align supplier evaluation with electrical and commissioning evidence, and follow up with pre-shipment inspection and site readiness checks.
For tailored procurement support or to discuss supplier evaluation for commercial solar carports and other systems, contact us at /inquiry or email info@carportiva.com. For product-level information see SolarGrid commercial solar system, review all systems, and consult our sourcing guides.
Acknowledgements and references for further reading:
- For metal coating and corrosion guidance consult the resources of the American Galvanizers Association [1].
- For quality management frameworks consider relevant ISO standards and guidance [2].
- For contractual delivery risk allocation and the meaning of delivery terms see Incoterms guidance [3].
- For U.S. import documentation and basic customs guidance consult official CBP resources [4].
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion