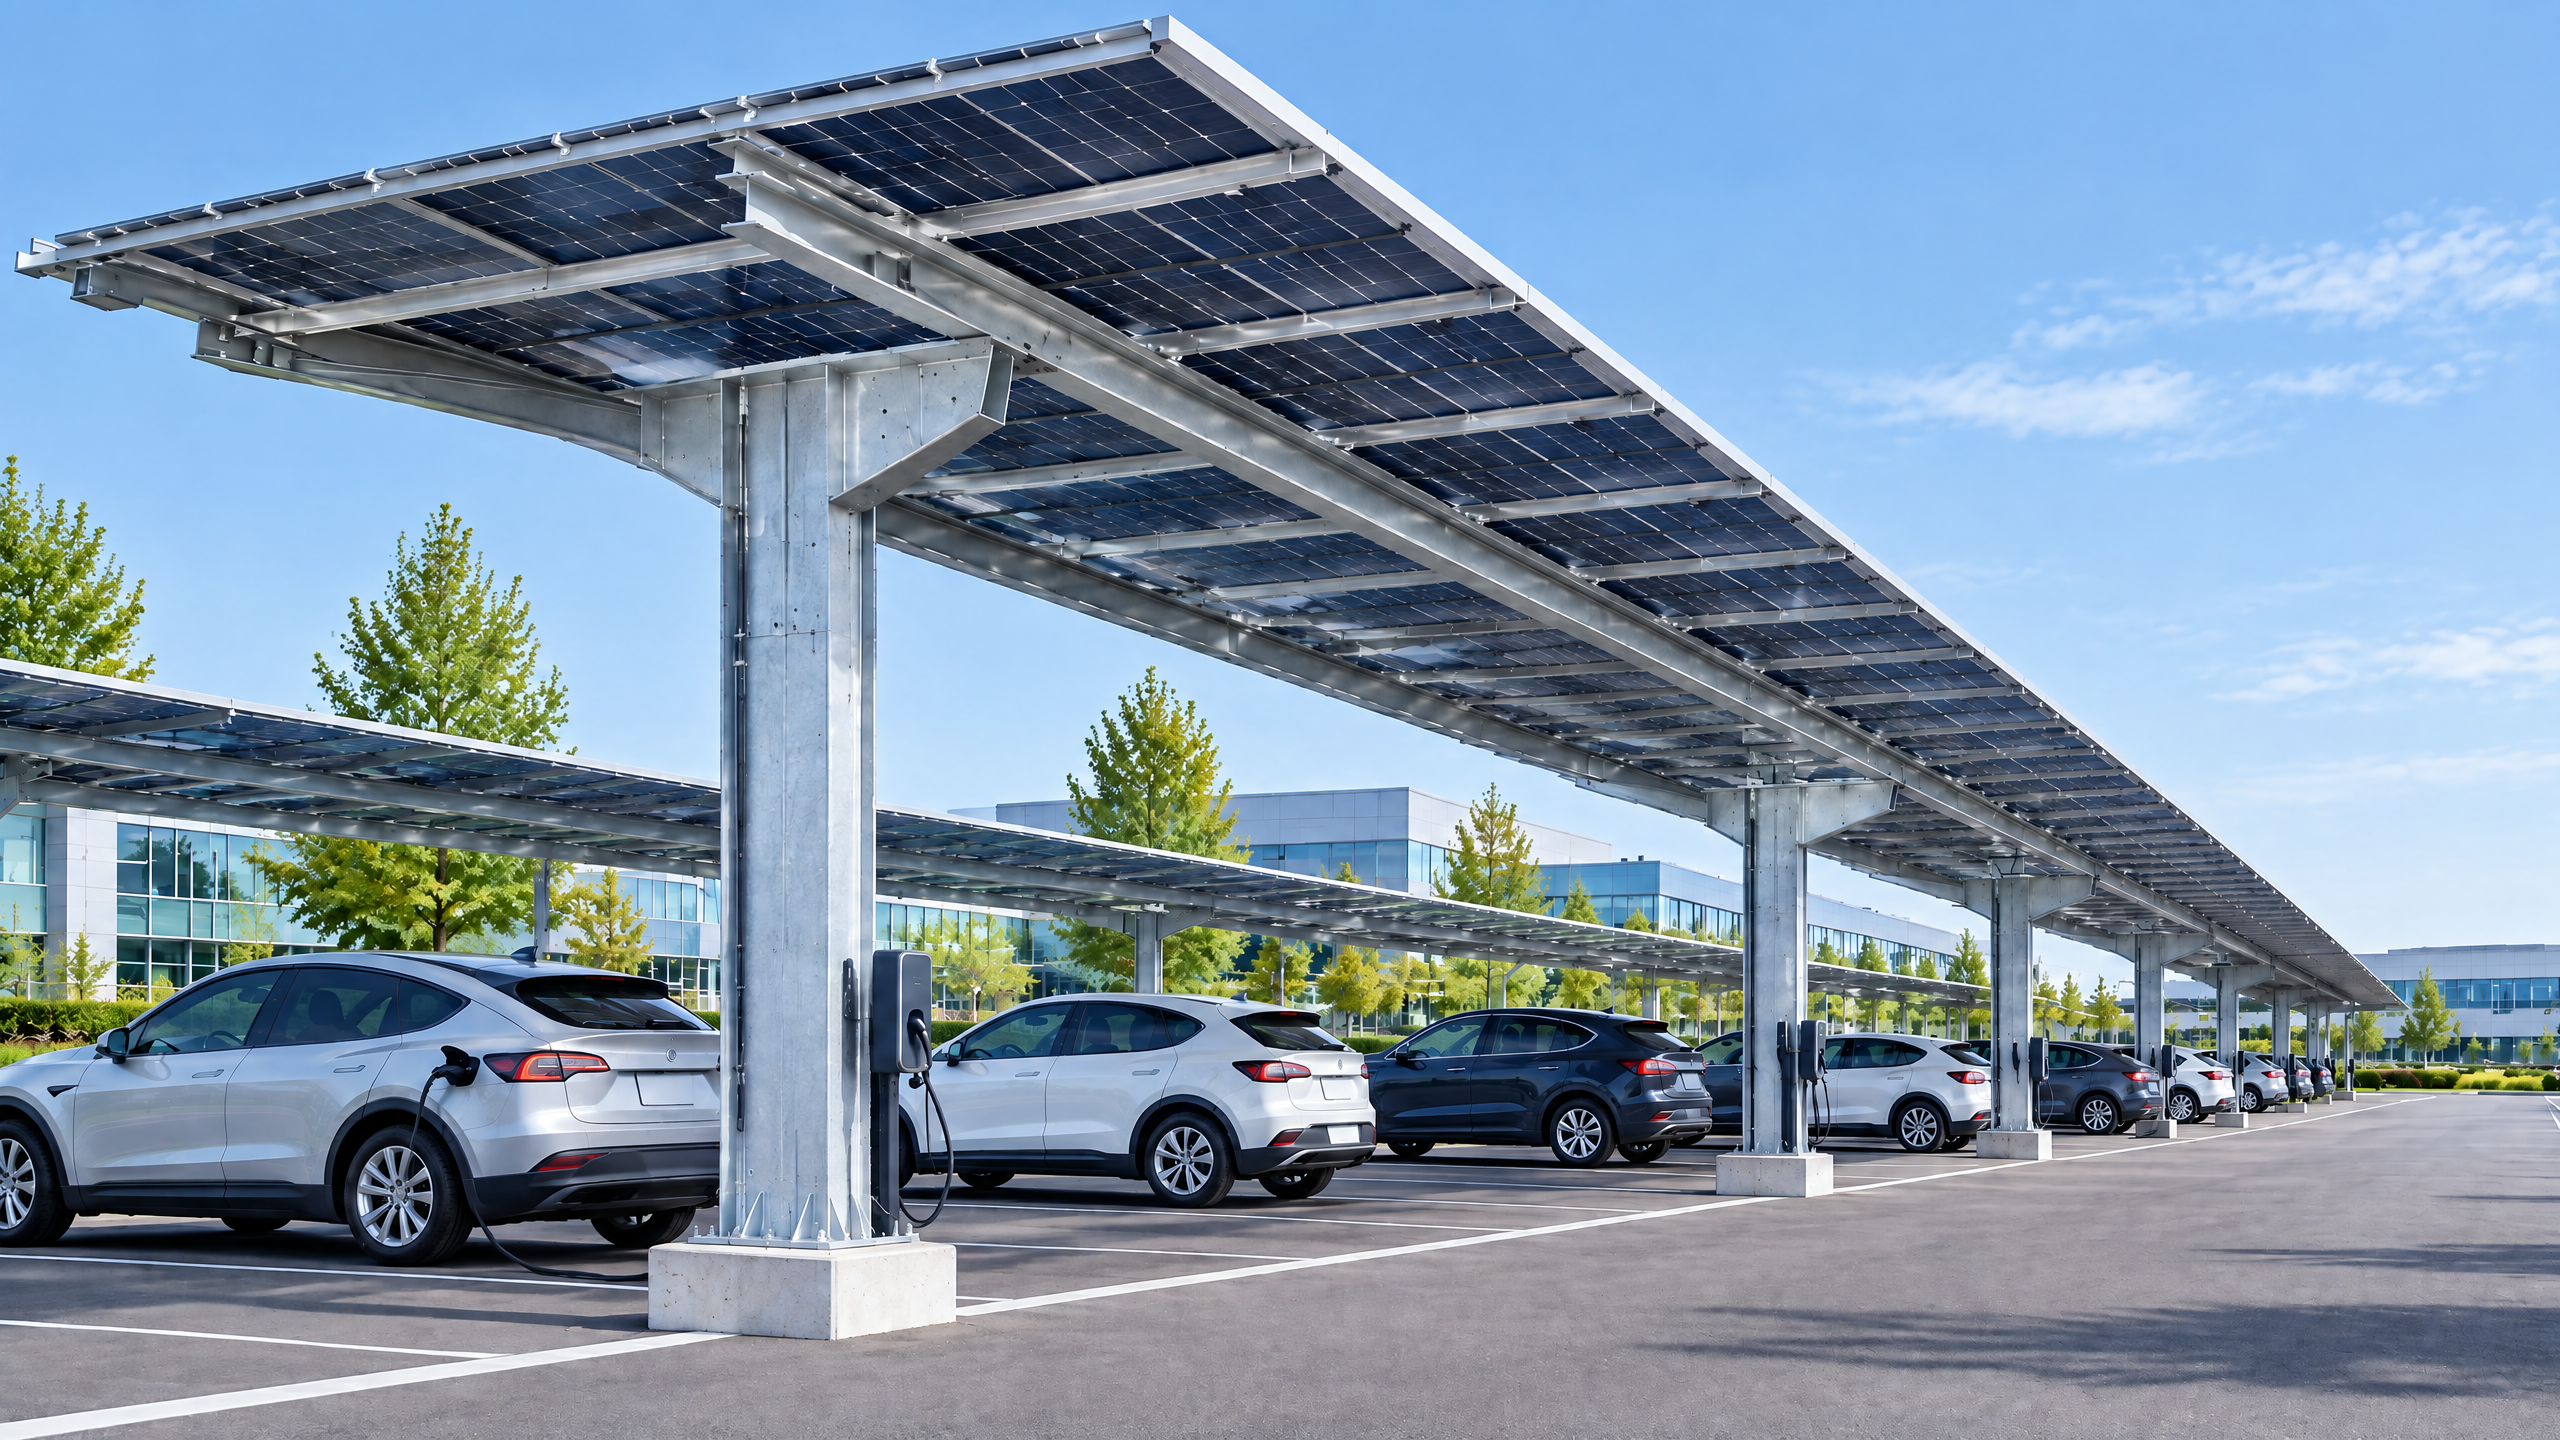
Answer (short): Evaluating solar carport manufacturer factory capability requires a structured, evidence-led review of how a supplier translates technical design into repeatable, auditable product and logistics outcomes. Focus first on scope clarity — what loadings, finishes, module interfaces, and site conditions the carport must meet — then assess the factory through documentary evidence (quality systems, material traceability, weld and coating records), on-site verification (audits, photos, witness tests) and commercial controls (delivery responsibility matrix, export packing coordination, clear Incoterms). Combine this with B2B supplier due diligence, a technical scope comparison between bids, and contract clauses that enforce project procurement controls. Always test assumptions with a prototype or pilot batch, and confirm that site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty are confirmed on a documented project basis with the relevant local qualified professionals, installers, utilities and authorities.
Buyer context and scope boundary
Why scope matters
- Solar carports are a systems product: architectural aluminium structure, solar modules, racking, electrical balance-of-system (BOS), foundations and attachments. The factory capability review should map to the exact technical and contractual scope you intend to buy.
- Ambiguity in scope creates downstream defects, delays and change orders. Define what the supplier is responsible for and what remains with the buyer, contractor or EPC.
Key scope items to agree before factory evaluation
- Structural design basis: design standards, wind/snow/seismic load cases, design life.
- Finish and corrosion protection: coatings, anodizing or hot-dip galvanizing and any local durability requirements.
- Module interface: frame dimensions, clamping method, electrical combiner/power block mounting.
- Foundations: embedded anchors vs. baseplates, soil-bearing assumptions.
- Logistics and delivery: packaging, partial shipments, on-site handling constraints.
- Warranty and spares: what parts are covered and delivery expectations.
- Acceptance criteria: inspection tests, dimensional tolerances, surface quality.
Scope boundary exercise (practical step)
- Create a short Scope Matrix mapping each system element to the responsible party (Buyer / Supplier / Installer / Other). This matrix becomes a baseline for the factory audit and the delivery responsibility matrix in the contract.
Core decision principle: capability as outcome, not promise
What “factory capability” really means
- Capability is demonstrated by consistent, auditable outputs: repeatable fabrication to specification, traceable materials, documented QA/QC, timely and protected shipment, and predictable handling of non-conformance.
- Verbal assurances or marketing materials are insufficient. Prioritize documents, observable process controls and prior process evidence (e.g., inspection records for similar systems, factory measurement logs).
Three evaluation lenses
- Technical fidelity — can the factory produce the geometry, tolerances and finishes required?
- Quality assurance — are there systems to prevent, detect and correct defects?
- Commercial delivery — can the supplier reliably pack, ship and deliver under the agreed terms and handle customs/logistics?
Decision rule for buyers
- Accept a supplier when technical fidelity + QA systems + commercial delivery controls meet the project’s risk tolerance and are contractually reinforced. When one dimension is weak, mitigate with proofs (pilot manufacture, hold points, bonds, staged acceptance).
Planning inputs: documents, stakeholders and baseline data
Essential documents to assemble before supplier engagement
- Project Basis of Design (BoD): loads, performance targets, site constraints.
- Site geotechnical report and structural capacity assumptions.
- Electrical single-line diagram and module/layout constraints.
- Local regulatory constraints: permits, fire egress, lighting, building code references.
- Procurement timeline and cashflow milestones.
Stakeholder map
- Internal: procurement, engineering, project manager, legal, finance.
- External: selected EPC/installer, local structural engineer, permitting authority, utility, insurer.
- Supplier-side: factory production manager, QA/QC lead, export logistics contact, technical lead.
Why documented baselines matter
- Factory tests and QA records are meaningful only when measured against a documented project basis. For example, welding acceptance criteria must reference applicable design standards; packing lists must match a defined shipment plan.
Practical planning checklist
- Confirm the BoD with engineering sign-off.
- Allocate responsibilities for onsite verification (who will witness deployment tests or acceptance).
- Set required lead-time windows and padding for customs clearance and on-site handling.
Technical specification and interfaces
Break the technical scope into clear, verifiable interfaces:
- Structural subsystem (aluminium extrusions, hot-rolled sections, connections).
- Corrosion protection and finishes (anodizing, powder coat, galvanizing where steel is used).
- PV module attachment and electrical BOS (rails, clamps, combiner boxes, cable gland interfaces).
- Foundations and anchors (embedded vs. post-installed anchors, torque requirements).
- Drainage, lighting and ancillaries (gutters, cabling trays, e-vehicle charging infrastructure readiness).
Key technical items to verify in the factory context
- Dimensional tolerances and fixture verification: ask for manufacturing drawings and shop fixture lists and confirm jigs/fixtures that maintain tolerance.
- Welding and joining procedures: obtain welding procedure specifications and welder qualification records where applicable.
- Surface treatment lines: confirm kiln/oven dimensions for powder coat, bath capacity and QA procedures for anodizing or galvanizing [1].
- Module interface templates: request CAD models or sample rails, and third-party module frame compatibility checks.
- Electrical assembly: factory-assembled combiner boxes and plug-and-play harnesses should have terminal diagrams, torque specs and dielectric/insulation test records.
Technical scope comparison
- Use a side-by-side technical scope comparison when evaluating multiple suppliers. A thorough technical scope comparison shows where suppliers include or exclude specific interfaces, which directly affects factory checks and on-site responsibility.
Example technical scope comparison table (Markdown)
| Technical element | Supplier A | Supplier B | Buyer baseline requirement |
|---|---|---|---|
| Structural sections: alloy & grade | 6061-T6 extrusions | 6005A extrusions | 6061-T6 or equivalent specified |
| Module mounting system | Clamps + rail, module frame up to 40 mm | Module-specific clamps only | Module-agnostic clamps preferred |
| Corrosion protection | Powder coat on pre-treated aluminium | Anodized only | Corrosion protection to local coastal spec |
| Pre-installed combiner boxes | Yes (factory wired) | No (on-site) | Factory-wired preferred where site access limited |
| Foundation anchors | Option: baseplates w/ anchor bolts | Embedded anchors only | Match site geotech & installer preference |
Note: populate the table using RFP responses.
Standards and references
- Specify applicable standards (ISO quality standards, structural codes, and PV-module interface norms) in the data sheet. Where general quality systems are claimed, expect supporting documentation (see Procurement/factory evidence).
Procurement and factory evidence
Core procurement aim
- Convert capability questions into verifiable evidence requirements in the RFQ and contract. This is the heart of B2B supplier due diligence.
Documentary evidence to request
- Factory quality documentation: quality manual, inspection plans, process control charts, traceability logs and NCM (non-conforming material) records. Use “factory quality documentation” as a mandatory deliverable in tendering.
- Material certificates: mill test reports (MTRs), alloy certifications and batch numbers.
- Coating and finish test records: thickness measurement logs, salt spray test reports where applicable.
- Welder qualifications and welding procedure specs.
- Manufacturing drawings, assembly drawings and bill of materials (BoM).
- Packing lists and export documentation templates required for customs (commercial invoice, packing list, certificates of origin). For guidance on export rules and import processes consult local authorities and general import guidance such as U.S. Customs and Border Protection for US ports of entry [4].
- Sample parts, prototype assemblies or full-scale mock-ups for critical joints.
Factory audits and on-site verification
- Types of audits: desktop document review, remote video walk-through, and on-site third-party audits. For high-value or high-risk projects favor on-site audits with sampling of production runs.
- Audit checklist topics: production flow, jigs and fixtures, QA stations, material storage, handling procedures, test equipment calibration, non-conformance handling, packing and staging area.
- Witnessing tests: dimensional checks, torque checks, load or proof tests for critical connections where practical.
Decision table — Factory evidence acceptance criteria
| Evidence type | Acceptable proof | Minimum buyer acceptance |
|---|---|---|
| Quality management system | ISO certificate or quality manual with records of practice | If no ISO certificate, detailed QA manual + 12 months of inspection records |
| Material traceability | MTRs with batch numbers tied to component receipts | MTR + factory traceability log linking MTR to part ID |
| Weld quality | WPS and welder qualification certificates | WPS + weld inspection reports for production parts |
| Coating | Coating procedure, thickness measurements | Procedure + thickness spot-check records; salt spray report when specified |
| Packing & export docs | Sample packing list, export packing coordination plan | Agreed packing template + shipping insurance plan |
Commercial and logistics evidence
- Export packing coordination must be explicit: who designs the export crates, load plan per container, dunnage, shrinkwrap, and export-facing labelling. Put export packing coordination into the contract and require approved packing drawings for each SKU.
- Incoterms: define delivery terms explicitly and align responsibilities with the delivery responsibility matrix; use ICC Incoterms to avoid ambiguity [3].
- Customs clearance readiness: require the supplier to confirm export documents and list any potential restricted materials; if shipping to the US, cross-reference import guidance [4].
Financial & contractual protections
- Include acceptance hold points, staged payments tied to factory milestones, and liquidated damages for late delivery where appropriate.
- Consider performance bonds or retention where practical for large projects.
Site installation and operations
Installation interface and handover
- Confirm who supplies what to site: subassemblies vs. shop-assembled units. Factory QA should include a packing manifest and labelled parts for on-site assembly.
- Require pre-shipment inspection (PSI) and photos of packed containers. A short corrective action plan for rework must be available in case of packing damage.
Installers, training and maintenance
- Decide whether the supplier will provide installation supervision, training and maintenance documentation. Factory capability extends to producing clear installation instructions, torque tables, and labeled parts for fast on-site assembly.
- Spare parts strategy: list of critical spares, lead times and minimum stock on site. Include this in project procurement controls.
Operational considerations
- Module tilt, shading management and access for maintenance must be verified during design handover. Factory should provide as-built drawings and BOMs per delivered shipment.
- Warranty and claims: include detailed acceptance testing at site and a documented process for defect reporting, root-cause analysis and remedies.
Important buyer caution (required statement)
- Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Implementation risk: failures, evidence gaps and mitigations
Common implementation risks
- Design drift between shop drawings and site conditions.
- Insufficient packing and container damage.
- Misaligned responsibilities leading to missing items or rework.
- Undetected non-conforming materials entering production.
- Customs delays due to incomplete documentation or restricted material issues.
Risk mitigations
- Lock down technical scope comparison and acceptance criteria before manufacturing.
- Require factory quality documentation and pre-shipment inspection.
- Use the delivery responsibility matrix to assign risks at each handover point.
- Stage deliveries and accept a pilot batch for first-line verification.
- Specify insurance and use clearly defined Incoterms to allocate shipping risks [3].
Decision table — Delivery responsibility matrix (example)
| Stage | Factory (Supplier) responsibility | Buyer / Installer responsibility |
|---|---|---|
| Design & drawings | Provide production drawings, BOM and fixture reports | Review and approve design and module interface |
| Fabrication | Manufacture to approved drawings; label and pack | None during fabrication |
| Pre-shipment inspection | Arrange PSI, provide reports and photos | Witness PSI or accept PSI report |
| Export packing & documentation | Export packing coordination; provide packing list & export docs | Arrange import customs clearance unless DDP agreed |
| Transportation to site | Hand over to carrier at agreed Incoterm point | Arrange site unload, storage, and installation |
| Installation & commissioning | Provide installation manuals and technical support (if contracted) | Install and commission; notify supplier of defects |
Use this matrix to convert expectations into contractual clauses and insurance allocations.
Six-step buyer workflow: “Assess — Validate — Contract — Control — Deliver — Close”
Step 1 — Assess: Define project basis and shortlist suppliers
- Prepare BoD, geotech and permit constraints.
- Shortlist by high-level capability based on product fit, references and initial documentary evidence.
Step 2 — Validate: Deep B2B supplier due diligence and technical scope comparison
- Issue a detailed RFQ with required factory quality documentation and a technical questionnaire.
- Conduct a side-by-side technical scope comparison to highlight omissions and options (see earlier table).
Step 3 — Prototype & Factory verification
- Request prototype, sample parts or a pilot batch for critical connections and finishes.
- Perform a factory audit (remote or on-site) and require pre-shipment inspection procedures.
Step 4 — Contract: Specify delivery responsibility matrix, export packing coordination and procurement controls
- Define Incoterms and set delivery responsibility matrix in the contract.
- Insert hold points, acceptance tests, warranty terms, and financial protections (retentions, bonds).
Step 5 — Control: Production monitoring and logistics
- Monitor production milestones, approve shop drawings, and confirm packing drawings.
- Review PSI reports, tracking numbers and customs documentation.
Step 6 — Deliver & Close: Site acceptance, commissioning and lessons learned
- Conduct site acceptance tests and reconcile packing manifests with delivered items.
- Hold final payments until acceptance criteria are met and produce a lessons-learned report for future procurements.
Practical timeline template
- RFQ & evaluation: 4–6 weeks
- Shop drawings & approvals: 2–4 weeks
- Fabrication: depends on volume 6–16 weeks
- Packing & shipment: 1–3 weeks
- Site installation & commissioning: project dependent
Adjust durations for site constraints, module lead time, and local permit timing.
Mid-article CTA If you want supplier-specific guidance or a documented factory audit checklist tailored to your project, begin a conversation at /inquiry or learn about our SolarGrid commercial solar system. See all systems and our sourcing guides for further context.
FAQ — practical answers to common procurement questions
Q: What is the minimum factory evidence I should expect? A: At minimum: material certificates (MTRs), production drawings, factory quality documentation (inspection plans and submission reports), packing lists, and photos of completed assemblies. Welding and coating procedures are required when those processes are in scope.
Q: Should I insist on an ISO certificate before bidding? A: An ISO certificate (e.g., ISO 9001) is a useful indicator of formal quality management but is not sufficient alone. If a supplier lacks ISO certification, require a detailed quality manual and evidence of consistent execution (12 months of corrected inspection records). See ISO for reference on system standards [2].
Q: How do I allocate shipping risk? A: Use Incoterms to make responsibilities explicit and pair them with a delivery responsibility matrix in the contract. Ensure export packing coordination and insurance are defined; for cross-border shipments ensure the supplier provides necessary export documents and you confirm import rules with local customs authorities [3][4].
Q: When is a pilot order necessary? A: For new designs, novel connections, or high-value projects a pilot batch or prototype reduces risk. Define acceptance criteria for the pilot and the remedial path for defects.
Q: What role should the installer play in factory checks? A: Installer involvement in design approval and pre-shipment inspection is valuable. Have the installer review shop drawings and witness PSI to confirm that parts are packaged and labelled for efficient site assembly.
Q: How do I verify corrosion protection claims? A: Require coating procedures, thickness measurements and where specified, salt spray or other environmental testing records. Where galvanizing is used for steel components, reference galvanizing practice and durability guidance such as that from the American Galvanizers Association [1].
Additional evidence & audit recommendations
Factory audit checklist (high level)
- Management commitment: quality policy, corrective action records.
- Production capability: available machinery, fixture capacity and production lead times.
- QA/QC station: in-process inspection frequency, calibration records.
- Material handling and storage: segregation of raw materials and finished goods.
- Packing and staging area: customised crates, labelling, dunnage and handling instructions.
- Traceability: part IDs, batch linking, MTR filing system.
- Health & safety and environmental controls: basic worker safety and handling for coatings/chemicals.
Document control and change management
- Require that any change to production drawings or BOMs is issued as a controlled revision and that changes require written buyer approval if they affect performance or interfaces.
Third-party testing and witnessing
- For critical connections or finishes, consider third-party test labs to witness/perform tensile or corrosion tests. Arrange witness dates in the purchase order.
Customs & export considerations
- Ensure export packing coordination is complete: container pack plan, weight/volume per container, hazardous materials declaration if batteries or other regulated items are included.
- Cross-check required documents with destination country import rules and use local customs brokers. Guidance on general import/export processes can be referenced through customs authorities [4].
Conclusion
Evaluating solar carport manufacturer factory capability is a multi-dimensional exercise that combines technical fidelity, documented quality systems and clear commercial logistics controls. Use the structured workflow provided — define scope, validate suppliers through B2B supplier due diligence and technical scope comparison, verify factory evidence (including factory quality documentation), and lock responsibilities with a delivery responsibility matrix and explicit export packing coordination. Protect your project with staged acceptance, pilot builds and contractually enforced project procurement controls. Always confirm site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty on a documented project basis with qualified local professionals, installers, utilities and authorities.
For tailored procurement support or to discuss how Carportiva’s systems integrate into your project, contact us at info@carportiva.com. Explore our SolarGrid commercial solar system, view all systems or consult our sourcing guides for more resources.
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion