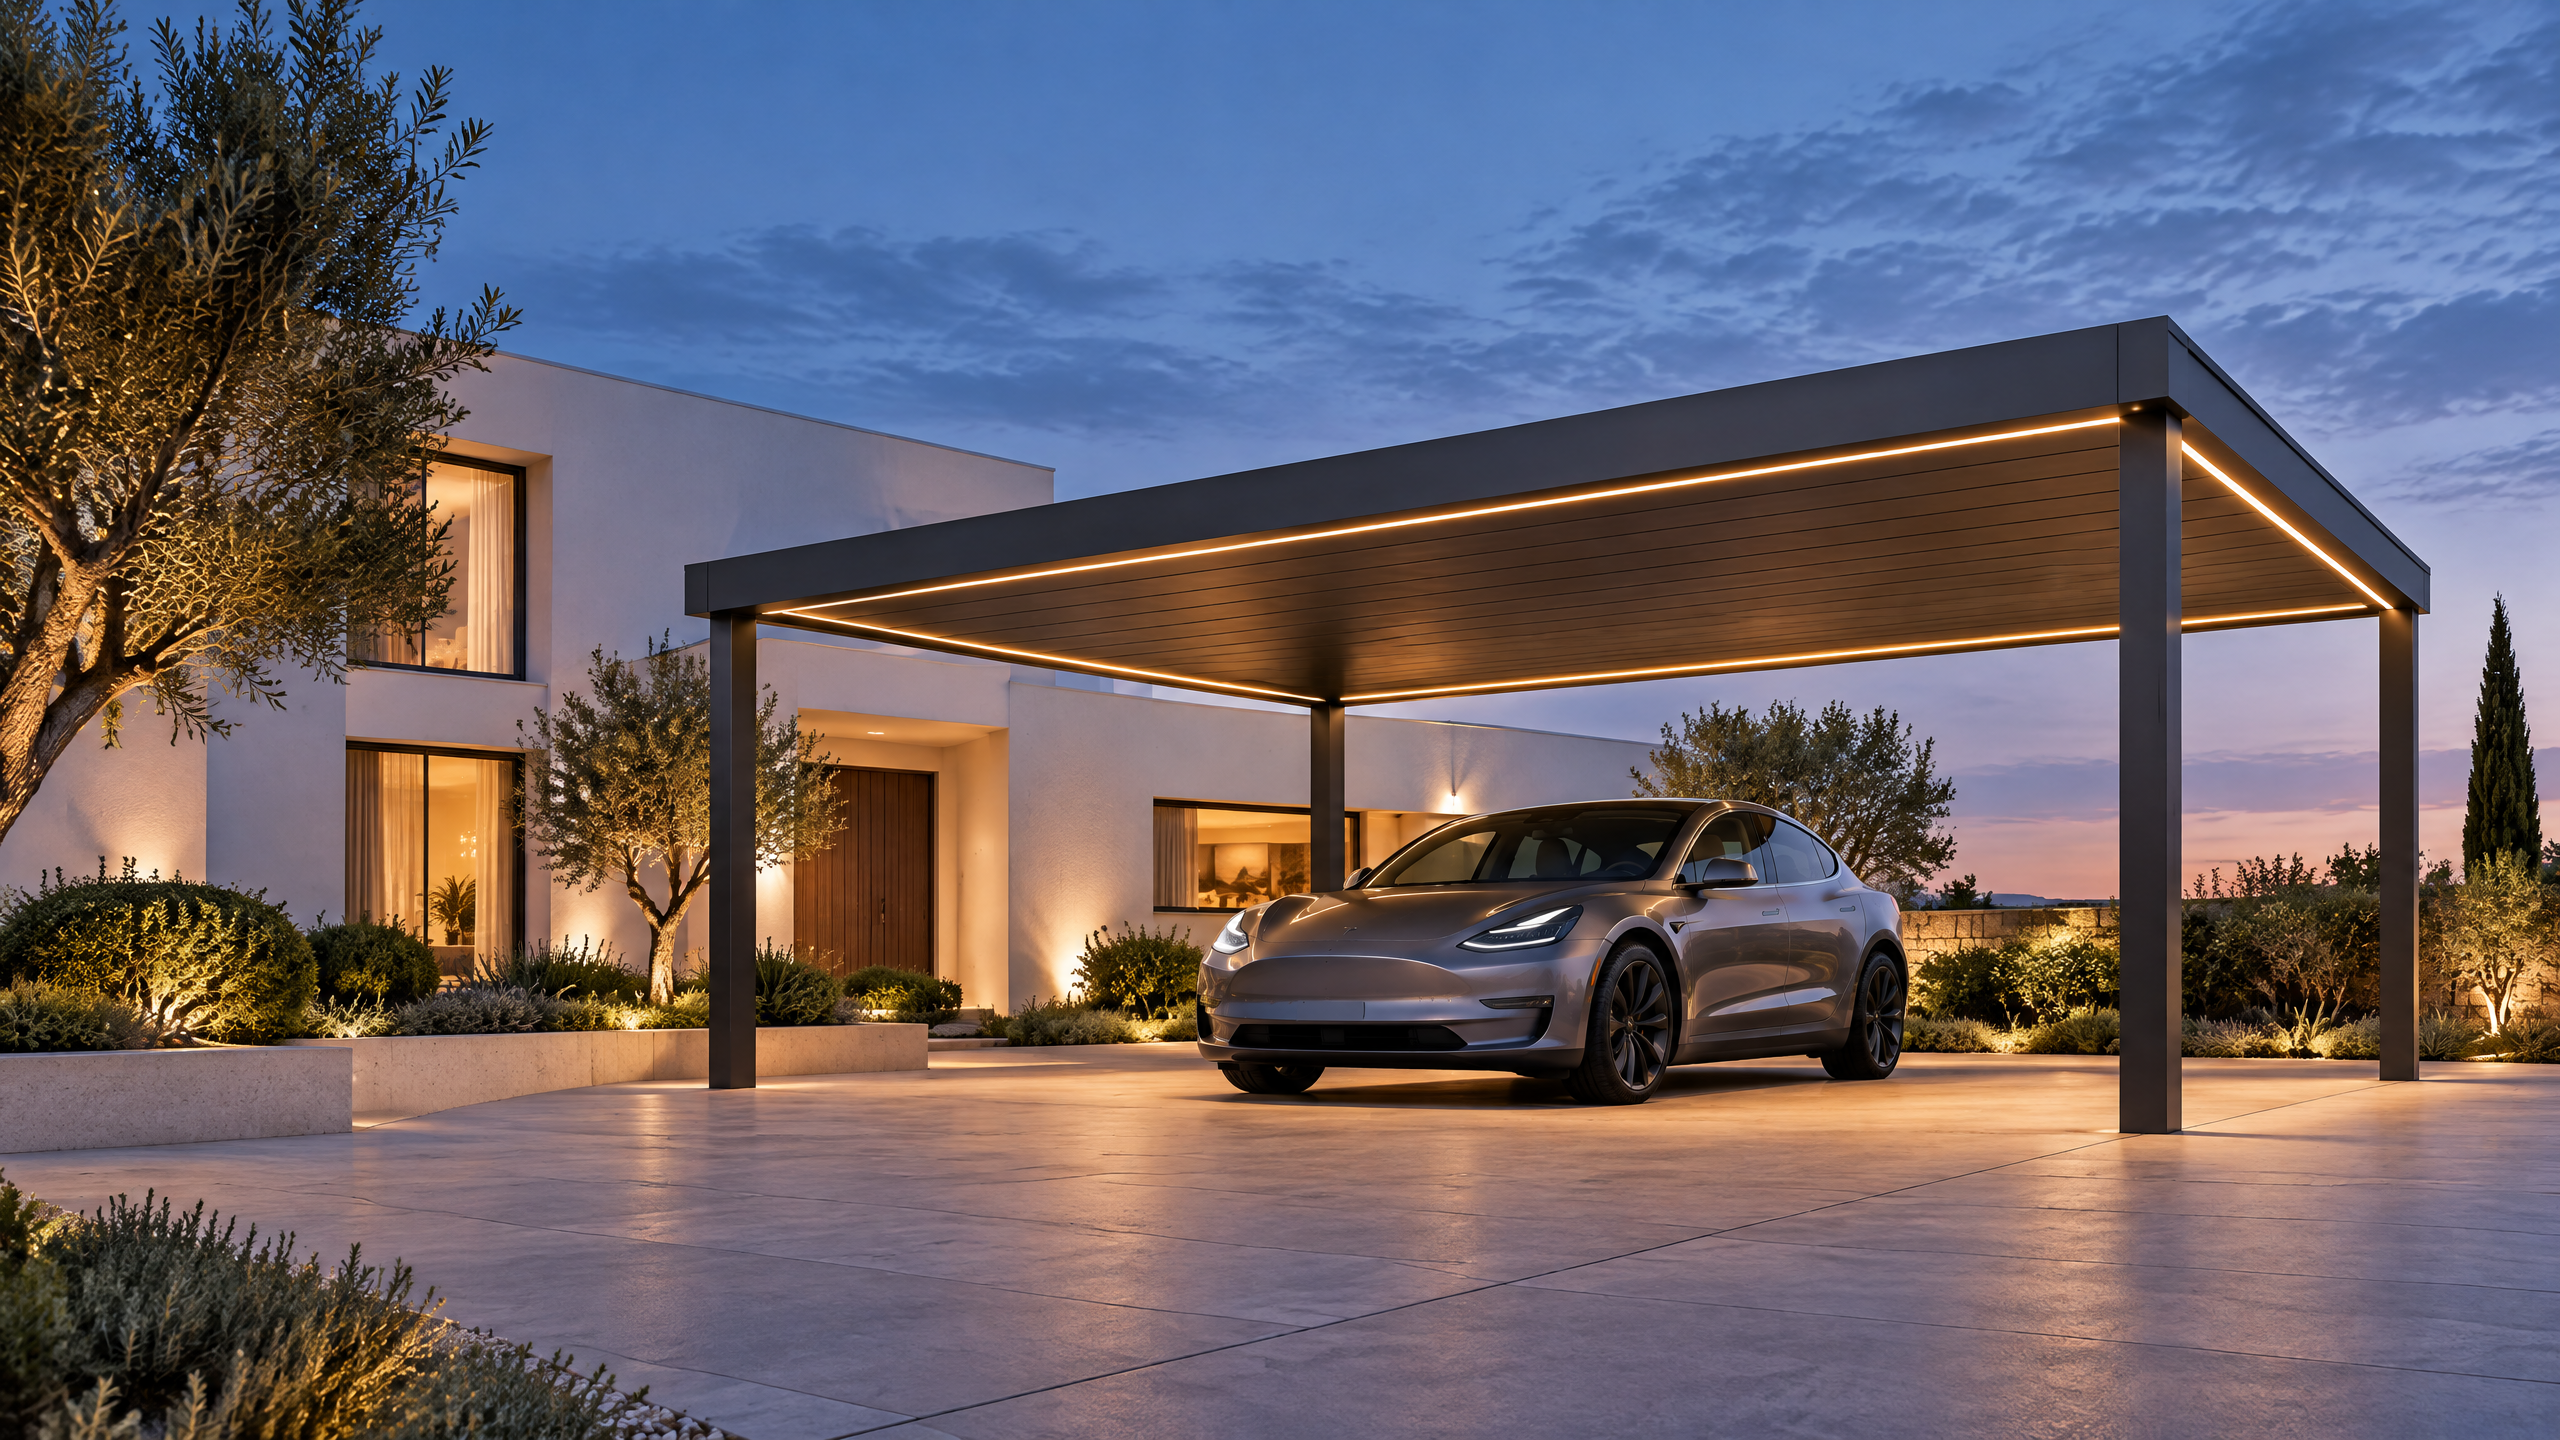
Modern carport architecture balances structural performance, architectural intent and lifecycle cost. The right choice begins with a clear project brief (use, loads, site constraints, budget and desired aesthetic), and proceeds through technical specification, documented shop drawing review and factory evidence before committing to procurement and on‑site installation readiness. This guide concentrates on architectural aluminium systems for carports — covering design principles, materials selection, drainage and electrical interfaces, procurement proofs and an explicit six‑step buyer workflow. It emphasizes verifiable inputs and commissioning checks so buyers (distributors, architects, contractors, developers, solar EPCs and fleet operators) can objectively compare supplier offers and reduce risk during implementation. Where decisions affect structural capacity, foundations, approvals, energy yield or warranty, a documented project basis and qualified local engineers, installers, utilities and authorities must be engaged.
Buyer context and scope boundary: what this guide covers — and what it does not
This guide focuses on modern carport architecture as a design and procurement discipline within the cluster of architectural aluminium systems. It explains how to:
- Translate program needs into an architectural carport specification.
- Assess aluminium systems, finishes and connections for long‑term performance.
- Coordinate roof drainage, PV and electrical interfaces.
- Evaluate supplier documentation, factory QA and shop drawing review.
- Validate site installation readiness and operational handover.
This guide does not replace site‑specific structural design, foundation engineering, electrical design for PV systems, local permitting, energy yield modelling, contract or warranty legal review. These require a documented project basis and appropriate local professionals: structural engineers, geotechnical engineers, certified installers, utilities and local authorities. Where structural loading or wind/snow standards are relevant, consult national versions of the Eurocodes and local building codes for final design criteria [1]. For material and coating performance, consult material standards and manufacturers’ technical data sheets and test reports [2][3][4].
Core decision principle: prioritize a performance‑based specification tied to a verifiable acceptance plan
At the enterprise procurement level, the primary decision principle is: define desired performance outcomes, quantify acceptance criteria, and require supplier evidence demonstrating conformance. For modern carport architecture this means specifying:
- Structural design criteria (design loads, serviceability limits, design life).
- Material and coating systems with referenced standards (alloy, temper, surface treatment).
- Drainage rates and roof sealing criteria to avoid ponding and water ingress.
- Interface definition for PV (if applicable): string locations, cable routing, combiner box zones and inverter access.
- Manufacturing and QA evidence (shop drawing review, factory inspection, test records).
- On‑site acceptance tests and a clear installation readiness checklist.
By anchoring procurement to evidence (drawings, calculations, test reports, factory QC records and installation checklists) buyers move from subjective comparisons (price, look) to objective risk reduction.
Planning inputs: translating program and site into technical requirements
Collect the following inputs before you ask suppliers for proposals. Incomplete inputs produce ambiguous bids and hidden costs.
Required project inputs (minimum)
- Scope and use: vehicle types (cars, EV charging bays, buses, trucks), solar PV intention, pedestrian pathways.
- Site survey: contours, utilities, vehicular access, underground services, local wind and snow map data.
- Geotechnical report: soil bearing capacity and recommended foundation types.
- Local code and permit requirements: fire access, setbacks, building height, zoning.
- Desired design life and maintenance regime: 20, 30 or 50+ year horizons.
- Aesthetic brief: exposed connections, colour palette, profile sightlines, soffit treatments.
- Electrical brief (if PV or EV): inverter/comms location, AC/DC routing, safety clearances, earthing.
- Project schedule: procurement timing, preferred manufacturing lead times, installation windows.
Translating loads and structural requirements
- Specify design reference standards for structural design. For projects in jurisdictions that recognize Eurocodes, identify which parts apply for wind, snow and seismic design [1]. For material property and corrosion guidance reference national aluminium standards and manufacturers’ datasheets [2].
- Include serviceability limits in addition to ultimate loads (maximum allowed deflection, permissible vibration for cantilevers, vertical alignment tolerances).
Decision table — initial scope classification
| Project type | Key drivers | Typical system focus |
|---|---|---|
| Architectural villa / residential (single/multi-unit) | Aesthetics, low to moderate loads, bespoke shapes | Profile visibility, integrated guttering, NordFlat style clean lines |
| Commercial / retail | Customer experience, canopy lighting, mid loads | Integrated drainage, signage integration, reinforced columns |
| Solar carport / PV canopy | Energy yield, module access, mounting spans | PV mounting rails, service cable routing, roof drainage coordination |
| Industrial / fleet shelters | Heavy vehicle clearances, robust durability, ease of maintenance | Heavy gauge profiles, weld or bolted bases, foundation coordination |
Note: Use this classification only as a starting point. All structural and electrical design elements require project‑specific calculations and local approvals.
Technical specification and interface details
This section describes the technical elements that should be explicit in an architectural carport specification. Use clear, measurable requirements — not subjective phrasing.
- Structural system and connections
- Specify member types (columns, beams, rafters), cross‑section dimensions and expected manufacturing tolerances.
- Require structural calculations (by qualified engineers) stamped for the project location. Identify the governing load cases (dead, live, wind, snow, seismic) and serviceability criteria per local code (e.g., Eurocodes where applicable) [1].
- Define connection detailing: bolted vs welded connections, paint stripping allowances for welding, sacrificial washers, and corrosion allowances.
- Aluminium material and extrusions
- State required alloys and tempers acceptable for the project (e.g., 6000 series for structural extrusions), and require manufacturer certificates for chemical composition and mechanical properties. Reference aluminum industry guidelines for alloy selection and corrosion behavior [2].
- Define surface finish and thickness tolerances for extruded profiles.
- Aluminium profile selection
- For modern carport architecture, aluminium profile selection governs span capabilities, visual proportion and thermal movement. Provide:
- Required clear spans and cantilever lengths.
- Maximum permitted deflection ratios (L/200, etc.) for aesthetic rooflines.
- Thermal expansion considerations and sliding or floating connections for long spans.
- Roof and waterproofing interfaces
- Specify roof cladding type (flat panels, standing seam, translucent panels, PV modules). For PV, specify module frames, clamps and rail systems and require compatibility testing with the chosen profile.
- Roof drainage coordination: state minimum slope, gutter capacities, downpipe locations and debris protection. Define overflow requirements and freeze protection where applicable.
- Finish and fastener compatibility
- Require corrosion compatibility between aluminium profiles, fasteners and coatings. Specify fasteners (material and finish) to avoid galvanic corrosion — e.g., stainless fasteners insulated from aluminium where required, or aluminium fasteners with suitable coatings.
- State coating systems (e.g., PVDF, anodizing) and performance expectations, with reference to standards and expected life cycles. For architectural appearances, require colour and gloss tolerances and reference colour codes.
- Thermal movement and tolerances
- Provide temperature range expectations and calculate expansion for long runs. Specify movement joints and sliding connections at design locations.
- Electrical and PV interfaces
- For solar carports, define PV layout, module orientation, tilt, cable trays, conduit penetrations and locations of combiner boxes and inverters. Require clearance and access zones for maintenance.
- Specify lightning protection and bonding requirements in line with project electrical engineer recommendations.
- Foundations and anchorage
- Give soil bearing pressure assumptions and minimum embedment depth if geotechnical data is not yet available, and clearly state that final design depends on geotechnical input.
- Define anchor types, grout or bolts, and tolerances for base plate positions.
Decision table — technical acceptance checklist (use with supplier offers)
| Specification item | Minimum buyer requirement | Supplier evidence |
|---|---|---|
| Structural calculations | Stamped engineer calculations for local code | Signed calculations, load case list |
| Aluminium alloy | Specified alloy/temper class | Mill test certificate |
| Surface finish | Coating system and expected life | Coating datasheet, test report |
| Fasteners | Material and insulation strategy | Material certs and sample |
| Drainage | Calculated gutter capacities, slopes | Layout drawings and drainage calcs |
| PV interface | Mounting detail and cable routing | PV mounting spec and routing plan |
| Shop drawings | Full set for production | Shop drawing review sign‑off |
Procurement, factory evidence and shop drawing review
When evaluating suppliers, require a structured evidence package and perform a documented shop drawing review before any factory work begins.
Required procurement documents
- Detailed quotation referenced to the buyer’s specification (include exclusions).
- Bill of materials and part numbers for extrusions and purchased items (fasteners, gutters, PV rails).
- Production lead time and key milestones (shop drawing approval, pre‑production samples, production start, shipment).
- Test and inspection plan: dimensional checks, welding records, coating adhesion tests, packaging details.
Factory evidence and QA expectations
- Factory Quality Management: request evidence of systems (e.g., ISO 9001 registration evidence — consult the ISO platform for standards where relevant) [4]. Do not accept generic claims without documentation.
- Sample approvals: physical samples of critical elements (junction details, coated profiles, fasteners) signed off by the buyer prior to mass production.
- Non‑conformance management: supplier procedure for handling deviations and corrective action records.
- Packaging and logistics plan: show protection details for finished aluminium profiles, shipping orientations and handling limits.
Shop drawing review
- Require supplier shop drawings and a structured review process. The buyer should return comments in a documented punch list; supplier must produce revised drawings and a sign‑off sheet prior to manufacturing.
- Keep shop drawing review focused on dimensions, tolerances, connection interfaces, embedded items, hole locations and drainage slopes. This is the primary opportunity to identify clashes with foundations, openings, PV tray locations and electrical penetrations.
- Explicitly include a schedule for review turnaround time and consequences for missed approvals.
Include "shop drawing review" as a milestone in procurement contracts and link acceptance to release for production.
Caveat: supplier drawings and factory QA records do not replace certified structural calculations and site inspections done by local professionals.
Site installation, logistics and installation readiness
Successful on‑site installation depends on early coordination and clear installation readiness criteria.
Pre‑installation coordination
- Confirm foundation positions and set‑out with surveyor. Require survey control points and as‑built foundation verification reports showing anchor bolt positions and levels within specified tolerances.
- Coordinate delivery windows to match crane and site availability. Provide storage and handling instructions to avoid profile bending or coating damage.
- Verify electrical shutdown windows and routing for PV stringing and inverter installation.
Installation readiness checklist (minimum)
- Foundations: as‑built verification report and template accuracy within tolerance.
- Anchors: correct material, embedment and torque specifications available.
- Lifting and rigging plan: certified equipment and personnel.
- Weather plan: actions for heavy rain, high winds or freezing conditions.
- Installation drawings and assembly sequence printed and accessible on site.
- Spares: list of spare profiles, fasteners and sealants delivered to site.
- Quality records: inspection sheets, torque logs, drainage slope checks, final sign‑off form.
Testing and commissioning
- Structural: final alignment and fixity checks, bolt torque verification and weld inspection as required.
- Drainage testing: water test for gutter runs and downpipes to confirm absence of leaks and adequate fall.
- PV commissioning: perform electrical commissioning per electrical engineer and utility requirements. Energy yield modelling must be completed by a competent PV modeller and is basis‑specific; do not rely on generic estimates.
Always confirm that local installers are certified to install aluminium architectural systems and, where PV is included, that PV installers are accredited under relevant local schemes.
State requirement: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Implementation risks and mitigation strategies
Major risks and practical mitigations for modern carport architecture procurement and delivery.
Risk: Incomplete or ambiguous specifications
- Mitigation: Use a performance‑based architectural carport specification with measurable acceptance criteria and a mandatory shop drawing review clause.
Risk: Mismatch between factory production and site conditions (holes, anchor locations)
- Mitigation: Enforce pre‑installation survey and as‑built verification; adopt a tolerance schedule and require supplier to allow for site adjustment in bolted connections.
Risk: Galvanic corrosion between incompatible materials
- Mitigation: Require finish and fastener compatibility documentation, specify insulated connections or compatible materials, and include sacrificial layers where appropriate.
Risk: Drainage failure causing ponding or water ingress
- Mitigation: Include roof drainage coordination early; require drainage calculations, overflow provisions and water testing on site.
Risk: PV integration conflicts (module shading, cable routing)
- Mitigation: Provide PV layout early in design, require combined structural and PV mounting review, and identify maintenance access zones.
Risk: Unexpected lead times or supply chain delays
- Mitigation: Ask for firm lead time commitments, identify critical long‑lead items (special extrusions, custom colours), and consider early ordering of long‑lead components or alternate suppliers from all systems.
Risk: Warranty disputes due to unclear acceptance tests
- Mitigation: Define acceptance tests and handover documentation in the procurement contract and collect factory QA records. Preserve signed shop drawing review documentation and installation readiness checklists.
Risk: Local compliance and permitting
- Mitigation: Engage local building authorities and utilities early. Ensure supplier documentation includes information necessary for permit submissions (product datasheets, anchor loads, drawings).
Procurement evidence matrix — what to demand and why
Use this matrix to shortlist suppliers and compare apples to apples.
| Evidence item | Why it matters | Minimum acceptable |
|---|---|---|
| Stamped structural calculations | Ensures the system is designed for local loads | Signed engineer calculations for project jurisdiction |
| Mill certificates for alloys | Verifies material conforms to spec | Certificate showing alloy and temper |
| Coating datasheets and test reports | Predicts performance and maintenance | Manufacturer datasheet and lab test evidence |
| Shop drawings with revision history | Prevents production errors and site clashes | Buyer‑reviewed and signed shop drawings |
| Factory inspection reports | Confirms production quality and non‑conformance handling | Records of dimensional checks, weld tests, coating adhesion |
| Installation procedure and checklist | Reduces on‑site errors and ensures consistent installation | Detailed procedure and a site sign‑off form |
| Sample approvals | Validates finish and assembly before production | Signed physical samples or mock‑ups |
| Packaging and transport plan | Prevents damage in transit | Packaging details and handling instructions |
A named six‑step buyer workflow: from brief to handover
This buyer workflow is a repeatable sequence you can apply across projects to reduce disputes and improve delivery outcomes.
Step 1 — Define the project brief and measurable outcomes
- Produce a document that includes program, loads (design references), finish requirements, PV intent, maintenance regime and schedule. Share the brief with vendors and consultants. Include reference to sourcing guides where relevant.
Step 2 — Prequalification and shortlist
- Request capabilities, sample profiles and factory evidence. Evaluate supplier capacity for custom extrusions, QA systems and lead times. Visit factories where high value or bespoke systems are involved.
Step 3 — Issue detailed architectural carport specification and invite proposals
- Include all required inputs (site survey, geotechnical information, structural code reference). Require quotes tied to specific revision numbers of drawings and materials.
Step 4 — Shop drawing review and sample approvals
- Initiate formal shop drawing review. Approve samples for finish, fasteners and junctions. Record comments and require revised drawings before production release. This is the formal "shop drawing review" milestone.
Step 5 — Production and factory inspection
- Perform agreed factory inspections or witness key tests. Secure factory QA records and shipping documents. Confirm packaging meets site handling constraints.
Step 6 — Delivery, installation readiness and handover
- Ensure foundations and anchors meet as‑built tolerances. Complete the installation readiness checklist before assembly. Conduct final acceptance tests (structural, drainage and electrical). Close procurement with documented handover and warranty records.
Throughout the workflow, maintain a single source of truth for documents (drawings, revision history, certificates) and require formal sign‑offs at each milestone.
Mid‑article CTA
For detailed system descriptions and component options, review the NordFlat architectural villa system, explore all systems and consult our sourcing guides. To discuss a project brief or request a specification template, start an inquiry: /inquiry.
Frequently asked questions (FAQ)
Q: How do I compare aluminium systems from multiple suppliers? A: Compare using a common technical baseline: same design loads, same finish expectations, same tolerances and same acceptance tests. Use the procurement evidence matrix on page X and insist on shop drawing review before manufacturing.
Q: What alloy should I specify for structural extrusions? A: Select alloys based on structural needs and corrosion environment; 6000 series alloys are commonly used for structural extrusions, but final alloy and temper must match the engineering calculations and supplier mill certificates [2]. Always require material certification.
Q: Who is responsible for foundations and anchor bolts? A: Foundations and anchors are the buyer’s responsibility unless explicitly included in supplier scope. Foundations require geotechnical input and must be verified as‑built before installation to ensure installation readiness.
Q: How should I manage finish matching between coated extrusions and other materials? A: Demand finish and fastener compatibility data. For coated systems, require colour and gloss tolerances, and use the same coating specification across connected elements where possible to reduce galvanic and aesthetic issues. Consider using anodized finishes where appropriate and consult AAMA or coating manufacturers for performance expectations [3].
Q: Are off‑the‑shelf extrusions enough for large spans? A: Off‑the‑shelf extrusions can be used, but long spans often demand bespoke profiles to control deflection and limit the number of joints. Include aluminium profile selection criteria early in design to avoid costly redesign.
Q: What should be in an installation readiness checklist? A: See the Installation readiness checklist earlier in this guide. Core items include verified foundations, anchor locations, weather plan, lifting plan, drawings on site, spares delivered and signed QA documentation.
Q: Can I rely on supplier lead times quoted at tender? A: Supplier lead times should be contractual and tied to milestones such as shop drawing approval. Long‑lead items should be identified and tracked; consider contingency plans or alternative suppliers for critical components.
Q: How to verify drainage performance? A: Require roof drainage coordination drawings and gutter capacity calculations based on local rainfall intensity. Verify on site with water tests and include overflow provision and debris screens where appropriate.
Conclusion
Modern carport architecture is a convergence of architecture, structural engineering and systems integration — particularly when aluminium profiles, finishes and solar PV are involved. Buyers achieve consistent outcomes by specifying measurable performance criteria, demanding verifiable supplier evidence (material certificates, stamped calculations, signed shop drawings and factory QA records), and enforcing a structured procurement workflow that includes sample approvals and installation readiness checks. Critical interfaces — foundations, roof drainage coordination, PV and electrical systems — must be coordinated early and resolved through defined acceptance tests. Site‑specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty all require a documented project basis and input from local qualified professionals, installers, utilities and authorities. Use the six‑step workflow, the procurement evidence matrix and the checklists in this guide to reduce risk and deliver modern carport architecture that meets both design intent and operational needs.
For project consultations or to request specification templates, contact our team: /inquiry or email info@carportiva.com.
References (selected)
- Eurocodes for structural design and load definitions [1].
- Industry guidance on aluminium materials and properties [2].
- Coating and façade performance guidance [3].
- ISO standards and certification information platform [4].
References
- European Commission Eurocodes: https://eurocodes.jrc.ec.europa.eu/
- The Aluminum Association: https://www.aluminum.org/
- American Architectural Manufacturers Association: https://aamanet.org/
- ISO Online Browsing Platform: https://www.iso.org/obp/ui/
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion