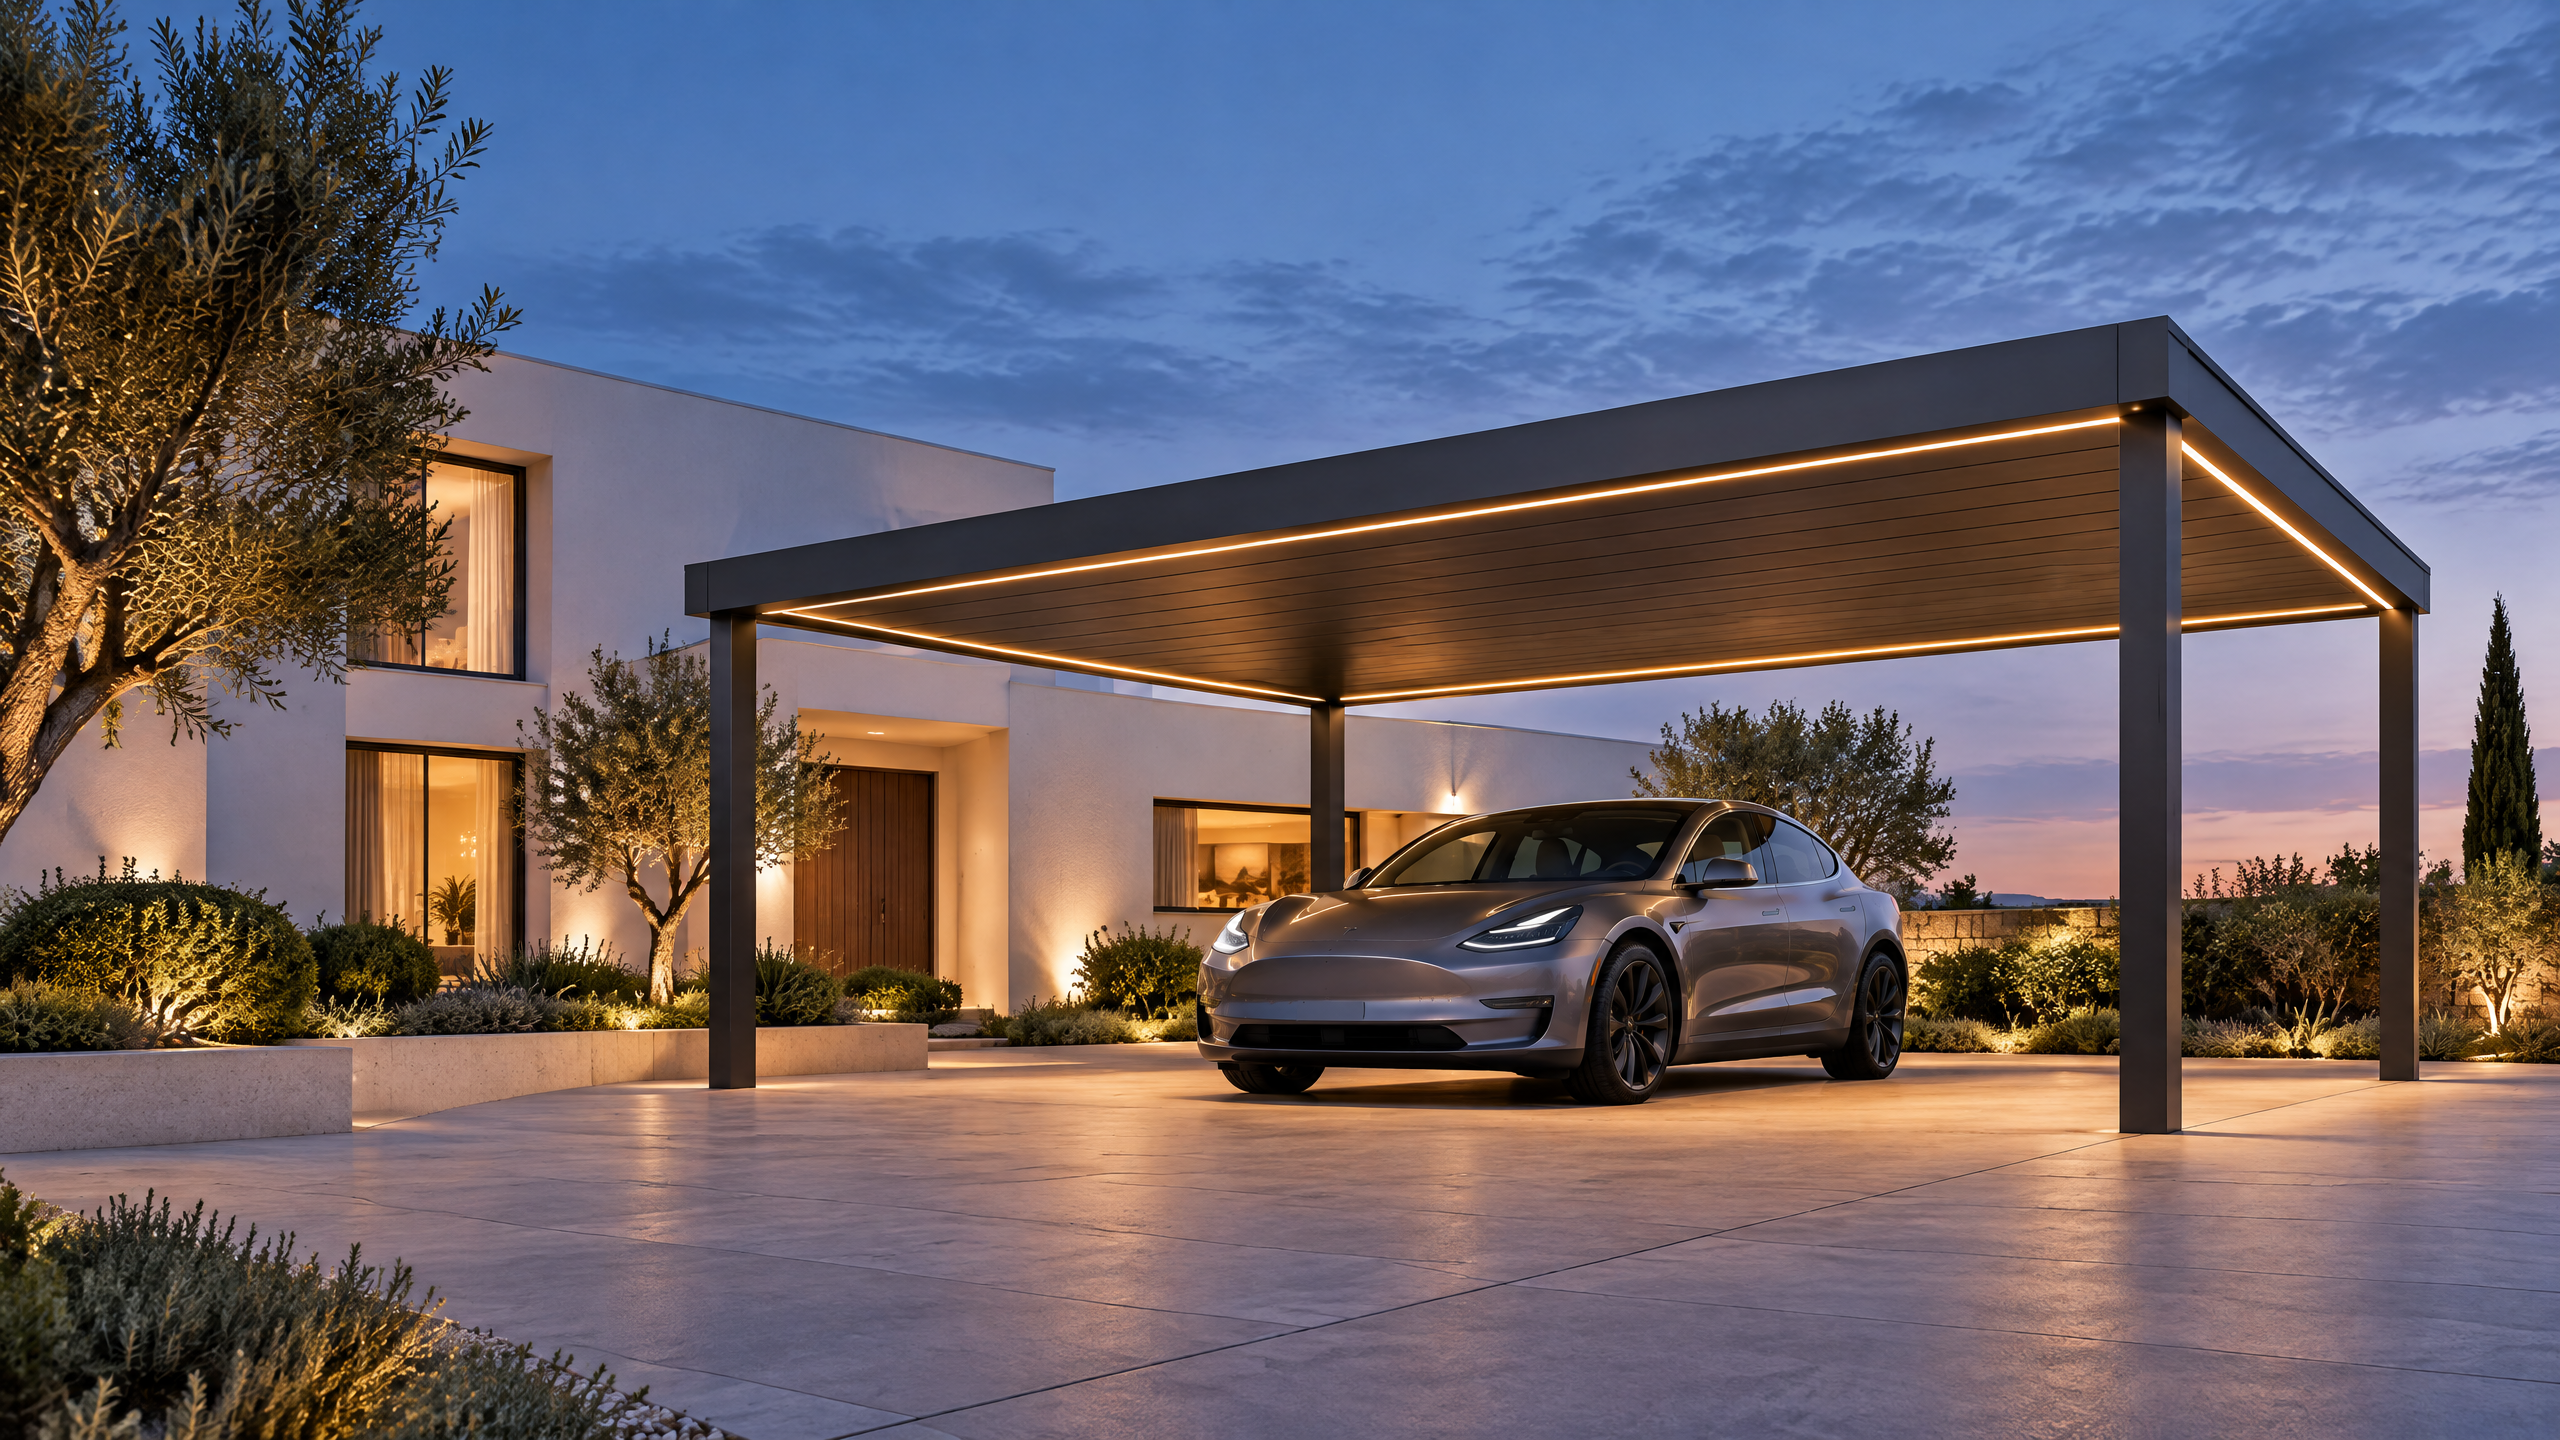
An effective B2B purchase starts by confirming capability, interfaces and responsibilities—not price or promises. Before committing to a specific aluminum carport canopy factory you must verify the factory’s ability to deliver design documentation, manufacturing tolerances, connection detail compatibility, and logistics that match your project constraints. Confirm that the factory can supply shop drawings and a clear aluminum carport canopy roof system layout, show how the aluminum carport canopy column layout ties into foundations and local load paths, and demonstrate production QA processes and traceable material data. Equally important: establish who on the project team (architect, structural engineer, local authority, utility, installer) will approve drawings, choose finishes, and accept on-site assembly. This checklist-style confirmation prevents scope gaps when integrating modern carport architecture or a modern carport aluminium system into a larger build or solar installation.
What this guide covers — and what it does not
This guide explains the confirmations, documents and coordination steps you should expect from an aluminum carport canopy factory during bidding, contract and delivery stages. It addresses design interfaces (roof system and column layout), manufacturing scope, documentation, transport and site handover for architectural carports, solar carports and fleet shelters.
It does not promise structural capacity, permit approvals, code compliance, lead times, price, energy yield or warranty. Final, site-specific determinations must be made by local qualified professionals, authorities, utility providers and installers.
Six core confirmations to request from any aluminum carport canopy factory
- Factory deliverables: list of documents and drawings the factory will supply for approval (e.g., preliminary layout, shop drawings, assembly drawings, parts lists, BOM).
- Design responsibility split: which parties supply structural inputs (loads, uplift, snow, seismic), which party produces connection details, and who signs/accepts them.
- Material traceability: aluminium alloy designations, temper, surface finish specification and paint/ anodize process, with measurable tolerances.
- Interface details: exact aluminum carport canopy roof system profiles, water/drainage strategy and the aluminum carport canopy column layout including baseplate and anchor specifications.
- Quality assurance processes: factory inspection stages, dimensional control, packing checks and non-destructive testing procedures where applicable.
- Logistics and installation scope: whether the factory provides preassembly, lifting/handling instructions, on-site supervision, spare-parts lists and packaging protection.
Confirm each item in writing and include acceptance criteria in the purchase order or contract.
Documents and drawings you must obtain and check
- Concept and site layout: plan showing the canopy footprint relative to property lines, utilities and access.
- Shop drawings: full-size elevation, section and plan views of the aluminum carport canopy roof system and column grid.
- Connection details: baseplate, anchor bolt patterns, splice locations and lifting points for each column and beam.
- Bill of Materials (BOM): unique part numbers, material designations and quantities.
- Assembly sequence: labeled components and bolting torque or welded splice instructions.
- Finish specification: paint system or anodizing class, color codes and maintenance guidance.
- Packing and handling drawings: crate dimensions and weights for transport planning.
These documents form the basis of permit submissions and installer tender packages; ensure the factory commits to update them if on-site conditions change.
Technical interface: roof system, column layout and drainage
A clear technical interface prevents redesigns on site.
- Aluminum carport canopy roof system: confirm the roof profile geometry, module spans, and how roofing panels or PV racking fix to the primary beams. Ask for load paths for point loads (e.g., solar modules), continuous loads (snow, dead load), and dynamic loads (wind uplift). While the factory can supply profile drawings, the structural engineer must validate load assumptions for the site.
- Aluminum carport canopy column layout: request a grid plan showing column coordinates, baseplate sizes and anchor bolt patterns that match slab or pad details. The factory should indicate column centers, column-to-beam connections, and where expansion joints or movement slots are required.
- Drainage and waterproofing: confirm internal or external guttering, downpipes and connections to site drainage. Clarify leak testing or pre-sealing activities the factory performs in controlled conditions versus what the installer must complete on site.
Decision table: Roof vs Column interface responsibilities
| Responsibility area | Factory provides | Buyer/Local professional must confirm |
|---|---|---|
| Roof member geometry and profiles | Shop drawings and cut lists | Site-specific load combinations and local code loads |
| Column coordinates and baseplate details | Baseplate shop drawings and anchor pattern | Foundation design, concrete strength and bolt embedment |
| Drainage outlets and overflow | Gutter/drain layout and roof slope | Connection to local stormwater system and permits |
Material, finishes and long-term behaviour
Ask the factory to specify exact alloys, temper designations and surface treatment steps in a modern carport aluminium system. Typical confirmations include alloy (e.g., a common structural grade), surface treatment (anodize class or powder-coat system with film thickness ranges), and expected tolerances for extrusions and plate work.
Ensure the factory provides:
- Material certificates or mill test reports traceable to BOM items.
- Coating system datasheets naming primers, topcoats, target DFT, and adhesion tests the factory performs.
- Maintenance recommendations: frequency and products for cleaning and touch-up.
For architectural applications use references to modern carport architecture principles when discussing visible joints, shadow lines and thermal movement; ensure the finish selection supports the desired appearance and durability.
Caveat: do not rely on factory claims alone for long-term corrosion behaviour or finish performance; local environmental conditions and maintenance determine service life.
Reference note: industry material and finish standards exist and can guide specification choices [2][3].
Manufacturing quality, inspection and acceptance
Confirm the factory’s inspection checkpoints and which records they will provide:
- Incoming material inspection
- Dimensional control at section cut and assembly
- Fastener and torque verification
- Finish inspection (appearance, thickness)
- Final packing inspection
Ask for example inspection templates or a copy of the factory’s non-conformance process. For complex projects, specify independent inspection points or hold-points requiring buyer sign-off before shipping.
Decision table: Typical QA documentation to request
| Document | Why it matters | Accept/Reject criteria |
|---|---|---|
| Mill test reports (MTRs) | Verifies alloy and temper | Matches BOM alloy and material grade |
| Shop dimensional check reports | Prevents field rework | Key dimensions within contractual tolerances |
| Coating inspection records | Confirms finish integrity | DFT within specified range and visual pass |
| Packing and handling checklist | Avoids transit damage | Components protected and lifting points marked |
Logistics, packaging and site assembly interface
Large canopy elements require early coordination:
- Shipping units: request crate sizes, gross weights and lifting points to confirm transport and crane capacity.
- On-site handling: factory should supply assembly sequence, required number of installers, recommended torque values, and temporary bracing procedures.
- Spares and consumables: identify a small spare-parts list (gaskets, fasteners, small extrusions) the factory will include or make available post-delivery.
- Acceptance criteria: define first-off inspection at site, and an agreed snag punchlist process for resolving issues found during installation.
Be explicit about which party will provide on-site supervision, and how design changes will be handled (change notices, cost and time implications). If the project includes photovoltaic mounting, coordinate the canopy roof system with the solar EPC for attachment points and cable routing.
Procurement and contract language to include
Insert the following into commercial documents to reduce ambiguity:
- Deliverable list (drawings, MTRs, inspection records)
- Factory hold-points requiring approval prior to shipment
- Packaging and lifting instruction obligations
- Spare parts and field replacement lead-time commitments
- Warranty administration contact and process (but not warranty terms themselves)
Also align contractual design responsibility language so the factory cannot assume responsibility for local code compliance or foundation design unless explicitly contracted.
Link: For broader product options see all systems and design reference materials in our sourcing guides. If your brief is architectural-villa focused, review NordFlat architectural villa system.
Five-step buyer workflow: “Confirm, Coordinate, Contract, Control, Close”
- Confirm: Issue a written technical inquiry listing required deliverables and site constraints (coordinates, wind zone, access, utility locations).
- Coordinate: Share the project basis of design with factory and obtain preliminary shop drawings for review.
- Contract: Include explicit deliverables, hold-points and inspection requirements in the purchase order or supply contract.
- Control: Monitor factory QA records, approve hold-point outputs and manage change orders with clear cost/time implications.
- Close: Accept deliveries against the documentation package, establish a snag list, and confirm spare parts and as-built drawings.
If you prefer a six-step variant, add “6. Maintain” to schedule periodic inspections and maintenance handover.
Mid-article CTA: If you are ready to request a formal document package or initial shop drawings, start an inquiry at /inquiry or email info@carportiva.com with your project brief.
Risk allocation and who must decide what
- Factory: supplies documented shop drawings, parts, finish and packing per contract.
- Architect/Design team: approves aesthetics, alignment with modern carport design specification and integration with adjacent architecture.
- Structural engineer: verifies load cases and foundation design.
- Local authorities/utilities: approve permits and utility connections.
- Installer/contractor: performs on-site assembly per approved shop drawings and handles final sealing, testing and commissioning.
State clearly in contracts that local qualified professionals, authorities, utility providers and installers make final site-specific decisions. The factory’s technical input is part of a larger compliance and installation ecosystem.
Common trade-offs and guidance for specification choices
- Span vs column density: wider spans reduce column count but increase beam section sizes and handling constraints.
- Concealed fixes vs exposed fasteners: concealed fixings improve aesthetics typical of modern carport architecture but increase fabrication and tolerance demands.
- High-performance coatings vs cost: select finishes aligned with local exposure (marine, industrial) and maintenance budgets; factory data should inform choices.
Decision table: Design trade-offs at a glance
| Priority | Option | Effect on schedule | Effect on cost | Effect on maintainability |
|---|---|---|---|---|
| Minimize columns | Increase span/girder size | May increase fabrication time | Higher | Similar or higher |
| Architectural continuity | Concealed joints and precise finishes | More complex approvals | Higher | Potentially easier to maintain visually |
| Rapid install | Modular pre-assembly | Requires larger transport lifts | Moderate | Reduces on-site labor |
Related sourcing terms
In project research, these connected terms should be reviewed against the same live brief: modern carport manufacturer. They are search phrases, not separate technical guarantees.
Frequently asked questions
Q: Will the factory approve my foundation design? A: The factory provides baseplate and anchor patterns but does not approve foundations; foundation design must be verified by a local structural engineer.
Q: Can the factory guarantee compliance with local building codes? A: The factory can design to supplied code parameters, but final code compliance and permit approvals are the responsibility of local authorities and the project’s registered professionals. Consult relevant standards as needed [1].
Q: What documentation should I expect before shipping? A: Expect shop drawings, BOM, packing lists, MTRs and factory inspection records. Confirm required hold-points in the contract.
Q: Who is responsible for integrating PV modules on a canopy? A: The solar EPC typically defines module attachment and electrical routing. The factory must provide structural attachment points and demonstrate compatibility with the aluminum carport canopy roof system; final electrical connections and energy yield assessments are beyond the factory’s scope.
Q: How do I handle changes found during site assembly? A: Use a written change-control process: capture the issue, request a proposed modification and cost/time impact from the factory, and approve via issued change order.
Conclusion
Selecting an aluminum carport canopy factory for commercial or architectural projects is a coordination task as much as a procurement exercise. Prioritize clear, contractual confirmations: deliverables, interface drawings, material traceability, QA records and logistics. Keep responsibilities for structural verification, permits and on-site acceptance with local qualified professionals, utilities and installers. Use the five-step workflow above to convert technical queries into a controlled delivery and installation process.
Final CTA: To request a documentation package, initial shop drawings or to start a formal inquiry, go to /inquiry or email info@carportiva.com.
References
- European Commission Eurocodes.
- The Aluminum Association.
- American Architectural Manufacturers Association.
- ISO Online Browsing Platform.
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion