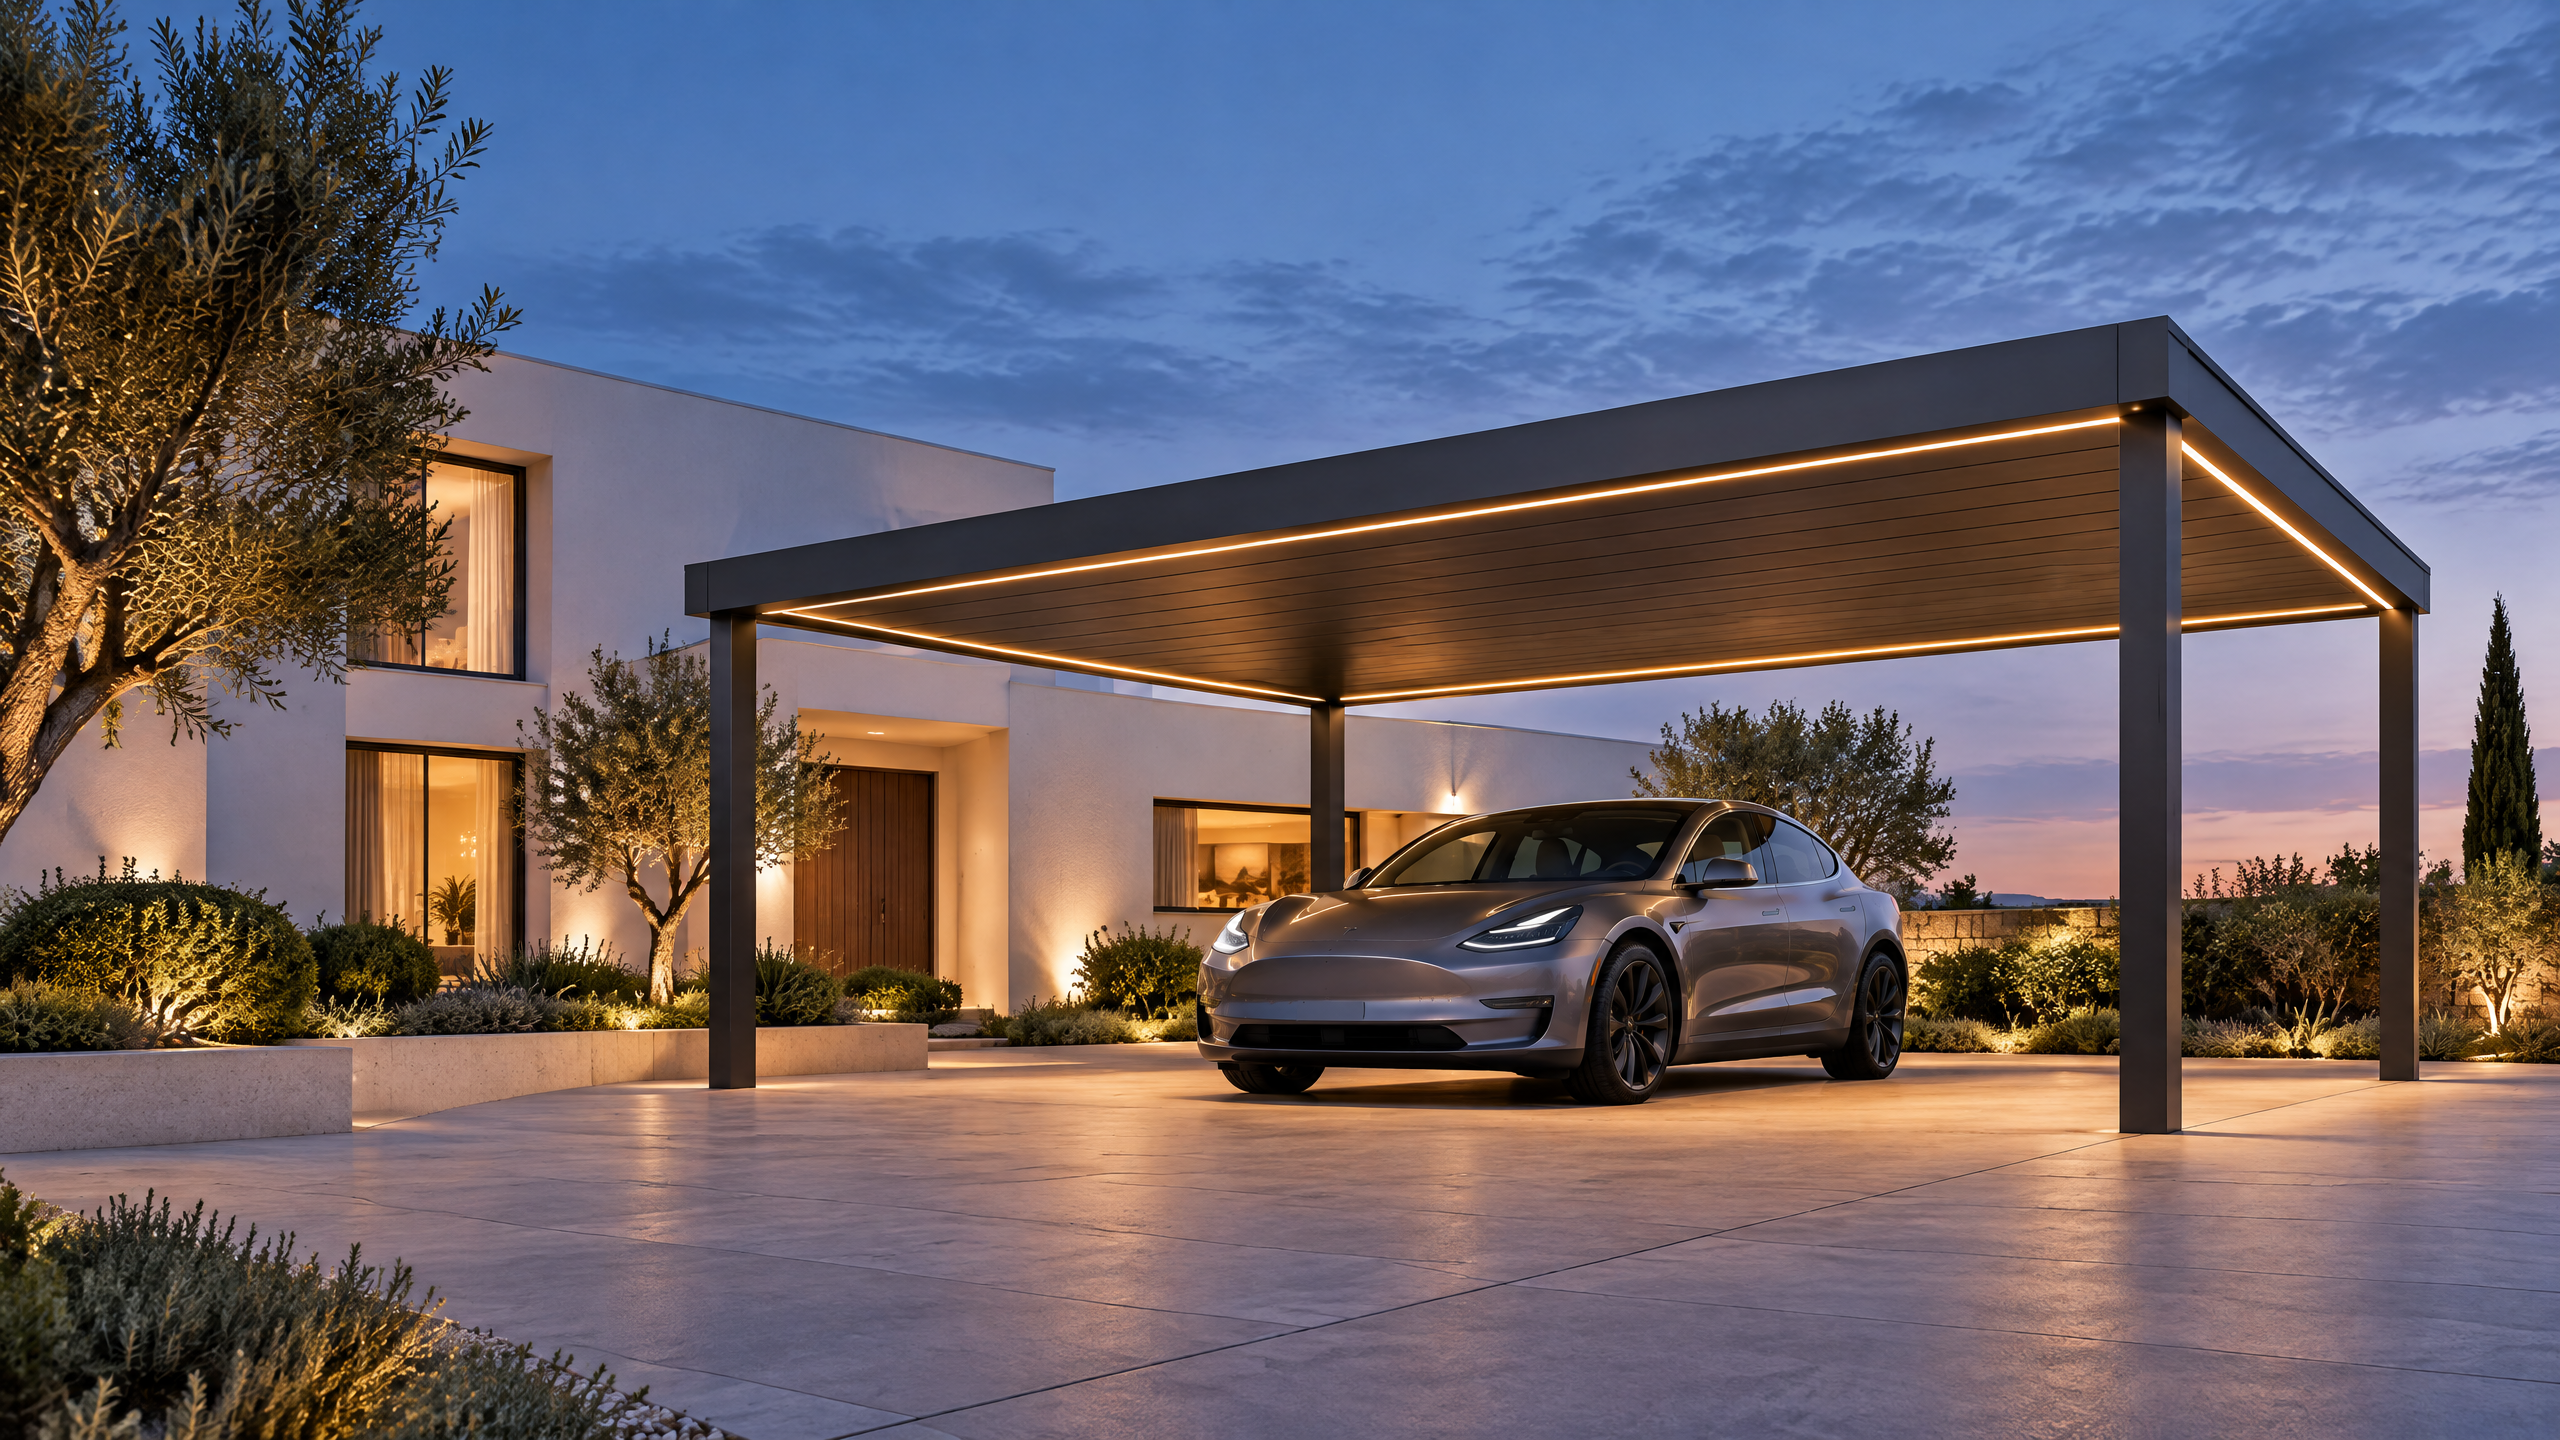
Direct answer (approx. 140 words) An attached aluminium carport design must be treated as an integrated architectural-aluminium system that reconciles site constraints, structural loads, building interfaces and long-term performance requirements. For a purchaser or project team the immediate confirmations are: that the design meets the project scope and local codes for wind, snow and lateral loads; that the architectural carport specification aligns with building façades and penetrations; that aluminium profile selection, finishes and fasteners are compatible with adjacent materials; that roof drainage coordination and electrical routing (for lighting or PV) are fully resolved; and that shop drawing review and installation readiness milestones are defined and resourced. Procurement should demand factory evidence (manufacturing records, QA, material traceability) and a documented risk and maintenance plan. Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and involvement of relevant local qualified professionals, installers, utilities and authorities.
Buyer context and scope boundary: who must act and why this matters
Purpose
- Define the decision authority and boundaries for any attached aluminium carport design procurement: architect/engineer of record (AOR), client, façade contractor, structural engineer, installer, and responsible procurement lead.
- Clarify that an attached carport is an architectural element with structural, waterproofing and service-integration responsibilities similar to other load-bearing attachments.
Scope boundary checklist
- Is the carport purely a covered parking structure or does it carry PV panels and electrical systems?
- Is it attached to a residence, multi-residential building, commercial façade or industrial structure?
- Are there local code constraints for attachments to building envelopes (movement joints, fire separation, waterproofing)?
Why this matters
- Attachment conditions affect load paths, waterproofing details and future maintenance access. Decisions at procurement time determine who owns risk — the supplier for manufacturing tolerance, the installer for fixing to structure, or the building owner for foundations and loads.
Primary buyer roles and responsibilities
- Architect / Specifier: define architectural carport specification, interface with building aesthetics and cladding.
- Structural Engineer: verify loads, connection detailing and foundation design.
- Procurement / Buyer: confirm aluminium profile selection, finishes, lead times, and contractual acceptance criteria.
- Installer / Contractor: ensure installation readiness and local performance testing.
- Manufacturer / Supplier (e.g., Carportiva): deliver shop drawings, manufacture to spec, and provide factory evidence.
Core decision principle: match design intent to verifiable acceptance criteria
Decision principle statement
- The central procurement principle is: translate design intent into verifiable acceptance criteria that are measurable, testable or auditable at factory, on delivery and after installation. Avoid acceptance by visual inspection alone where structural or service performance is required.
Key acceptance categories
- Structural performance (loads, deflection limits, anchor capacity).
- Water and thermal performance (drainage, thermal bridging, condensation).
- Durability (corrosion resistance, wear points, fastener compatibility).
- Integration readiness (electrification for PV/lighting, roof drainage coordination).
- Fabrication and QA evidence (material certificates, dimensional checks, non-conformance reports).
Evidence-led approach
- Require objective documents and measurements: engineering calculations stamped by a local qualified professional, material mill certificates, fabrication shop measurement reports, and a signed shop drawing review confirming installation readiness.
Relevant standards and guidance
- Use recognized design frameworks such as Eurocodes for structural actions and combinations where applicable [1]. For materials and alloy properties consult The Aluminum Association [2]. Where finish performance is specified, industry standards from the American Architectural Manufacturers Association (AAMA) for coating and finish systems are relevant [3]. For quality management and specified tests, consult ISO series relevant to product data and production control [4].
Planning inputs: site, program, and performance data you must collect before design lock
Essential site data
- Geographical location and coordinates (for wind, snow and seismic zoning).
- Building attachment elevation and elevation-based constraints (movement joints, roof lines).
- Existing structural drawings showing load-bearing capacity at proposed attachment points; as-built surveys if retrofitting.
- Ground conditions near columns for foundation feasibility.
Program and operational data
- Number of bays and parking layout; required clearances for vehicle types (cars, light commercial vehicles, fleet trucks).
- Intended functionality: shading only, weather protection, integrated PV, EV charging or combined.
- Maintenance access and service routes for drain cleaning, PV maintenance, gutter access.
Environmental and local authority constraints
- Local codes for attachments, fire performance for attached structures, and historic district or aesthetic controls.
- Utility restrictions for PV or electrical connection points; required permits and interconnection procedures.
Data capture checklist (for procurement and design kick-off)
- Structural plan excerpt with attachment points and capacity.
- Roof and façade details at attachment line.
- Drainage route and existing rainwater downpipes.
- Electrical single-line diagram if PV or lighting is planned.
- Maintenance strategy and frequency expectations.
Technical specification and interfaces: what to specify in contract documents
Architectural carport specification essentials
- Architectural description: plan, elevation, bay widths, and pitch.
- Profile family and cross-sectional dimensions for primary and secondary members — this is where aluminium profile selection matters.
- Structural loadings and deflection limits (serviceability criteria) with reference to local codes or specified acceptable limits.
- Connection type to building: bolted to structural steel, cast-in anchors, or through-bolted to masonry with isolators.
- Roof finish type (flat, mono-pitch, standing seam), roof material and allowable live maintenance loads.
Material and alloy considerations
- Base alloy and temper for extrusions; corrosion allowance for coastal or industrial environments.
- Surface treatment: powder coat class and film thickness, anodizing class and pretreatment processes.
- Finish and fastener compatibility must be specified to avoid galvanic corrosion where dissimilar metals meet; specify stainless fasteners or isolating washers when in doubt.
Water management and roof drainage coordination
- Define gutter size, downpipe locations and capacity for local design storms; indicate whether carport drainage ties into building rainwater network or has an independent storm system.
- Clarify overflow routes, scuppers and local thresholds.
- For PV: define under-panel drainage paths and mounting details to avoid ponding.
Thermal and acoustic interfaces
- Specify thermal breaks if connectors pass across insulated building envelopes.
- Detail acoustic expectations where carports attach near residential windows or sleeping areas.
Electrical and PV interfaces
- For carports intended to support PV: include electrical loading points, conduit/duct routing, PV mounting interface details and lightning protection strategy.
- Define who supplies modules, inverters and cabling and who is responsible for integration with carport framing.
Shop drawing review and design approval
- Require a formal shop drawing review process where the supplier produces full fabrication drawings, connection details, anchor bolt schedules, and erection sequence plans for sign-off by the AOR and structural engineer. The term shop drawing review should be included as a milestone in the contract.
Example technical specification excerpt (short)
- Primary beams: aluminium extruded profile series X, T6 temper, minimum section modulus Y mm3.
- Coating: polyester powder coat, minimum 60 µm DFT, AAMA 2604-equivalent performance.
- Anchors: stainless steel grade 316 where exposed; isolating washers to be provided where connecting to steel.
Procurement and factory evidence: what to demand before accepting manufacture and delivery
Why factory evidence matters
- Verifiable factory evidence reduces ambiguity at site, shortens installation time, and provides traceability for warranty and maintenance. It also helps show compliance with the architectural carport specification.
Minimum evidence checklist (procurement)
- Material mill certificates for aluminium alloys and temper.
- Coating and pretreatment records (batch numbers, process control data).
- Dimensional inspection reports for critical profiles and sections.
- Welding/assembly records where applicable (including personnel qualifications).
- Torque and pull-test records for anchor assemblies premade in shop or proof tests on sample assemblies.
- Non-conformance reports and corrective actions history for previous production batches (if requested).
- Packaged shop drawings and an assembly/erection manual.
Procurement acceptance table (decision table 1)
| Evidence type | Purpose | Minimum procurement acceptance |
|---|---|---|
| Material mill certificates | Confirm alloy and temper | Signed mill certificate matching lot/heat number |
| Coating process records | Confirm pretreatment & coating | Batch report + thickness measurement (µm) |
| Dimensional inspection | Ensure fit and tolerance | Report with measured dimensions vs. tolerance |
| Shop welding/assembly records | Trace critical joins | Weld procedure spec + welders’ qual. (if applicable) |
| Anchor proof test | Confirm capacity | Load test report or calculation + embed detail |
| Shop drawings | Coordinate installation | Issued-for-construction drawings with sign-offs |
Factory Quality Control expectations
- The factory should operate under documented production control procedures. Where buyer requires, request evidence of systematic QC procedures, inspection points, and acceptance criteria. ISO certification for the factory is useful for process oversight but should not substitute project-specific evidence.
Aluminium profile selection considerations
- Profiles should be chosen for structural adequacy, ease of connection, thermal behavior and aesthetic compatibility. Ensure the selected profiles are available in required finishes and that tooling lead times are acceptable.
Two-tier acceptance strategy
- Pre-production: approve sample profiles, coated sample panels, and stamped shop drawings.
- Post-production: accept batch evidence and dimensional reports; perform joint factory acceptance testing if critical.
Interface management on site: installation readiness and role clarity
Installation readiness
- Confirm that the site has been prepared: foundation castings or anchor boxes in place, utility routes open, access scaffolding or lifts booked and inspection points scheduled.
- Installation readiness must be a formal milestone that includes signed-off pre-install checklists by installer and client representative.
On-site interface checklist
- Confirm building-mounted connections are accessible and match the shop drawing locations.
- Confirm roof/wall penetrations and flashing details have been completed or will be completed in the same sequence as installation.
- Confirm deliveries and storage protection for extrusions, coated panels and fasteners to avoid damage and contamination.
Finish and fastener compatibility on site
- Verify that the actual fasteners on site are the specified types (material grade, coating) and that any washers or isolation pads are present where connecting to dissimilar metals.
- In coastal or chemically aggressive atmospheres, confirm additional protection or sacrificial measures as specified in contract.
Installation sequencing and tolerances
- Define acceptable dimensional tolerances for holes and anchorage positions on site. When tolerances are tight, plan to allow for field-adjustment brackets or shims and specify them in shop drawings.
- Erection sequence must be coordinated with building occupants for safety, and with trades that need sequencing (glazing, waterproofing trades).
Installation readiness table (decision table 2)
| Item | Responsible party | Acceptable evidence for “installation readiness” |
|---|---|---|
| Foundations/anchors set | Structural contractor / civil works | As-built foundation survey + anchor positions within tolerance |
| Building attachment prepared | Building contractor | Signed interface checklist + waterproofing access |
| Materials on site & protected | Supplier/installer | Delivery dockets + condition report |
| Lifting & access booked | Installer | Crane/lift permit and schedule |
| Electrical/PV preworks | Electrical contractor | Conduit positions and pull-boxes installed |
| Shop drawing approvals | AOR / Structural engineer | Signed shop drawings and stamped calculations |
Special note: installation readiness includes a safety plan and sequence of temporary bracing for wind uplift and partial loading during erection.
Implementation risks and how to mitigate them
Common procurement and implementation risks
- Mismatch between shop drawings and as-built conditions.
- Delays due to long lead items (special extrusions, custom finishes).
- Corrosion failures due to improper fastener/finish combinations.
- Water ingress at attachment points or inadequate roof drainage.
- Unresolved electrical or PV interfaces causing delays or additional work.
- Permit or utility interconnection delays.
Risk mitigation strategies
- Early site survey: invest in an accurate as-built survey and laser scan where tolerances are critical.
- Early engagement of structural engineer: get connection design early to prevent late redesigns.
- Standardize profiles where possible: reduces tooling lead time and simplifies spare parts.
- Define acceptance criteria in contracts: include clear hold points for shop drawing approval and factory acceptance.
- Specify pre-delivery mock-up: for complex junctions, a small pre-production mock-up can expose issues early.
- Require finish and fastener compatibility statements from suppliers: require material compatibility analysis.
- Schedule float and lead-time buffers: explicitly include procurement buffers in the program.
Insurance and contractual measures
- Ensure scope of responsibility across connected trades is explicitly documented in contract. For example, if water ingress occurs at building penetration, clearly state which party is accountable.
- Consider staged payments tied to verifiable milestones (shop drawing acceptance, factory inspection, delivery, final sign-off).
Documented risk register
- Maintain a live project risk register with owners and mitigation actions; link to procurement milestones and acceptance criteria.
Procurement contracts and warranties: what to specify and verify
Contractual clauses to include
- Clear scope with excluded items (e.g., foundations, electrical tie-in).
- Reference to accepted shop drawings and installation readiness checklists as contractual documents.
- Material traceability obligation — supplier must provide mill certificates and coating batch records.
- Lead time commitments with agreed remedies or schedule liquidated damages where appropriate.
- Performance warranty with defined start date — clarify if warranty begins on delivery, completion, or after commissioning.
- Spare parts and maintenance kit supply terms (recommended for inaccessible or integrated PV systems).
Warranties and limitations
- Warranties should be specific about surface finishes, structural integrity and load-bearing capacity under defined load cases. Avoid generic language; tie claims to documented maintenance practices and environmental expectations.
- State explicitly that warranty for attachment to building is subject to correct installation and that site-specific structural capacity and foundations must be verified by local engineers.
Quality acceptance and handover
- Define final acceptance tests, such as water testing of drainage, torque checks on critical fasteners, and electrical continuity tests for PV-integrated installations.
- Include a defect liability period and a process for issuing and closing snags.
Regulatory compliance and third-party approvals
- Require supplier declarations of conformity with local regulatory requirements where appropriate (for example, material composition declarations).
- Where national codes apply, specify the code edition used (e.g., applicable Eurocode parts) and require stamped calculations [1].
Six-step buyer workflow for attached aluminium carport design (named workflow)
"Confirm, Specify, Validate, Procure, Inspect, Handover" — a practical six-step workflow
- Confirm (Project basis and site verification)
- Collate site data: as-built drawings, structural capacity, permits and utility conditions.
- Confirm project objectives: capacity, PV requirements, aesthetic constraints.
- Specify (Technical and contractual requirements)
- Produce architectural carport specification and include aluminium profile selection, finishes and finish and fastener compatibility clauses.
- Define shop drawing review milestones and installation readiness criteria.
- Validate (Engineering and regulatory approval)
- Obtain engineering calculations with local professional stamp; validate attachment detail and deflection limits against codes [1].
- Confirm drainage and electrical integration plans with relevant local authorities and utilities.
- Procure (Tender/Order and factory evidence)
- Issue tender with evidence checklist; evaluate offers on both technical compliance and production quality evidence.
- Secure production dates and agreed acceptance tests.
- Inspect (Factory acceptance and pre-delivery)
- Perform or commission factory inspections for material certificates, coating records and dimensional checks.
- Approve packaging and transport strategy for sensitive components.
- Handover (Installation, commissioning and maintenance)
- Confirm installation readiness, perform commissioning (drainage, PV electrical interconnection tests) and issue final acceptance.
- Provide maintenance schedule and spare parts list.
Each step must generate documented outputs that become contractual references (e.g., signed shop drawings, factory acceptance certificates, installation readiness checklist).
Site installation and operations: execution detail to avoid common failures
Erection safety and temporary works
- Define temporary bracing for wind uplift and partial loads during erection. Attachments to partially-complete buildings can be vulnerable to uplift and should be addressed in temporary works drawings.
- Use certified lifting equipment and define load paths during lifting and placement.
Anchorage and tolerance recovery
- Provide adjustable anchor brackets or slotted connections to absorb site positional variances. Include spares and provision for field-welding if permitted.
Waterproofing and flashing
- Ensure flashings and sealants are specified with compatible substrates and UV-resistant properties. Roof-to-wall junctions need tested or proven flashings and integration with building membranes.
Operations and maintenance
- Define a maintenance schedule for gutter cleaning, finish inspection and fastener torque checks.
- For PV installations: define panel washing frequency, inverter service intervals and module replacement strategy.
Spare parts and lifecycle planning
- Maintain a list of spare extrusions, specialized fasteners and coating touch-up kits. Where custom profiles are used, document tooling references to enable re-order.
Installation readiness reminder
- Reiterate: installation readiness should be signed off by all parties before arrival of site-critical components; this reduces waiting-on-site time and avoids partial erections that increase risk.
Frequently Asked Questions (FAQ)
Q: How do I select the right aluminium profiles for a carport? A: Aluminium profile selection should be based on structural calculations (load and span), thermal behavior (for connections across thermally insulated facades) and aesthetic requirements. Profiles should be specified as family series with cross-section dimensions, alloy and temper. Request supplier dimensional inspection records and manufacturing capabilities.
Q: Who is responsible for drainage when a carport is attached to a building? A: Responsibility must be defined in the contract. If the carport ties into the building stormwater system, coordination with the building team and utilities is required. roof drainage coordination is a critical interface and must be resolved before fabrication.
Q: What should I demand in the shop drawing review? A: Require full fabrication drawings, erection sequence, anchorage details with bolt schedule, interfaces with building membranes and penetrations, and a signed shop drawing review from the AOR and structural engineer.
Q: Are powder coatings durable enough for coastal sites? A: Powder coatings can perform well if the system and application process are appropriate. For highly aggressive environments, consider anodizing or higher-category coatings and ensure finish and fastener compatibility to prevent galvanic corrosion. Ask for process records and environmental performance data from the supplier.
Q: What level of factory evidence is reasonable to require? A: At minimum: mill certificates, batch coating reports, dimensional inspection reports and shop drawings. For critical projects, request factory acceptance tests and photographs of assembly jigs.
Q: Can carports be pre-assembled and lifted into place? A: Yes, where logistics and lifting capacity permit. Pre-assembly reduces on-site works but increases risk if site tolerances aren’t met. Ensure shop drawing review and installation readiness are confirmed before prefabricated modules are shipped.
Q: How do we manage warranties across parties? A: Separate warranties (manufacture, coating, installation, PV equipment) should be detailed and begin on clearly defined milestones. Ensure that performance warranties reference correct maintenance obligations and do not transfer responsibilities ambiguously.
Implementation checklist: minimum documents and sign-offs before manufacturing
- Confirmed and signed project basis (scope, functional requirements, site data).
- Site survey or as-built drawings with attachment points annotated.
- Stamped structural calculations for connections and member sizing.
- Architectural carport specification with aluminium profile selection and finish and fastener compatibility clauses.
- Signed shop drawings and issuance for fabrication.
- Factory QA evidence packet: mill certificates, coating records, dimensional reports.
- Installation readiness checklist signed by installer and client.
- Permits and utility approvals for PV/electrical works where applicable.
Important legal/technical note
- Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities. The supplier’s scope should be written to reflect these dependencies.
Decision tables and procurement comparisons
Design priority decision table (decision table 3)
| Priority scenario | Suitable design focus | Comments |
|---|---|---|
| Aesthetic integration with façade | Use slim profiles with concealed fixings; coordinate colours | Requires precise shop drawing review and tight tolerances |
| PV-first approach (max yield) | Maximise roof pitch and unobstructed module layout; robust mounting rails | Electrical integration must be defined early; roof drainage coordination critical |
| Fast procurement and installation | Standard profiles, factory pre-assembly, simplified finishes | May limit bespoke aesthetics; ensure site tolerances can accept pre-assembled units |
| Long-term durability in coastal site | Specify anodized or high-performance coatings; stainless fasteners | Higher initial cost but lower life-cycle maintenance costs |
| Low maintenance / fleet operations | Robust gutters, accessible inspection points, durable finishes | Consider sacrificial sacrificial sacrificial elements or easily replaceable panels |
Note: The above table should be used as a decision aid; project-specific structural verification remains mandatory.
Procurement evidence acceptance table (decision table 4)
| Document | Accept / Conditional Accept | Reject criteria |
|---|---|---|
| Mill certificate | Accept if matches lot/heat | Missing lot info or mismatch with material marking |
| Coating batch report | Accept if process parameters within spec | Absent film thickness data or no pretreatment record |
| Dimensional inspection | Accept if measurements within tolerances | Variances beyond specified tolerance without mitigation plan |
| Anchor proof test report | Accept if meets design load | Failure or missing test date and responsible party |
| Shop drawings | Accept with engineer sign-off | Missing connection details or inconsistent dimensions |
| Factory QA procedure | Conditional accept | No documented inspection points or traceability |
Mid-article action (CTA)
If you need a project-specific review of attached aluminium carport design details — shop drawing review, aluminium profile selection advice, or factory evidence assessment — request a technical inquiry with our team here: /inquiry. For reference on residential-focused applications, see the NordFlat architectural villa system.
Frequently referenced standards and guidance
- Structural design and load combinations should be referenced to national codes and recognized frameworks such as Eurocodes where applicable [1].
- Material properties and aluminium design guidance are available from The Aluminum Association and similar national aluminium bodies [2].
- Coating and fenestration finish performance guidance can be referenced from standards published by AAMA where relevant to the project region [3].
- For product conformity and specified tests, consult the ISO Online Browsing Platform for relevant standards and test methods [4].
Conclusion: prioritize measurable commitments over assumptions
An attached aluminium carport design is an architectural system with multiple technical interfaces. The buyer’s primary task is to convert design intent into measurable, auditable procurement and installation milestones. That means specifying clear acceptance criteria (material certificates, shop drawings, factory evidence), resolving roof drainage coordination and electrical interfaces early, and ensuring finish and fastener compatibility. Use a structured workflow (Confirm, Specify, Validate, Procure, Inspect, Handover) and insist on documented installation readiness before delivery. For tailored systems and procurement support, review Carportiva’s all systems and our sourcing guides, and contact us to start a project discussion.
For project-specific inquiries about attached aluminium carport design, procurement evidence, shop drawing review or installation readiness, contact us: /inquiry or info@carportiva.com.
Important reminder: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
References
- European Commission Eurocodes: https://eurocodes.jrc.ec.europa.eu/
- The Aluminum Association: https://www.aluminum.org/
- American Architectural Manufacturers Association: https://aamanet.org/
- ISO Online Browsing Platform: https://www.iso.org/obp/ui/
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion