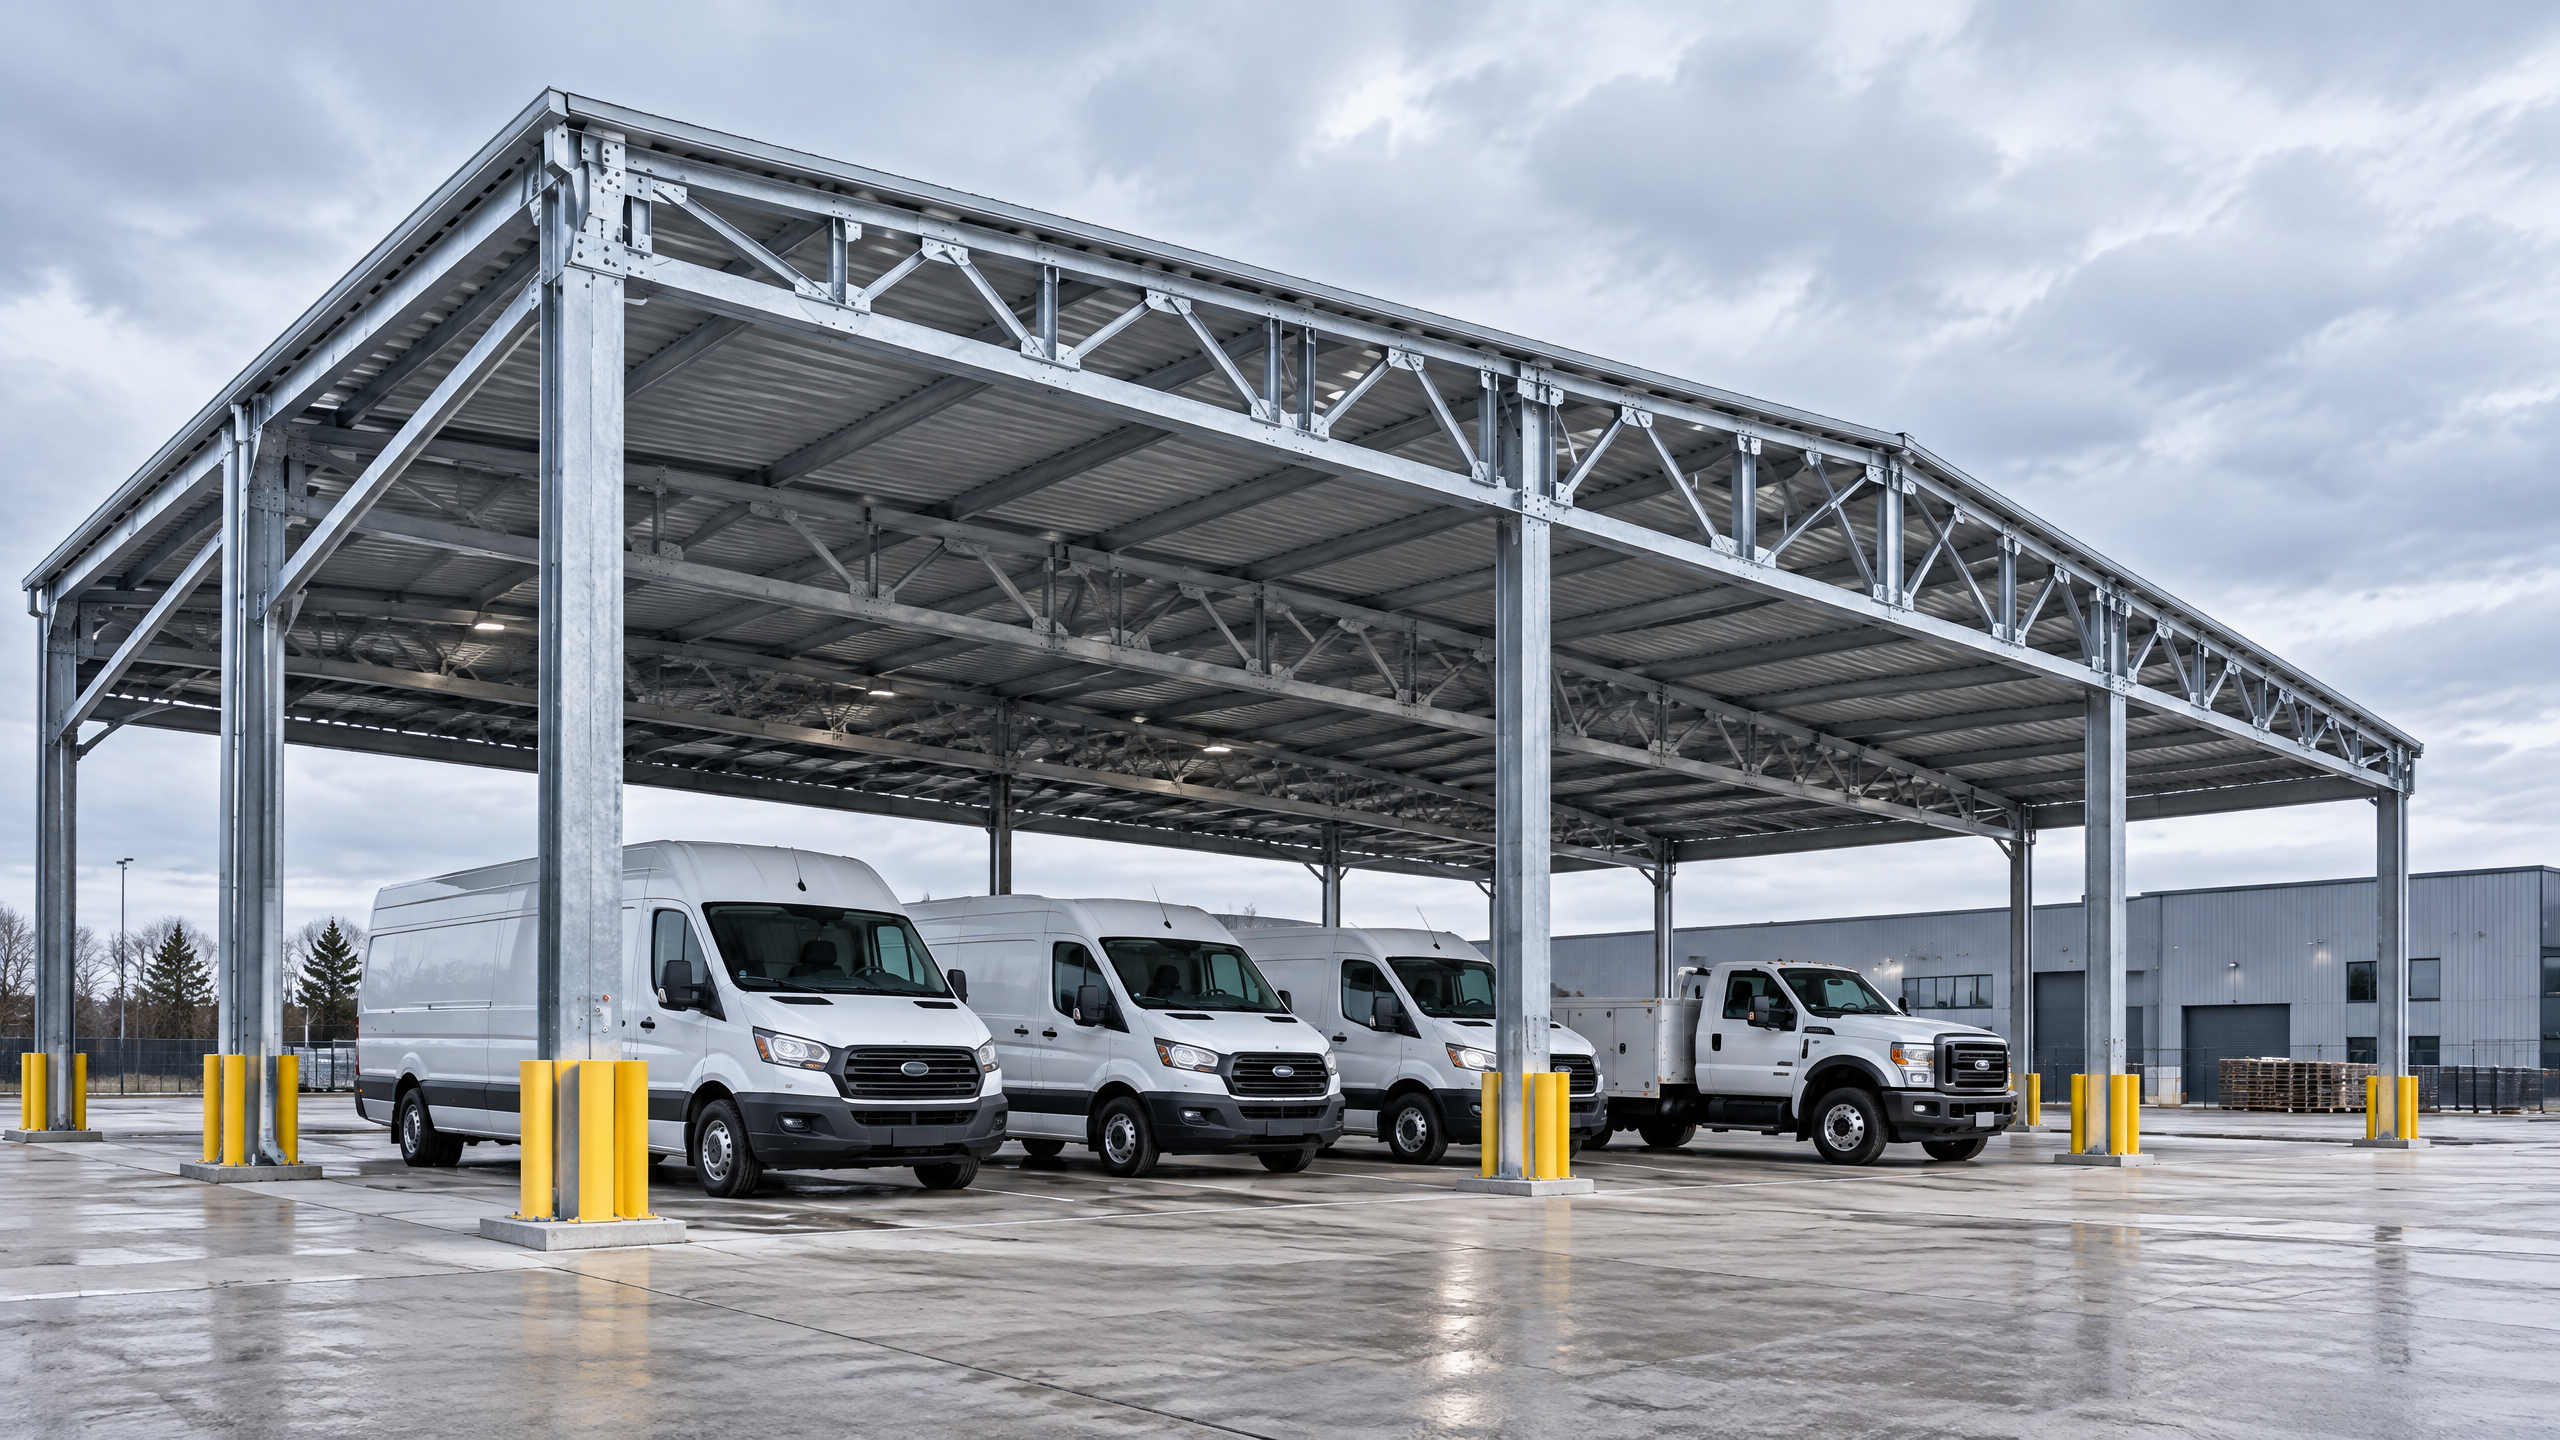
Answer: Assessing industrial carport manufacturer factory capability is a structured, evidence-led process that matches your project’s technical scope, timeline and risk appetite to what a supplier can reproducibly deliver. Start by defining the required product families (architectural aluminium canopies, commercial solar carports, industrial/fleet shelters), the site and electrical interfaces, and the acceptance criteria for materials, finishes and installation. Then use a targeted B2B supplier due diligence checklist to verify factory capacity, staff skills, documented quality systems, traceable material certificates and factory quality documentation, plus outbound logistics and export packing coordination. Validate these with witnessed inspections or third‑party audits and lock responsibilities into a delivery responsibility matrix and contract terms that support your project procurement controls. Site-specific items—structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty—must be resolved on a documented project basis with local qualified professionals, installers, utilities and authorities before final sign-off.
Buyer context and scope boundary: what “industrial carport manufacturer factory capability” must cover
Why define factory capability?
- It focuses the procurement team on measurable supplier outputs (finished modules, sub-assemblies, protective finishes, packaging and documentation) rather than vague commercial promises.
- It separates what must be produced in-factory from site responsibilities (foundations, on-site electrical wiring, PV installation if applicable), reducing interface risk.
What capability elements to include in the scope boundary
- Product range and modularity: single-span canopies, multi-bay industrial carports, integrated solar racking, drive-through shelters, and bespoke architectural variations.
- Production outputs: metal fabrication (cutting, CNC, press braking), structural welding, bolted assembly, powder coating or anodizing logistics, pre-assembly for shipping.
- Quality assurance outputs: inspection records, non-conformance reports, material traceability, and factory test procedures.
- Logistics and packaging: unitized packing for sea/air freight, skid/blocking and bracing, markings for customs.
- Aftermarket support: spare parts provisioning, replacement components, long-term maintenance documentation.
Scope boundary decisions that buyers must make
- Define which items are factory-delivered “fit‑for‑installation” versus “factory-supplied but site-finished” (for example, painted vs. field-painted cut edges, or PV modules supplied by EPC).
- Establish who owns the structural interface: supplier provides baseplates and anchor layout, or buyer supplies as-built foundation drawings and carries foundation risk.
- Decide whether the supplier’s factory will assemble canopy frames into installable modules or ship knocked-down kits.
Reminder: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Core decision principle: capability must be proven, repeatable and contractually enforced
Primary criterion
- Can the factory repeatably manufacture the specific assemblies you require, at the tolerances, finishes and volumes needed, within your required schedule and with a clear allocation of responsibilities?
How to test that criterion
- Evidence over assertion: require factory plans, flow diagrams, staff-role descriptions, and recent production records for comparable builds.
- Repeatability: look for jigs, fixtures and controlled processes that reduce reliance on individual craft skill.
- Contract enforceability: ensure factory obligations — tolerances, coatings, inspection steps, packing, documentation, and delivery milestones — are written into commercial and technical attachments.
Decision thresholds (examples)
- Single or small-run projects: prioritize factory flexibility and documented procedures to avoid one-off workmanship errors.
- Volume roll-outs: prioritize throughput, cycle-time data, quality-control sampling plans and capacity buffers.
Core trade-offs buyers accept
- Speed vs. customization: highly customized architectural carports typically require longer lead time and closer factory supervision.
- Price vs. traceability: lower-cost suppliers may lack material traceability and may be higher risk for long-term warranties.
Planning inputs — the data the buyer must provide before assessing factories
Accurate and complete planning inputs materially reduce procurement risk. Provide the factory with the following documented items as a minimum:
- Project brief and acceptance criteria
- Scope (type and quantity of carports).
- Finish standards, corrosion class and environmental exposure.
- Acceptance tolerances and test requirements (e.g., bolted joint torque checks, weld inspections).
- Site data
- Geotechnical report or foundation design parameters (bearing capacity, frost depth).
- CAD/site survey with obstacle clearance, layout grid and drainage constraints.
- Local snow, wind and seismic design loads, or reference to local codes.
- Electrical and PV interfaces (when applicable)
- PV module layout, stringing plan, inverter locations and DC/AC interfaces.
- Local utility interconnection requirements.
- Logistics and delivery constraints
- Access restrictions, maximum vehicle length/weight, crane access, staging areas.
- Customs/regulatory constraints for imported assemblies.
- Schedule constraints
- Fixed milestones such as tenant move-in dates, incentive deadlines for PV, or construction schedules.
- Commercial boundaries
- Agreed Incoterm (see delivery responsibilities), warranty start points, and acceptance process.
Note: Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Technical specification and interfaces: what to compare and document
An evidence-led technical scope comparison between buyer requirements and factory capabilities reduces surprises. Include the following categories:
- Structural design and load capacity
- Verify factory capacity to produce sections sized for your design loads and fabrication tolerances. Confirm connection design standardization for faster installation.
- Materials and coatings
- Specify aluminium grade, fastener materials (stainless steel grades), and corrosion protection system. For hot-dip galvanizing or zinc-coated steels, reference accepted practice and inspection criteria (see galvanizing guidance) [1].
- Welding and fabrication standards
- Require welding procedure specifications (WPS), qualified welders, and inspection plans. Confirm non‑destructive testing (NDT) requirements where critical.
- Surface treatment
- Powder coating or anodizing process control, film thickness targets, adhesion test methods, and cure documentation.
- Pre-assembly and modularization
- What assemblies come pre-assembled? Are bolted sub-frames supplied as drop-in modules to speed site installation?
- Electrical and PV mounting interfaces
- Supply mechanical mounting details for PV racking (rail interfaces, module clamps, earthing). Ensure compatibility with PV module type and inverter locations.
- Tolerances and fit-up
- Define allowable cumulative tolerances for bay-to-bay alignment, anchor hole location, and verticality.
- Documentation deliverables
- Shop drawings, bill of materials (BOM), material test certificates (MTC), mill test reports, assembly instructions, torque schedules, and maintenance manuals.
Use a technical scope comparison table to make responsibilities and acceptance clear.
Technical scope comparison
| Item / Interface | Buyer-specified requirement | Factory responsibility (deliverable) | Site responsibility |
|---|---|---|---|
| Structural columns & beams | Design loads, tolerances, baseplate size | Fabrication to shop drawings; MTCs; welding records | Grouted baseplate and anchor bolts; leveling |
| Surface finish | Corrosion class and color code | Pre-treatment, powder coat, cure records, QC inspection | Touch-up of minor field damage |
| PV mounting rails | Module type & clamping detail | Supply rails with pre-drilled holes; earthing points | PV module installation, string wiring |
| Foundation interface | Anchor bolt pattern & embed depth | Baseplate drilling templates; anchor templates | Cast-in anchors or epoxy anchors (by local contractor) |
| Packing & export | Export packing specification | Unitized packing, blocking/bracing, packing list | Inland transfer from port; customs clearance |
Include the exact phrase "technical scope comparison" in procurement documentation and use it as a checklist item in RFPs and supplier scoring matrices.
Procurement, factory evidence and logistics: checklists, documents and verifications
A disciplined procurement process looks for specific documentary evidence and on-site/third-party verifications before awarding contracts. Adopt a tiered evidence approach depending on project risk and value.
Minimum factory evidence set (for all purchases)
- Company registration and address verification.
- Facility photos and production flow diagrams.
- List of relevant projects (references) – verify with the listed customers.
- Basic QA procedures and inspection points.
Enhanced factory evidence set (recommended for medium to large projects)
- Factory quality documentation: ISO/QMS certificates or documented quality plans, internal audit reports, and sample inspection records.
- Material test certificates and mill test reports (MTCs) for structural alloys and fasteners.
- Welding Procedure Specifications (WPS) and welder qualification records.
- Paint/coating technical data sheets (TDS), batch/lot traceability.
- Production capacity graphs and planned lead time data.
Highest-risk projects or multi-site rollouts
- Third-party factory audit or witnessed production runs.
- Pre-shipment inspection (PSI) and hold points.
- Sample production prototype review and destructive/non-destructive testing plans.
Decision table: Factory evidence tiering
| Risk/Value tier | Documents & verification required | Typical verification method |
|---|---|---|
| Low (small, low-value) | Basic documents: facility photos, basic QA, references | Remote document review; supplier call |
| Medium (single large site) | Factory quality documentation; MTCs; WPS; sample inspection | Document review + sample witness inspection |
| High (multi-site or warranty-critical) | Third-party factory audit; PSI with hold points; traceability | On-site audit or accredited inspector; agreed test programs |
B2B supplier due diligence
- Financial stability: trade references, bank references where appropriate.
- Corporate governance and compliance: anti-bribery policies, export controls.
- Insurance: product liability and transport insurance coverage.
Factory quality documentation
- Ask for a factory’s quality plan with defined inspection hold points, non-conformance handling, calibration records for gauges and CMM (if used), and traceability from raw material batch to shipped assembly. This is essential for warranty support and long-term maintenance.
Export packing coordination
- Define packaging units (per-bay, per-frame), dunnage requirements, blocking & bracing standards for sea freight, desiccant requirements for humid routes, and labelling. Ensure a packing list and cargo weight/volume data are provided.
- For cross-border shipments, confirm export documentation requirements (commercial invoice, packing list, bill of lading, certificates of origin) and align with your customs broker. Where relevant, consult documented export/import guidance for the destination country [4].
Delivery responsibilities and Incoterms
- Select an Incoterm that matches your capability and risk appetite and then populate a delivery responsibility matrix that lists who is responsible for packing, export clearance, carriage, insurance and import clearance [3].
- Ensure the contract links Incoterm obligations to quality hold points and acceptance criteria.
Delivery responsibility matrix (example)
| Responsibility | EXW (Factory) | FOB (Port of export) | CFR / CPT | DAP / DDP |
|---|---|---|---|---|
| Packaging & export packing coordination | Supplier | Supplier | Supplier | Supplier |
| Export customs clearance | Buyer | Supplier | Supplier | Supplier |
| Inland carriage to export port | Buyer | Supplier | Supplier | Supplier |
| Sea carriage & insurance | Buyer | Buyer (insurance optional) | Supplier (carriage) / Buyer insurance optional | Supplier |
| Import customs clearance | Buyer | Buyer | Buyer | Supplier (if DDP) |
| Unloading at site & local delivery | Buyer | Buyer | Buyer | Supplier or Buyer per agreement |
Note: Use the delivery responsibility matrix above as a template. Always align the agreed Incoterm with documentary handover points, insurance and responsibility for damage in transit [3].
Regulatory documents and customs
- For exports, confirm the required certificates (origin, conformity) and packaging/label requirements for the destination market. The buyer’s customs broker should be engaged early; CBP and other authorities publish general import guidance that can inform documentation needs [4].
Reference standards and technical norms
- Use ISO standards to structure QMS and testing where applicable (e.g., ISO 9001 for quality systems) and refer to galvanizing or coating standards for corrosion protection cases [2][1].
Mid-article CTA: If you want a factory evidence checklist tailored to your project, raise a formal request via /inquiry.
Site installation, commissioning and operations: factory-to-site handover
Clear factory outputs and site inputs reduce interface failures. Define these categories in the contract and acceptance plan:
Factory-delivered items
- Shop drawings for all shipped assemblies.
- Pre-assembled modules or kits, clearly labelled with part numbers and assembly sequences.
- Hardware kits (bolts, washers, sealing gaskets) in sealed bags with torque schedules.
- Installation drawings and torque/sequencing checklists.
- Certificates and test reports required for handover.
Buyer/site-delivered inputs
- Foundations per agreed basis (cast-in anchor setting, tolerance confirmation).
- Lifting equipment and qualified rigging crew.
- Local electrical contractors for PV/electrical connections.
- Local authorities’ permits and inspections.
Commissioning and acceptance
- Define factory hold points: dimensional check, dry-fit assembly, bolting torque verification, and final acceptance.
- Agree acceptance tests (alignment, verticality, mechanical fastening torque, PV commissioning tests if applicable).
- Record acceptance with signed handover certificates and generate as-built drawings and spare parts lists.
Operations and maintenance
- Require suppliers to submit an operation and maintenance manual with spare parts identification, recommended inspection intervals, and corrosion repair instructions.
- Make spare parts availability and lead times a contractual KPI for multi-site fleets.
Warranty handover
- Clarify when warranty starts (date of practical completion, provisional acceptance, or commissioning). Include the exact triggers in the contract and ensure the factory provides warranty certificates tied to serial numbers or batch numbers where practicable.
Reminder: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Implementation risk register: common failure modes and mitigations
A focused risk register aligned to factory capability helps buyers prioritize checks. Below are typical risks, indicators, and mitigations.
Risk: Incomplete or poor documentation
- Indicator: Missing MTCs or inconsistent BOMs.
- Mitigation: Hold final payment until complete documentation is delivered; require traceability as a contract clause.
Risk: Surface coating failure (early corrosion, peeling)
- Indicator: Inconsistent film thickness records, lack of pre-treatment documentation.
- Mitigation: Require coating TDS, cure records, and adhesion test results; specify visual acceptance criteria and repair procedure.
Risk: Dimensional mismatch on site
- Indicator: No templates or jigs; insufficient tolerance specification.
- Mitigation: Request factory templates, drill guides, or pre-assembled frames where possible; add site trial-fit hold point.
Risk: Packing damage in transit
- Indicator: Loose components, palletization not specified.
- Mitigation: Define export packing coordination requirements; use unitized containers with blocking/bracing and external markings.
Risk: Customs or documentation delay
- Indicator: Missing certificates of origin, incorrect commodity codes.
- Mitigation: Engage customs broker early; align packing lists to customs invoices and coordinate export documentation handover.
Risk: Installer skills mismatch
- Indicator: Factory relies on specific assembly procedures not known to local contractors.
- Mitigation: Require supplier to provide installation supervision or nominate approved installers for initial commissioning.
Risk: Long-term spare parts unavailability
- Indicator: No spare parts plan or single-supplier proprietary items.
- Mitigation: Lock parts lead times and MOQ in contract; require BOM for spares and interchangeability notes.
Contractual and commercial mitigations
- Link payments to verifiable milestones and documentation delivery.
- Include liquidated damages or schedule penalties where appropriate for critical-path deliveries.
- Define acceptance and warranty triggers clearly.
Project procurement controls
- Establish a single source of truth (shared document repository), clear version control for drawings and a change order process. Require supplier to participate in periodic project procurement controls reviews and change management meetings.
A named, six-step buyer workflow for evaluating industrial carport manufacturer factory capability
This workflow is a practical sequence to follow for procurement teams. Name it the CARPORT FIVE+1 workflow (Configure, Assess, Request, Prototype, Observe, Transfer). Each step describes actions and deliverables.
- Configure: Define project basis and acceptance criteria
- Deliverables: Project brief, site data package, design loads, interface drawings.
- Action: Engage structural and electrical consultants to prepare the documented project basis. (Reminder: local professionals must confirm foundations, permits, approvals.)
- Assess: Market screening and B2B supplier due diligence
- Deliverables: Shortlist (3–5 suppliers), financial & compliance checks, factory capability questionnaire.
- Action: Use a standardized supplier questionnaire that asks for factory floor plans, production capacity, QA certificates, and references.
- Request: Issue technical RFP with technical scope comparison template
- Deliverables: RFP that includes the technical scope comparison table, delivery milestones, packing requirements, and acceptance criteria.
- Action: Require complete BOM, MTCs, WPS, lead times, and proposed Incoterms in proposals.
- Prototype: Approve sample/prototype and witness verification
- Deliverables: Prototype piece, inspection reports, non-conformance resolution plan.
- Action: For new or bespoke systems, run a build-off or prototype approval as a contractual milestone.
- Observe: Factory validation, pre-shipment inspection and logistics planning
- Deliverables: Factory audit report, PSI findings, packing plan and export paperwork checklist.
- Action: Conduct onsite or third-party audit; coordinate export packing coordination and delivery responsibility matrix prior to shipment.
- Transfer: Delivery, installation, commissioning and transition to operations
- Deliverables: As-built documentation, spare part lists, maintenance manual, signed acceptance certificates.
- Action: Supervise first installation with supplier or approved installer, collect punch-list items, confirm warranty paperwork.
Link resources: For integrated logistics planning see Titan industrial and logistics system and review configuration options across all systems to align module sizes with transport constraints. For procurement templates and checklists consult sourcing guides.
Frequently Asked Questions (FAQ)
Q: How do I verify a supplier’s claimed production capacity? A: Ask for verifiable indicators: production floor layout, process cycle times, recent production records for comparable assemblies (with customer references), and a capacity plan showing maximum weekly/monthly output. For high-value projects, consider a factory tour or third-party capacity audit.
Q: What documents should I require before shipping? A: Minimum: packing list, commercial invoice, bill of lading, material test certificates, shop drawings, installation instructions, and any certificates of conformity required by the destination regulator. For international shipments ensure export packing coordination and customs documents are confirmed.
Q: Should I demand ISO certification? A: ISO 9001 (quality management) is useful as an indicator of systematic processes but is not a substitute for project‑specific factory quality documentation. Use ISO certification as one element among material traceability, WPS, and inspection records [2].
Q: How do I decide on the right Incoterm? A: Select an Incoterm that matches your capability to manage inland transport and customs. If you want the supplier to manage export and sea carriage but not import risks, FOB or CFR/CPT can be suitable. If you prefer minimal logistics involvement, DAP or DDP may be better — but DDP places clear import and customs responsibility on the supplier and should be priced accordingly [3].
Q: Who is responsible if rust appears after 18 months? A: Responsibility depends on the contract, acceptance criteria and documented coatings process. Ensure factory provides coating TDS, cure records and inspection records as part of factory quality documentation; define warranty terms and start date. For long-term corrosion prevention, base the specification on recognized practices, and verify pre-delivery inspection records.
Q: How to handle multiple shipments and assembly at site? A: Use sequenced packing lists, consistent labelling, and delivery schedules aligned to site installation windows. Ensure the factory’s export packing coordination covers unitization so partial deliveries remain organized.
Q: Do I need pre-assembly at factory? A: Pre-assembly reduces on-site time and alignment errors but increases packing size and may complicate transport. Use the technical scope comparison to weigh the benefit: where site access is limited or labor is constrained, factory pre-assembly often saves overall project time.
Q: Can Carportiva provide installation supervision? A: For specific arrangements, contact Carportiva via /inquiry or info@carportiva.com to discuss installers, supervision options, or to align factory scope with local installer capability.
Practical checklist: documents to require in the contract appendix
- Project brief and site data annex.
- Shop drawings and list of transferrable drawings for as-built package.
- Material test certificates (MTCs) and batch traceability.
- Welding Procedure Specifications (WPS) and welder qualification certificates.
- Paint/coating TDS, process logs and cure records.
- Factory quality documentation and inspection schedules.
- Pre-shipment inspection plan and hold points.
- Packing list, unitization scheme, and export packing coordination plan.
- Agreed Incoterm and delivery responsibility matrix mapping each responsibility.
- Spare parts list with lead times and recommended spares.
- Warranty certificates and start date definitions.
- Acceptance and handover forms tied to milestones.
Conclusion: making capability the core procurement filter
When industrial carport manufacturer factory capability is the primary procurement filter, buyers can turn a technically complex supply chain into a series of verifiable milestones. Your procurement strategy should combine:
- A clear, documented project basis prepared with local qualified professionals to address site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty.
- A rigorous B2B supplier due diligence program and a technical scope comparison built into the RFP.
- A demand for factory quality documentation and agreed pre-shipment inspections.
- A delivery responsibility matrix and explicit export packing coordination tied to Incoterm-based contractual obligations.
- Project procurement controls that make documentation, inspections and milestones a payment and acceptance trigger.
If you want a tailored evaluation or a factory evidence checklist aligned with Carportiva product families, contact us via info@carportiva.com. We can also discuss system sizing and logistics integration using Titan industrial and logistics system and mapping across our all systems. For procurement templates and deeper sourcing advice see our sourcing guides.
Final reminder: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion