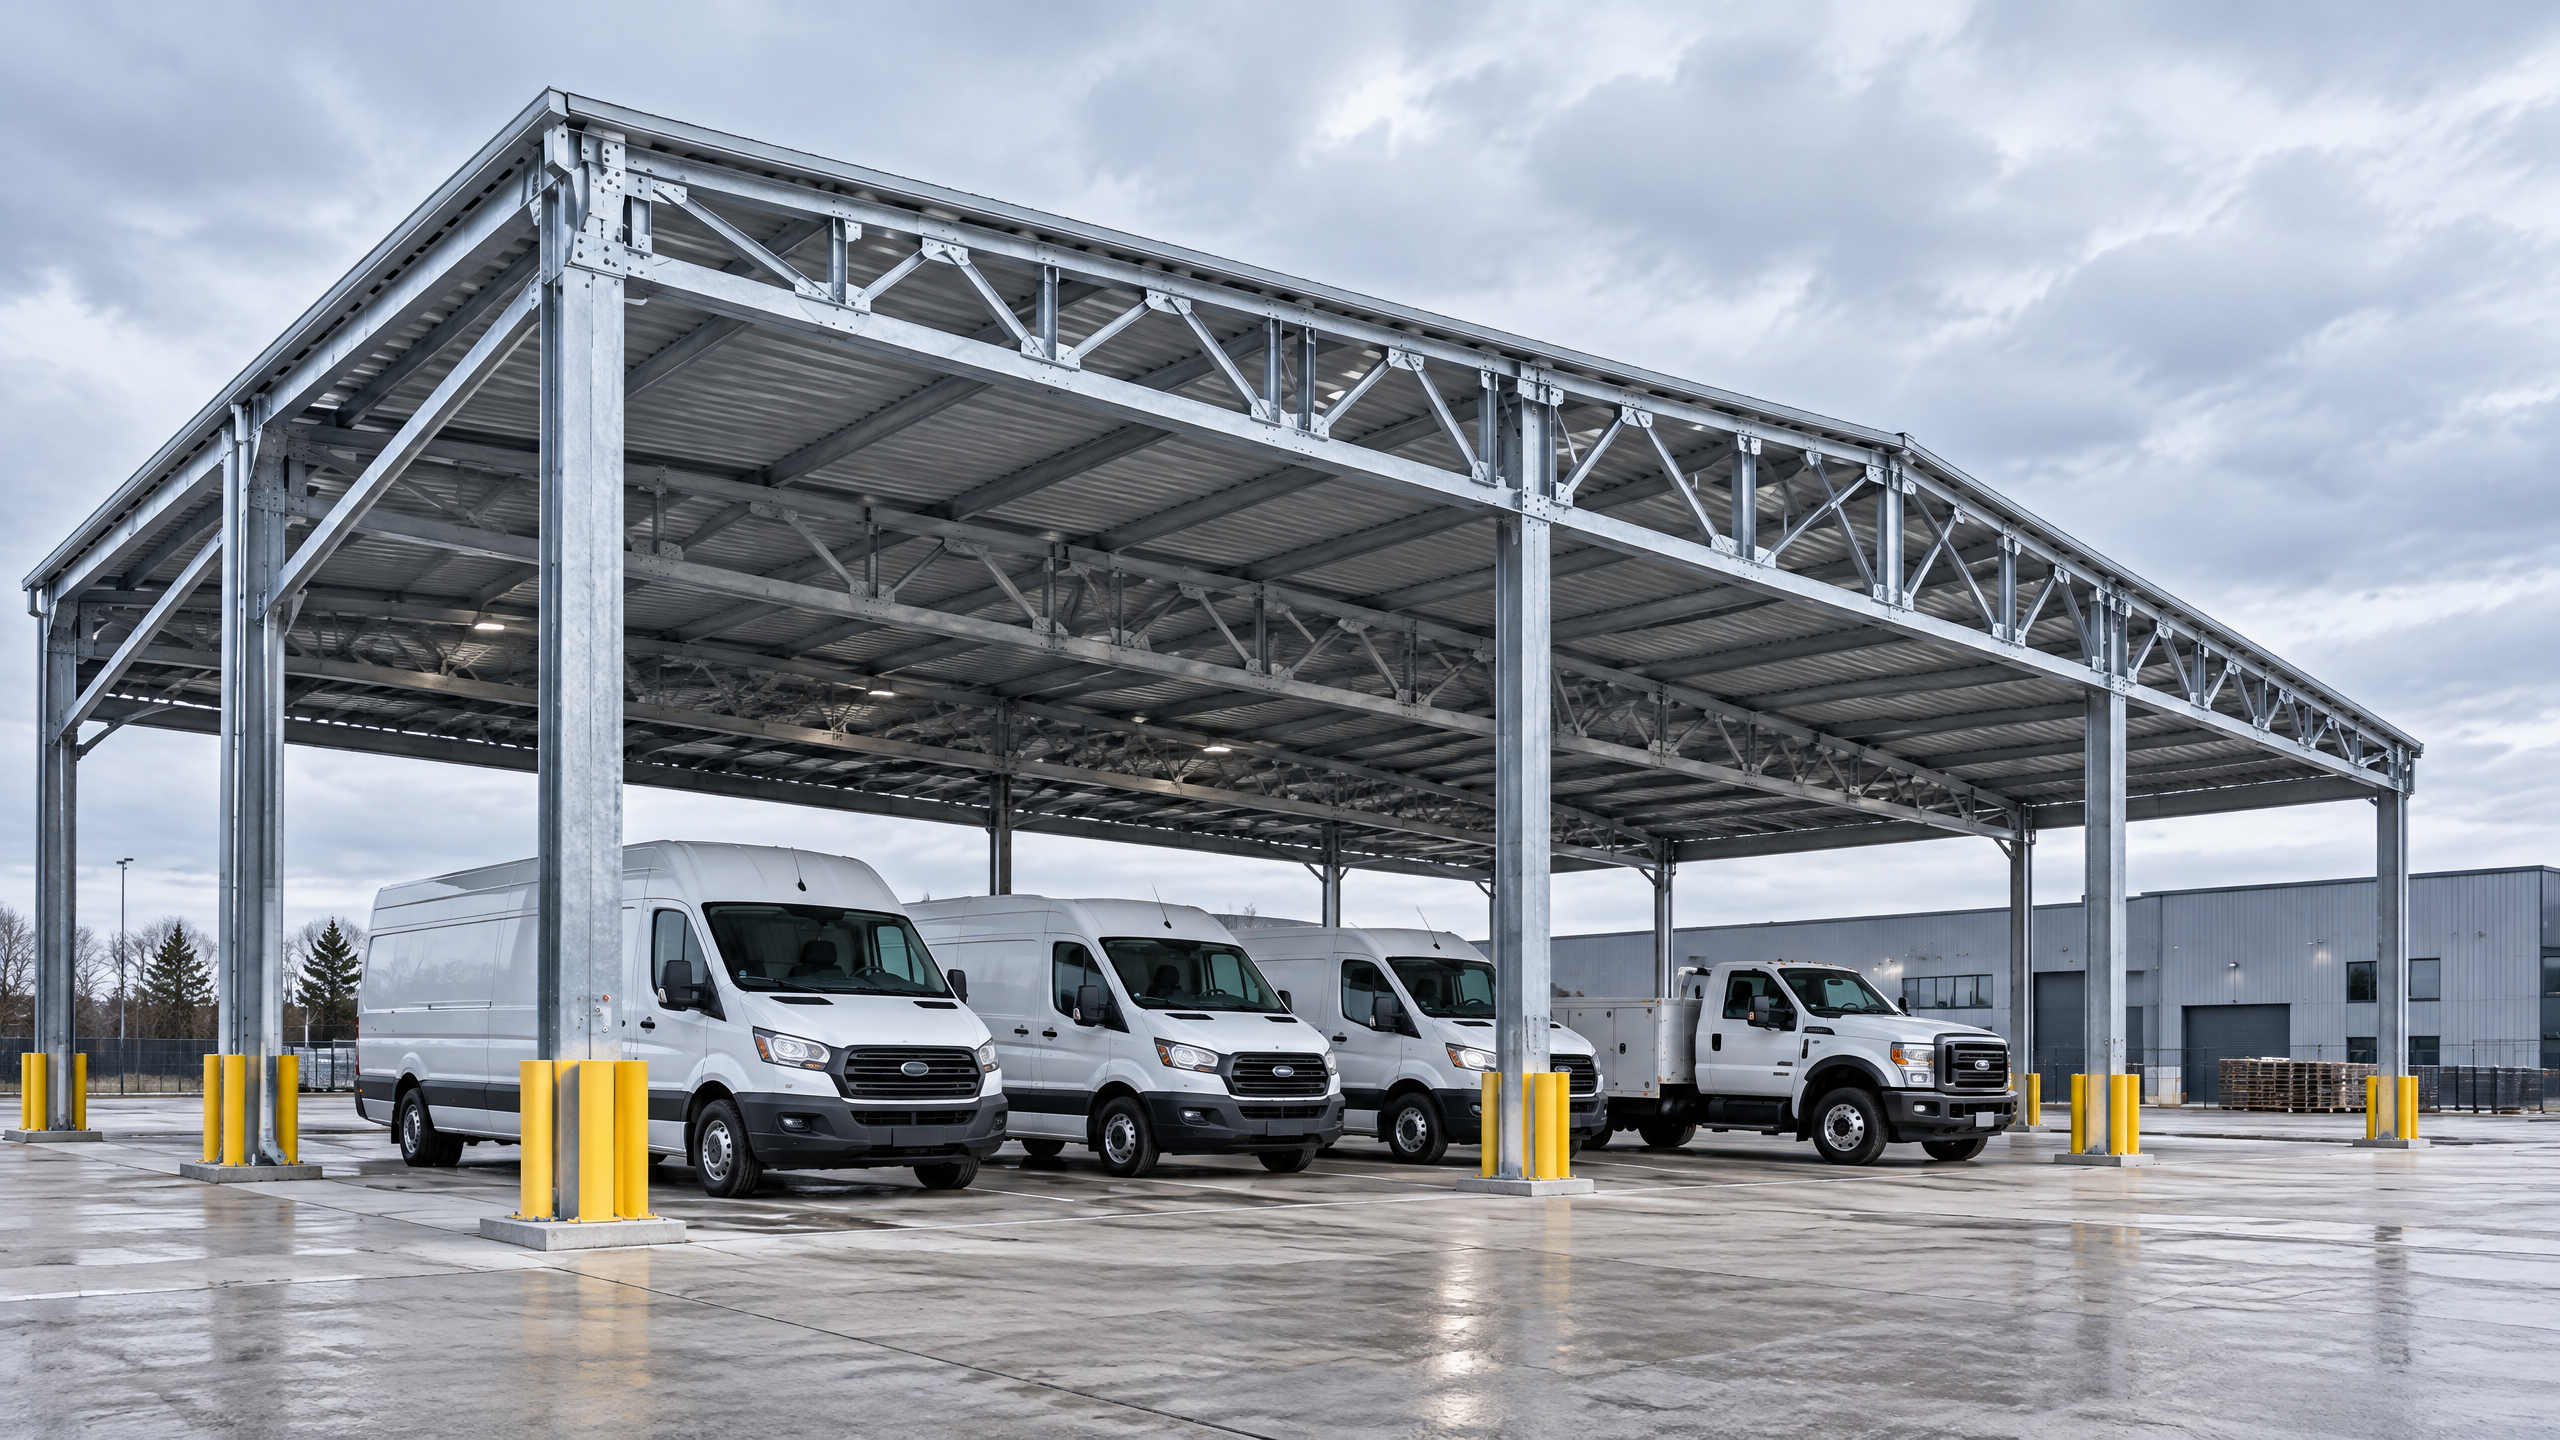
A project team must confirm that a prospective fleet carport manufacturer can deliver a complete, documented solution that matches the project’s operational, structural and commercial boundaries. That confirmation covers the manufacturer’s technical scope (structural canopy specification, foundation interfaces, PV and charging integration), demonstrable factory and quality evidence (material traceability, production controls, test records), supply and schedule assurances (lead times, logistics, factory acceptance), and practical site delivery capabilities (installation readiness, on-site supervision, warranty and spare‑parts provision). Equally important are the project inputs the team provides—fleet composition, vehicle clearance planning, commercial parking layout and operational access coordination—because the manufacturer’s design and quotation depend on them. Finally, the team should require a documented project basis and rely on local qualified professionals for site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty.
Buyer context and scope boundary
Purpose: define who this guide is for and the scope boundary for decisions you must make when selecting a fleet carport manufacturer.
Intended audience
- Distributors and system integrators procuring components for resale or EPC delivery.
- Architects and design teams responsible for layouts and building interfaces.
- Contractors and civil engineers responsible for foundations, site works and installation.
- Developers, fleet operators and logistics managers who operate or fund fleets.
- Solar EPCs and energy managers who require PV-ready or PV-integrated structures.
Scope boundary
- This guide addresses commercial and industrial applications for fleet shelters, including multi-vehicle logistics yards, parking for delivery fleets, last-mile operations, depot canopies and industrial loading areas.
- It concentrates on the manufacturer’s role: product engineering, factory production, documentation, pre-installation checks and post-installation support. It is not a substitute for site-specific design, geotechnical analysis, electrical engineering, permitting or local authority approvals—these require qualified local professionals.
Key decision drivers (summary)
- Operational fit: vehicle clearance planning, operational access coordination, and how the canopy supports fleet workflows.
- Structural fit: structural canopy specification, wind, snow, seismic loads and foundation interfaces.
- Commercial fit: cost, lead time, warranty and lifecycle costs.
- Integration fit: PV, EV charging, lighting, CCTV and building interface requirements.
Core decision principle
A single, actionable principle should guide procurement decisions:
Select the fleet carport manufacturer that demonstrably reduces total project risk across technical, programme and operational dimensions for your specific fleet and site.
What "demonstrably" means in practice:
- Documented project basis: the manufacturer must work from a scope that your team signs off (vehicle lists, layouts, geotechnical report references, utilities and permit constraints).
- Evidence: factory test reports, material certificates, shop drawings, installation method statements and references for comparable system classes (not necessarily the same site).
- Interface clarity: clear delineation of responsibilities—who supplies foundations, trenching, electrical works, earthing, and who commissions PV or EV systems.
- Contingency and commissioning plan: defined acceptance criteria and failure modes, with remedial responsibilities and timelines.
This principle helps prevent scope gaps—common in mixed civil/structural/electrical projects—and aligns commercial terms to technical deliverables.
Planning inputs every team must deliver
Before you ask a fleet carport manufacturer for a final proposal, assemble the planning inputs they need to design and price accurately. Missing or ambiguous inputs are the most frequent cause of cost and schedule variation.
Essential planning inputs
- Fleet inventory and utilisation: vehicle types, dimensions (length, width, height), axle loadings and operational turning radii. Include anticipated future fleet mixes.
- Commercial parking layout: scaled site plan with property lines, access points, circulation paths, and proposed parking arrangements. Indicate ingress/egress, queueing areas and any reserved lanes for priority vehicles.
- Vehicle clearance planning: required clearances for doors, roof racks, tail lifts and vehicle lifts. Note vehicle manoeuvring under full load and any mounted equipment.
- Operational access coordination: loading/unloading sequences, staging areas, shift patterns and maintenance access requirements.
- Geotechnical baseline: soil classification and basic bearing capacity or a note that the geotechnical investigation is pending. If available, include borehole logs and groundwater levels.
- Utilities and services: existing and proposed electrical supply points, duct routes, drainage lines and telecoms.
- Environmental constraints: flood zones, high wind exposure, seismic zones and local snow-load requirements; reference local data where available.
- Permitting constraints: setback requirements, easements, rights of way, heritage considerations and local building rules that affect height, footprint and lighting.
- Renewable-energy aspirations: whether canopies will be PV-ready, PV-integrated or not PV-equipped; desired energy yield or export strategy.
- Timeline and phasing: the desired project phasing plan, critical handover dates and any seasonal constraints affecting installation.
Planning inputs table (quick checklist)
| Input area | Minimum required by manufacturer | Who typically provides |
|---|---|---|
| Fleet inventory | Vehicle types and dimensions | Fleet operator |
| Site plan | Scaled CAD or PDF with access routes | Architect / Developer |
| Vehicle clearance | Vertical/side clearances for equipment | Fleet operator / Vehicle supplier |
| Geotech | Soil report or provisional bearing capacities | Geotech engineer |
| Utilities | Point of supply and duct routing | M&E consultant / Utility |
| Permitting | Known constraints and local rules | Planning consultant |
| Phasing | Desired dates and staging areas | Project manager |
Note: the manufacturer’s proposal will not be valid without these inputs; if inputs are incomplete, expect provisional pricing and conditional warranties.
Technical specification and interfaces
A fleet carport manufacturer must provide clear technical documentation that defines the product and how it interfaces with site civil and electrical systems. Key technical aspects include structural canopy specification, foundation interfaces, PV and low-voltage electrical integration, and provisions for ongoing operations.
Structural canopy specification
- Materials: primary members commonly use structural aluminium or steel. For architectural aluminium canopies, specify grade (e.g., 6000-series alloys), surface finish (anodizing or powder coat) and corrosion protection for coastal or chemically aggressive environments.
- Structural system: column spacing, beam sizes, connection details, and lateral load-resisting approach. Manufacturer must provide design assumptions (wind, snow, seismic) and show that members support the specified loads.
- Load cases: dead loads (decking, PV), live loads, wind uplift, snow, seismic and vehicular impact loads where applicable. Manufacturer should state compliance approach—national codes or engineering standards used to size members.
- Drainage and water management: roof slope, guttering, downpipes, and tie-in to site drainage.
Foundations and interface
- Responsibility boundary: clarify whether the manufacturer supplies foundation designs for the client’s civil contractor to execute, or supplies modular/anchored bases that a contractor installs to manufacturer tolerances.
- Anchor details: bolt sizes, embedment depths, grout and tolerances. Manufacturer should provide PFDs (project foundation drawings) consistent with local soil data.
- Vehicle impact protection: bollards, kerbs and crash-rating where vehicles operate close to columns.
Electrical, PV and services interfaces
- PV module layout, loading and support, inverter and cable routing. If the canopy supports PV, the manufacturer must coordinate structural loads and cable trays.
- Electrical handover points: specified point where low-voltage works transfer from the electrical contractor to the manufacturer or operator (e.g., inverter AC connection point, metering location).
- Earthing/ bonding: details for structural earthing of aluminium canopies and coordination with PV system earthing.
- EV charging integration: conduit routing, charging pedestal foundations, and load-management spaces in the canopy design.
Operational interfaces
- Lighting and security: mounting points, containment and access for maintenance.
- Access for maintenance: requirement for gantries, lifts or safe access platforms.
- Modularity and expandability: ability to add spans or convert canopies later without full replacement.
Technical deliverables expected from manufacturer
- Preliminary Schematic and 3D renderings showing clearances and vehicle fit.
- Structural canopy specification document and member lists.
- Shop drawings and connection details for foundations.
- Installation method statement, lifting plan and temporary works documentation.
- Electrical interface drawings for PV, inverters and earthing arrangements.
- Factory acceptance test (FAT) checklist and commissioning criteria.
- Warranty and spare-parts list with life‑cycle recommendations.
Caveat: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Procurement and factory evidence
Procurement decisions should be evidence-led. A credible fleet carport manufacturer will provide auditable evidence of capability, quality systems, and supply-chain controls.
Minimum procurement evidence checklist
- Company credentials: corporate registration, years of operation, and organisational structure for project delivery (project manager, QHSE, production, site supervision).
- Quality management: ISO 9001 certification is relevant but not mandatory—what matters is documented quality plans, control records and traceability.
- Material certificates: mill test reports for metals, coating certificates for finishes and PV module datasheets when supplied as part of the system.
- Welding and fabrication records: welding procedures, welder qualifications and inspection records for structural joints.
- Factory acceptance tests: documented FAT procedures and witness options. FAT should include dimensional checks, assembly tests and pre‑punch checks.
- Sample assemblies: prototype or sample canopy sections, including finish samples and bolted connections.
- Production capacity and lead times: realistic production schedules with capacity information for backlog management.
- Logistics and packaging: method statements for transport, lifting points and packing to avoid damage to PV modules or finishes.
- Insurance and warranties: product warranty scope, duration, and exclusions; liability insurance evidence.
- References and case studies: project descriptions of similar system types (size/complexity class) with client contact details for verification.
Decision table — Manufacturer evidence vs procurement risk
| Evidence provided | Low risk | Medium risk | High risk |
|---|---|---|---|
| Complete material certificates, FAT records, shop drawings | X | ||
| Partial certificates or verbal assurances only | X | ||
| No verifiable production records or references | X |
Factory acceptance tests (FAT)
- FATs reduce site rework and confirm installation readiness. A FAT for a canopy system typically includes:
- Dimensional and fit checks of bolt patterns and member connections.
- Verification of finish thickness and adhesion for powder-coating/anodizing.
- Pre-assembly of a representative bay and documentation of tolerances.
- Agree on FAT witness arrangements early in procurement terms.
Contractual risk transfer
- Define acceptance milestones and the transfer of responsibility for damage, loss or defects.
- Include remedies for latent defects and determine spare-parts stocking responsibilities.
- Specify holdbacks or retention quantities tied to final acceptance.
Linkage to systems and sourcing advice
- Evaluate manufacturer systems in the context of your portfolio—compare the selected product against Titan industrial and logistics system and other options in all systems.
- Use sourcing guides to align procurement checklists, especially for PV integration and civil interface responsibilities.
Mid-article CTA To discuss a documented procurement plan or request evidence templates for factory acceptance and drawings, contact our team via /inquiry or info@carportiva.com.
Site installation and operations
Installation readiness is a decisive phase. Poorly prepared sites cause delays, increase costs and degrade final performance. The manufacturer must verify site conditions and coordinate with civil, electrical and traffic contractors.
Installation readiness checklist
- Site survey and verification: actual column positions, as-built utilities and underground obstructions must be verified prior to fabrication stamping.
- Foundations complete to manufacturer tolerances: anchor positions, levels and grout tolerances confirmed; if foundations are contractor-supplied, manufacturer must approve cast-in conditions.
- Unobstructed access for delivery and crane lifts: access routes should accommodate maximum component size and crane locations; provide traffic management plans where necessary.
- Temporary works and safety: site fencing, lifting plans, exclusion zones, and coordination with site safety officer per OSHA construction standards [3] and local rules.
- Weather considerations: establish acceptable weather windows for lifting operations and sensitive finishing works.
- Storage and handling: on-site storage for PV modules and delicate components with secure, dry and level areas.
- Commissioning sequence: electrical make-safe, PV stringing, inverter commissioning and metering.
Operational handover
- Acceptance testing: mechanical tolerances, PV performance baseline (if applicable), earthing verification and lighting operation.
- Training: operator training for basic maintenance, PV emergency shutdown and inspection regimes.
- Maintenance plan: scheduled inspections for fixings, coatings and drainage; spares list and lead times for replacement components.
Table — Site responsibility split (typical allocation)
| Task | Manufacturer responsibility | Client / Contractor responsibility |
|---|---|---|
| Structural canopy fabrication and finishing | X | |
| Foundation design (if provided) | X (design) | X (construction) |
| M&E integration to main switchboard | X | |
| PV module supply (if vendor-supplied) | X or client (TBD) | X or manufacturer (TBD) |
| Site traffic management during installation | X | |
| Final commissioning and warranty handover | X | X (coordinated) |
Operational access coordination and vehicle clearance planning
- Operational access coordination requires simulation of vehicle movements with the proposed canopy positions. Use swept-path analysis for large delivery vehicles and forklifts.
- Verify tail-lift and ramp operations under canopy; confirm sufficient vertical and lateral clearances.
- Confirm turning radii at entrance gates and loading bays; coordinate bollard placements and column protection.
Safety and regulatory compliance
- Provide method statements aligned with OSHA [3] for construction safety and safe lifting operations.
- Where public access is involved, check parking design against accessibility guidance (see [1]) for compliance with accessible parking and aisle widths.
Implementation risk: common issues and mitigations
Implementation risk is multifaceted—technical, programme, commercial and operational. Below are frequent issues and pragmatic mitigations.
Risk: Incomplete site information
- Symptom: manufacturer produces provisional designs; foundations mismatch at site.
- Mitigation: require a site verification milestone before final fabrication; include a contingency for minor positional corrections and a rework clause.
Risk: Misaligned responsibilities for foundations and M&E
- Symptom: disputes on who fixes misaligned anchor bolts or trenching conflicts.
- Mitigation: clear responsibility schedule in contract with acceptance tolerances and rectification costs.
Risk: Weather and seasonal installation windows
- Symptom: installation delayed by rain or high winds, leading to demobilisation costs.
- Mitigation: build seasonal allowances into the project phasing plan and specify acceptable weather conditions for critical lifts.
Risk: Supply-chain delays for PV modules, inverters or bespoke finishes
- Symptom: canopy fabrication complete but modules late.
- Mitigation: stagger procurement and include defined delivery milestones; consider temporary cover if needed.
Risk: Unexpected geotechnical conditions
- Symptom: foundations require redesign, adding cost and time.
- Mitigation: require an early geotechnical investigation; specify provisional foundation design with allowance for variation and fast-track sub-surface verification.
Risk: Interface with existing infrastructure (drainage, telecoms)
- Symptom: buried services disrupted by foundation works.
- Mitigation: perform ground-penetrating radar (GPR) or utility surveys and coordinate trenching plans.
Risk: Warranty and spare parts ambiguity
- Symptom: lack of clarity on who supplies replacement parts or how long lead times are.
- Mitigation: contractually agree on spare parts kits, lead-time commitments and escalation paths for critical failures.
Risk mitigation table — Likelihood vs impact and actions
| Risk | Likelihood | Impact | Primary mitigation |
|---|---|---|---|
| Incomplete site data | Medium | High | Site verification milestone; provisional allowances |
| Supply delays | High | Medium | Staggered procurement; alternative sourcing |
| Foundation surprises | Low–Medium | High | Early geotech; contingency in scope |
| Interface disputes | Medium | Medium | Clear responsibility schedule; interface drawings |
| Weather delays | Medium (season-dependent) | Medium | Phasing plan; weather windows |
Six-step Fleet Carport Procurement Workflow
"Six-step Fleet Carport Procurement Workflow" — a named, actionable process to turn the procurement principle into deliverables.
- Define scope and inputs (Documented Project Basis)
- Assemble the planning inputs: fleet inventory, commercial parking layout, geotechnical baseline, utilities and permit constraints.
- Produce a scope of works document that the team signs off.
- Shortlist manufacturers and request evidence
- Issue an RFQ/RFP with required deliverables, FAT witness options and reference projects of similar complexity.
- Request procurement evidence from each supplier (see earlier checklist).
- Technical validation and interface design
- Evaluate offered structural canopy specification and check compatibility with foundations, PV and electrical systems.
- Run vehicle clearance planning and operational access coordination with swept-path checks.
- Commercial negotiation and contractual alignment
- Agree contract terms covering acceptance milestones, warranties, spare parts, lead times and holdbacks.
- Include liquidated damages or incentive clauses aligned to the project phasing plan where appropriate.
- Pre-fabrication checks and installation readiness
- Confirm final shop drawings, FAT arrangements, and delivery schedules.
- Complete site verification, foundation installation and temporary works approvals.
- Commissioning, handover and post‑installation support
- Conduct on-site installation inspection, commissioning tests, and operator training.
- Sign off final acceptance and implement the maintenance plan; agree spare-parts stocking and response SLAs.
Checklist for each step (summary)
- Step 1: Signed scope document.
- Step 2: Evidence pack from shortlisted manufacturers.
- Step 3: Approved shop drawings and interface approvals.
- Step 4: Executed contract with delivery milestones and warranties.
- Step 5: FAT records, site readiness certificate and delivery schedule.
- Step 6: Commissioning report, training sign-off and maintenance contract.
Decision tables for system selection and procurement
Decision table — System suitability by application
| Application | Preferred system attributes | Considerations |
|---|---|---|
| High-use logistics depot | Heavy-duty structural canopy, high bay height, vehicle impact protection, modular expandability | Long service life, easy column protection and route segregation |
| Delivery fleet parking (urban) | Compact spans, PV integration for low export, high finish quality for urban context | Coordination with local authorities; pedestrian safety |
| Industrial equipment shelter | High vertical clearance, reinforced anchorage, integrated gantry access | Vehicle clearance planning and lifting points |
| Long-term vehicle storage | Corrosion-resistant finishes, secure access, low maintenance | Consider local climate; materials and coatings |
Decision table — Procurement evidence and acceptable alternatives
| Evidence requested | Preferred | Acceptable alternative | Unacceptable |
|---|---|---|---|
| Full material mill certificates | Provided | Partial traceable batch certificates | No documentation |
| FAT with witness | Witnessed FAT and signed report | Recorded FAT with remote witness allowed | No FAT or factory records |
| Shop drawings stamped by engineer | Engineer-stamped drawings | Manufacturer-engineered drawings with third-party review | No shop drawings |
| Manufacturer references | Comparable system references | Non-comparable references with verifiable contacts | No references |
Frequently asked questions (FAQ)
Q: What is the difference between a canopy supplier and a fleet carport manufacturer? A: A canopy supplier may provide off-the-shelf shelter products, while a fleet carport manufacturer typically delivers engineered, project-specific systems with documented structural calculations, shop drawings, fabrication and site support. For fleet and industrial applications, the manufacturer role includes coordination with civil and electrical works and providing factory evidence such as FAT records.
Q: How important is vehicle clearance planning? A: Critical. Vehicle clearance planning determines column placement, canopy height and bolt pattern orientation. Failure to account for tail lifts, roof equipment or door openings can render a shelter unusable. Use swept-path analysis for the largest vehicles when positioning columns.
Q: Can my civil contractor install foundations to manufacturer-supplied anchor templates? A: Yes. This is common. The manufacturer should provide anchor bolt layouts and tolerances. The civil contractor must deliver to those tolerances, and a site verification prior to fabrication is recommended to confirm as-built positions.
Q: Do manufacturers usually include PV modules? A: Manufacturers may offer PV-ready canopies or supply PV-integrated systems. Responsibilities—module supply, inverter selection, commissioning and metering—should be clearly allocated. If energy yield estimates are required, involve a qualified solar engineer for accurate modelling.
Q: How do I manage warranty and spare parts? A: Define warranty scope and duration in the contract. Request spare parts lists and lead times at procurement. Consider stocking critical consumables or agreeing on guaranteed lead times for critical components.
Q: Which regulations should be considered? A: Local building codes, electrical regulations and accessibility standards apply. For accessible parking layout guidance, refer to authoritative materials such as the U.S. Access Board for parking guidance [1] where relevant. For construction safety, consult OSHA standards for construction [3]. Flood risk assessments should refer to authoritative resources such as FEMA flood mapping [2]. For highway interface or sightlines, consult applicable highway authority guidance such as the Federal Highway Administration [4] if relevant.
Q: How to validate a manufacturer’s production capacity? A: Ask for production lead-time tables, current backlog, factory capacity figures and sample production schedules. Where possible, inspect the factory or request time-stamped FAT documentation.
Conclusion
Selecting a fleet carport manufacturer for commercial and industrial applications is a technical procurement decision that requires coordinated inputs, explicit interface definitions and auditable manufacturer evidence. Successful projects align operational requirements—commercial parking layout, vehicle clearance planning and operational access coordination—with sound structural canopy specification and clear responsibility boundaries for foundations, M&E and commissioning. Use an evidence-led procurement process that verifies factory capabilities (material certificates, FATs, shop drawings) and verifies installation readiness on site.
Remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities. Use the six-step procurement workflow to reduce risk, impose discipline on scope definition and secure clear acceptance milestones.
For tailored advice on integrating canopy systems into depot operations, including evaluating Titan industrial and logistics system against your operational needs, contact us through /inquiry or info@carportiva.com. For broader comparisons, review our all systems and sourcing guides resources.
References
- U.S. Access Board parking guidance: https://www.access-board.gov/ada/guides/chapter-5-parking/
- FEMA flood maps: https://www.fema.gov/flood-maps
- OSHA construction standards: https://www.osha.gov/laws-regs/regulations/standardnumber/1926
- Federal Highway Administration: https://highways.dot.gov/
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion