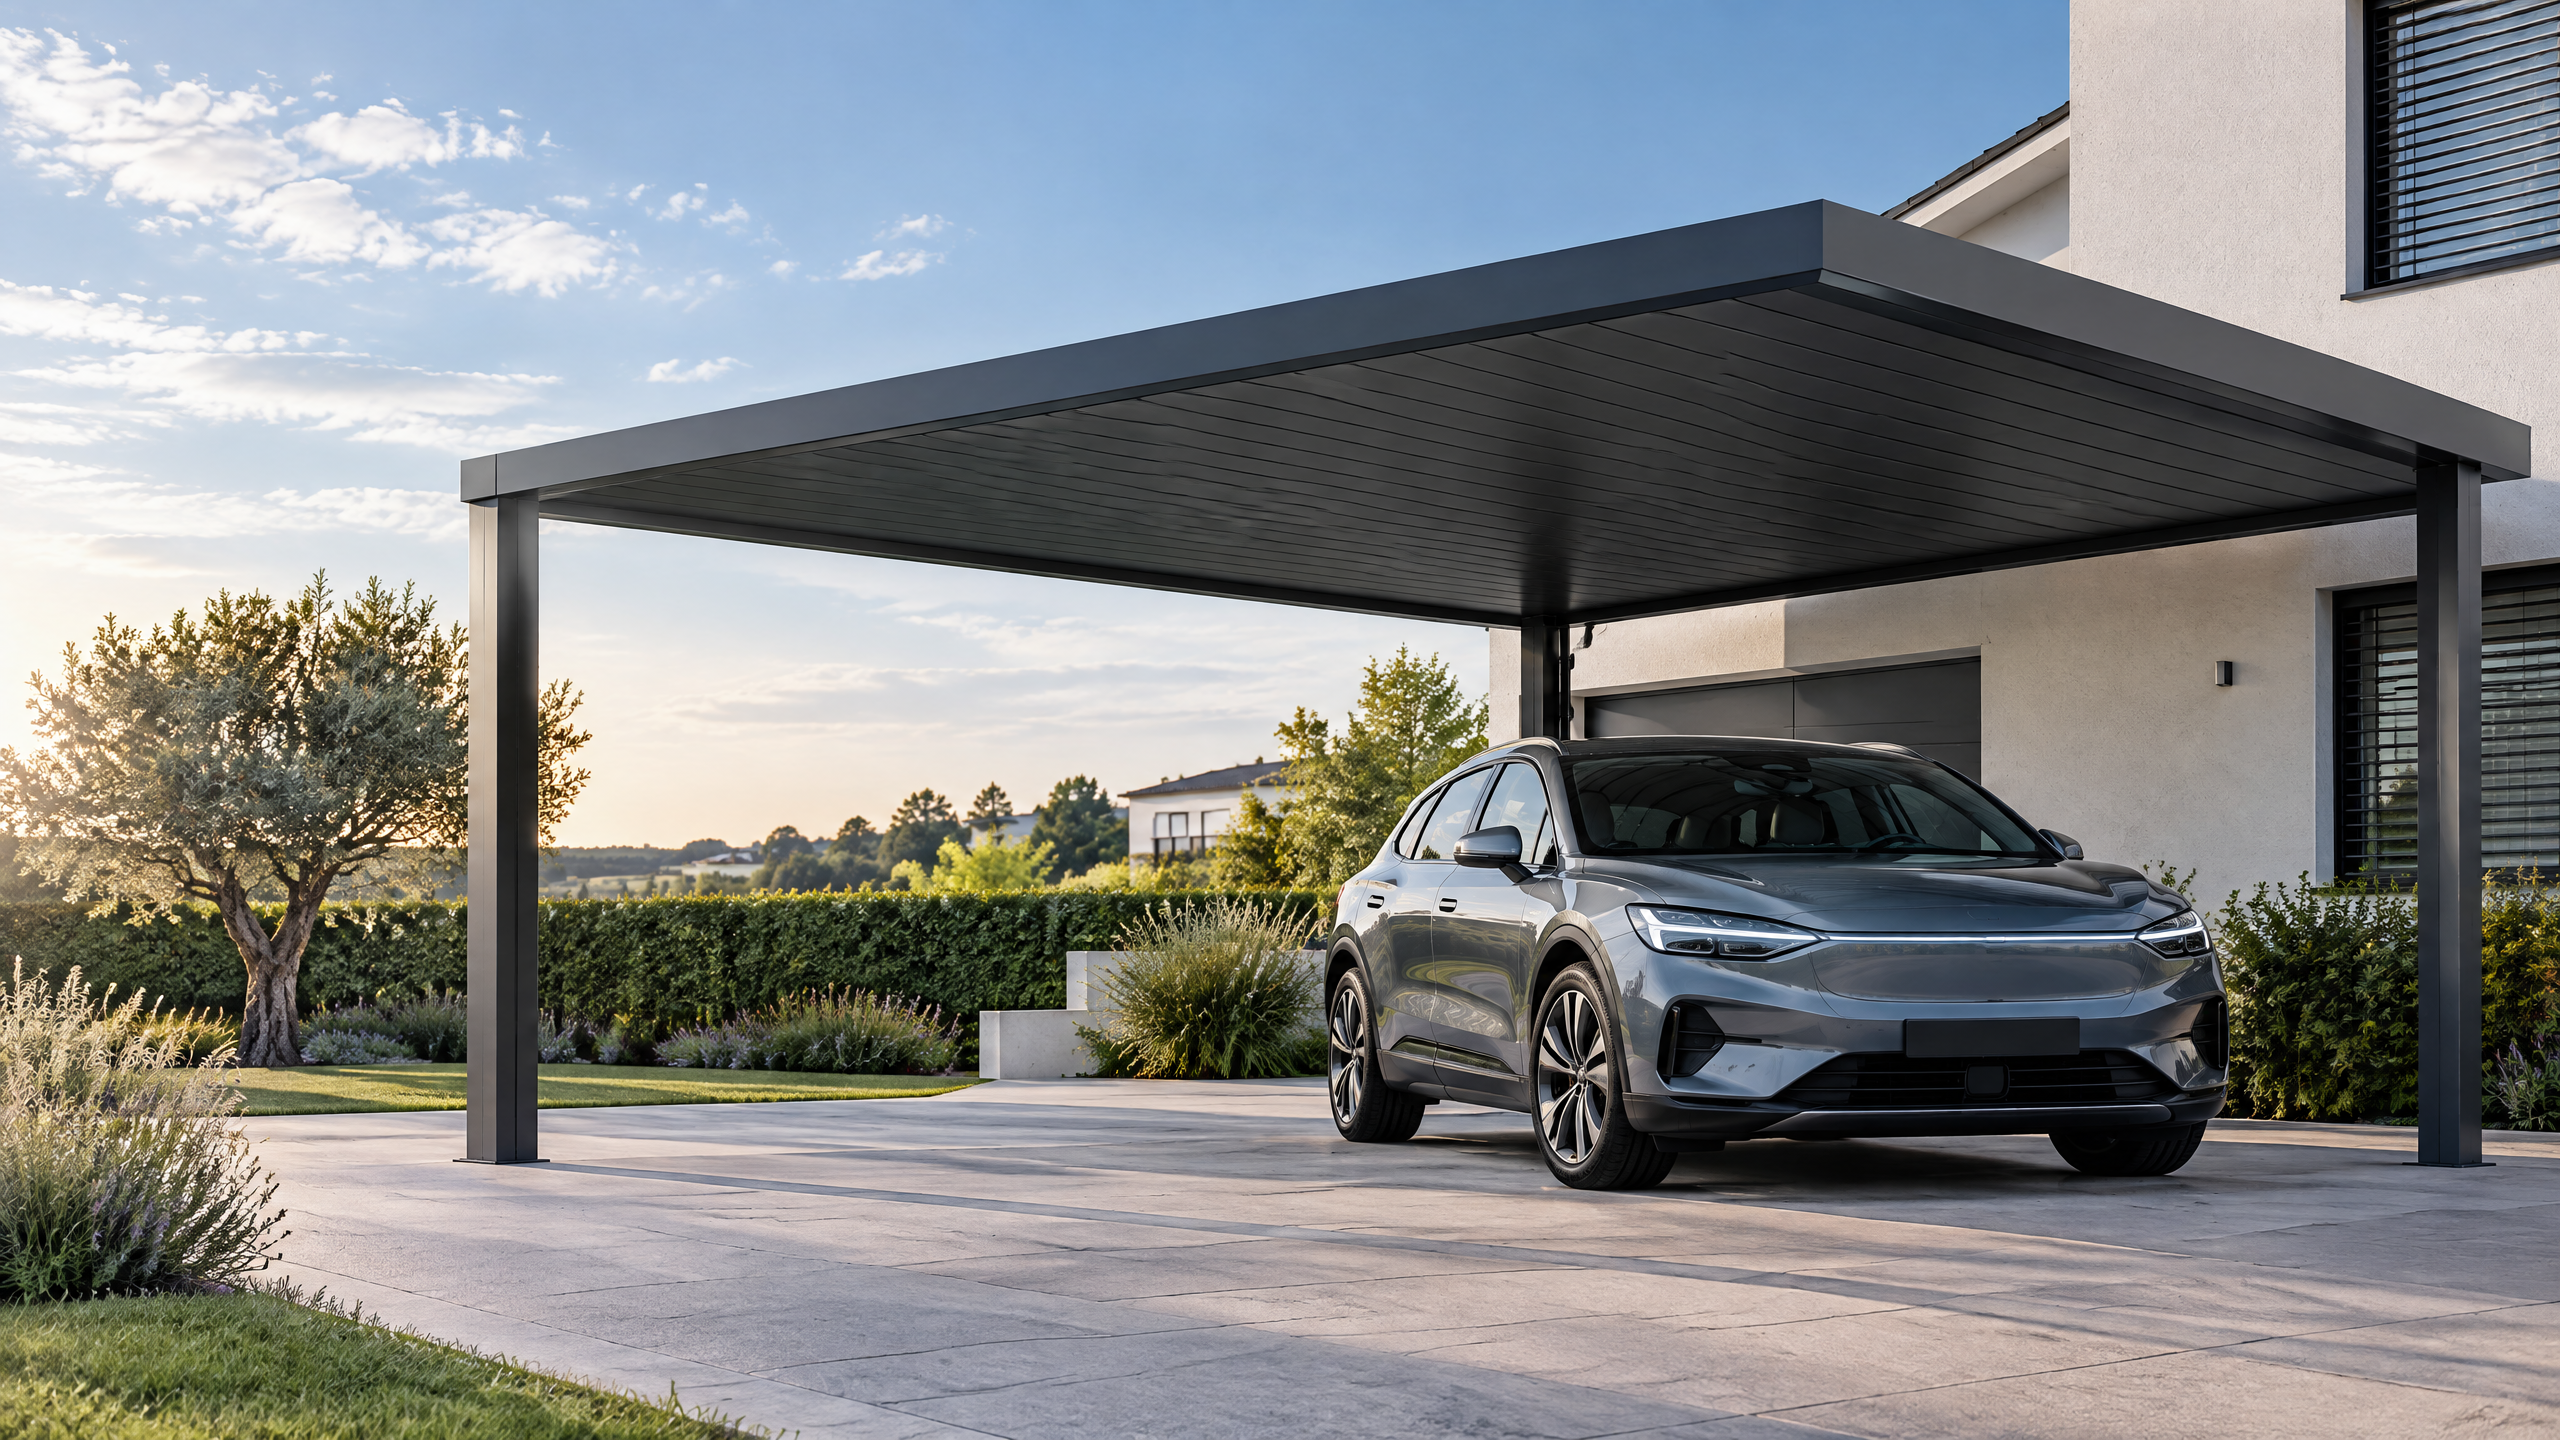
Factory-direct procurement matters when project constraints — design complexity, schedule pressure, high customization or integration (for example, PV-ready commercial solar carports) — exceed the value that local resellers or standard catalog systems deliver. Aluminium carport system factory direct can reduce specification ambiguity, shorten lead times for bespoke sections, ensure single-source quality control and traceability of material and finish, and allow design-for-manufacture choices that reduce site labour and risk. Conversely, factory-direct is less compelling for simple, repeatable shelters where local stocking distributors, approved installers, or component-level buying deliver faster responsiveness or lower freight cost. This guide explains when factory-direct procurement is strategically necessary, what technical and contractual evidence to require, how it affects the architectural carport specification and aluminium profile selection, and which factory outputs you must validate in shop drawing review to achieve installation readiness.
Buyer context and scope boundary
Audience and typical use-cases
- This guide addresses global B2B buyers: distributors, architects, contractors, developers, solar EPCs and fleet operators procuring architectural aluminium systems including architectural aluminium carports, commercial solar carports and industrial/fleet shelters.
- Use-cases range from small-deck residential multifamily canopies to large commercial parking arrays with PV integration and heavy-duty fleet shelters.
What “factory direct” means here
- “Factory direct” means contractual procurement from the manufacturer that supplies finished, factory-assembled components or kits-of-parts for direct delivery to site (including optional pre-assembly, powder-coating/finishing at factory and PV integration), rather than sourcing through a distributor, reseller or local fabricator.
- It does not imply elimination of local installers, structural engineers, or site civil works contractors — nor does it remove the need for local approvals, foundations or electrical utilities.
Scope boundaries and what this guide does not cover
- This guide focuses on procurement and implementation implications of aluminium carport system factory direct versus other supply models. It does not replace project-specific structural calculations, foundation design, permits, electrical design, approvals, lead time quotes, price negotiation, energy-yield modelling for PV, or warranty legal reviews. Those items require a documented project basis and local qualified professionals, installers, utilities and authorities — see mandatory statement below.
Mandatory project-professional statement
- Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Linkage to Carportiva systems
- For design-aligned product options see NordArch architectural aluminium system and browse all systems. For procurement checklists and templates see our sourcing guides.
Core decision principle: When factory direct is the better commercial and technical route
High-level decision rule
- Choose aluminium carport system factory direct when two or more of the following are true:
- The project demands bespoke geometry, non-standard span or integrated equipment (PV arrays, EV charging infrastructure, façade interfaces).
- Single-source responsibility for finish and fastener compatibility across the entire metalwork is required.
- Traceability of alloy, temper, or finish to supplier certificates is contractually necessary.
- Tight schedule requires concurrent design-for-manufacture to reduce site labour.
- Freight logistics (e.g., full-container shipments to the region with on-factory packaging) materially reduce total cost compared to many small shipments.
Why this rule works
- Factory-direct concentrates responsibility with one commercial and technical party. For architectural aluminium systems, that reduces the number of interfaces where specification drift, incompatible fasteners or mismatched finishes can cause site rework, corrosion risk or warranty disputes.
When factory direct is less suitable
- Low-complexity, high-repeatability projects where stock components and local fabrication produce faster turnaround and lower import duties.
- Projects with extremely tight immediate on-site start dates where local inventory reduces time-to-first-install.
Decision table: When to consider factory direct
| Project factor | Factory direct recommended? | Notes |
|---|---|---|
| Bespoke geometry or integrated PV arrays | Yes | Factory can adapt aluminium profile selection and prefabricate brackets and PV rails. |
| Standard catalog shelter, repeat order, local installer network | No | Local distributors reduce freight and customs risk. |
| Need for full material traceability and single warranty | Yes | Factory provides mill certificates and centralized quality control. |
| Urgent start within days and stock available locally | No | Lead time to ship factory-made kits may be longer. |
| Complex finish matching to façade or anodised finishes | Yes | Central finishing in factory reduces color and coating variance. |
Planning inputs: what information the buyer must provide before factory engagement
Essential project brief items
- Site survey: coordinates, topographic plan, and utilities layout.
- Structural inputs: design live loads (snow, wind, seismic as applicable), soil report for foundation design and uplift checks. Use local standards or Eurocodes where applicable for wind and snow load calculations [1].
- Architectural carport specification: intended use (public, private, PV integration), required clearances, height restrictions, and interfacing elements (pedestrian routes, canopies, drainage).
- Electrical and PV brief: point-of-connection, inverter location, routing for AC/DC cable trays, and earthing requirements.
- Permitting constraints: local planning constraints, façade and color approval processes, and any heritage or municipal restrictions.
- Interface drawings: adjacent building elevations, gutter and downpipe positions, and landscape elements.
Minimum documentation for a credible factory quotation
- Concept drawings (plan and elevations).
- Preliminary structural load assumptions or reference to local wind/snow maps.
- Bill of quantities (or schedule of items) including quantity of bays, span lengths and any special ancillaries.
- Expected delivery date window and site delivery constraints (offloading capacity, crane availability).
- Required finish specification and fastener preference (e.g., stainless steel A4 fasteners vs sacrificial zinc).
Why these inputs matter
- Early clarity on loads, interfaces, drainage, and finish prevents scope creep and changes after factory production starts, which are costly and often impossible without de-fabrication.
Technical specification and interfaces: what to verify in the architectural carport specification
Key specification topics and what to validate
- Architectural carport specification: Ensure the document defines performance requirements, not only visual design. A visual-only brief leaves critical decisions (alloy temper, finish film thickness, fastener material) to the manufacturer without buyer approval.
- Aluminium profile selection: Confirm alloy and temper (e.g., 6000-series alloys commonly used in architectural extrusions), wall thickness, and section modulus. Specify dimensional tolerances required for site-fit and bolt patterns.
- Finish and fastener compatibility: Match coating systems (powder-coat, anodize, PVDF) with fastener material and surface treatments to prevent galvanic corrosion. Specify AAMA or ISO test standards required for the finish life [3][4].
- Roof drainage coordination: Integrate drainage outlets and rainwater leaders with building drainage systems to avoid water ingress or ponding; define gutter positions and interface details to the primary building drainage system.
- PV and electrical interfaces: Define PV-module clamping details, stringing access, cable management, and inverter locations. Ensure earthing continuity through the aluminium structure is specified.
- Foundation and anchorage: Define anchor bolt types, embedment depths, plate sizes, and any requirement for anti-lift measures against wind uplift.
Checklist: Technical interface essentials
| Interface | Key buyer item to define | Why it matters |
|---|---|---|
| Structural loads | Wind/snow/seismic assumptions or reference codes | Required for aluminium profile selection and foundations |
| Finish | Coating spec (thickness, standard tests) | Determines lifespan, maintenance and compatibility with other metals |
| Fasteners | Material, coating, torque values | Prevents galvanic corrosion and ensures structural capacity |
| Drainage | Downpipe positions, gutter capacities | Avoids ponding and water damage to adjacent structures |
| PV integration | Mounting details, access for maintenance | Affects roof profile, wind load and electrical routing |
| Shop drawing tolerances | Fit-up tolerances and bolt hole positions | Avoids site modification or re-drilling |
Standards and references
- Use national codes or Eurocodes for structural design when applicable (for wind and snow, see Eurocodes [1]). Specify finish or tests referencing AAMA or ISO standards where the finish performance is critical [3][4]. Consult The Aluminum Association for alloy reference data where needed [2].
Procurement: what factory evidence to request and how to evaluate it
What to insist on for factory-direct procurement
- Product breakdown and BOM: clear list of extrusions, profiles, fasteners, coatings, spacer/dampers, anchors and ancillaries.
- Mill certificates and material traceability: certificates for aluminium alloy batches and, if required, heat numbers or mill test reports.
- Coating and finish records: production runs coated at factory with batch numbers, color formulas and test results (e.g., thickness, adhesion).
- Welding and assembly QA: if welds are part of the structure, request welding procedure specifications and welder qualifications.
- Load check or design calculations: factory-supplied calculations showing the chosen profiles and connections meet the buyer's designated design loads.
- Production capacity and lead times: evidence of capacity (available production slots) and confirmed delivery windows.
- Packaging and transport plans: how kits will be packaged, labeled and protected for sea/land transport.
- Quality control plan: inspection points, acceptance criteria and non-conformance procedures.
Decision table: Procurement evidence checklist for factory direct
| Evidence item | Acceptable deliverable | Red flags |
|---|---|---|
| Mill certificates | Signed mill test reports for aluminium alloy | No traceability or only generic alloy statements |
| Finish records | Batch coating test results and color formula | No test references or vague performance claims |
| Design calculations | Calculations tied to specified loads and profiles | Calculations not linked to specific section properties |
| Welding QA | WPS and welder certifications | No evidence of qualified welders or QA checks |
| Packing & delivery | Detailed packaging plan with labelling | No packaging details or untested export crating |
| Lead time confirmation | Firm production schedule and shipment ETA | Floating lead times with wide windows |
How to evaluate the supplier's manufacturing capability
- Visit the factory if the procurement size and risk justify it, or request a virtual factory tour focusing on extrusion lines, finishing booths and assembly jigs.
- Verify that the factory has documented processes for powder coating or anodizing if finish is critical.
- For PV-integrated carports, confirm the supplier’s experience with module rail systems, module grounding and access for electrical service.
Commercial terms to negotiate
- Acceptance tolerance for deviations, responsibility for on-site rework, packaging and uncrating costs, warranty terms, and penalties for missed delivery windows.
- Staged acceptance (component acceptance at factory, site kit acceptance, final commissioning acceptance) to manage risk and payment triggers.
Caveat on certifications and claims
- Do not accept unsubstantiated claims of “certified” performance without seeing the actual test reports or relevant third-party certification documentation. Where standards are referenced, request specific clause-level compliance evidence.
Shop drawings, pre-delivery validation and installation readiness
What shop drawing review must cover
- Dimensional coordination: bolt hole positions, bracket placement, splice details and absolute dimensions to millimetre or specified tolerance.
- Interface callouts: drain lines, building penetration details and adjacent façade interfaces.
- Connection design: bolted/welded connection capacity, fastener grades and torque instructions.
- Sequencing diagrams: how kits are to be labeled, unpacked and assembled on site.
- Lifting and handling instructions: safe lifting points for prefabricated bays or heavy components.
Using shop drawing review to reduce site risk
- Establish a document review cycle with named reviewers from the buyer’s side (architect, structural engineer, electrical/PV engineer) and the manufacturer. Include a formal sign-off that confirms responsibility for dimensions.
- When dealing with imported kits, insist on a pre-shipment inspection (PSI) and a packing list that correlates to shop drawings.
Installation readiness: items to verify before the first delivery
- Foundations and anchor bolts installed to specified positions and tolerances; template and datum confirmed.
- Crane/handling equipment availability on site and any temporary works required for erection.
- Storage capacity and protection on site for components; avoid storing coated extrusions in direct sun for extended periods.
- Installer competency and tooling: torque wrench specifications and calibrated tools.
- Electrical and PV preparatory work: conduit routing, dedicated earthing rods where specified, and the on-site electrician assigned.
Example checklist for installation readiness
| Item | Action required | Responsibility |
|---|---|---|
| Anchor bolt layout | Confirm positions using template and as-built survey | Site civil contractor / structural engineer |
| Lifting plan | Signed lifting plan for large bays | Main contractor / installer |
| Installer training | Factory or approved installer training scheduled | Buyer / manufacturer |
| Torque calibration | Torque wrench calibration certificate on file | Installer |
| Electrical point-of-connection | Conduit and meter location prepared | Electrical contractor |
Remember: shop drawing review is not optional
- Shop drawing review is the last practical point to catch misaligned expectations before fabrication. The phrase shop drawing review should be included in contractual deliverables and a named buyer reviewer indicated.
Use of the keyword: include "shop drawing review" explicitly in contract deliverables and procurement checkpoints to formalize the review process.
Site installation and operations: typical sequences and operational considerations
Typical installation sequence for factory-direct kits
- Site verification and anchorage confirmation.
- Delivery of kits in labelled bundles with packing list tied to shop drawings.
- Erection of primary frames and secure temporary bracing.
- Attachment of secondary members and roof panels or PV rails.
- Installation of drainage, gutters and downpipes.
- Electrical and PV tie-in, commissioning and earthing checks.
- Final checks, fixings torque verification and handover.
Operations and maintenance considerations
- Maintenance access: design in removable panels or access hatches for PV string combiner/inverter access and for periodic cleaning.
- Lifetime planning: specify expected lifecycle for finish and fasteners and required maintenance intervals in the contract.
- Spares package: include a kit of spare extrusions, fasteners (matching lot numbers), and touch-up paint or coating. This reduces downtime for repairs and ensures compatibility.
Durability and corrosion control
- Aluminium resists atmospheric corrosion, but design must avoid direct contact with dissimilar metals without proper isolation. Specify finish and fastener compatibility to reduce galvanic action — reference finish and fastener compatibility in the technical specification.
- Use appropriate gaskets, isolators or sacrificial layers where the aluminium interfaces with stainless steel or hot-dip galvanized parts.
Operational safety and warranties
- Documented commissioning tests (e.g., torque checks, continuity for earthing, visual finish inspection) should be a precondition of final acceptance.
- Warranties should be clear about what is factory responsibility and what is local trades responsibility (foundations, site wiring, civil works). Warranties can be invalidated by unauthorized modifications, poor maintenance, or failure to adhere to installation instructions.
Implementation risk: common failure modes and mitigations
Risk: specification drift between architectural intent and delivered product
- Mitigation: lock critical items in the architectural carport specification and require factory confirmation on those items at shop drawing review.
Risk: incompatible fastener and finish combinations causing corrosion
- Mitigation: specify finish and fastener compatibility with material callouts, isolation methods and acceptable galvanic couples.
Risk: site misalignment of anchor bolts causing rework
- Mitigation: provide accurate anchor templates and require as-built verification before fabrication or pre-shipment.
Risk: logistics and customs delays for factory-direct shipments
- Mitigation: factor realistic lead times, include buffer in procurement schedule and consider staged shipments for critical path items.
Risk: insufficient installer competency for non-standard systems
- Mitigation: require factory or certified installer training and include installation supervision in contract scope.
Risk: changes after production started
- Mitigation: change control clause with clear pricing and lead-time consequences; prefer freezing design before start of manufacturing.
Risk: warranty disputes arising from mixed responsibility
- Mitigation: define clear acceptance stages and responsibilities for foundations, civil works and electrical systems; maintain documented commissioning records.
Risk mitigation table: failure mode vs evidence-based controls
| Failure mode | Evidence to request | Control action |
|---|---|---|
| Corrosion at fastener interfaces | Fastener material proof, finish test records | Select compatible materials and isolators |
| Anchor mis-location | As-built survey, anchor templates | Hold off delivery of critical pre-drilled baseplates until anchor verification |
| Unclear responsibility for PV tie-in | Written scope split in contract | Explicitly allocate PV mounting vs electrical commissioning roles |
| Transport damage | Packing list, pre-shipment photos | Insist on PSI and insured shipment terms |
Named six-step buyer workflow: The Carportiva Factory-Direct Decision Pathway
Overview
- This named workflow is designed for B2B buyers to move from project brief to commissioned canopy while controlling risk and ensuring installation readiness.
Step 1 — Define (Project Intent & Constraints)
- Deliverable: formal project brief with site survey, load assumptions and architectural carport specification.
- Who signs off: project architect or developer.
Step 2 — Select (Supplier & System)
- Deliverable: shortlist of factory suppliers and product system selection (e.g., NordArch architectural aluminium system or alternatives from all systems).
- Who signs off: procurement lead with inputs from architect and structural engineer.
Step 3 — Validate (Technical Verification)
- Deliverable: shop drawing review, design calculations, finish and fastener compatibility confirmation (include "aluminium profile selection" and "finish and fastener compatibility" checks).
- Who signs off: structural engineer and client technical representative.
Step 4 — Procure (Contract & Factory Evidence)
- Deliverable: purchase order with documented factory evidence: mill certificates, finish records, and production schedule.
- Who signs off: procurement legal and contracting.
Step 5 — Deliver (Logistics & Pre-delivery Inspection)
- Deliverable: PSI report, packing list, and staged delivery schedule leading to site.
- Who signs off: site manager and buyer representative.
Step 6 — Commission (Installation Readiness & Handover)
- Deliverable: final installation report, commissioning certificates, spare parts list, and handover pack including recommended maintenance schedule.
- Who signs off: client, contractor, and manufacturer after "installation readiness" checks.
Workflow notes
- Each step should have named approvers and a defined response timeframe to avoid ambiguity.
- Integrate the sourcing guides templates for RFQ and PO attachments where applicable.
Frequently asked questions (FAQ)
Q: How does factory-direct affect lead time compared with local supply? A: It depends. For highly customized work, factory-direct can be faster because of design-for-manufacture and single-source planning; for off-the-shelf items, local stock is often quicker. Confirm production slots and shipping estimates with the factory early.
Q: Will factory-direct reduce total cost? A: Not always. Factory-direct can reduce labour cost and site rework but introduces freight, customs and import handling costs. Use a total-cost-of-ownership analysis including logistics, site labour savings and warranty management.
Q: How do I ensure finishes match adjacent building elements? A: Require color formulae, batch numbers and physical sample panels from the factory. Include AAMA or ISO finish tests as contractual obligations [3][4].
Q: Who is responsible for PV electrical connections when the factory supplies PV-mounted rails? A: Define responsibilities explicitly in the contract: often the factory supplies mechanical mounting and earthing continuity, while the electrical contractor performs stringing, inverter installation and grid connection.
Q: Can I request certain alloy temper for structural profiles? A: Yes. Specify alloy series and temper requirements and require mill certificates; consult The Aluminum Association for alloy properties if necessary [2].
Q: What is the best practice for avoiding anchor-bolt misplacement? A: Provide anchor templates and do an as-built anchor survey before shipping components that require precise bolt-hole alignment.
Q: Are there third-party standards I should reference for load design? A: Yes — use applicable national codes or Eurocodes for wind/snow/seismic design as relevant [1]. Reference these in the architectural carport specification.
Q: Is factory direct suitable for PV-integrated systems? A: Frequently yes, because factories can integrate PV rails, shear connectors and tailored bracing into the kit, reducing site work and ensuring consistent earthing and fastening systems.
Conclusion and practical next steps
Practical summary
- Aluminium carport system factory direct is a strategic choice where complexity, finish control, traceability and integrated equipment demand single-source manufacture and quality assurance. It becomes less attractive when a project is simple, repeated and supports quick local supply. The core procurement tools to make factory-direct successful are: a well-defined architectural carport specification, rigorous shop drawing review, explicit finish and fastener compatibility requirements, and documented factory evidence including mill certificates and production schedules.
Immediate next steps for B2B buyers
- Prepare a concise project brief with the items listed in the Planning inputs section.
- Use the six-step buyer workflow to assign accountability and timelines.
- Request the procurement evidence checklist from shortlisted factories and compare like-for-like across BOM, finish tests and lead times.
- Schedule a shop drawing review window and assign reviewer roles in the contract.
- Plan for pre-shipment inspection and on-site installation readiness verification.
Mid-article action
- To request bespoke technical support or to start an RFQ using manufacturer-level inputs, submit project details via our inquiry channel: /inquiry
Final note
- Responsible procurement requires documented project bases and local professionals. Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require input from relevant local qualified professionals, installers, utilities and authorities.
For bespoke system choices and design integration refer to NordArch architectural aluminium system or view all systems. For RFQ templates and procurement checklists refer to our sourcing guides.
Closing action
- For technical quotations, warranty clarifications or to request factory evidence, contact us at info@carportiva.com.
References (selected standards and guidance)
- Eurocodes for structural design and load cases [1].
- The Aluminum Association for alloy and extrusion data [2].
- American Architectural Manufacturers Association for finish guidance [3].
- ISO Online Browsing Platform for referenced test standards [4].
References
- European Commission Eurocodes: https://eurocodes.jrc.ec.europa.eu/
- The Aluminum Association: https://www.aluminum.org/
- American Architectural Manufacturers Association: https://aamanet.org/
- ISO Online Browsing Platform: https://www.iso.org/obp/ui/
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion