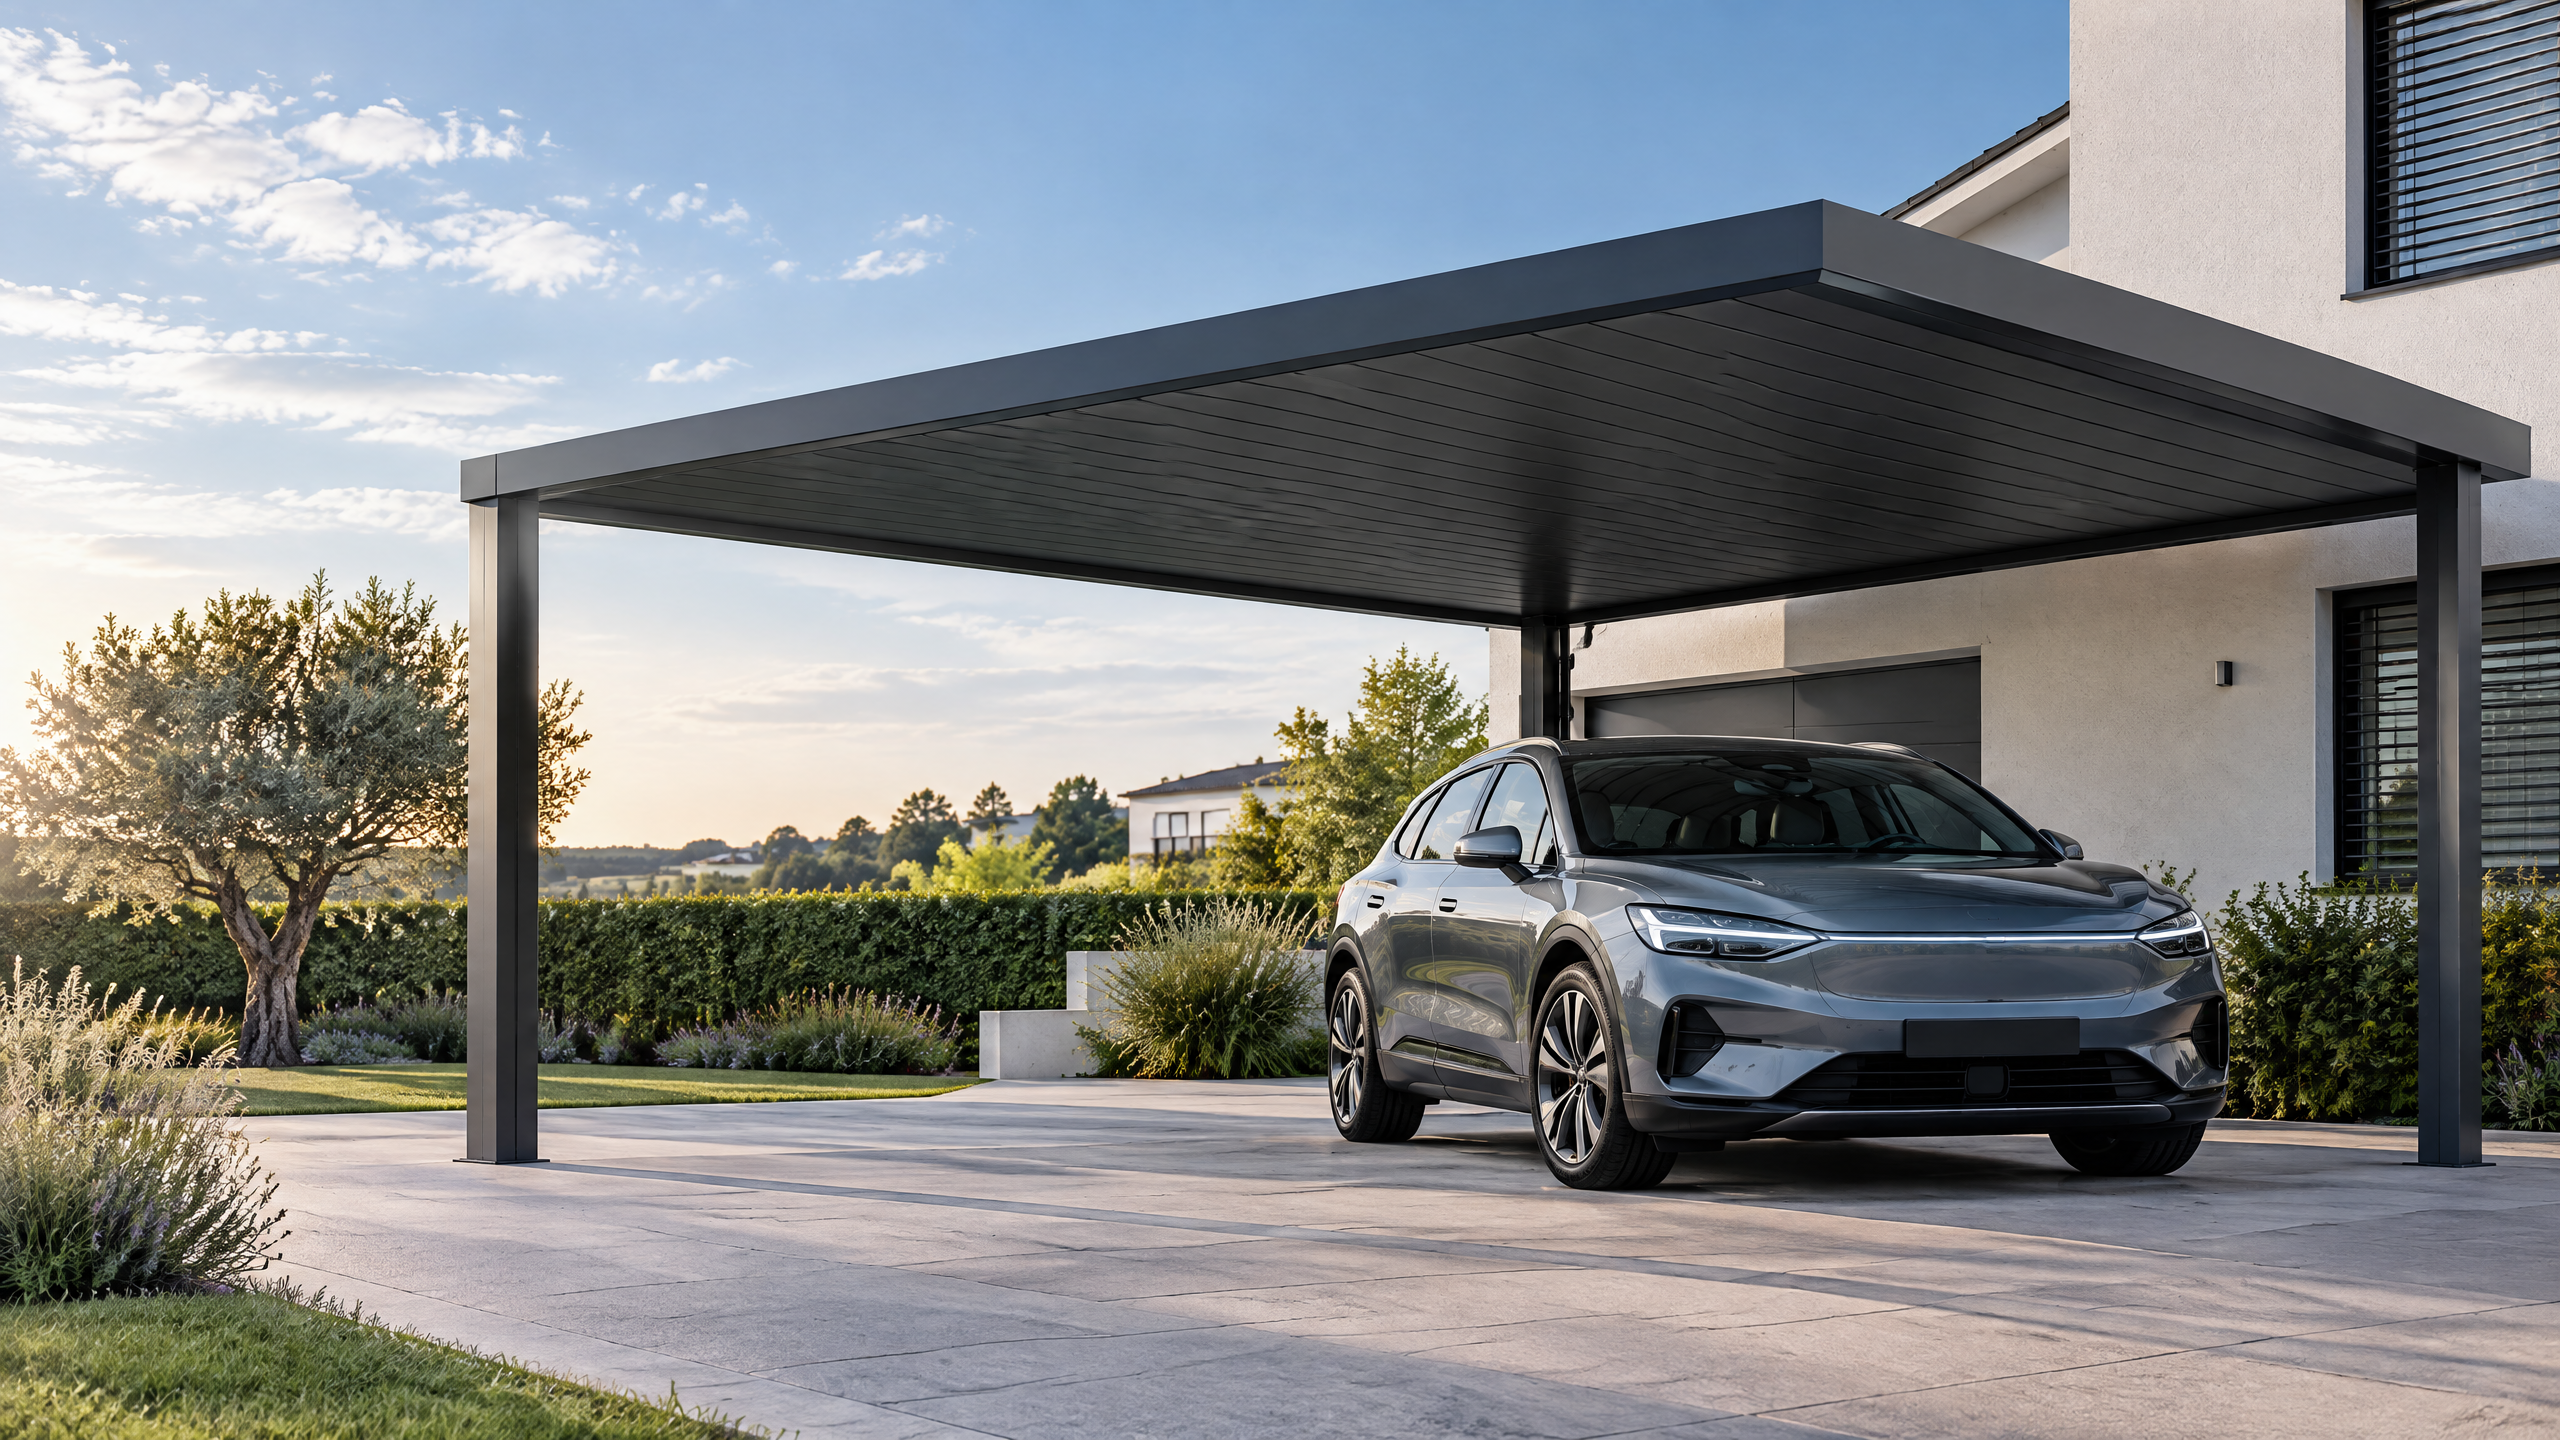
Direct answer (≈150 words) Specifying aluminium carport frame profiles for a commercial carport project requires turning performance requirements into measurable, verifiable procurement deliverables. Start by defining the project scope (span, loads, canopy use, solar integration, expected lifespan and maintenance regime), then translate those requirements into material (alloy and temper), cross‑section geometry, wall thickness, connection concept, finishes and compatible fasteners. Define interfaces early — roof drainage coordination, electrical and PV mounting, foundations and access — and include shop drawing review and factory acceptance evidence in procurement documents. Require structural calculations tied to the project’s governing codes and provide a documented basis for site-specific decisions. Evaluate suppliers on their ability to deliver detailed shop drawings, material test reports, finishing standards, dimensional tolerances and an installation readiness plan. For product options see the NordArch architectural aluminium system and explore all systems or our sourcing guides. For complex items engage local qualified engineers, installers and authorities to confirm design assumptions.
Buyer context and scope boundary
Who should read this, and what is in scope
- Audience: distributors, architectural specifiers, contractors, developers, solar EPCs, fleet operators and procurement teams considering commercial aluminium carports, solar carports or fleet shelters.
- In scope: selection and specification of aluminium carport frame profiles (extrusions, fabricated sections and connections), related interface requirements (roofing, drainage, PV fixation, electrical containment), procurement evidence and on‑site assembly readiness.
- Out of scope: site geotechnical design, local permit approvals, detailed electrical design for PV arrays, or warranty claims handling (each require local professional input).
Project types covered
- Architectural canopies and public carparks with aesthetic requirements;
- Commercial solar carports with integrated PV modules and electrical routing;
- Industrial/fleet shelters prioritising rapid installation and heavy‑vehicle clearance.
Boundaries and dependencies
- The profile selection cannot be finalised until loads (wind, snow, live loads), span and support spacing are determined and checked against local codes. Structural calculations must reference the project’s governing code (e.g., Eurocodes where applicable) and be performed by a qualified engineer [1].
- Surface finish selection must align with fastener selection to avoid galvanic corrosion; detail this under finish and fastener compatibility.
Core decision principle
A single overriding procurement test The central procurement principle is: specify what the profile must do (functional performance) and how compliance will be demonstrated (evidence). That means converting requirements into measurable attributes and acceptance criteria such as:
- Design loads and code basis (e.g., governing wind/snow/seismic standard) [1];
- Material alloy and temper with supporting material test reports (MTRs) referencing recognised standards [2];
- Structural capacity demonstrated by calculations and section properties;
- Dimensional tolerances and finish specifications with verification methods (inspection, thickness tests, colour panels) referencing AAMA or ISO standards where applicable [3][4];
- A clear interface acceptance matrix: what the supplier supplies vs what the contractor supplies (gaskets, sealants, anchor bolts, downpipes).
Why this matters
- Saves iterative redesign on site;
- Enables apples‑to‑apples commercial evaluation;
- Reduces warranty and interface disputes by spelling out responsibilities.
Planning inputs (what the specification must be fed with)
Essential project inputs procurement needs to gather before specifying profiles
- Code and design basis
- Local design code and edition (e.g., Eurocodes for Europe) and any project‑specific load factors or combinations [1].
- Loads and spans
- Clear indication of spans, column spacing, tributary widths, and service loads (including snow drift or concentrated loads).
- Environmental exposure
- Corrosion category (marine, industrial, rural), UV exposure, temperature extremes and abrasion risk.
- Roof and drainage requirements
- Slope, waterproofing type, location of outlets, gutters and overflow arrangements — roof drainage coordination is essential to avoid water ingress at frame junctions.
- PV and electrical interface
- PV module type, mounting rails, cable trays, inverter/combiner locations and conduit routing; clarify which party supplies PV attachments.
- Foundations and anchorage
- Soil report, anchor embedment depth, and required anchor types or precast templates.
- Programme, logistics and access
- Lead time expectations, site access constraints (crane capacity, laydown), and staged delivery requirements.
- Aesthetic and finish requirements
- Colour targets, gloss level, anodising requirement, and serviceability expectations (graffiti resistance, washdown).
- Maintenance and lifecycle
- Expected inspection regime, maintenance access and desired design life (e.g., 20/25+ years).
Collecting these inputs up front prevents specification gaps. Note: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Technical specification and interfaces
How to write the profile specification so procurement and engineering align
Key specification headings (each should include acceptance criteria)
- Product name/identifier and drawing references (linked to NordArch architectural aluminium system if using that system).
- Design code and calculation scope (reference governing code).
- Material: alloy, temper, acceptance tests (chemical analysis, mechanical properties) and traceable material test reports (MTRs) to support claims [2].
- Geometry: cross‑section drawing(s) including nominal dimensions, wall thicknesses, corner radii, and extrusion tolerances.
- Section properties: moment of inertia, section modulus and shear area to be provided by supplier and cross‑checked against structural calculations.
- Connections and fasteners: type (bolts, welds, splice plates), washer types and torque requirements, and whether fasteners are supplied loose or pre‑installed.
- Finishes: pre‑treatment, coating system and thickness; reference AAMA specification where appropriate for powder coat durability [3]. For anodised finishes specify chemical film thickness and visual acceptance.
- Interfaces: roof clamping, PV module rails, gutter and downpipe interfaces, sealant and flashing details.
- Drainage: specify ponding limits, slope and locations for outlets; require collaborative roof drainage coordination between client, carport supplier and roofing specialist.
- Fabrication and shop drawing requirements: see shop drawing review section.
- Testing and verification: dimensional checks, coating adhesion, fastener torque tests and sampling plan.
Dimension tolerances and QA
- Specify tolerances for straightness, squareness and hole positional accuracy referencing ISO standards for profiles and extrusions where relevant [4].
- Require a supplier quality plan including inspection points and sample sizes for each lot.
Compatibility rules
- State specific restrictions such as incompatible metal pairings, required isolators (e.g., polymer washers), and expectations for sacrificial anodes or barrier coatings in aggressive environments.
Materials and alloys
- Aluminium alloys and tempers should be specified by the design team (common structural alloys include 6000 series) and must be supported by MTRs showing chemical composition and mechanical properties [2]. Do not accept generic “aluminium” descriptions without alloy/temper details.
Connections and assembly
- Where bolted connections occur, specify bolt grade and coating (stainless for coastal sites), hole tolerances, slotting allowances for thermal movement and required torque procedures. For welded connections specify filler material and weld procedure qualification if welds are performed in shop.
Thermal movement and expansion
- Provide guidance on allowable movement and design for expansion joints or sliding connections, particularly where long unsupported spans are present.
Profile types and aluminium profile selection considerations
Matching profile geometry to performance and fabrication logic
- Structural box sections (closed rectangular/box) provide torsional stiffness and are often preferred for long spans or when channels must be concealed.
- Open channels and C‑sections are simpler to fabricate and lighter but may require bracing or increased wall thickness to resist torsion.
- I‑sections and castellated sections can be effective for cantilevers where bending capacity is the controlling factor.
- Custom extrusions can integrate stiffening ribs, drainage channels or mounting tracks to reduce secondary fabrication on site.
Decision factors to evaluate for aluminium profile selection
- Span and load: longer spans and higher loads increase the need for deeper sections or box profiles.
- Torsional demands: where wind or asymmetric loading introduces twisting, prefer closed sections.
- Fabrication vs supply chain: standard mill sections may reduce lead time; custom extrusions offer integration but add tooling lead time and cost.
- Integration of services: profiles that incorporate cable channels or PV mounting grooves can reduce on‑site works but require early coordination.
Decision table: Profile type vs common use cases
| Primary driver | Typical profile form | Fabrication implications | Procurement trigger |
|---|---|---|---|
| Long span, high bending moment | Closed box / deep rectangular section | Requires heavier extrusion or welded assembly; may need larger transport footprint | Require section properties and factory stress-relief procedures |
| High torsion / asymmetric loading | Box or multi‑web closed section | Higher extrusion complexity; welding increases QA scope | Demand torsion capacity and MTRs |
| Lightweight, short span | C-channel or hat profile | Simple to extrude; may need bracing | Check deflection criteria and connection details |
| Integrated PV mounting and drainage | Custom extrusion with grooves/recesses | Longer lead time; requires prototype and tooling sign‑off | Prototype sample and shop drawing review |
Avoid specifying only a catalogue name; always require section properties and testable evidence.
Roof drainage, PV and finish interfaces
Integrating roof, drainage and module works
- Roof drainage coordination must be documented early. Specify outlet quantities, locations, gutter capacity and overflow paths and require a combined roof drainage plan that integrates canopy frame penetrations, water ingress prevention at postheads and downpipe routing.
- Detail whether gutters are part of the carport frame scope or supplied separately. Interfaces must include gasket, sealant and flashings.
PV integration specifics
- Require PV mounting details: clamp type, span of module rails, module edge clearances, and additional loads (wind uplift on modules). Specify PV module attachment live load and requirement for supplier to assess point loads where modules attach to profile.
- Cable management: include reserved cavities or dedicated clips in profiles for cable routing and earthing conductor paths or reference separate cable trays.
Finish and fastener compatibility
- State required finish systems and explicitly address finish and fastener compatibility. For example, powder coatings on aluminium require different fastener materials than bare aluminium; stainless steel fasteners with polymer isolators are common in coastal environments.
- Specify surface preparation (degrease, etch or conversion coating) and coating thickness by micron or by AAMA standard [3].
- For anodised surfaces, specify anodic film thickness, sealing treatment and acceptance criteria for colour and uniformity.
Corrosion management
- Provide galvanic compatibility rules: avoid direct contact between aluminium and incompatible metals (e.g., untreated steel) without an isolating material. Where dissimilar metals meet in wet conditions, require barriers or sacrificial measures.
Fabrication, shop drawing review and factory evidence
What procurement must require from suppliers
- Comprehensive shop drawings for each unique profile and assembly, showing overall dimensions, hole positions with tolerances, welds and surface finish zones. Include an explicit shop drawing review process and approval timeline — shop drawing review must be part of contractual milestones.
- Material Test Reports (MTRs) for aluminium billets or extrusions showing alloy/temper and mechanical tests [2].
- Coating/finish data: batch certificates, test reports (salt spray if specified), and sample panels.
- Dimensional tolerance statement and inspection reports for a production sample.
- Factory Quality Control (FQC) plan and a list of critical control points (CCPs) with inspection hold points.
- Prototype and mock‑ups: where new extrusions or complex architectures are used, require a first‑article sample and a witnessed factory acceptance test (FAT).
Decision table: Procurement evidence checklist
| Evidence item | Purpose | Acceptance criterion |
|---|---|---|
| Material Test Reports (MTR) | Verify alloy and mechanical properties | MTR traceable to heat/batch and matching order |
| Structural calculations | Confirm section performance against project loads | Calculations signed/stamped by qualified engineer referencing code [1] |
| Shop drawings | Verify dimensions, holes and interfaces | Reviewed and approved by client/engineer prior to production |
| Finish certificates | Demonstrate coating system and thickness | AAMA or vendor spec with batch test records [3] |
| Prototype / first article | Check fit-up, finish and assembly | Client inspection and sign-off before mass production |
| Inspection and packing plan | Ensure traceable deliveries and damage prevention | Documented packing marks and handling notes |
Factory acceptance and FAI
- Define a factory acceptance test package that includes dimensional checks on a statistically relevant sample, coating thickness testing, torque tests on bolted assemblies and verification of pre‑installed elements.
- Require photographic evidence and signed FAT reports for each phase.
Traceability and marking
- Ask suppliers to provide batch/heat numbers stamped or coded on profiles and to include these on delivery paperwork to ensure traceability back to MTRs and inspection records.
Mid-article CTA If you need a tailored specification checklist, request an initial review or submit project particulars via /inquiry or email info@carportiva.com. Evaluate product options including the NordArch architectural aluminium system and review options across all systems and our sourcing guides.
Site installation, logistics and installation readiness
Preparing the site and supply chain to accept aluminium frames Installation readiness checklist
- Foundation and anchor readiness: ensure setting templates and anchor positions are checked against the approved as‑built levels; confirm grout and bolt types.
- Delivery and handling plan: flag any oversized deliveries, lifting points and off‑loading equipment; avoid stacking that damages finishes.
- Pre‑assembly and pre‑drilling: agree on scope of shop‑fit items vs field‑fit items; itemise bolts, sealants and gaskets to be provided to the installer.
- Spares and wear items: specify spare extrusions, end caps, fasteners and finishes to be supplied with the shipment.
Anchorage and torque control
- Provide anchor embedment and torque requirements and specify whether anchors are by client or supplied loose by the carport vendor.
- For bolted connections in slotted holes, set permissible slippage and final torque sequence.
Handling finishes on site
- Protect coated and anodised surfaces during lifting and storage. Do not allow steel chains or slings to contact finished aluminium. Require protective lifting points or fixtures.
Installation sequencing
- Coordinate installation sequence with other trades (PV installers, electrical trades, roofing contractors). Define milestone sign‑offs such as “frame set complete and checked” before PV mounting begins.
Installation readiness
- Request an installation readiness statement from the supplier that confirms that all pre‑punching, marking, and assembly aids are complete and that site spares and documentation (as‑built shop drawings, parts list, torque charts) will be provided. This is the installation readiness deliverable.
Implementation risks and mitigations
Common implementation risks and practical mitigations
- Scope mismatch (who supplies what)
- Risk: Gaps between supplier and contractor scope lead to delays.
- Mitigation: Detailed interface responsibility matrix in the contract.
- Tolerance accumulation and fit issues
- Risk: Fabricated assemblies do not fit due to nested tolerances.
- Mitigation: Tighten hole positional tolerances on critical interfaces; require shop drawing review and first article approval.
- Corrosion and finish failure
- Risk: Incompatible fasteners or exposure conditions accelerate corrosion.
- Mitigation: Enforce finish and fastener compatibility; specify isolate washers and stainless fasteners where needed.
- Late changes to roof drainage or PV layout
- Risk: Late changes force rework of pre‑fabricated profiles.
- Mitigation: Lock drainage and PV layouts before fabrication and include change control fees for late modifications.
- Lead time and procurement scheduling
- Risk: Custom extrusions and long lead finishes extend the programme.
- Mitigation: Include clear lead times in the tender, and identify long‑lead items early. Allow prototype and tooling time in the programme.
- Testing and acceptance failure
- Risk: Factory tests reveal non‑conformance delaying shipments.
- Mitigation: Pre‑qualify suppliers’ QC and request factory inspection rights and remedial timelines.
- Warranty and performance expectations
- Risk: Warranty claims hinge on who provided which component.
- Mitigation: Contractually tie warranty coverage to parties responsible for specific failure modes and document normal maintenance regimes.
Regulatory and contractual risks
- Ensure that all structural design responsibility, electrical interface and local permit compliance are clearly assigned in contract documents. Structural calculations must be stamped by the responsible engineer under the local licencing regime and reference the applied code (e.g., Eurocodes where applicable) [1].
Important reminder Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Six-step buyer workflow (named and actionable)
A reproducible procurement workflow to specify aluminium carport frame profiles
- Define Project Requirements (Assess)
- Document span, module usage (PV? sheltered parking?), target life, environmental exposure and key interfaces (roof/drainage/electrical).
- Deliverables: Project brief, list of critical dimensions and code basis.
- Establish Code and Load Basis (Code)
- Confirm governing code edition and load combinations (refer to project engineer).
- Deliverables: Code statement and required design live loads.
- Produce Technical Specification (Specify)
- Convert performance to measurable attributes: alloy, temper, section properties, hole tolerances, finish spec, fastener compatibility and testing requirements.
- Deliverable: Technical specification and preliminary Bill of Materials (BOM).
- Pre‑qualify Suppliers and Issue Tender (Select)
- Request evidence: MTRs, past project references, factory QA documents, lead time and prototype capability; ask for preliminary shop drawings.
- Deliverable: Shortlist with capability matrix.
- Review Shop Drawings and Factory Evidence (Approve)
- Execute shop drawing review, approve first article, confirm FAT scope and produce installation readiness statement.
- Deliverable: Approved shop drawings and FAT report.
- Manage Delivery and Site Acceptance (Install)
- Verify deliveries to packing/marking list, perform site checks, torque and sealant acceptance, and sign off on installation readiness.
- Deliverable: As‑built drawings and handover pack.
Each step should have a named owner (client engineer, procurement, supplier QC, site lead) and acceptance criteria documented in contracts.
Related B2B sourcing terms
For the same project brief, buyers may also encounter these connected search terms: architectural carport specification. They must be interpreted against the actual project scope rather than treated as independent technical guarantees.
Frequently asked questions (FAQ)
Q: How specific do I need to be about alloy and temper? A: Be explicit. Require alloy designation and temper, and demand MTRs that show mechanical properties and chemical composition [2]. “Aluminium” without alloy is insufficient for structural procurement.
Q: Can I rely on supplier standard sections to save cost? A: Yes, where standard sections meet performance criteria. But require section properties and an assessment against project loads; do not waive structural calculations.
Q: What finish standard should I specify for high‑abrasion urban environments? A: Consider high‑durability powder coatings meeting AAMA 2604/2605 or equivalent. Specify film thickness, pretreatment and test requirements (e.g., adhesion, salt spray if required) [3]. Include maintenance guidance.
Q: Who is responsible for roof drainage? A: Define this in the contract. If drainage is by the roofing contractor, the frame supplier should supply interface details. Early roof drainage coordination avoids rework.
Q: Should bolts be shop‑installed or loose for site installation? A: Where practical, shop‑ install critical alignment bolts; supply loose bolts for field connections where site tolerance take‑up is needed. Make the decision based on handling, transport constraints and field final alignments.
Q: Are stainless fasteners always required? A: Not always. Select fastener material based on exposure and substrate. In coastal or corrosive environments stainless fasteners and isolators are strongly recommended to manage galvanic corrosion.
Q: What about thermal movement for long canopies? A: Specify sliding or elongated slots at connections and provide maximum allowable movement. Thermal expansion should be evaluated by the engineer during aluminium profile selection.
Q: How do I handle late design changes? A: Implement formal change control with cost/time impact assessments. Freeze critical interfaces (PV/layout, drainage, foundations) before fabrication.
Conclusion
Specifying aluminium carport frame profiles for a commercial project is an exercise in converting functional requirements into measurable, verifiable procurement clauses and acceptance criteria. Focus on measurable attributes (material, section properties, tolerances, finish and fastening systems), require shop drawing review and factory evidence, and insist on an installation readiness deliverable that aligns with site sequencing. Use the six‑step buyer workflow to structure procurement and risk control. For product selection and system-level options review the NordArch architectural aluminium system, see other options across all systems, and consult our sourcing guides for template clauses.
If you want a tailored specification review, to request shop drawing assistance or to discuss a project, contact us via /inquiry or info@carportiva.com.
Further reading and standards (selective)
- Eurocodes provide the basis for structural design and load combinations [1].
- Aluminium material guidance and testing standards are available from The Aluminum Association [2].
- Coating and facade finish performance guidance from the American Architectural Manufacturers Association [3].
- ISO standards for dimensional tolerances and product specifications can be referenced for shop tolerance zones [4].
Legal and professional reminder This document is a procurement and decision guide and does not replace the need for project‑specific structural calculations, local permits, electrical design and approvals. Those items require a documented project basis and engagement with relevant local qualified professionals, installers, utilities and authorities.
References
- European Commission Eurocodes: https://eurocodes.jrc.ec.europa.eu/
- The Aluminum Association: https://www.aluminum.org/
- American Architectural Manufacturers Association: https://aamanet.org/
- ISO Online Browsing Platform: https://www.iso.org/obp/ui/
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion